Custom Hydraulic Manifold Blocks from Vietnam: CNC Machining Guide 2026
February 25, 2026 · 13 min read
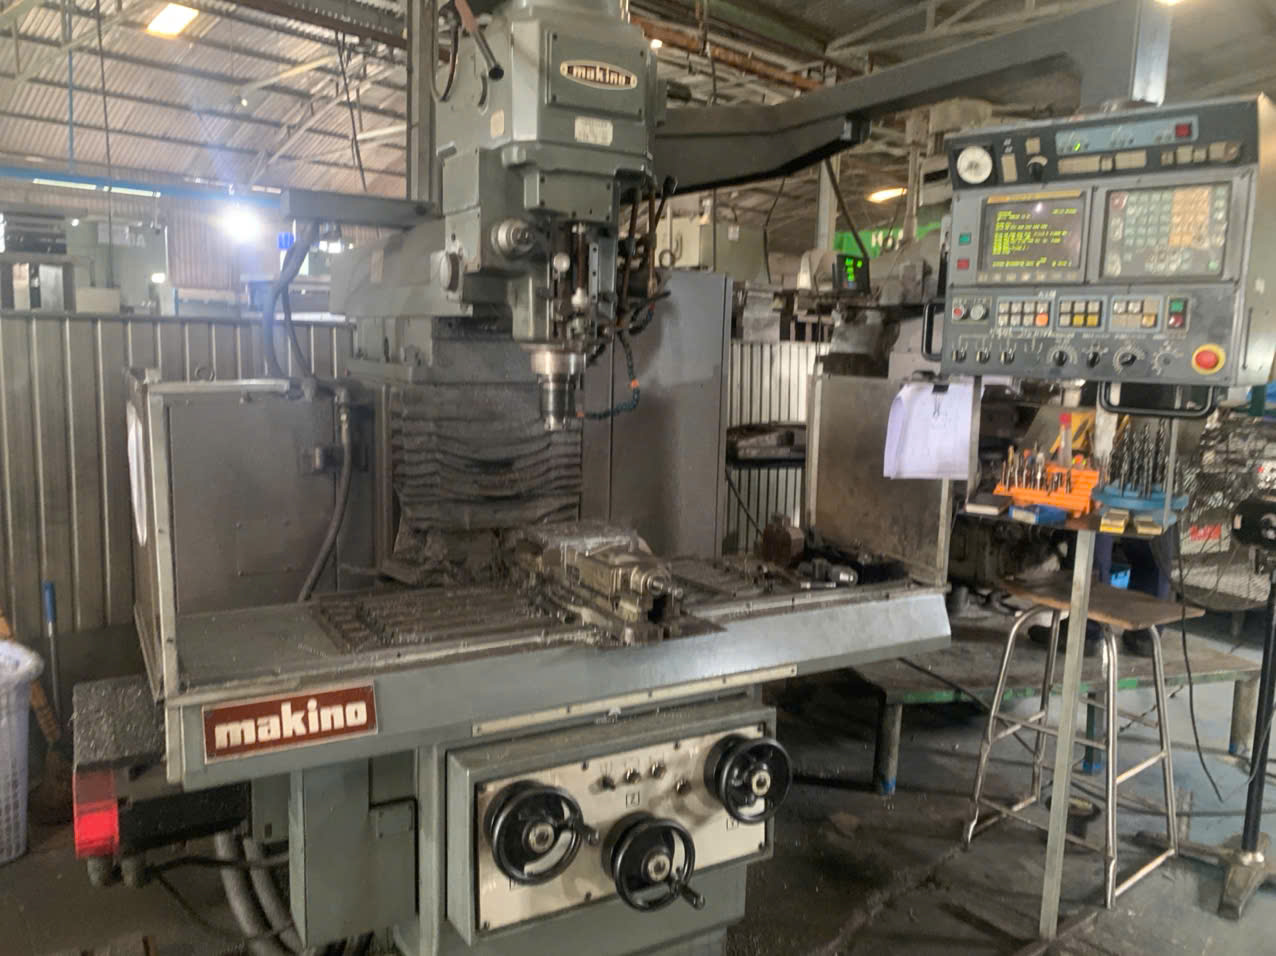
Hydraulic manifold blocks are among the highest-value CNC machined components in industrial manufacturing. A single medium-complexity manifold involves 30–60 machining operations: deep-hole drilling, precision boring for cartridge valve cavities, tapping SAE ports, and meticulous internal deburring. They demand a supplier who understands hydraulics — not just CNC machining.
Vietnam's precision CNC machining industry has matured rapidly, with shops now equipped with dedicated gun drilling machines, thermal deburring systems, and CMM inspection — the exact capabilities needed for hydraulic manifold production. Combined with 45–55% cost savings over US domestic sourcing and exemption from Section 301 Chinese punitive duties, Vietnam is emerging as the preferred China+1 source for hydraulic components.
Yes — Vietnam's precision CNC shops machine custom hydraulic manifold blocks with gun-drilled deep passages, cartridge cavities held to ±0.013mm, thermal deburring, and 100% pressure testing, delivering hydraulic components to US buyers at relief from Section 301 Chinese punitive tariffs for qualifying goods versus China's 25%.

Inside a Vietnam Technology Manufacturing Plant — CNC & Automation
Watch on YouTube
Real footage from an audited DEWIN partner factory in Vietnam.
Why Hydraulic Manifolds Require Specialist CNC Capabilities
A manifold isn't a typical machined part. The internal passage network operates at 3,000–6,000 PSI (some systems reach 10,000 PSI), and any manufacturing defect — a misaligned intersection, a loose burr, a slightly oversized valve cavity — can cause system failure, fluid leaks, or downstream component damage. Here's what makes manifold machining uniquely demanding:
- Deep-hole drilling (10:1 to 20:1 L/D ratios) — Internal passages often run 120–200 mm deep at Ø6–12 mm diameter. Gun drilling or BTA drilling maintains straightness within 0.5 mm over full depth. Standard twist drills wander beyond 5:1 L/D ratio, creating passages that miss their intersection targets.
- Cartridge valve cavities at ±0.013 mm — Every major valve manufacturer (Sun Hydraulics, Eaton, Parker, Bosch Rexroth, HydraForce) publishes cavity specs per ISO 7789 / NFPA T3.5.31. Cavity diameter tolerance is typically ±0.013 mm (±0.0005") with surface finish Ra 0.4–0.8 µm. This is grinding-territory precision on a bored hole.
- Internal deburring and cleanliness — Cross-drilled intersections create burrs that must be completely removed. Loose burrs contaminate hydraulic fluid, score valve spools, and destroy pump seals. Thermal deburring (TEM), abrasive flow machining (AFM), or precision flexible honing is required. Cleanliness standard: NAS 1638 Class 8 or ISO 4406 18/16/13.
- 100% pressure testing — Every manifold must pass proof pressure testing at 1.5× working pressure (ISO 4413 / NFPA T2.24.1). A 5,000 PSI system requires 7,500 PSI proof test — zero leakage, 3-minute minimum hold.
Vietnam's CNC Capabilities for Manifold Production
Vietnam's precision machining sector has invested heavily in equipment and processes that directly serve hydraulic manifold production:
- Gun drilling machines — Multiple Vietnamese CNC shops in our network operate dedicated gun drilling equipment capable of Ø3–25 mm, depths to 500 mm, with straightness control <0.5 mm per 100 mm depth. Key brands in use: TBT, Gühring, and SIG Sauer gun drilling units.
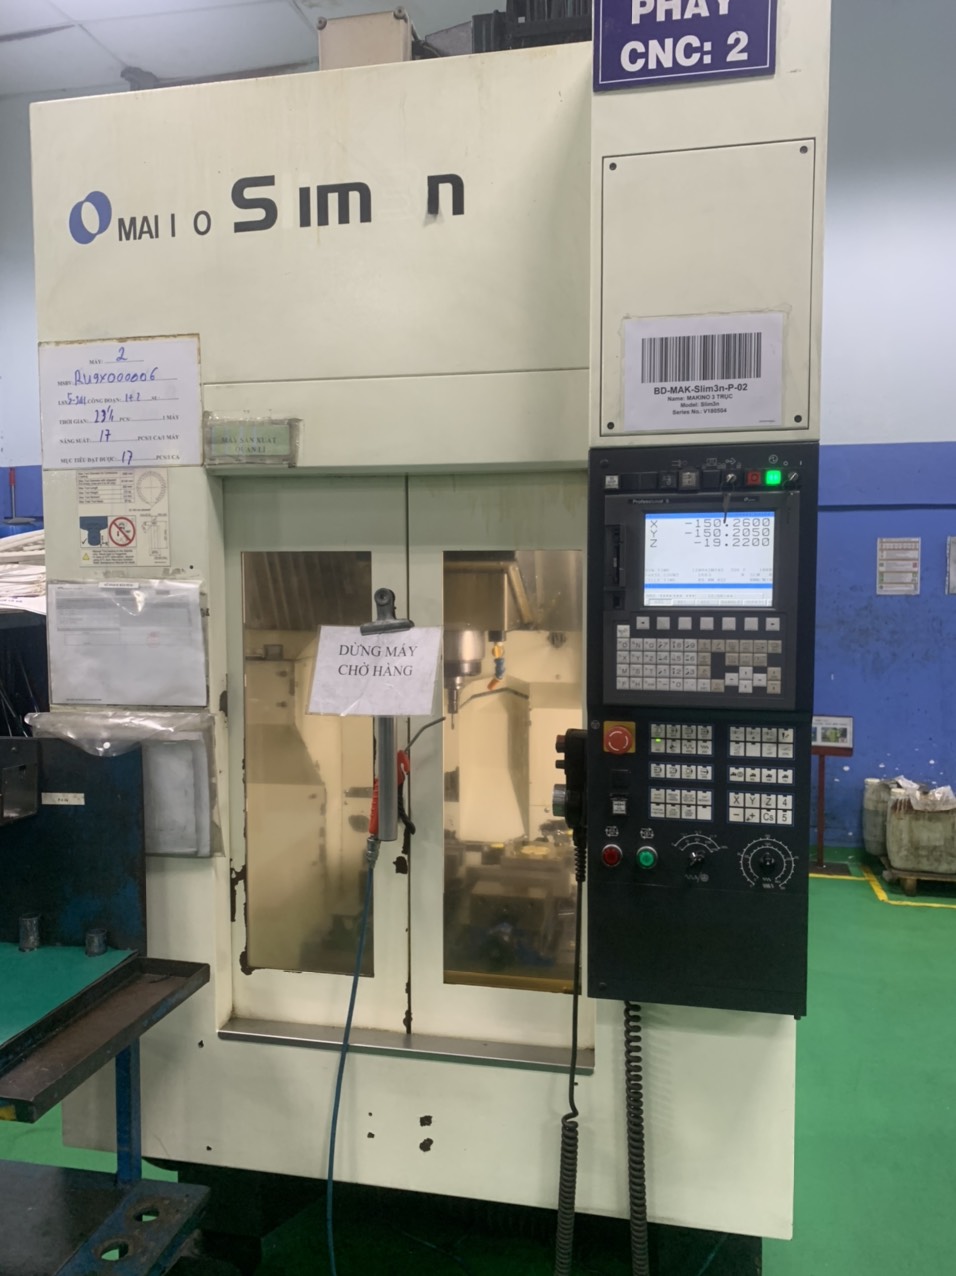
- Horizontal machining centers with 4th axis — Ideal for manifold production: machine 4 faces in a single setup, minimizing fixture changes and improving positional accuracy between faces. Common machines: Mazak HCN-5000, Okuma MA-500HII, Doosan NHP-5000.
- Thermal deburring (TEM) — Available at select shops for batch deburring of manifolds. Removes burrs from all internal intersections simultaneously using a controlled gas explosion — superior consistency to manual methods.
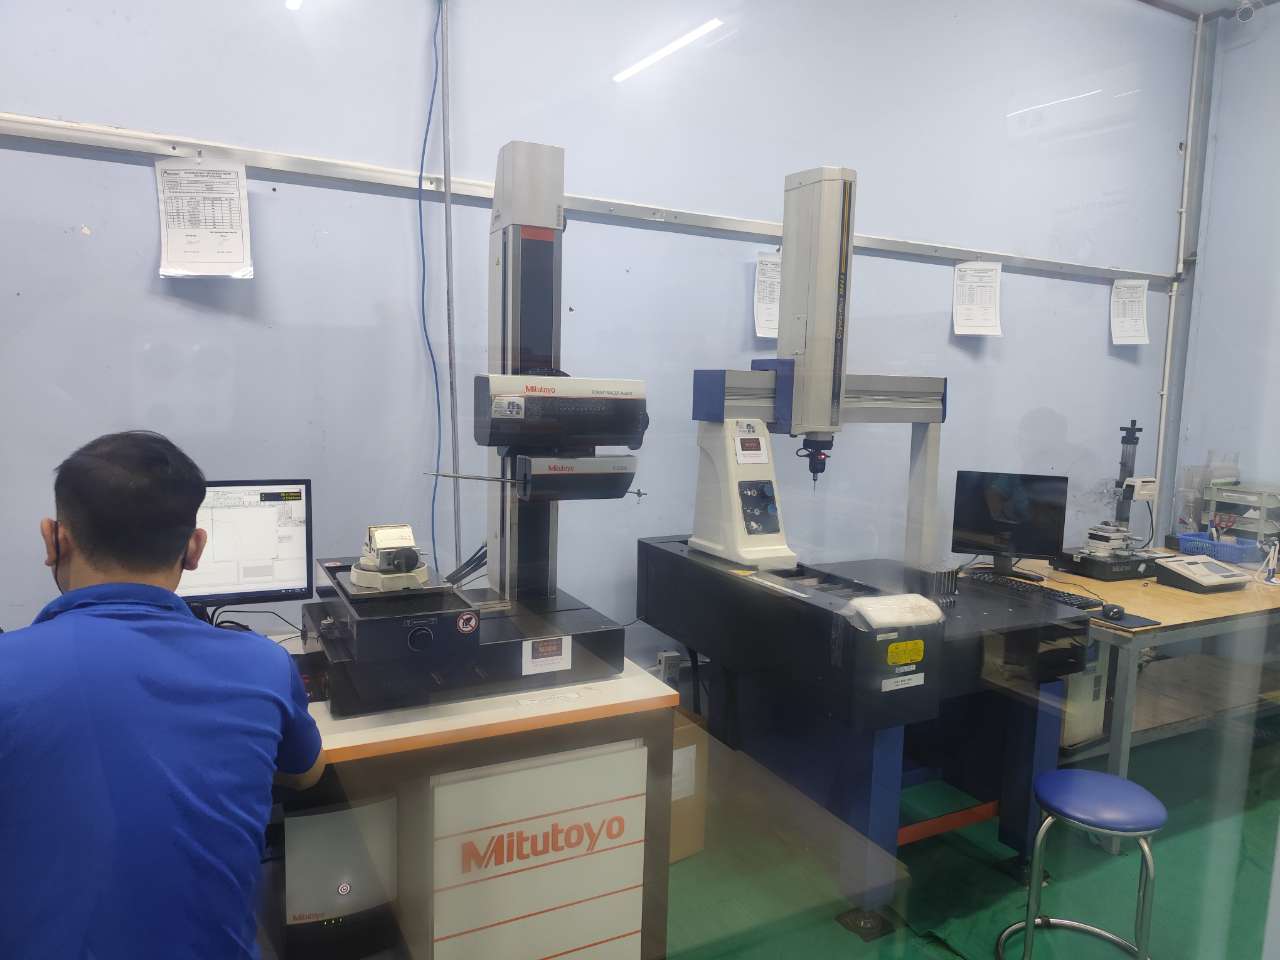
- CMM inspection — Zeiss, Mitutoyo, and Hexagon CMMs for verifying cartridge cavity dimensions, port positions, and mounting surface flatness. First article inspection reports (FAIR) per AS9102 format available.
- Pressure test benches — Dedicated hydraulic test stands with automated pressure logging, capable of testing to 10,000+ PSI. Test certificates with pressure/time curves provided.
Material Selection for Manifolds Made in Vietnam
All standard manifold materials are readily available from Vietnamese steel and aluminum distributors:
- 6061-T6 Aluminum — Up to 3,000 PSI. Best for mobile hydraulics, lightweight applications. Vietnam price: $3.50–5/kg. Fastest machining — lowest cost per block. Hard anodize (Type III) available domestically.
- A36 / S235 Carbon Steel — Up to 5,000 PSI. Industrial workhorse. Vietnam price: $1.20–2.50/kg. Most common choice for standard industrial hydraulic power units.
- 4140 / 42CrMo4 Alloy Steel — Up to 6,000+ PSI. For high-pressure applications. Vietnam price: $2.80–4.50/kg. Heat treatment to HRC 28–32 available in-country from certified heat treaters.
- 316 Stainless Steel — Corrosive/washdown environments. Vietnam price: $5.50–9/kg. Passivation per ASTM A967 available.
- Ductile Iron (GGG-50 / 65-45-12) — For high-volume programs (200+/year). Cast near-net-shape at Vietnamese foundries, then finish-machined. Casting tooling: $1,500–6,000 (30–40% less than China).
Pricing: Vietnam vs. US vs. China for Hydraulic Manifolds
Real 2026 price comparisons from our supplier network. Medium manifold: 200×150×100 mm, 6061-T6 aluminum, 20 cavities/ports, gun-drilled passages, TEM deburred, pressure tested.
For US buyers, Vietnam matches or beats China's landed manifold cost: a medium aluminum block lands near $144–277 at qty 25 and $67–133 at qty 500, versus China's tariff-inflated $200–350 and $94–163.
Qty 25 Order
- US domestic: $380–550/block
- China: $160–280/block + 25% Section 301 tariff = $200–350 landed
- Vietnam (via Dewin): $140–270/block + 2.5% duty = $144–277 landed
Qty 100 Order
- US domestic: $250–380/block
- China: $110–190/block + 25% tariff = $138–238 landed
- Vietnam (via Dewin): $95–180/block + 2.5% duty = $97–185 landed
Qty 500 Order
- US domestic: $175–260/block
- China: $75–130/block + 25% tariff = $94–163 landed
- Vietnam (via Dewin): $65–130/block + 2.5% duty = $67–133 landed
Key takeaway: Vietnam matches or beats China's landed cost for US buyers — and that's before considering the supply chain risk reduction of not being dependent on a single tariff-exposed source.
Tariff and Trade Advantages
The tariff math is compelling for US hydraulic OEMs:
- Section 301 tariffs on China: 25% on hydraulic components (HTS 8412.90, 7616.99). This applies to manifold blocks, valve bodies, cylinder components, and most machined hydraulic parts.
- Vietnam MFN duty rate: 0–5% depending on HTS classification. Aluminum articles: 2.5%. Steel articles: 2.5–3.4%. Hydraulic parts: 2–3.5%.
- CPTPP membership: Vietnam is a CPTPP member. While the US is not currently a signatory, Vietnam's trade agreements with other markets (EU-Vietnam FTA, RCEP) keep its export infrastructure well-developed and customs-efficient.
- Net tariff savings: 20–23% tariff advantage over China on identical parts. On a $200/block manifold at 500 blocks/year, that's $20,000–23,000/year in tariff savings alone.
Critical Tolerances: What to Spec in Your RFQ
Tier your tolerances to optimize cost. Here's the practical breakdown:
- ±0.013 mm: Cartridge valve cavity diameters only. Per valve manufacturer spec sheet. This is the only dimension that truly needs sub-0.025 mm tolerance.
- ±0.05 mm: Cavity depths, SAE port spot face perpendicularity, mounting surface flatness (ISO 4401 interfaces for D03/D05/D07 valves).
- ±0.1 mm: External block dimensions, non-critical hole positions, port thread depths.
- ±0.25 mm: Internal passage positions (non-intersecting), plug hole locations.
Cost impact: Properly tiered tolerances save 30–40% vs. blanket tight tolerances. Vietnamese shops we work with are experienced with this approach — they won't upsell you on unnecessary precision.
RFQ Checklist for Hydraulic Manifolds
Provide these items for the fastest, most accurate quote:
- Hydraulic schematic — Shows circuit function, flow paths, pressure zones. Helps the machinist understand what the block does.
- 3D CAD model + 2D drawing — STEP file preferred. Drawing must call out all critical dimensions with GD&T, material spec, and surface finish requirements.
- Valve specifications — Manufacturer, model, and cavity spec for every cartridge valve. Example: "Sun CBCA-LHN, T-11A cavity."
- Port specifications — SAE J1926 O-ring boss (preferred) or NPT. Size for every port. Labeling that matches your schematic.
- Working pressure per section — Allows optimization of wall thickness and passage sizing.
- Testing requirements — Proof pressure, hold time, acceptable leakage (should be zero for most applications).
- Quantity and schedule — First article quantity, production quantity, annual forecast, delivery schedule.
Quality Assurance Process
Our manifold production quality process for Vietnam-sourced blocks:
- Material certification — Mill test reports (MTR) for every heat/lot of material used.
- In-process inspection — Cavity dimensions checked after boring, before deburring. Passage depths verified during drilling.
- Deburring verification — Borescope inspection of accessible intersections. Cleanliness particle count per NAS 1638 Class 8.
- CMM first article report — Full dimensional report per AS9102 format for first 1–3 pieces. All critical dimensions verified.
- 100% pressure test — Every block individually tested at 1.5× working pressure. Logged pressure/time curve provided.
- Final inspection + packing — Visual inspection, thread gauging, surface finish verification. VCI paper wrapping for steel blocks to prevent corrosion during transit.
Lead Times and Logistics
- First article (1–3 blocks): 2–3 weeks production + 1 week air freight = 3–4 weeks total
- Production (25–100 blocks): 3–4 weeks production + 1 week air or 3–4 weeks sea = 4–8 weeks total
- Production (500+ blocks): 5–6 weeks production + 3–4 weeks sea freight = 8–10 weeks total
Air freight for manifold blocks typically runs $5–8/kg (DDP to US port). A 25-piece order of medium aluminum manifolds (~75 kg total) costs approximately $400–600 for air freight. Sea freight (LCL) drops to $0.80–1.50/kg but adds 3–4 weeks.
Get a Hydraulic Manifold Quote
Send us your hydraulic schematic and manifold drawing. We'll return a detailed quote within one business day — with per-block pricing, material options, pressure test documentation, and lead time from our Vietnam CNC machining network.
Get Your Free Manifold Quote →
Frequently Asked Questions
Which manifold dimensions actually need ±0.013 mm tolerance?
Cartridge valve cavity diameters are the only dimensions that genuinely need sub-0.025 mm precision, held to ±0.013 mm per the valve manufacturer's spec sheet. Cavity depths, SAE port spot face perpendicularity, and mounting surface flatness work at ±0.05 mm, and external block dimensions at ±0.1 mm. Tiering this way saves 30–40% versus blanket tight tolerances.
What proof pressure test should I require on manifolds from Vietnam?
Proof pressure testing at 1.5× working pressure on every block is the standard requirement — a 5,000 PSI system means a 7,500 PSI test with zero leakage and a three-minute minimum hold, per ISO 4413 / NFPA T2.24.1. Vietnamese test benches handle 10,000-plus PSI and supply certificates with pressure/time curves.