
Choosing the wrong surface treatment for custom stamping parts can ruin a good design. I have seen bare brackets rust in transit before our team stepped in to fix the spec.
To choose the right surface treatment for custom stamping parts, match the finish to the part’s operating environment, base material, and function. Define corrosion, conductivity, appearance, and thickness requirements early—before tooling—then confirm compliance needs like RoHS and validate with salt spray or adhesion testing.
That is the short answer. Now let me walk you through the details, step by step, so you can specify the right finish with confidence.
What surface treatment options are available for custom stamping parts?
A buyer once sent me a drawing that simply said "plated." That single word triggered three rounds of emails. Our engineers needed to know which plating, how thick, and why.
Common surface treatment options for custom stamping parts include zinc, nickel, tin, and chrome plating; powder coating and e-coating; anodizing for aluminum; passivation and electropolishing for stainless steel; plus deburring, polishing, and cleaning as preparatory or finishing steps.
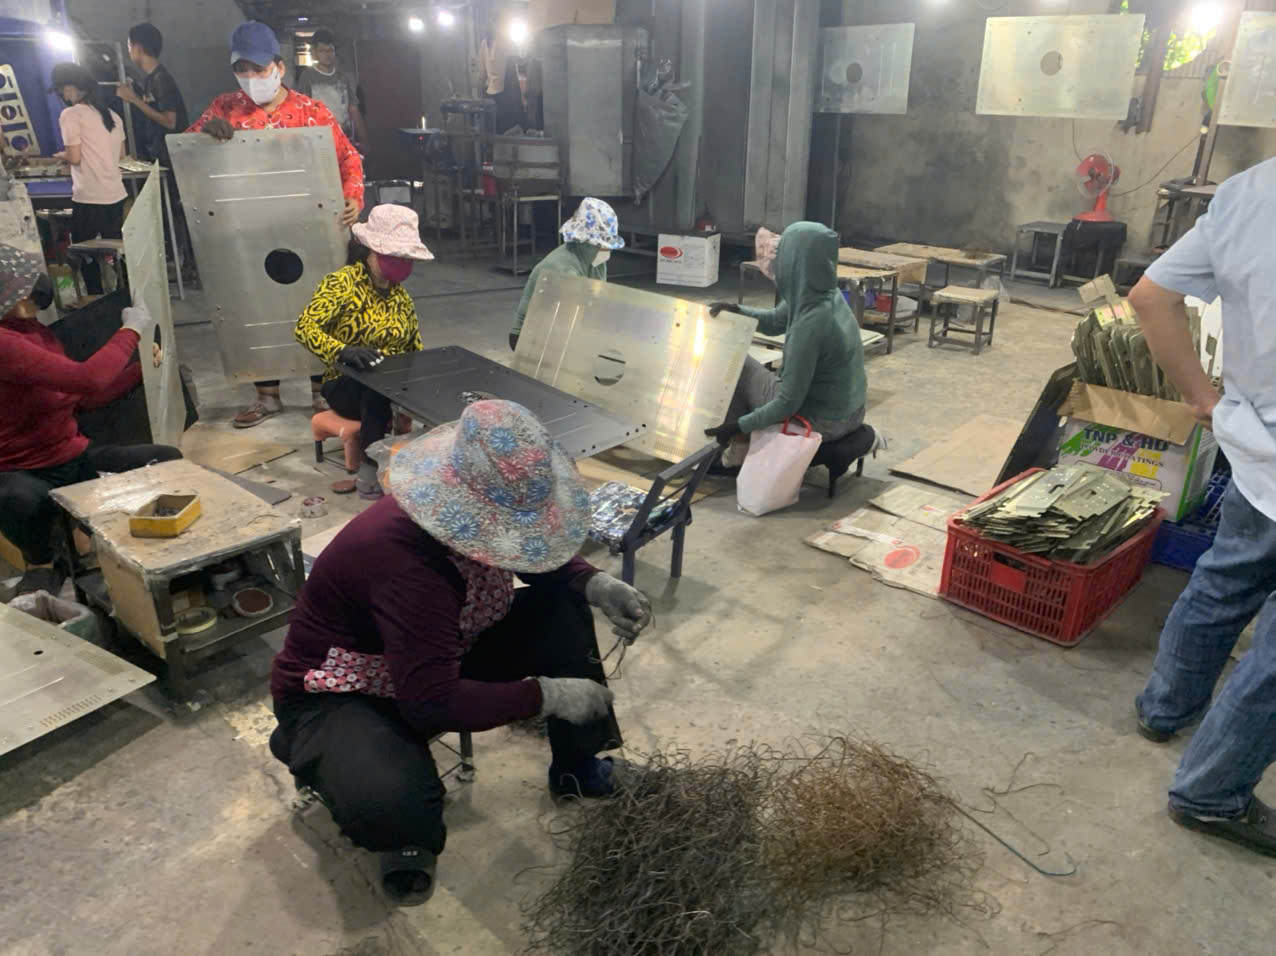
Each finish family solves a different problem. So the first step is understanding what each one actually does. In our sourcing projects across Vietnam and other Asian countries, these are the treatments we quote most often.
The main finish families
Plating adds a thin metal layer to the stamped part. Zinc plating 1 is the workhorse for carbon steel brackets. It is cheap and gives solid corrosion protection. Nickel plating 2 adds wear resistance and a brighter look. Tin plating supports solderability 3 for electrical parts. Chrome adds hardness and a decorative shine.
Coatings work differently. Powder coating 4 sprays a polymer layer and bakes it on. It gives thick, durable, colorful coverage. E-coating uses an electrical charge to pull paint into every recess, which helps on complex bends.
Then there are subtractive or preparatory processes. Deburring removes sharp edges left by the die. Electropolishing smooths micro-irregularities on stainless steel 5. Cleaning strips oils and stamping lubricants so later coatings can adhere.
| Treatment | Best For | Key Benefit | Typical Limitation |
|---|---|---|---|
| Zinc plating | Carbon steel parts | Low-cost corrosion protection | Moderate lifespan outdoors |
| Nickel plating | Wear surfaces, connectors | Hardness, bright finish | Higher cost than zinc |
| Tin plating | Electrical terminals | Solderability, conductivity | Soft surface |
| Powder coating | Visible housings, brackets | Thick, decorative, durable | Adds thickness, not conductive |
| E-coating | Complex geometries | Uniform full coverage | Limited color options |
| Anodizing | Aluminum stampings | Corrosion + wear resistance | Aluminum only |
| Passivation | Stainless steel | Restores corrosion resistance | Not decorative |
| Electropolishing | Stainless, medical parts | Smooth, clean surface | Slight material removal |
One more decision sits behind all of these: pre-plating versus post-plating. Pre-plated coil stock can lower cost. But stamping cuts through the coating, leaving bare edges. Post-plating covers everything, including cut edges, which matters in harsh environments.
How do I match surface treatment to my part's function and environment?
The hardest trade-off we weigh on stamping projects is protection versus thickness. A thicker coating survives longer outdoors, but it can also jam a tight-tolerance mating slot.
Match the treatment by ranking your priorities: corrosion resistance for humid or outdoor use, conductivity for electrical contacts, wear resistance for sliding parts, and cosmetics for visible components. Then verify the finish suits your base metal and does not violate dimensional tolerances.

Start with the environment, because it eliminates options fast. A bracket mounted inside a dry electronics enclosure needs far less protection than a clip exposed to road salt. If your part will see rain, salt spray 6, high humidity, or chemicals, you need robust corrosion protection, full stop.
A simple four-step selection framework
- Define the environment. Indoor, outdoor, marine, chemical exposure, or temperature swings.
- Rank the functions. Corrosion resistance, conductivity, solderability, wear, or appearance.
- Check the base material. The substrate narrows your realistic options.
- Verify geometry and tolerances. Confirm the coating thickness fits your holes, slots, and mating features.
Material-specific guidance
The base metal matters more than most buyers expect. In our experience exporting to the US, this table settles most early debates:
| Base Material | Typical Treatments | Notes |
|---|---|---|
| Carbon steel | Zinc plating, powder coat, e-coat | Needs strong corrosion protection |
| Stainless steel | Passivation, electropolishing | Often no coating needed, just surface restoration |
| Aluminum | Anodizing, chromate conversion | Anodizing is the common default |
| Copper / brass | Tin, nickel, or precious-metal plating | Finish must preserve conductivity |
Geometry deserves special attention on stamped parts. Deep draws, sharp bends, and small punched holes can cause uneven coating buildup or coverage gaps. Our engineers flag features like elongated slots on bracket drawings because plating thickness can shrink the effective opening. If a hole must stay conductive or stay bare, call out masking on the drawing. Doing this before tooling avoids expensive rework later.
Finally, do not forget compliance. Automotive, medical, and consumer projects often restrict certain coatings. Confirm RoHS or REACH requirements 7 before you approve any finish spec.
What factors affect the cost of surface treatment for stamping parts?
Early in one project, a client asked why nickel plating doubled his bracket quote versus zinc. The answer taught him how finish costs really work, so let me share it here.
Surface treatment cost depends on the coating material, coating thickness, part size and geometry, order volume, masking requirements, testing and documentation needs, and whether the finisher is in-house or outsourced. Precious-metal plating and complex masking drive the biggest cost increases.

Finishing cost is rarely one number. It is a stack of smaller decisions. Understanding each layer helps you negotiate better quotes and cut waste from your spec.
The main cost drivers
Material choice sits at the top. Zinc is inexpensive. Nickel costs more. Gold or silver plating for connectors costs far more again. Specify the cheapest finish that meets your real requirement, not the fanciest one.
Thickness comes second. Plating cost scales with deposit thickness. A drawing that says "zinc plate, 8 microns minimum" is cheaper and clearer than one that just says "zinc plate," which invites either over-quoting or under-delivery.
Geometry and masking add labor. Every masked hole or bare zone requires manual work per part. On high-volume runs, masking can cost more than the coating itself.
Volume changes the math. Barrel plating suits small stampings in bulk and is cheap. Rack plating gives better cosmetic quality but costs more per piece. Powder coating gets efficient at high volume.
| Cost Factor | Low-Cost Scenario | High-Cost Scenario |
|---|---|---|
| Coating material | Zinc | Gold, silver, hard chrome |
| Thickness | Thin functional layer | Heavy-duty outdoor spec |
| Process type | Barrel plating, bulk | Rack plating, hand masking |
| Volume | Large steady runs | Small prototype batches |
| Testing | Visual inspection only | Salt spray + adhesion + reports |
| Logistics | In-house finishing | Outsourced with extra transport |
Testing and documentation matter too. Salt spray hours, cross-hatch adhesion tests, and compliance certificates all add cost and lead time. They are worth it for critical parts. They are wasted money on hidden, low-risk components. On our projects, we help clients decide which tests genuinely protect them and which just inflate the quote.
How can I ensure consistent surface treatment quality when sourcing from Asian suppliers?
A lesson I learned the hard way: a stamping shop can be excellent at forming metal and still hand your parts to a mediocre plating subcontractor. Our team in Vietnam audits both.
Ensure consistency by writing a complete finish specification, auditing both the stamper and the finisher, requiring approved samples before mass production, defining salt spray and adhesion test criteria, and using PPAP-style documentation with final inspection before shipment.

Distance makes finish problems expensive. A color mismatch or thin plating discovered in a US warehouse means rework, air freight, or scrapped stock. So the goal is simple: catch problems before the parts leave Asia.
Write a spec that leaves no room for guessing
Most finish disputes trace back to vague drawings. A strong specification includes the coating type and standard, minimum thickness, color and gloss expectations, masked areas, and required tests. When we run supplier audits in Vietnam, we check whether the finisher can actually measure and hold these values, not just promise them.
Control the process, not just the outcome
Here is the workflow we apply on custom parts projects:
- Supplier audit. Verify the plating line, chemical controls, and thickness measurement equipment. Ask who the finishing subcontractor is, and audit them too.
- Golden samples. Approve physical samples for color, gloss, and texture. Cosmetic judgments by email photos fail constantly.
- First article and PPAP. Lock the process with documented parameters before mass production. This is core to how we deliver "right first time" results.
- In-process checks. Thickness readings and visual checks during the run, not only at the end.
- Final inspection. Verify salt spray results, adhesion tests, thickness reports, and packaging that protects the finish in transit.
Packaging deserves its own line. Plated stampings can scratch or develop white rust if packed damp or loose. We specify VCI paper or bags and interleaving for cosmetic parts, then manage door-to-door logistics so the finish that passed inspection is the finish that arrives.
Payment structure helps too. With open account terms, our clients hold leverage until parts are verified, which keeps everyone focused on getting the finish right the first time.
Conclusion
The wrong finish causes rust claims, rejected shipments, and rework. Specify the surface treatment for custom stamping parts early, match it to environment and function, and verify it before shipment. Our team is glad to help you get it right the first time.
Frequently Asked Questions
What surface treatment options are available for custom stamping parts?
A buyer once sent me a drawing that simply said "plated." That single word triggered three rounds of emails. Our engineers needed to know which plating, how thick, and why.
How do I match surface treatment to my part's function and environment?
The hardest trade-off we weigh on stamping projects is protection versus thickness. A thicker coating survives longer outdoors, but it can also jam a tight-tolerance mating slot.
What factors affect the cost of surface treatment for stamping parts?
Early in one project, a client asked why nickel plating doubled his bracket quote versus zinc. The answer taught him how finish costs really work, so let me share it here.
Footnotes
1. Explains the electroplating process behind this common low-cost corrosion protection method. ↩︎
2. Provides technical background on this wear-resistant, bright decorative plating option. ↩︎
3. IPC sets electronics industry standards for solderability referenced in tin plating selection. ↩︎
4. Background on the polymer spray-and-bake process referenced for durable stamped part finishes. ↩︎
5. Authoritative industry body on stainless steel properties relevant to electropolishing decisions. ↩︎
<span id="footn