
When we started auditing fabrication suppliers across Vietnam and China for our U.S. clients, one problem kept surfacing — hidden weld defects in custom sheet metal parts that passed visual inspection but failed in the field. These escapes cost our buyers thousands in rework, returns, and lost trust. The root cause was almost always the same: the supplier lacked verified NDT capabilities 1, or worse, had equipment sitting idle and uncalibrated. Evaluating supplier NDT capabilities and equipment is not optional — it is the single most important quality gate between a conforming part and a costly field failure.
To evaluate supplier NDT capabilities for sheet metal fabrication, verify their specific non-destructive testing methods, confirm equipment calibration traceable to national standards, demand Cpk data and First Article Inspection reports, and ensure NDT personnel hold recognized certifications like ASNT-TC-1A Level II or III.
This guide breaks down the exact steps, questions, and documentation you need to confirm a supplier’s NDT strength before placing your order. Let’s walk through each critical area.
How do I assess if a sheet metal supplier has the right NDT equipment for my custom parts?
A lesson we learned early in our supplier audit process was that equipment lists alone mean nothing. During a facility visit in Vietnam, we found a supplier advertising radiographic testing capability — but the X-ray unit had not been calibrated in over two years.
Assess a supplier's NDT equipment by requesting a detailed inventory with model numbers, installation dates, calibration records traceable to NIST or ISO standards, and maintenance schedules — then verify these documents during an on-site or virtual audit before awarding any production contract.

Getting this right requires you to go far beyond a supplier's marketing claims. Here is how we approach it on every sourcing project.
Start with a Detailed Equipment Inventory
Ask the supplier to provide a full list of NDT equipment. This list should include the equipment type, manufacturer, model number, year of installation, and last calibration date. Vague answers like "we have ultrasonic testing" are red flags. You want specifics — for example, "Olympus Epoch 650 ultrasonic flaw detector, installed 2022, calibrated March 2024."
Match Equipment to Your Part Requirements
Not every NDT method suits every part. A precision-engineered mounting bracket with multiple weld joints — like the mirrored brackets we frequently source, featuring sharp bends, cutouts, and visible weld marks — needs different testing than a simple flat panel. Consider the material, geometry, and defect types you are most concerned about.
| Part Feature | Primary Concern | Best NDT Method |
|---|---|---|
| Welded joints on steel brackets | Internal weld voids, cracks | Ultrasonic Testing (UT) 2 or Radiographic Testing (RT) |
| Surface of non-porous aluminum parts | Surface-breaking cracks | Dye Penetrant Testing (LPI) |
| Ferromagnetic steel components | Near-surface defects | Magnetic Particle Inspection (MPI) 3 |
| Critical wall thickness areas | Material thinning | Ultrasonic Thickness Gauging |
Verify Calibration and Traceability
NDT equipment calibration must be traceable to national or international standards such as NIST or ISO 17025 4. Ask for calibration certificates — not just a statement. Check the calibration interval. Most NDT equipment requires annual calibration, but high-use tools may need it more frequently. If calibration is overdue, the test results from that equipment are unreliable.
In-House vs. Subcontracted NDT
We always prefer suppliers who perform NDT in-house. When a supplier subcontracts testing, turnaround slows down, traceability of NDT results becomes harder to verify, and communication gaps increase. If the supplier does subcontract, ask for the subcontractor's qualifications and audit records.
Equipment Age and Technology
Older equipment is not automatically bad, but it must be well-maintained. Ask about the supplier's preventive maintenance program. Modern equipment — such as phased array ultrasonic units or digital radiography systems — can offer faster, more accurate results and better digital data capture for long-term traceability.
Which non-destructive testing methods are most critical for my high-precision sheet metal projects?
One trade-off we weigh on nearly every project is whether to specify a single NDT method or require multiple methods for different features on the same part. The answer depends on the part geometry, material, and where failure would be most costly.
For high-precision sheet metal projects, ultrasonic testing and dye penetrant inspection are the most critical non-destructive testing methods — ultrasonic testing detects internal flaws and measures thickness, while dye penetrant inspection reveals surface cracks invisible to the naked eye.
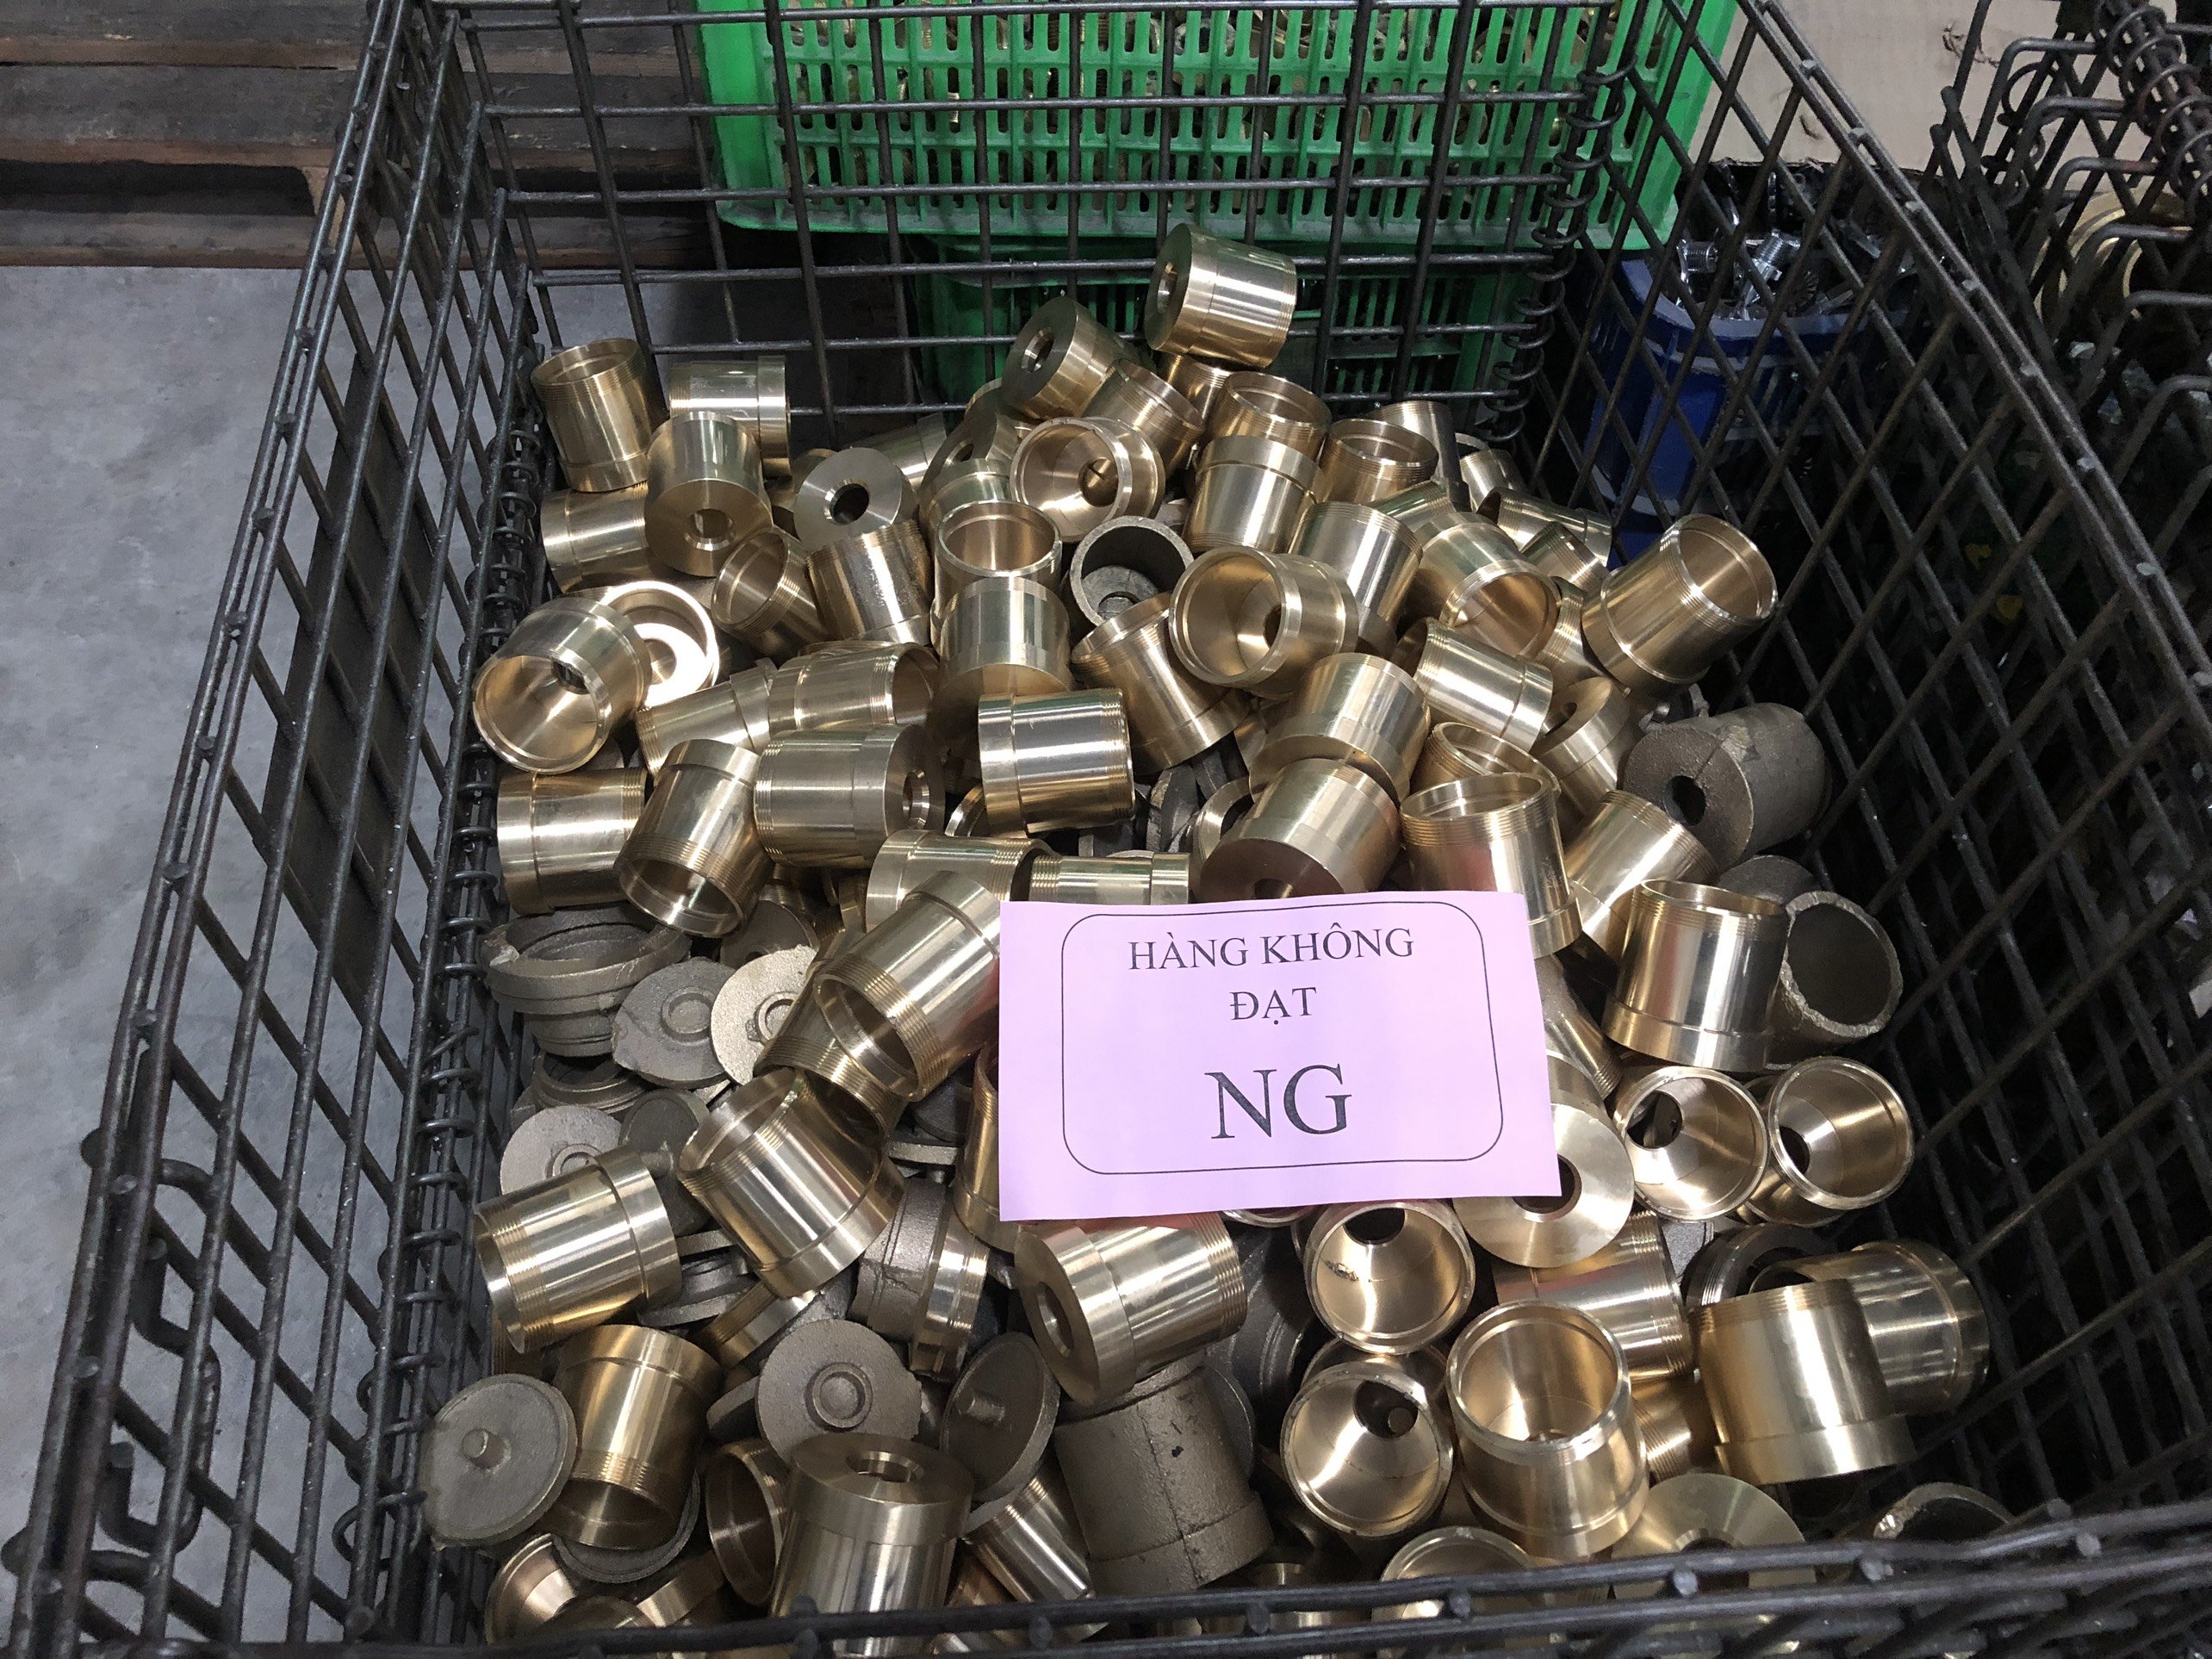
Choosing the right method — or combination of methods — is essential. Here is a practical breakdown of the most common NDT methods used in sheet metal fabrication and when each one matters most.
Ultrasonic Testing (UT)
Ultrasonic testing uses high-frequency sound waves to detect internal flaws, measure material thickness, and identify delaminations. It is highly effective for weld inspection techniques on thicker sheet metal components. For the heavy-duty mounting brackets we source — with multiple weld joints and complex folds — UT is often the first method we specify.
Radiographic Testing (RT)
Radiographic inspection uses X-rays or gamma rays to create images of internal structures. It excels at finding voids, inclusions, and incomplete weld penetration. However, it requires strict environmental and safety compliance protocols, especially regarding radiation. Not every shop floor can safely accommodate RT equipment.
Magnetic Particle Inspection (MPI)
MPI detects surface and near-surface defects in ferromagnetic materials like carbon steel. It is fast, relatively inexpensive, and effective for finding cracks at weld toes. But it does not work on non-ferromagnetic materials like aluminum or stainless steel.
Dye Penetrant Inspection (LPI)
Liquid penetrant inspection is versatile. It works on almost any non-porous material. Dye Penetrant Inspection (LPI) 5 A colored or fluorescent dye is applied to the surface, drawn into any cracks by capillary action, and then made visible with a developer. It is ideal for material defect detection on surface-breaking flaws in aluminum and stainless steel sheet metal.
| NDT Method | Detects | Best For | Limitations |
|---|---|---|---|
| Ultrasonic Testing (UT) | Internal flaws, thickness variation | Thick welds, critical joints | Requires skilled operator, surface prep needed |
| Radiographic Testing (RT) 6 | Internal voids, inclusions, porosity | Complex weld joints, castings | Radiation safety requirements, higher cost |
| Magnetic Particle (MPI) | Surface and near-surface cracks | Ferromagnetic steel parts | Not usable on aluminum or stainless steel |
| Dye Penetrant (LPI) | Surface-breaking cracks | All non-porous metals | Cannot detect subsurface defects |
Combining Methods for Full Coverage
For high-precision parts, a single method is rarely enough. We often specify UT for internal weld integrity combined with LPI for surface crack detection. This layered approach gives the most complete picture of part quality. The acceptance criteria for NDT should be defined clearly in your purchase order or drawing — do not leave it to the supplier's discretion.
Industry-Specific Requirements
If your parts go into aerospace, automotive, or energy applications, industry NDT standards may dictate which methods are mandatory. For example, aerospace programs often require NADCAP-accredited NDT processes. Make sure you communicate these requirements at the RFQ stage, not after production starts.
How can I verify that my supplier's NDT staff are qualified to meet my strict quality requirements?
A buyer interaction last year highlighted this issue sharply. A U.S. client received a batch of brackets with passing NDT reports — but the reports were signed by an operator with no formal certification. When we investigated, the "inspector" had learned on the job with no structured training. The parts were re-inspected by a certified technician, and two out of fifteen had rejectable indications.
Verify NDT staff qualifications by requiring proof of NDT personnel certification to recognized standards like ASNT-TC-1A or ISO 9712, confirming the certification level matches the testing method performed, and checking that certifications are current and issued by an accredited body.

NDT is only as good as the person performing and interpreting the test. Here is how to confirm your supplier's team is truly qualified.
Understand Certification Levels
The most widely recognized NDT personnel certification standard is ASNT-TC-1A 7 (American Society for Nondestructive Testing). It defines three levels:
| Level | Role | Capability |
|---|---|---|
| Level I | Technician | Performs tests under supervision, follows written procedures |
| Level II | Inspector | Sets up tests, interprets results, writes reports independently |
| Level III | Expert | Develops procedures, trains others, selects methods, evaluates standards |
For routine production inspection, Level II is the minimum you should accept. Level I technicians should always work under Level II or III supervision.
Request Certification Copies
Ask for copies of each NDT operator's certification card or certificate. Check the issuing body, the specific NDT method covered, and the expiration date. Certifications typically require renewal every three to five years, including re-examination. Expired certifications mean the inspector is not qualified.
Verify Training Programs
Beyond individual certifications, a strong supplier maintains a documented training program. This program should include initial qualification, periodic re-certification, and ongoing practical experience requirements. During our supplier audits, we ask to see training records and exam results — not just certificates.
Look for a Written Practice
Under ASNT-TC-1A, the employer is responsible for developing a "Written Practice" — a document that defines how NDT personnel are qualified, certified, and re-certified within that organization. Ask to review this document. If the supplier cannot produce it, their certification program may lack structure.
Cross-Check with the Quality Management System
The supplier's quality management system — whether ISO 9001, AS9100, or another framework — should reference NDT personnel qualifications. During an audit, check that the QMS procedures align with actual practice on the shop floor. Paper certifications without active enforcement are a common gap we find.
What specific NDT reports should I request to guarantee my order is right the first time?
Getting it right the first time is the promise our clients care about most — and it is the promise that falls apart fastest when documentation is weak. On a recent project involving custom mounting brackets with multiple weld joints and pre-drilled mounting holes, we required full NDT documentation before shipment. That documentation caught two parts with marginal weld penetration that would have caused assembly failures at the client's facility.
Request First Article Inspection reports with measured dimensions, NDT test reports referencing applicable standards and acceptance criteria, Cpk/Cpk process capability data for critical dimensions, calibration certificates for all test equipment, and Non-Conformance Reports with root cause analysis for any deviations found.
Documentation is your evidence. Without it, you are trusting — not verifying. Here is the specific documentation package we require on every project.
First Article Inspection (FAI) Reports
An FAI report compares actual measured dimensions against drawing tolerances for the first production piece. First Article Inspection (FAI) reports 8 It confirms the process can produce conforming parts. We require FAI reports formatted per AS9102 or equivalent, with every dimension measured and recorded — not just critical ones. This report should include material certifications, process parameters, and NDT results for the first article.
NDT Test Reports
Each NDT test report should include:
- Part identification and serial number
- NDT method used
- Equipment identification and calibration status
- Reference standard or procedure followed
- Inspector name, certification level, and certificate number
- Test results with clear accept/reject determination
- Date and signature
The acceptance criteria for NDT must be stated on the report and must match the criteria specified in your purchase order or drawing. We have seen suppliers use their own internal criteria that are less strict than the customer's requirement — always cross-check.
Process Capability Data (Cpk)
Cpk data 9 tells you whether the process is centered and capable of consistently producing parts within tolerance — not just whether individual parts pass. A Cpk value of 1.33 or higher is a common benchmark for critical dimensions. If a supplier can provide Cpk data, it signals mature process control, not just machine capability.
Non-Conformance Reports (NCR)
An NCR system tracks any deviation from specifications, documents the root cause analysis, and records corrective and preventive actions. Ask the supplier how they handle non-conformances. Do they contain affected parts? Do they investigate root cause? Do they track corrective actions to closure? A supplier without an NCR system will repeat mistakes.
Calibration Certificates
Every measurement device and NDT instrument used on your parts must have a current calibration certificate. These certificates must be traceable to recognized standards. We keep copies of all calibration certificates in our project files for full traceability of NDT results.
Design for Manufacturability (DFM) Reports
While not an NDT document, a DFM report from the supplier shows they understand your design intent. It can flag features that may be difficult to inspect or test — allowing you to adjust the design or specify additional NDT before production begins. Strong suppliers proactively provide DFM input.
Summary: Your Documentation Checklist
| Document | Purpose | When to Request |
|---|---|---|
| First Article Inspection (FAI) | Confirms process produces conforming parts | Before production run |
| NDT Test Reports | Documents testing method, results, and acceptance | With each shipment |
| Cpk/Cpk Data | Proves process capability for critical dimensions | During PPAP or production |
| Non-Conformance Reports (NCR) | Tracks deviations, root cause, and corrective actions | Ongoing / as needed |
| Calibration Certificates | Verifies equipment accuracy and traceability | Annually or per audit |
| DFM Report | Identifies design risks and optimization opportunities | At RFQ or pre-production |
You should also ensure that quality assurance clauses in your fabrication contract explicitly reference the NDT documentation requirements and acceptance criteria you expect from the supplier.
Conclusion
Evaluating supplier NDT capabilities protects your investment, prevents costly field failures, and ensures your custom sheet metal parts are right the first time — every time. Verify equipment, certifications, process control data, and documentation before you commit. For a broader perspective on what to look for, explore how to evaluate sheet metal fabrication supplier capabilities and qualifications as part of your overall sourcing strategy.
Frequently Asked Questions
How do I assess if a sheet metal supplier has the right NDT equipment for my custom parts?
A lesson we learned early in our supplier audit process was that equipment lists alone mean nothing. During a facility visit in Vietnam, we found a supplier advertising radiographic testing capability — but the X-ray unit had not been calibrated in over two years.
Which non-destructive testing methods are most critical for my high-precision sheet metal projects?
One trade-off we weigh on nearly every project is whether to specify a single NDT method or require multiple methods for different features on the same part. The answer depends on the part geometry, material, and where failure would be most costly.
How can I verify that my supplier's NDT staff are qualified to meet my strict quality requirements?
A buyer interaction last year highlighted this issue sharply. A U.S. client received a batch of brackets with passing NDT reports — but the reports were signed by an operator with no formal certification. When we investigated, the "inspector" had learned on the job with no structured training. The parts were re-inspected by a certified technician, and two out of fifteen had rejectable indications.
Footnotes
1. Explains the purpose and importance of non-destructive testing methods. ↩︎
2. Provides an overview of ultrasonic testing principles and applications. ↩︎
3. Explains the principles and applications of magnetic particle inspection. ↩︎
4. Official standard for competence of testing and calibration laboratories. ↩︎
5. Comprehensive guide to liquid penetrant inspection for surface-breaking defects. ↩︎
6. Describes the method of using X-rays or gamma rays for internal inspection. ↩︎
7. Official guidelines for NDT personnel qualification and certification programs. ↩︎
8. Details the process and importance of First Article Inspection in manufacturing. ↩︎
9. Explains the Process Capability Index (Cpk) for assessing process performance. ↩︎