
Quality standard differences with Vietnamese stamping parts suppliers nearly cost one of our U.S. clients an entire product launch. The stamped brackets looked fine. The tolerances did not.
To handle quality standard differences with Vietnamese stamping parts suppliers, convert your expectations into written, measurable specifications, audit the supplier’s real process capability, require First Article Inspection and PPAP before mass production, and lock inspection, traceability, and corrective-action rules into the contract.
That is the short version. The rest of this article breaks it down into practical steps you can apply on your next stamping project.
How can I ensure my drawing specifications are correctly understood by Vietnamese stamping suppliers?
A few years back, our Vietnam office reviewed a drawing package for a stepped zigzag mounting clip. The U.S. drawing said "deburr all edges." The supplier read that as optional cosmetic advice.
Ensure correct understanding by providing bilingual drawings with explicit GD&T tolerances, separating critical dimensions from general tolerances, defining burr limits and surface requirements in measurable numbers, and confirming comprehension through a technical review meeting and a signed-off First Article Inspection.

Most quality failures we see are not skill failures. They are interpretation failures. A drawing that seems obvious to a U.S. engineer can carry hidden assumptions. Vietnamese stamping suppliers work hard and follow instructions well. But they follow what is written, not what you meant.
Make Every Requirement Measurable
"High quality" is not a specification. Neither is "clean edges." We rewrite vague notes into numbers before any RFQ leaves our desk. For example, burr height should be capped at a specific value, often no more than about 10% of material thickness. Surface finish should reference a standard, not an adjective.
Here is how we translate common vague notes into supplier-ready requirements:
| Vague Drawing Note | Supplier-Ready Specification |
|---|---|
| "Deburr all edges" | Max burr height 0.05 mm or 10% of material thickness |
| "Good surface finish" | No scratches visible at 300 mm under normal lighting; Ra value if functional |
| "Standard tolerance" | ISO 2768-m for general dimensions; critical features toleranced individually |
| "Galvanized steel" | SGCC, 1.2 mm, zinc coating Z12, alternates listed with approval rule |
| "Flat part" | Flatness within 0.2 mm over full length |
Close the Communication Loop
Many Vietnamese stamping factories, especially in northern clusters like Bac Ninh and Hai Phong, were trained under Japanese or Korean OEM systems. So referencing JIS standards 1 alongside your ASME callouts often speeds up understanding. Our Vietnam-based team runs a drawing review meeting before tooling starts. We ask the supplier to explain the drawing back to us. If they cannot, we found the gap before it cost anyone money.
What quality control processes should I require to avoid non-conforming stamped parts?
One buyer once told me he assumed his supplier inspected every dimension on every lot. The supplier was checking three dimensions out of nineteen. Both sides were surprised.
Require incoming material verification with mill certificates, First Article Inspection before production, in-process SPC on critical dimensions with a Cpk target of at least 1.33, documented die maintenance, final AQL-based sampling inspection, and third-party pre-shipment inspection for added assurance.

Quality control in stamping is a chain. If one link is missing, non-conforming parts slip through. When our team audits a stamping supplier in Vietnam, we map their controls against the full production flow. Gaps almost always appear in the same places: material receiving, die maintenance, and in-process measurement.
The QC Chain You Should Demand
Here is the control framework we apply on custom stamping projects for our U.S. clients:
| Stage | Required Control | Evidence to Request |
|---|---|---|
| Material receiving | Verify grade, thickness, coating against PO | Mill certificates, coil-level traceability records |
| Tooling launch | First Article Inspection on all dimensions | FAI report, PPAP documentation |
| Production | SPC on critical dimensions | Control charts, Cpk data (target ≥ 1.33) |
| Die management | Preventive maintenance schedule | Maintenance logs, punch sharpening records every 50,000–100,000 strokes |
| Final inspection | AQL sampling with defect classes | Dimensional reports, defect classification (critical/major/minor) |
| Pre-shipment | Independent verification | Third-party inspection report |
Define AQL and Defect Severity in Writing
Do not assume a shared definition of "defect." A light scratch on a hidden bracket flange may be acceptable to you but rejected by an over-cautious inspector, or the reverse. We write AQL tables 2 into the quality agreement. Critical defects get zero tolerance. Major and minor defects get explicit AQL levels. This removes debate at the final inspection table.
Die wear 3 deserves special attention. Burr height creeps up as punches dull. A part that passed FAI can drift out of spec after 80,000 strokes. That is why maintenance records matter as much as inspection records.
How do I resolve tolerance and material standard gaps between U.S. requirements and Vietnamese manufacturing practices?
There is a trade-off we weigh on almost every project: hold the exact U.S. material callout and accept longer import lead times, or approve a locally available equivalent grade. Both paths work. Only one is planned by accident.
Resolve the gaps by cross-referencing U.S. material grades to available JIS or local equivalents with documented approval, tolerancing critical features individually rather than relying on blanket standards, verifying the supplier's press and measurement capability, and confirming everything through capability studies before production.

U.S. drawings usually call out ASTM or SAE materials 4. Vietnamese mills and service centers stock JIS grades, often imported from Japan, Korea, or Taiwan. The gap is manageable if you address it before quoting, and painful if you discover it after tooling.
Build a Material Cross-Reference Early
Our engineers prepare an equivalence table for every stamping RFQ. The buyer approves it in writing before the tool is cut. A simplified example:
| U.S. Callout | Common Vietnamese/JIS Equivalent | Notes |
|---|---|---|
| ASTM A1008 CS | SPCC (JIS G3141) | Standard cold-rolled sheet, widely stocked |
| ASTM A653 galvanized | SGCC (JIS G3302) | Confirm zinc coating weight matches |
| SAE 1050 spring steel | S50C / SK5 | Verify hardness after forming and tempering |
| 304 stainless | SUS304 | Near-direct equivalent; confirm finish designation |
If no local equivalent is acceptable, we import the exact grade. That adds lead time, sometimes several weeks, so the decision must be made at the quote stage, not at production launch.
Handle Tolerance Gaps with Data, Not Assumptions
A supplier may be able to make your part once but not hold ±0.05 mm across 100,000 pieces. Spring-back 5 on bent flanges is a common drift point on brackets and clips like the ones we manage. We ask for a short capability study 6 on critical dimensions during the pilot run. If Cpk falls below 1.33, we adjust the tool, the process, or occasionally the tolerance itself after an honest engineering conversation with the client. Blanket tight tolerances raise cost and reject rates without adding function. Tolerance only what matters, and tolerance it tightly.
What steps can I take to prevent rework and delivery delays caused by quality standard mismatches?
A lesson we learned early in our Vietnam operations: rework is never just a quality cost. It is a schedule cost. One rejected lot of stamped brackets can push a delivery by three to four weeks once you count containment, re-stamping, re-plating, and re-booking freight.
Prevent rework and delays by using a staged approval workflow from RFQ to ramp-up, requiring FAI and PPAP sign-off before volume production, monitoring production with SPC and in-country oversight, and writing rework responsibility, change control, and delivery commitments into the contract.

Delays caused by quality mismatches are almost always born upstream. By the time a non-conforming lot reaches final inspection, the schedule damage is done. So prevention has to happen before and during production, not at the factory gate.
Follow a Staged Approval Workflow
We run every custom stamping project through the same gate sequence:
- RFQ with a complete technical package, including tolerances, material approvals, burr limits, and packaging requirements.
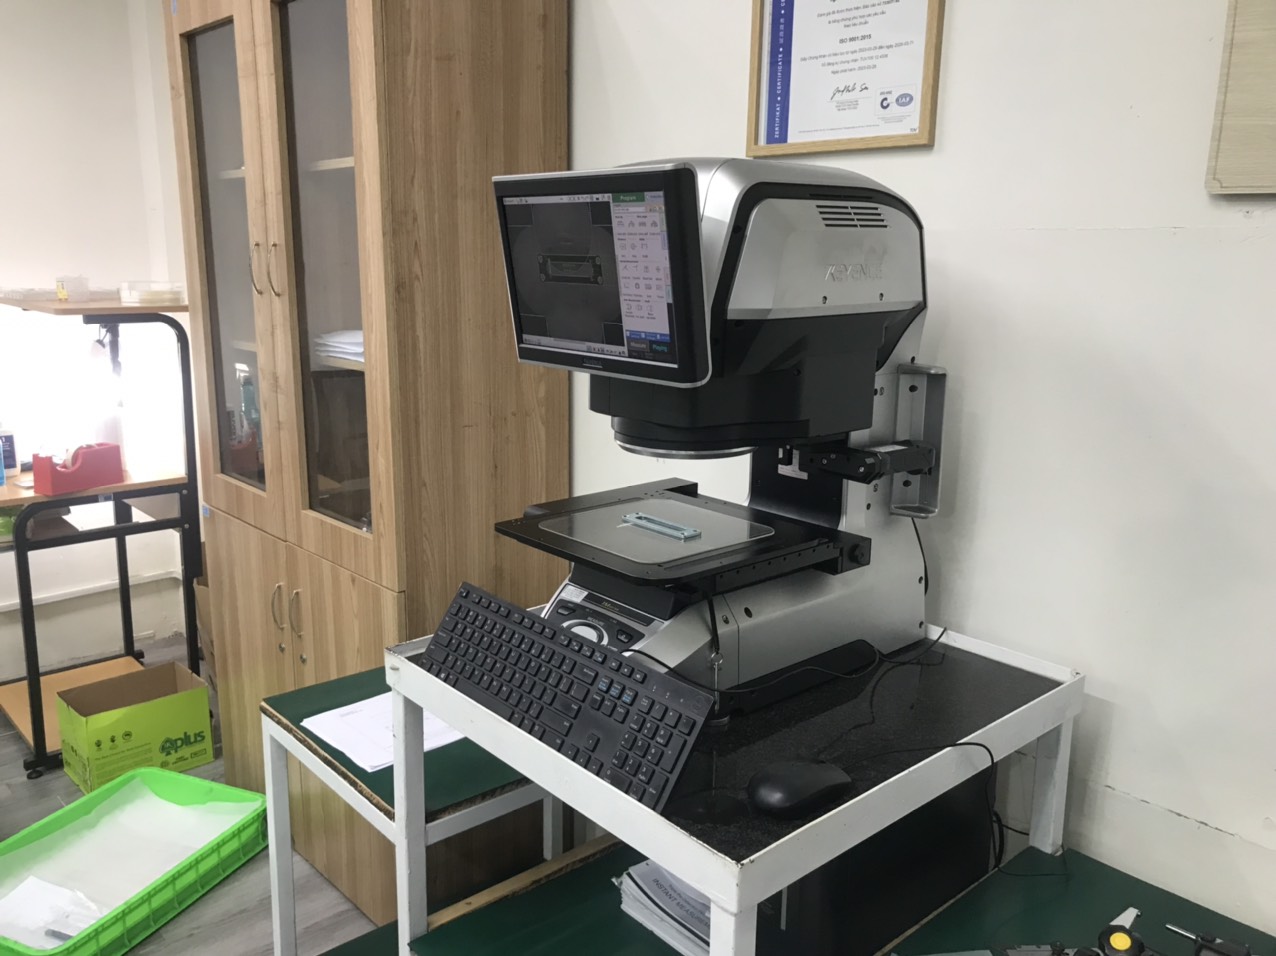
- Supplier capability review and on-site audit, checking press tonnage, toolroom capability, and measurement equipment.
- Tooling build, typically four to eight weeks, with progress checkpoints.
- Pilot run and First Article Inspection with full dimensional reports.
- Written FAI/PPAP approval before any volume authorization.
- Controlled ramp-up with SPC on key dimensions.
- Ongoing monitoring with a corrective-action loop for any deviation.
No gate gets skipped, even under schedule pressure. Skipping a gate to save a week usually costs a month.
Keep Eyes on the Ground
Between inspections, things can change quietly. Dies wear. Cost pressure can tempt a factory to substitute a cheaper steel grade without telling anyone. Our local team in Vietnam visits suppliers between shipments to check maintenance logs, verify material certificates 7 against actual coils, and catch drift early. If you do not have in-country staff, a rotating quality engineer or a sourcing partner with a local office fills that role.
Put the Rules in the Contract
The contract should state who owns the die, who maintains it, expected die life, rework and replacement responsibility, delay remedies, mandatory reporting of out-of-spec parts, and change-control notification. Ambiguity is where delays hide. Clear terms turn a dispute into a procedure.
Conclusion
Quality standard differences with Vietnamese stamping parts suppliers are solved upstream. Write measurable specs, audit real capability, gate production with FAI and SPC, and contract the rules clearly.
Frequently Asked Questions
How can I ensure my drawing specifications are correctly understood by Vietnamese stamping suppliers?
A few years back, our Vietnam office reviewed a drawing package for a stepped zigzag mounting clip. The U.S. drawing said "deburr all edges." The supplier read that as optional cosmetic advice.
What quality control processes should I require to avoid non-conforming stamped parts?
One buyer once told me he assumed his supplier inspected every dimension on every lot. The supplier was checking three dimensions out of nineteen. Both sides were surprised.
How do I resolve tolerance and material standard gaps between U.S. requirements and Vietnamese manufacturing practices?
There is a trade-off we weigh on almost every project: hold the exact U.S. material callout and accept longer import lead times, or approve a locally available equivalent grade. Both paths work. Only one is planned by accident.
Footnotes
1. Official Japanese Industrial Standards body explains the JIS framework suppliers often follow. ↩︎
2. ASQ explains acceptance quality limit sampling used to define defect classifications in contracts. ↩︎
3. Background explanation of tool and die wear mechanisms affecting stamped part tolerances. ↩︎
4. ASTM International defines the material grades U.S. drawings commonly reference for stamping. ↩︎
5. Wikipedia explains the springback phenomenon causing tolerance drift on bent metal flanges. ↩︎
6. Explains process capability studies and Cpk metrics used to validate stamping tolerance stability. ↩︎
7. ISO governs standards for material certification and traceability documentation referenced here. ↩︎