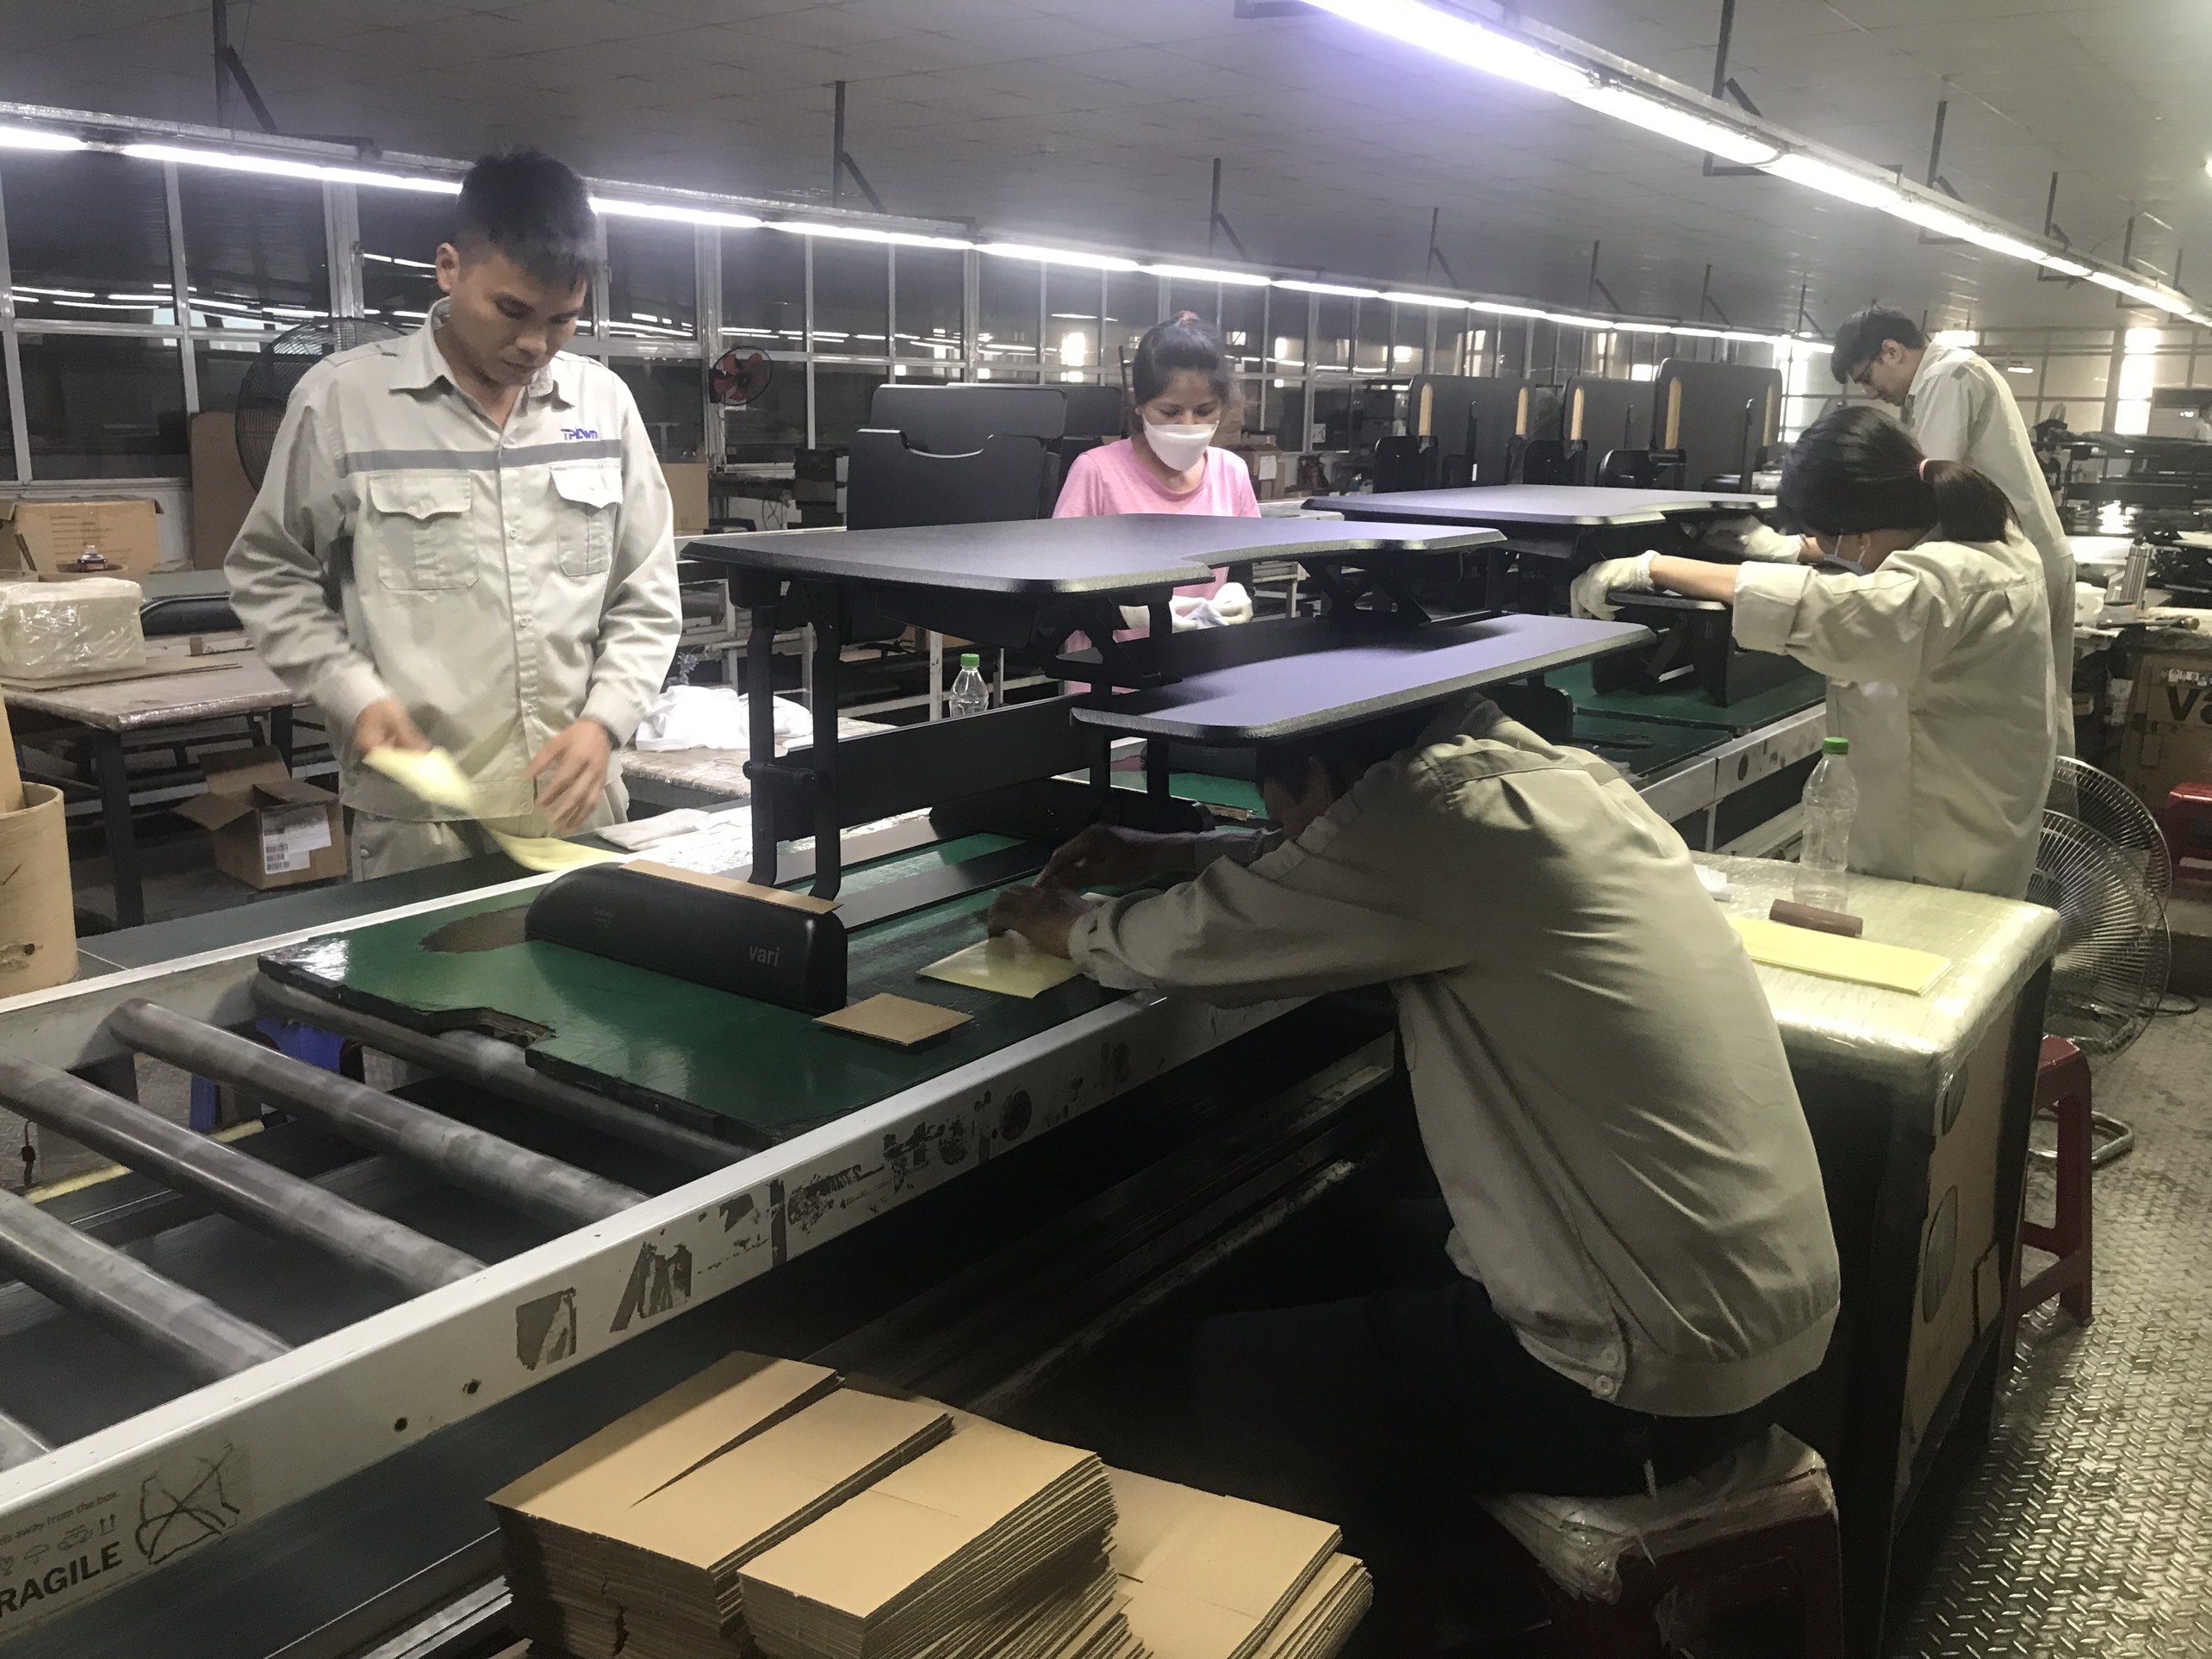

Getting environmental [reliability test data from stamping parts suppliers](https://dewintech.com/blog/how-request-reliability-test-data-stamping-parts-suppliers/) sounds simple until a shipment fails in the field PPAP stage 1. Our team learned this the hard way while auditing a plating vendor in Vietnam.
To request environmental reliability test data from stamping parts suppliers, specify the exact standard (such as ASTM B117 or IEC 60068), the part revision, finish, sample size, acceptance criteria, report format, and lab accreditation. Send this as a written checklist at the RFQ or PPAP stage.
That is the short answer. But the details matter. Below, I break down what to ask for, how to verify it, and how to compare suppliers across regions.
What Environmental Reliability Test Data Should I Request Before Approving a Stamping Parts Supplier?
A few years back, our Vietnam office qualified a stamping shop for zinc-plated brackets. The parts looked perfect. Then a client asked for salt spray data, and the supplier had none on file. That gap delayed approval by six weeks.
Before approving a stamping parts supplier, request salt spray test results (ASTM B117), humidity and thermal cycling reports, material composition certificates, plating thickness data, RoHS/REACH declarations, and lot traceability records. Each report should state the standard, sample size, test dates, and pass/fail criteria.

Environmental reliability for stamped parts is mostly a surface and finish story. The base steel rarely fails first. The plating, passivation, or coating does. So your data request must connect the finish chemistry to the test evidence.
The Core Document Package
In our sourcing projects for U.S. clients, we ask every stamping supplier for a package tied to a specific part revision. A report for a "similar part" is not enough. Here is the minimum set we require:
| Document | What It Proves | When It Is Critical |
|---|---|---|
| Salt spray report (ASTM B117 2) | Corrosion resistance of plating | Outdoor, marine, automotive use |
| Thermal cycling report | Coating adhesion under temperature swings | Engine bay, HVAC, electronics enclosures |
| Humidity test report | Resistance to condensation and white rust | Humid climates, sealed packaging |
| Material cert (mill cert) | Correct alloy grade and thickness | Every stamped part |
| Plating thickness report | Coating meets drawing spec | Every plated part |
| RoHS/REACH declaration | Regulatory compliance | EU and U.S. regulated markets |
| Lot traceability record | Report matches your shipment | High-risk or safety parts |
Match the Data to the Failure Mode
Do not request every test for every part. Think about how the part fails. A bare steel bracket inside a dry indoor cabinet needs less evidence than a zinc-plated clip near a coastal HVAC unit. When we scope a project, we first define the use environment with the client's engineer. Then we pick the two or three tests that address the real risk. That keeps supplier costs reasonable and keeps the data meaningful. Also ask whether the supplier tests in-house or uses an outside lab. In-house data is fine for process control. For qualification, third-party data carries more weight.
How Do I Verify That My Supplier's Test Reports Meet Industry Standards Like ASTM or IEC?
There is a trade-off I weigh on every project: verification takes time, but skipping it costs more. During one supplier audit in southern China, our QC engineer spotted a salt spray report with no chamber calibration record. The numbers were meaningless.
Verify supplier test reports by checking that the exact standard and revision is cited, the lab holds ISO/IEC 17025 accreditation, test parameters match the standard's requirements, equipment calibration certificates are current, and the report lists your part number, revision, finish, and lot identifiers.

A test report is only as good as the process behind it. Many buyers glance at the pass/fail line and file the document. That is a mistake. A credible report must be auditable from front to back.
A Five-Step Verification Routine
- Check the standard citation. The report must name the full standard and its year, for example ASTM B117-19 or IEC 60068 3-2-11. A vague phrase like "salt spray tested" is a red flag.
- Confirm lab accreditation. Look for an ISO/IEC 17025 accreditation 4 number. You can verify it on the accreditation body's website in minutes.
- Compare parameters to the standard. ASTM B117 requires a 5% NaCl solution at 35°C. If the report shows different values without explanation, question it.
- Trace the sample. The report should list your part number, drawing revision, plating batch, and test dates. Reports older than one to two years may not reflect current production.
- Request calibration records. Chambers and measurement instruments need current calibration certificates 5 traceable to national standards.
Common Standards Quick Reference
| Standard | Test Type | Key Parameters to Check |
|---|---|---|
| ASTM B117 | Neutral salt spray | 5% NaCl, 35°C, hours to white/red rust |
| IEC 60068-2-11 | Salt mist | Duration, chamber conditions |
| IEC 60068-2-14 | Thermal cycling | Temperature range, dwell time, cycle count |
| ISO 16750 | Automotive environments | Test severity level matched to vehicle zone |
| IEC 60068-2-78 | Damp heat, steady state | Temperature, humidity %, duration |
When our team reviews reports for clients, we also ask one simple question: does the tested finish match the current drawing? Suppliers sometimes change plating vendors without retesting. A report on the old finish proves nothing about the new one.
What Questions Should I Ask If a Supplier Can't Provide Complete Reliability Test Documentation?
A purchasing manager we work with once told me his rule: a missing document is information, not a dead end. I agree. Some capable stamping shops in Vietnam simply never had customers who asked. The right questions reveal whether the gap is fixable.
Ask why the data is missing, whether the supplier can test now through an accredited lab, what process controls substitute in the meantime, whether similar-part data exists with documented differences, and who bears the testing cost. Their answers reveal capability, transparency, and quality culture.

Missing documentation is common in Asia's stamping sector, especially with smaller shops. It does not always mean poor quality. But how a supplier responds tells you almost everything about their quality culture 6.
The Questions That Matter
Start with the reason. Ask: "Has this part or finish ever been tested, by anyone?" Sometimes the plating subcontractor holds the data and the stamping shop never requested it. That is an easy fix. Then probe deeper:
- "Can you arrange third-party testing now, and how fast?" A confident supplier says yes and quotes a lead time. A defensive supplier makes excuses.
- "What in-process controls do you use for the finish?" Look for plating thickness checks, bath chemistry logs, and incoming material inspection.
- "Do you have data on a similar construction?" Similar-part data is acceptable for low-risk parts, but only if the supplier documents exactly what differs.
- "Will you retain test records, and for how long?" A retention commitment shows discipline.
- "Who pays for qualification testing?" In our experience, sharing the cost on first orders is fair and builds commitment on both sides.
Reading the Response
When we run supplier audits for U.S. clients, we score the answers, not just the documents. A supplier that says "we will get the plating batch records from our subcontractor by Friday" is worth developing. A supplier that says "our parts never have problems" without evidence is a risk. We have walked away from lower-priced quotes for exactly that reason. Use a risk-based approach: accept declarations for low-risk indoor parts, but require fresh accredited-lab reports for new finishes, safety-related parts, or regulated end markets. Never accept "trust us" as the final answer on a critical application.
How Can I Use Environmental Test Data to Compare Stamping Suppliers Across Vietnam, China, and Taiwan?
Splitting our operations between Vietnam and China taught our team something useful: test data is the great equalizer. Marketing claims differ by region. Salt spray hours do not.
Normalize each supplier's data to the same standard, test duration, and acceptance criteria, then compare corrosion hours, cycle counts, lab accreditation, and traceability depth side by side. Score documentation completeness and turnaround speed alongside results to reveal true capability differences across Vietnam, China, and Taiwan.

Regional generalizations are dangerous. We have seen excellent labs in Vietnam and weak ones in Taiwan, and the reverse. Still, patterns exist, and structured data comparison exposes them quickly.
A Regional Comparison Framework
Here is the general pattern our sourcing team observes, which you should verify supplier by supplier:
| Factor | Vietnam | China | Taiwan |
|---|---|---|---|
| In-house test equipment | Growing, often basic | Common, wide range | Common, mature |
| Access to accredited labs | Good in major hubs | Extensive | Extensive |
| Documentation habits | Improving, needs coaching | Varies widely by tier | Generally strong |
| Typical response to data requests | Willing, may need templates | Fast if specified clearly | Structured, standards-fluent |
| Tariff position for U.S. buyers | Favorable | Exposed | Moderate |
Normalize Before You Compare
Raw numbers mislead when test conditions differ. One supplier may report 96 hours of salt spray to white rust; another reports 72 hours but used a thicker plating spec and stricter criteria. To compare fairly:
- Send all candidates the same test requirement: same standard, same duration, same acceptance criteria, same sample size.
- Require the same report format so nothing hides in translation.
- Compare not just results, but response quality. How fast did each supplier reply? Did they ask smart clarifying questions? Did they flag risks in your spec?
When we run parallel qualifications for clients diversifying out of China, the supplier who asks "which zinc passivation 7 color does your customer require?" usually outperforms the one who just quotes a price. Test data comparison works best when you treat the request itself as part of the audit. The evidence tells you about corrosion resistance. The process of getting the evidence tells you about the supplier.
Conclusion
Vague requests get vague documents, and vague documents hide field failures. Specify the standard, verify the lab, question the gaps, and normalize your comparisons. Do that, and environmental reliability test data becomes your strongest sourcing tool.
Frequently Asked Questions
What Environmental Reliability Test Data Should I Request Before Approving a Stamping Parts Supplier?
A few years back, our Vietnam office qualified a stamping shop for zinc-plated brackets. The parts looked perfect. Then a client asked for salt spray data, and the supplier had none on file. That gap delayed approval by six weeks.
How Do I Verify That My Supplier's Test Reports Meet Industry Standards Like ASTM or IEC?
There is a trade-off I weigh on every project: verification takes time, but skipping it costs more. During one supplier audit in southern China, our QC engineer spotted a salt spray report with no chamber calibration record. The numbers were meaningless.
What Questions Should I Ask If a Supplier Can't Provide Complete Reliability Test Documentation?
A purchasing manager we work with once told me his rule: a missing document is information, not a dead end. I agree. Some capable stamping shops in Vietnam simply never had customers who asked. The right questions reveal whether the gap is fixable.
Footnotes
1. Explains the production part approval process referenced for supplier documentation timing. ↩︎
2. Defines the salt spray standard referenced throughout for corrosion testing verification. ↩︎
3. Background on the environmental testing standard family cited for thermal cycling and humidity. ↩︎
4. Official ISO source explaining lab accreditation requirements mentioned as verification criteria. ↩︎
5. NIST resource on measurement calibration traceability required for credible test equipment. ↩︎
6. ISO’s quality management principles explain how supplier quality culture drives consistent, auditable performance. ↩︎
7. Wikipedia background on the passivation chemistry central to plating corrosion resistance. ↩︎