7 Common Injection Molding Defects and How to Prevent Them
February 13, 2026 · 9 min read

Injection molding is one of the most efficient ways to produce plastic parts at scale. But even experienced molders encounter defects that compromise part quality, drive up scrap rates, and delay production. Understanding the root causes of common defects — and how to prevent them through design and process control — is essential knowledge for any engineer or buyer working with molded parts.
This guide covers the seven defects we see most frequently at our Vietnam facilities, along with practical solutions drawn from thousands of production runs.
Most injection molding defects trace back to a few root causes — non-uniform wall thickness, poor gate placement, inadequate venting, and incorrect melt or pressure settings. Fixing them early through design and process control is far cheaper than scrapping parts or reworking tooling.
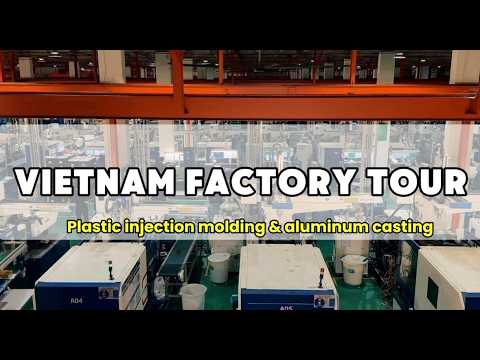
Inside a Vietnam Factory — Plastic Processing & Die Casting
Watch on YouTube
Real footage from an audited DEWIN partner factory in Vietnam.
1. Sink Marks
Sink marks are small depressions or dimples on the surface of a molded part, typically found opposite thick sections like ribs, bosses, or wall intersections. They occur when the outer skin of the part solidifies before the interior, and the shrinking core pulls the surface inward.
Sink marks are surface depressions that appear opposite thick features like ribs and bosses. They form when the outer skin cools and solidifies before the thicker core, which then shrinks and pulls the surface inward — the fix is uniform walls and adequate packing pressure.
Prevention:
- Keep wall thickness uniform — rib thickness should be 50–60% of the adjacent wall
- Increase packing pressure and packing time to compensate for shrinkage
- Relocate the gate closer to thick sections so packing pressure reaches them effectively
- Consider gas-assist or foam molding for parts with unavoidably thick sections
2. Warping
Warping is the distortion of a part after ejection, where flat surfaces bow or twist. It results from non-uniform shrinkage caused by inconsistent cooling, varying wall thicknesses, or residual stresses from the filling pattern.
Prevention:
- Design uniform wall thicknesses throughout the part
- Ensure balanced cooling channels on both sides of the mold
- Use symmetrical gate placement for even flow distribution
- Allow adequate cooling time before ejection
- Select materials with lower shrinkage rates (e.g., ABS over PP) when warpage is critical
3. Flash
Flash is thin excess material that seeps out along the parting line or around ejector pins and inserts. It happens when the mold halves don't seal completely — due to insufficient clamp force, worn tooling, or excessive injection pressure.
Prevention:
- Verify clamp tonnage is adequate for the projected area and injection pressure
- Inspect and maintain parting line surfaces regularly
- Reduce injection speed and pressure if flash persists
- Ensure mold components are properly aligned with no wear-induced gaps
4. Jetting
Jetting appears as snake-like, wavy lines on the part surface — usually starting near the gate. It occurs when molten plastic shoots through the gate into the cavity like a jet stream rather than flowing smoothly as a melt front. The initial stream cools on contact with the mold wall and doesn't fuse properly with subsequent material.
Prevention:
- Redesign the gate so the melt front contacts an opposing wall immediately (fan gate or tab gate)
- Reduce injection speed during the initial fill phase
- Increase melt temperature to improve flow characteristics
- Use a larger gate cross-section to slow the entry velocity
5. Short Shots
A short shot is a part that isn't completely filled — you get a partial part with missing sections. Causes include insufficient material volume, inadequate injection pressure, blocked gates or runners, trapped air, or flow paths that are too long and thin.
Prevention:
- Verify shot size and cushion settings
- Increase injection pressure and speed
- Raise melt and mold temperatures to improve flow length
- Add vents at the end of fill to release trapped air
- Redesign thin sections that create flow restrictions
6. Weld Lines
Weld lines (also called knit lines) form where two flow fronts meet and solidify together. They appear as faint lines on the surface and represent weak points — tensile strength at a weld line can be 10–25% lower than the base material. They are most common in parts with multiple gates, holes, or complex geometries that split the flow.
Weld lines form where two flow fronts meet and re-solidify, creating a visible line and a weak spot — tensile strength there can run 10–25% below the base material. Hotter melt, faster fill, and smarter gate placement move them off critical, load-bearing areas.
Prevention:
- Increase melt temperature so flow fronts are hotter when they converge
- Raise injection speed to reduce cooling before fronts meet
- Relocate gates to move weld lines to non-critical areas
- Add overflow wells to push the weld line off the visible surface
- Use mold flow simulation to predict and relocate weld lines during design
7. Burn Marks
Burn marks are dark brown or black discolorations at the end of fill or in areas where air is trapped and compressed. As the mold fills, air is pushed ahead of the melt front. If it can't escape through vents, it compresses, heats to the point of igniting the plastic (diesel effect), and leaves charred marks.
Prevention:
- Add or deepen vents at the last-to-fill locations
- Reduce injection speed so air has time to escape
- Redesign part geometry to eliminate air traps
- Clean existing vents — even a thin film of residue can block airflow
How Dewin Vietnam Handles Defect Prevention
At our facilities in Vietnam, defect prevention starts before the mold is built. Our engineering team runs mold flow analysis on every new project to predict potential sink marks, weld line locations, warping tendencies, and air traps. This simulation-driven approach lets us optimize gate locations, cooling layouts, and wall thicknesses before cutting steel — saving weeks of trial-and-error on the shop floor.
During production, our quality team monitors key process parameters in real time: injection pressure curves, melt temperature, cycle time, and cushion position. Statistical process control (SPC) charts flag deviations before they become defects. Combined with first-article inspection and regular tool maintenance schedules, this system keeps our defect rates consistently below 0.5% across high-volume production runs.
Need help with an injection molding project?
Talk to our engineering team about mold design, material selection, and defect-free production in Vietnam.
Frequently Asked Questions
Which injection molding defects weaken a part instead of just marking it?
Weld lines are the defect that measurably weakens a molded part — tensile strength where two flow fronts meet can be 10–25% lower than the base material. Sink marks, jetting, and burn marks appear as surface depressions, snake-like lines, and dark discolorations, while a short shot leaves the part incompletely filled. Relocating gates moves weld lines off load paths.
Can mold flow analysis prevent defects before the tool is cut?
Mold flow analysis run during design predicts sink marks, weld line locations, warping tendencies, and air traps before steel is cut. The simulation lets engineers optimize gate locations, cooling layouts, and wall thicknesses up front, saving weeks of trial-and-error on the shop floor. Fixing defects at this stage is far cheaper than scrapping parts or reworking tooling.
What defect rate is realistic for high-volume injection molding?
Defect rates below 0.5% are achievable across high-volume injection molding runs when process monitoring is in place. Reaching that level takes real-time tracking of injection pressure curves, melt temperature, cycle time, and cushion position, with statistical process control charts flagging deviations before they become defects. First-article inspection and regular tool maintenance schedules hold it there.