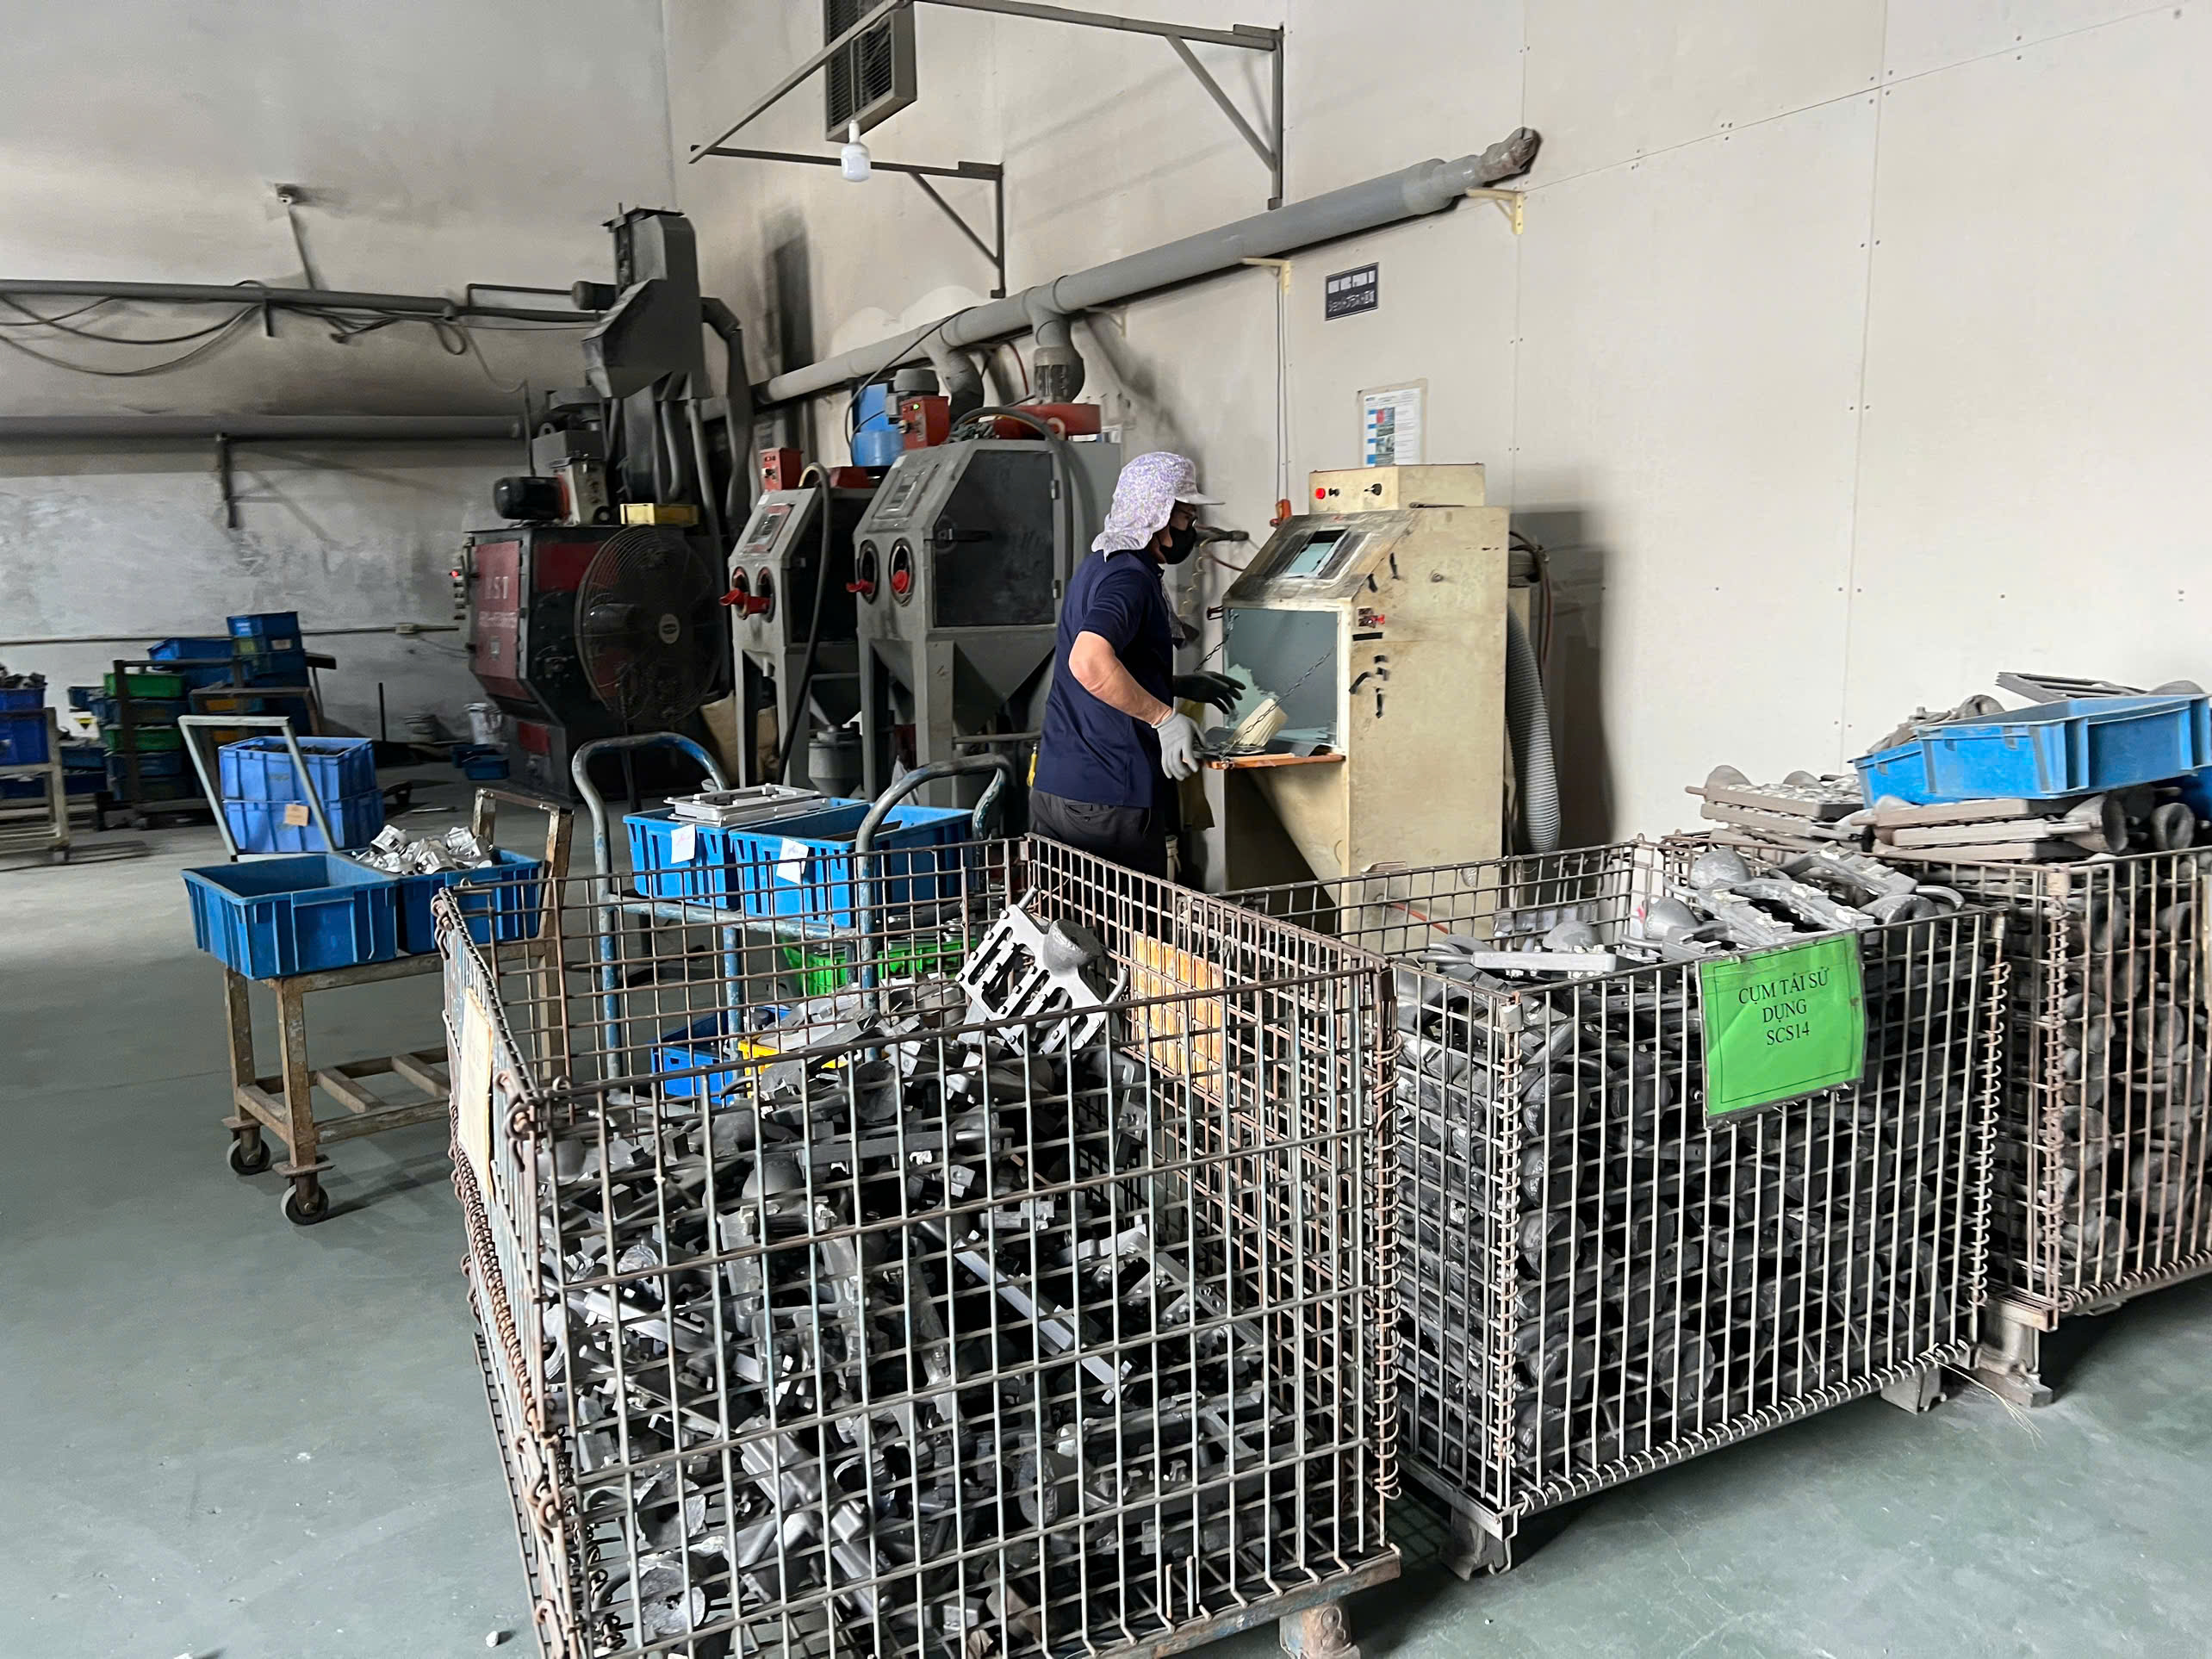
What DFM simulation and engineering review steps prepare multi-cavity injection molds for transfer between China and Vietnam?
Pre-quote engineering review relies on 2D and 3D tolerance analysis, mold flow simulation, and tool design evaluation before steel cutting. Managed through a 26-person engineering service center in Xi’an, these pre-production evaluations analyze high-temperature PEEK and PFA hot-runner multi-slider setups alongside plastic injection mold specifications prior to relocating production assets across Asian hubs.
Key Takeaways
- Pre-quote engineering utilizes 2D and 3D tolerance analysis, mold flow simulation, and hot-runner design reviews executed prior to tool steel cutting.
- Relocation of dies, fixtures, and quality control gauges from China to Vietnam follows a structured 10-month migration playbook to ensure uninterrupted production.
- Quality verification incorporates PPAP Level 3 documentation, material certificates of analysis, and ZEISS 3D CMM metrology to maintain a 50 PPM defect benchmark.
- Local engineering presence in Ho Chi Minh City and Bac Ninh manages QCLDM audits, factory verification, and native technical oversight across 300 mapped facilities.
Before physical molds, dies, or fixtures are packed for transport, detailed Design for Manufacturability (DFM) reviews establish strict baseline parameters. Engineering teams analyze 2D drawings and 3D CAD files to evaluate gate location, runner balance, wall thickness, and material shrinkage rates. Mold flow simulations identify potential air traps, weld lines, and cooling imbalances across multi-cavity configurations.
- Pre-quote 2D and 3D tolerance stack-up analysis
- Mold flow simulation and cooling channel optimization before cutting steel
- Hot-runner and multi-slider design evaluations for high-temperature PEEK, PFA, and fluoropolymer components
- Tooling review coordinated by a 26-person engineering center in Xi'an, China

How does the 10-month migration playbook relocate tooling and fixtures from China to Vietnam?
The 10-month migration playbook coordinates the transfer of dies, fixtures, and quality control gauges from Chinese manufacturing centers to local facilities in Ho Chi Minh City, Binh Duong, Dong Nai, Bac Ninh, and Haiphong. Local engineering teams manage on-site alignment, tool commissioning, and factory audits to prevent supply chain interruptions during international relocations.
Relocating high-precision tooling requires structured milestone management to maintain continuous part supply. The 10-month migration playbook outlines specific stages for tool disassembly, preventative maintenance, packing, international freighting, and re-commissioning on press lines in Vietnam.
- Transfer of multi-cavity molds, progressive dies, checking fixtures, and dedicated QC gauges
- On-site oversight by 7 local staff in Ho Chi Minh City covering manufacturing hubs in Bac Ninh, Haiphong, Binh Duong, and Dong Nai
- Factory selection from a network of 300+ mapped and 150+ audited Vietnam manufacturing facilities
- Validation of machine clamping force, hydraulic interfaces, and auxiliary hot-runner controllers at destination plants
Which quality inspection protocols and metrology standards validate relocated injection molding components?
Relocated tooling validation uses Production Part Approval Process Level 3 documentation, material certificates of analysis, and resident supplier quality engineering audits. Dimensional verification is performed using in-process ZEISS CMM inspection and Mitutoyo 3D coordinate measuring machines to maintain defect benchmark targets of 50 parts per million or lower across production runs.
Once transferred molds are mounted on destination presses, rigorous First Article Inspection (FAI) and sampling protocols begin. Native engineers verify material inputs against Certificates of Analysis (COA) and execute full dimensional metrology using laboratory-grade coordinate measuring equipment.
- Full PPAP Level 3 documentation package preparation
- In-process ZEISS CMM and Mitutoyo Crysta-Apex S 3D coordinate measuring machine metrology
- Resident Supplier Quality Engineer (SQE) audits on shop floors
- Quality control benchmarking to achieve and sustain ≤50 PPM defect thresholds
- Traceable material verification using COA documentation for high-purity polymers and metal components
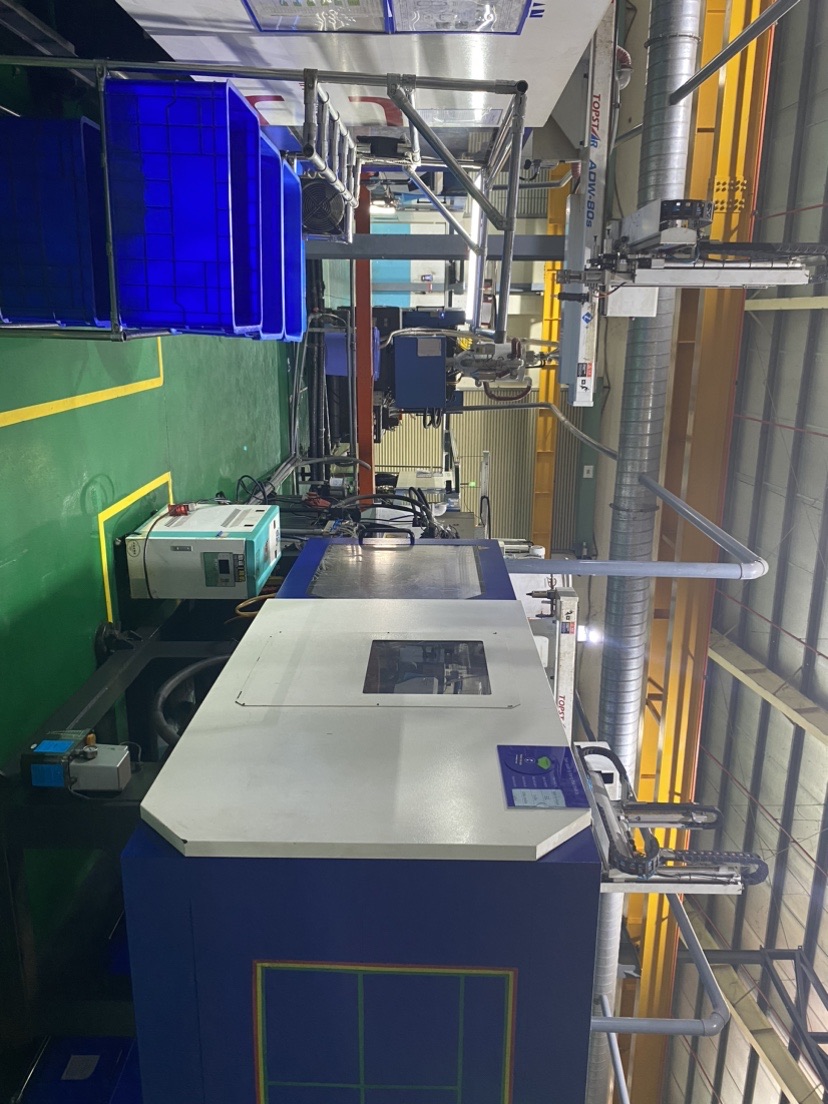
Polymer & Tooling Engineering Comparison Matrix
| Engineering Criterion | Bridge / Soft Tooling (P20 / 718H) | High-Volume Production Tooling (H13 / S136) | Quality Control Gate |
|---|---|---|---|
| Mold Steel & Cavity Life | 50,000 – 100,000 shots (Pre-hardened steel) | 500,000 – 1,000,000+ shots (Vacuum heat-treated) | Steel Hardness (HRC) & Cavity CMM Report |
| Dimensional Tolerance | DIN 16742 TG5 / Commercial standard | DIN 16742 TG3–TG4 / Fine engineering grade | T0/T1/T2 30-Piece Capability Study |
| Wall Thickness & Draft Angle | 1.5 mm – 4.0 mm wall; 1.0°–1.5° minimum draft | Uniform ±10% nominal wall; textured draft ≥ 2.5° | Moldflow Simulation & Cross-Section Check |
| Resin & Regulatory Compliance | Virgin resin lot certificate + COA | UL94, RoHS, REACH, FDA / ISO 10993 traceability | DSC Melt-Flow & Moisture Analyzer Check |
Frequently Asked Questions
What tooling and molding capabilities are documented for high-temperature polymer processing?
Documented facilities provide high-temperature PEEK and PFA injection molding utilizing hot-runner multi-slider tooling, PTFE compression sintering, and multi-axis CNC machining centers for high-purity applications.
How are on-site quality audits managed across Vietnam manufacturing hubs?
Native engineering teams based in Ho Chi Minh City conduct QCLDM factory audits, DFM drawing reviews, and in-process ZEISS CMM inspections across facilities in Bac Ninh, Haiphong, Binh Duong, and Dong Nai.
What metrology equipment is utilized to inspect precision molded and machined components?
Inspection laboratories use ZEISS CMM 3D coordinate measuring machines, Mitutoyo Crysta-Apex S metrology systems, contour testers, and surface roughness analyzers to perform dimensional verification.
What commercial terms and contracting structures support multi-country tool relocations?
Operations are managed under a single contract through Singapore HQ, offering up to Net 90 Days Open Account payment terms to support multi-facility relocations across China, Vietnam, and Southeast Asia.