Plastic Blow Molding Sourcing from Vietnam: A Technical Guide
February 14, 2026 · 12 min read
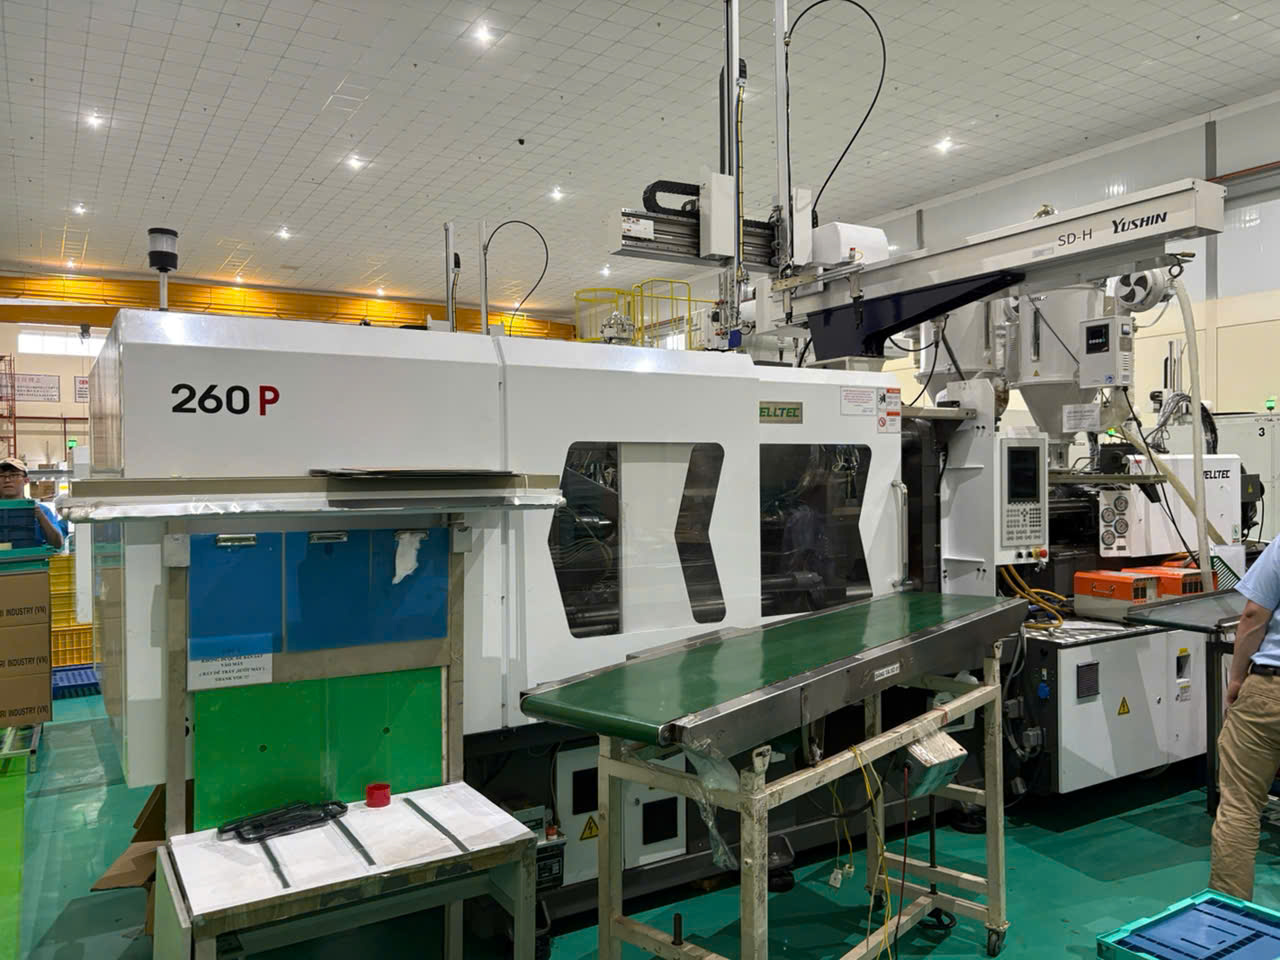
Blow molding produces hollow plastic parts — fuel tanks, fluid reservoirs, HVAC ducts, bottles, and industrial containers — by inflating a heated plastic parison inside a mold cavity. Vietnam's blow molding sector has matured rapidly, with factories now running Bekum, Kautex, and Graham machines capable of multi-layer co-extrusion. For US buyers navigating Section 301 tariffs on Chinese plastics (List 3: 25% on HTS 3923–3926), Vietnam offers an alternative exempt from Section 301 tariffs under the US-Vietnam Bilateral Trade Agreement and upcoming CPTPP benefits.
Blow molding forms hollow plastic parts — tanks, reservoirs, ducts, and bottles — by inflating a heated parison inside a mold. Sourcing from Vietnam adds a Section 301 tariff advantage: Vietnam-origin parts avoid the 25% duty applied to comparable Chinese plastics.
Inside a Vietnam Factory — Plastic Processing & Die Casting
Watch on YouTube
Real footage from an audited DEWIN partner factory in Vietnam.
Blow Molding Process Variants
Understanding the three main blow molding methods helps you specify correctly in RFQs and evaluate supplier capability:
The three main variants are extrusion blow molding (EBM) for HDPE tanks and ducts, injection blow molding (IBM) for tighter small containers, and injection stretch blow molding (ISBM) for clear PET bottles. Match the method to part size, tolerance, and clarity needs.
- Extrusion Blow Molding (EBM): A continuous parison is extruded, captured in a mold, and inflated at 4–8 bar. Best for HDPE containers, automotive ducts, and industrial tanks. Wall thickness tolerance: ±10–15%. Cycle times: 15–60 seconds depending on part size. Tooling cost: $8,000–$35,000 in Vietnam vs. $15,000–$60,000 in the US.
- Injection Blow Molding (IBM): A preform is injection molded, then transferred to a blow station. Tighter tolerances (±5% wall thickness) and superior neck-finish accuracy. Ideal for pharmaceutical bottles and small containers under 500ml. Tooling: $15,000–$50,000.
- Injection Stretch Blow Molding (ISBM): PET preforms are reheated and biaxially stretched, producing bottles with excellent clarity and barrier properties. Standard for beverage containers. Material savings of 10–20% vs. EBM due to molecular orientation improving strength.
Material Selection: What to Specify in Your RFQ
| Material | Grade Example | Key Properties | Typical Applications |
|---|---|---|---|
| HDPE | Marlex HHM 5502BN | Density 0.955 g/cm³, excellent chemical resistance, -40°C to 80°C service | Fuel tanks, chemical containers, ducting |
| PP | Braskem CP 360H | Higher stiffness than HDPE, 100°C continuous service, FDA-compliant grades | Automotive reservoirs, medical containers |
| PET | Eastman Eastar EN058 | Excellent clarity, oxygen barrier 8–12× better than HDPE, recyclable | Beverage bottles, food packaging |
| ABS+PC | SABIC Cycoloy C1200HF | Impact strength 500–650 J/m, flame retardant UL94 V-0, -30°C to 125°C | Electronic enclosures, EV battery housings |
| PA6 | BASF Ultramid B3K | Tensile strength 70 MPa, 180°C peak service, oil/fuel resistant | Under-hood air ducts, charge air cooler pipes |
RFQ tip: Always specify the resin grade (not just "HDPE"), melt flow index range, and any regulatory requirements (FDA 21 CFR 177, REACH, RoHS). Vietnamese suppliers can source SABIC, LyondellBasell, and SCG resins locally or import — confirm lead time for specialty grades (typically 4–6 weeks).
Critical Tolerances & Quality Parameters
Blow molding is inherently less precise than injection molding. Setting realistic expectations in your drawing prevents costly rejects:
- Wall thickness: ±10–15% for EBM, ±5–8% for IBM. Minimum practical wall: 0.5mm (PET ISBM) to 1.5mm (HDPE EBM). Specify min/max, not nominal only.
- Dimensional tolerance: ±0.5mm per 25mm for EBM; ±0.25mm for IBM on neck/thread dimensions.
- Weight consistency: ±2–3% shot-to-shot is standard; specify if tighter control needed.
- Drop test: ASTM D2463 — specify height (typically 1.2–1.8m) and temperature (23°C and -18°C for automotive).
- Burst pressure: For pressurized containers, specify per ASTM D2561. Typical: 2–3× working pressure.
- Environmental stress crack resistance (ESCR): ASTM D1693 — critical for HDPE containers exposed to chemicals. Request F50 > 1,000 hours.
Cost Structure: Vietnam vs. China vs. US
A typical 2L HDPE industrial container (200g, single-cavity EBM tool) cost comparison:
| Cost Element | Vietnam | China | US |
|---|---|---|---|
| Tooling (single cavity) | $10,000–$15,000 | $8,000–$12,000 | $25,000–$40,000 |
| Unit price (10K pcs) | $0.35–$0.50 | $0.30–$0.45 | $0.80–$1.20 |
| Unit + 25% tariff (China) | $0.35–$0.50 | $0.38–$0.56 | $0.80–$1.20 |
| Ocean freight per unit | $0.02–$0.04 | $0.02–$0.03 | N/A |
| Lead time (tool + T1) | 6–8 weeks | 4–6 weeks | 8–12 weeks |
Vietnam's landed cost advantage over China grows as tariff rates increase. With Section 301 tariffs at 25% on List 3 plastics, Vietnam delivers 15–25% total cost savings versus Chinese blow molded parts for US buyers, while offering comparable tooling lead times.
How to Evaluate a Vietnam Blow Molding Supplier
- Machine fleet: Ask for tonnage range, number of heads, and whether they run accumulator-head machines for parts >5L. Multi-layer co-extrusion capability indicates advanced operation.
- Parison control: Suppliers with MOOG or REX parison programming can achieve ±5% wall thickness on EBM — a significant quality differentiator.
- Leak testing: Every automotive blow molded part should be 100% leak-tested. Confirm they have in-line pressure decay testers (sensitivity ≤0.01 bar loss over 30 seconds).
- Certifications: IATF 16949 for automotive, ISO 13485 for medical, ISO 9001 minimum for all. Vietnam factories increasingly hold IATF — Katagiry, Nhựa Duy Tân, and An Phát are notable.
- Mold ownership: Always specify in your contract that tooling ownership transfers to the buyer upon full payment. Include IP protection clauses and right to transfer molds to another supplier.
Design-for-Manufacturing Tips
- Draft angle: Minimum 1° per side for EBM, 0.5° for IBM. More draft = easier demolding = fewer defects.
- Pinch-off design: The bottom weld line (pinch-off) is the weakest point. Design with a minimum 3mm land width and radius the inner corner to avoid stress concentration.
- Handle integration: Blow molded handles should have a minimum 15mm opening and 3mm wall to survive drop tests. Avoid sharp internal corners.
- Flash removal: Budget for secondary deflashing — typically adds $0.02–$0.05/part for automated trimming. Include trim line in your 3D model.
- Multi-layer design: For fuel system components requiring permeation barriers (CARB/EPA LEV III: ≤0.2 g/m²/day), specify 6-layer structure: HDPE/regrind/adhesive/EVOH/adhesive/HDPE.
Source Blow Molded Parts from Vietnam
DEWIN partners with certified blow molding factories across Vietnam — from single-layer HDPE containers to multi-layer automotive fuel systems. Get a quote →
Frequently Asked Questions
How do I make sure I own the blow mold tooling I paid for?
Tooling ownership has to be written into the contract: specify that ownership transfers to the buyer upon full payment, include IP protection clauses, and reserve the right to transfer molds to another supplier. Without those terms, moving production later is difficult. Single-cavity EBM tooling in Vietnam runs $10,000–15,000, so the sum at stake is real.
What should I ask about a blow molder's machines before quoting?
Three machine-fleet questions matter: tonnage range, number of heads, and whether the shop runs accumulator-head machines, which are needed for parts over 5 L. Multi-layer co-extrusion capability indicates an advanced operation. Suppliers with MOOG or REX parison programming can achieve ±5% wall thickness on EBM — a significant quality differentiator over the usual ±10–15%.
What wall structure do blow molded fuel system parts need?
Fuel system components requiring permeation barriers need a 6-layer structure: HDPE/regrind/adhesive/EVOH/adhesive/HDPE. That construction targets the CARB and EPA LEV III limit of 0.2 g/m²/day or less. Every automotive blow molded part should also be 100% leak-tested, so confirm the supplier has in-line pressure decay testers sensitive to 0.01 bar loss over 30 seconds.
Which test standards should I put on a blow molding drawing?
ASTM D2463 for drop testing, ASTM D2561 for burst pressure, and ASTM D1693 for environmental stress crack resistance cover most blow molded containers. On the drop test, specify height — typically 1.2–1.8 m — and temperature, 23°C plus -18°C for automotive. Burst pressure is typically 2–3× working pressure, and ESCR matters for HDPE exposed to chemicals, where F50 above 1,000 hours is the request.