What Automated Production Steps Ensure Precision Driveline Forging Tolerances?
Precision automotive driveline manufacturing relies on a 16-stage vertically integrated production workflow. Starting from raw steel bar cutting, isothermal annealing, and precision cold or warm forging, components undergo automated internal spline broaching and hard turning on robotic CNC lathes. Subsequent CQI-9 heat treatment and 3D CMM metrology verify raceway concentricity within tight tolerances.
Key Takeaways
- DEWIN coordinates regional manufacturing across China, Vietnam, and Thailand using a 26-person engineering hub in Xi'an and 7 local staff in Ho Chi Minh City.
- Driveline components utilize a 16-stage vertically integrated process flow including cold or warm forging, internal spline broaching, robotic CNC turning, and CQI-9 heat treatment.
- Multi-facility quality control integrates pre-quote DFM tolerance analysis, PPAP Level 3 documentation, ZEISS 3D CMM inspection, and a 50 PPM defect target.
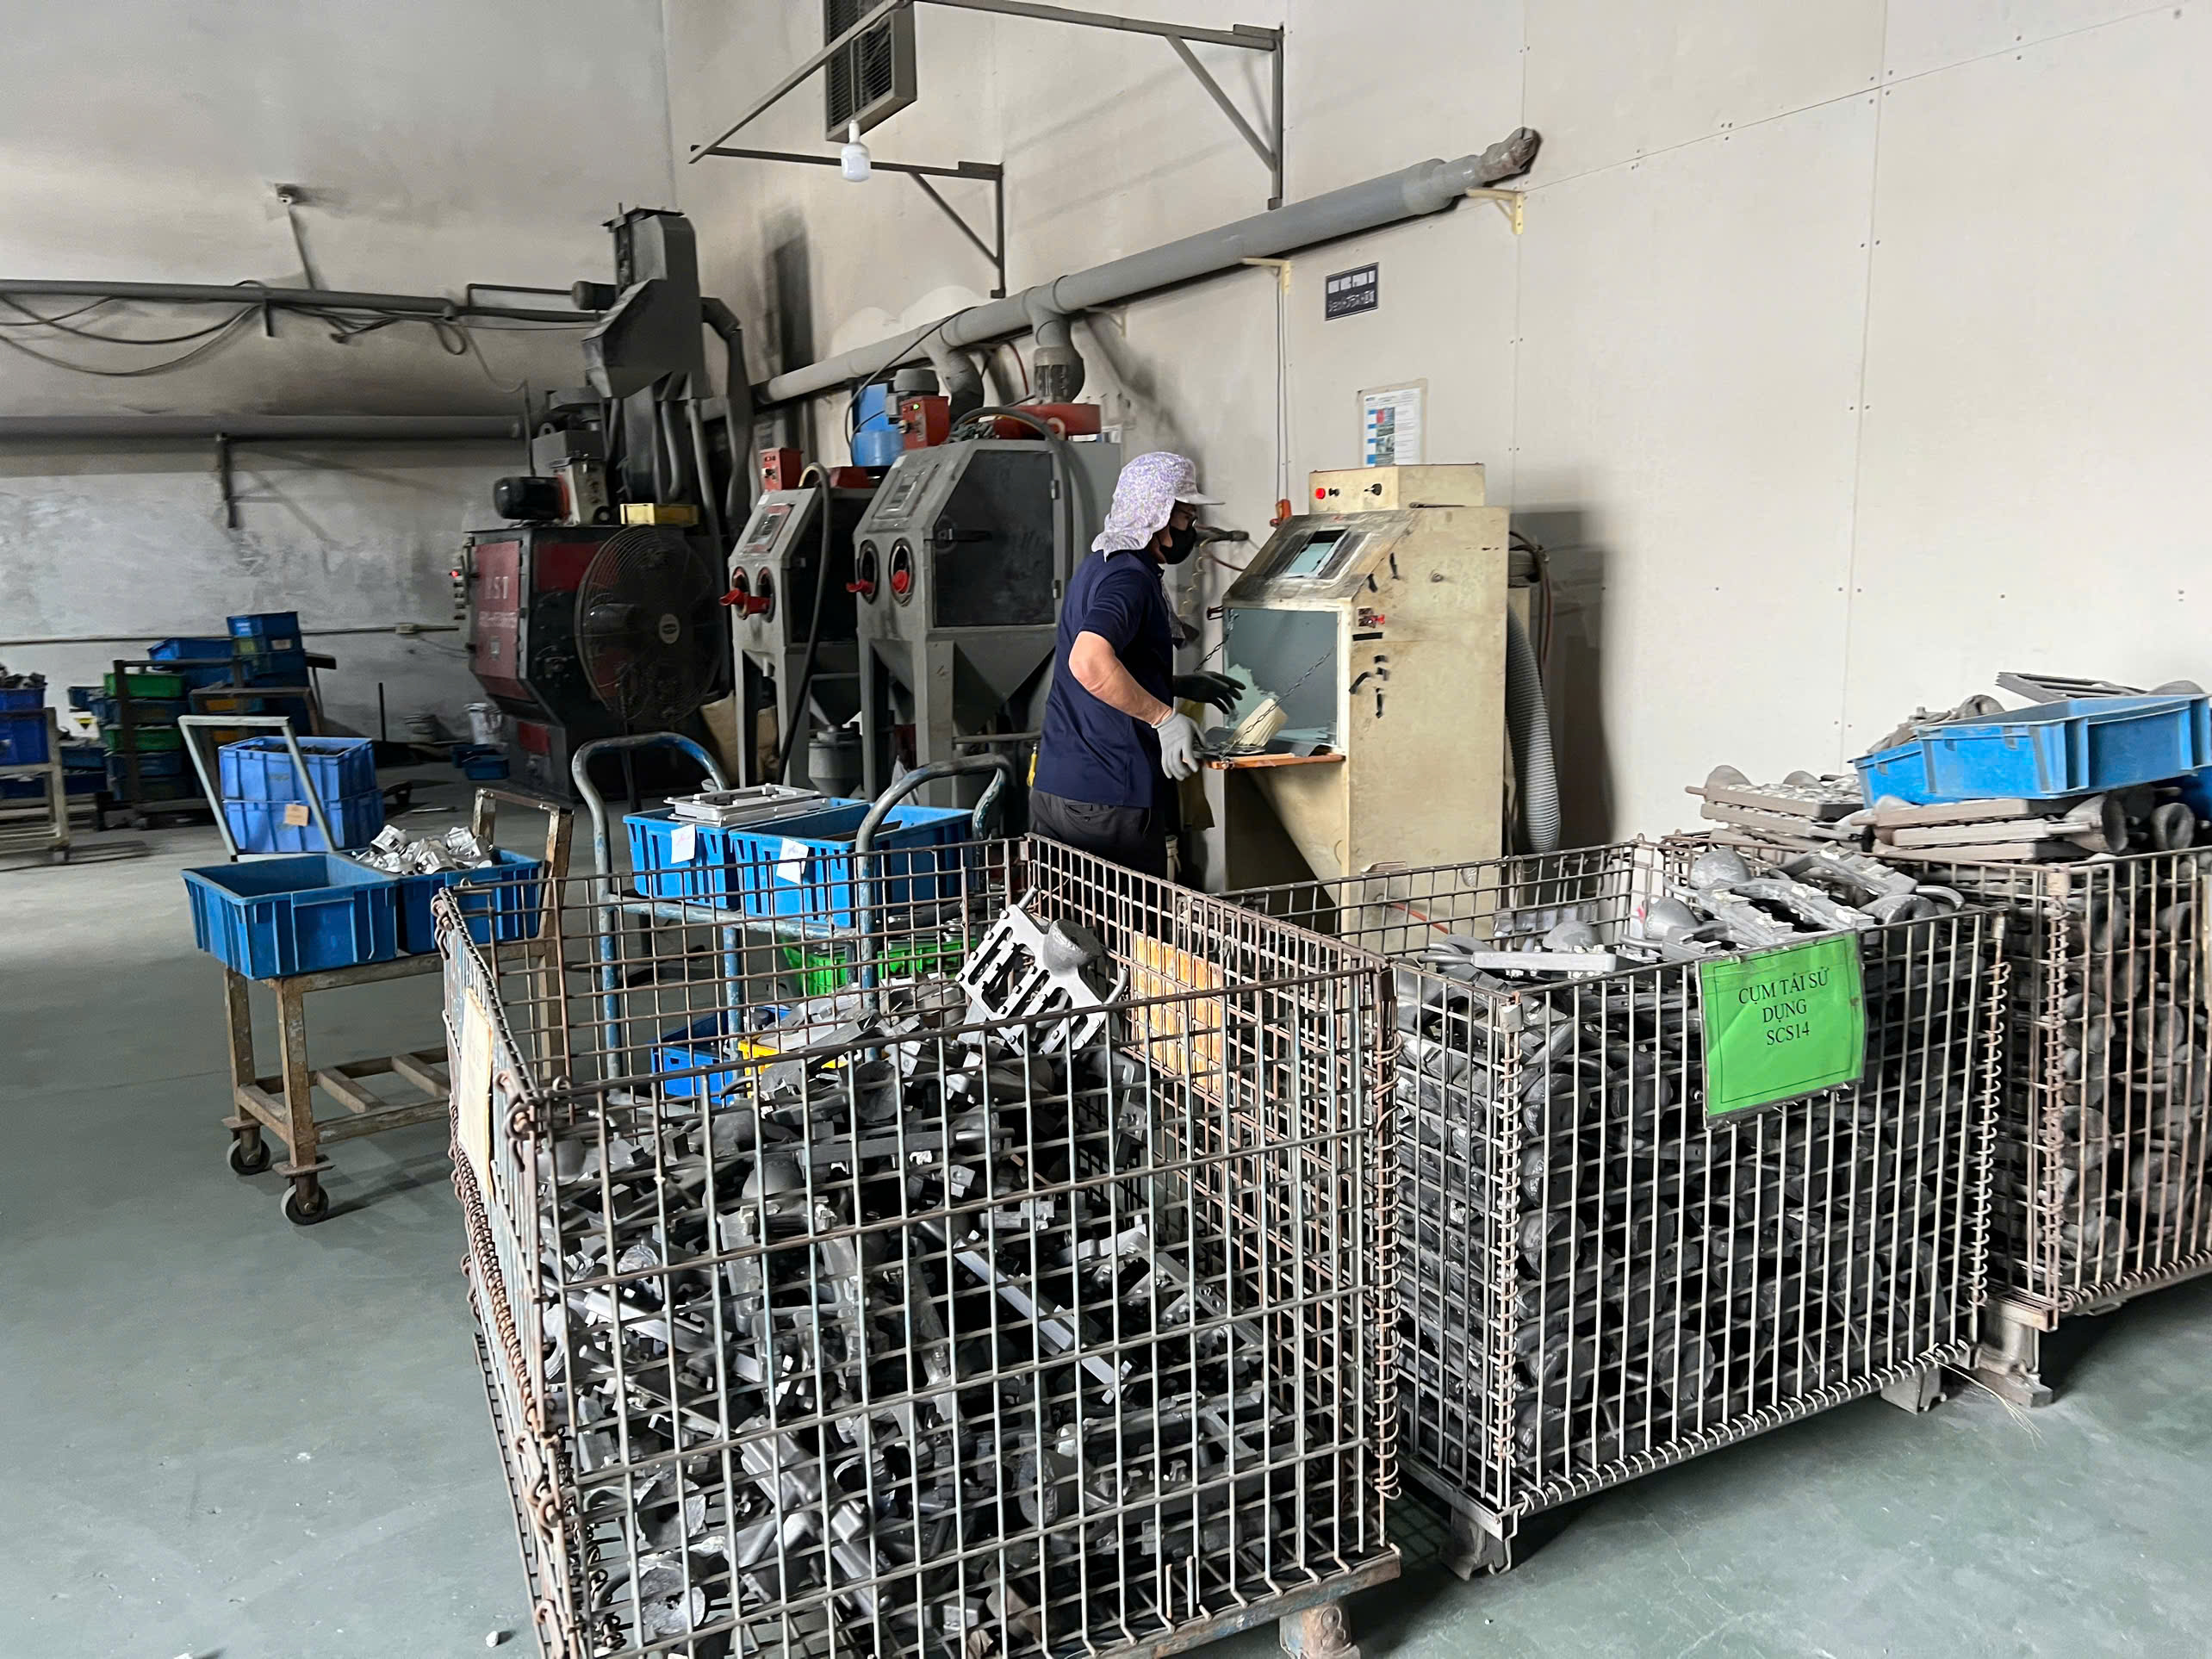
Driveline components such as CV joint star sleeves, trunnions, and spline shafts require precise metallurgical structure and controlled dimensional accuracy. Facilities like Ningbo Keminsheng Machinery utilize 160T to 630T closed-die forging presses combined with isothermal normalizing to achieve uniform ferrite-pearlite grain flow before machining.
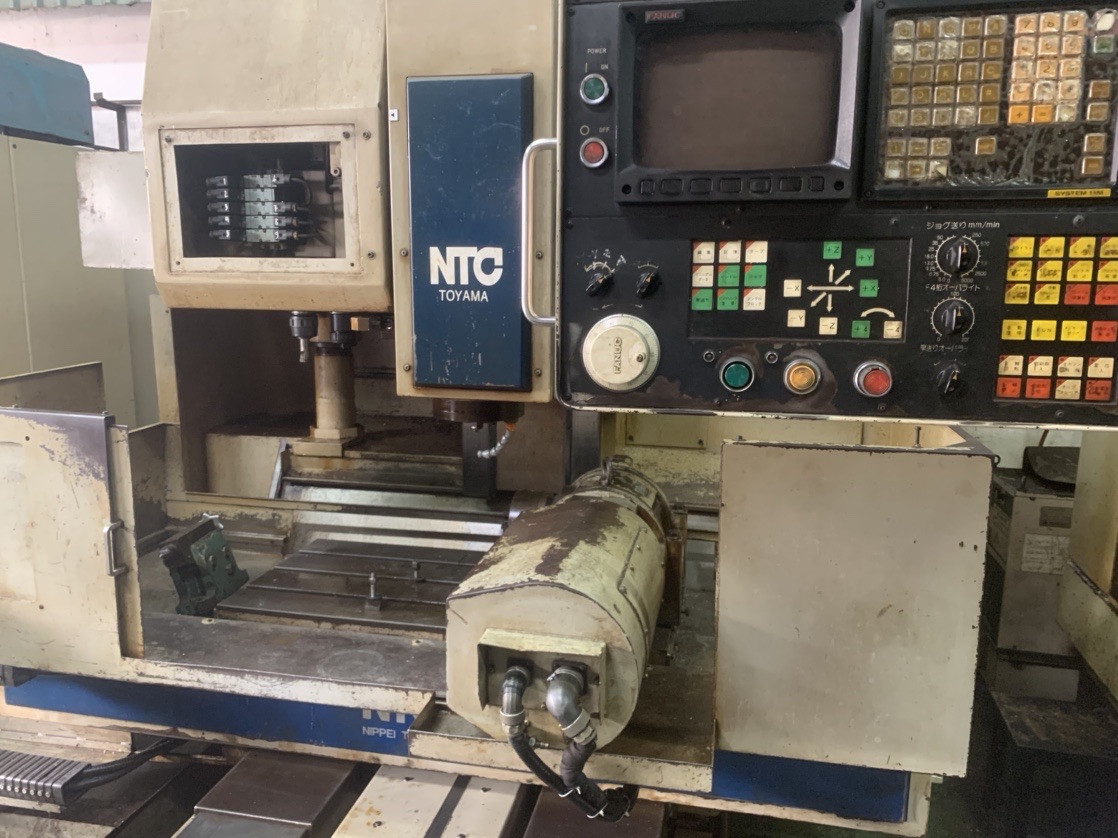
High-speed hydraulic pull broaching along with automated hard turning across 136 robotic CNC lathes and EMAG machining cells maintains a raceway concentricity tolerance of plus or minus 0.008 mm. Components then pass through continuous CQI-9 carbonitriding furnaces to achieve case hardening of HRC 58 to 62 before 100 percent eddy-current crack sorting and vacuum anti-rust packaging.
- Precision closed-die forging blanks from 160T to 630T presses with isothermal normalizing
- Internal spline broaching maintaining DIN 5480 and JIS B 1603 module standards
- High-speed automated turning using 136 robotic CNC lathes and 4 German EMAG centers
- Controlled CQI-9 furnace carbonitriding achieving HRC 58 to 62 hardness at 0.85 to 1.25 mm case depth
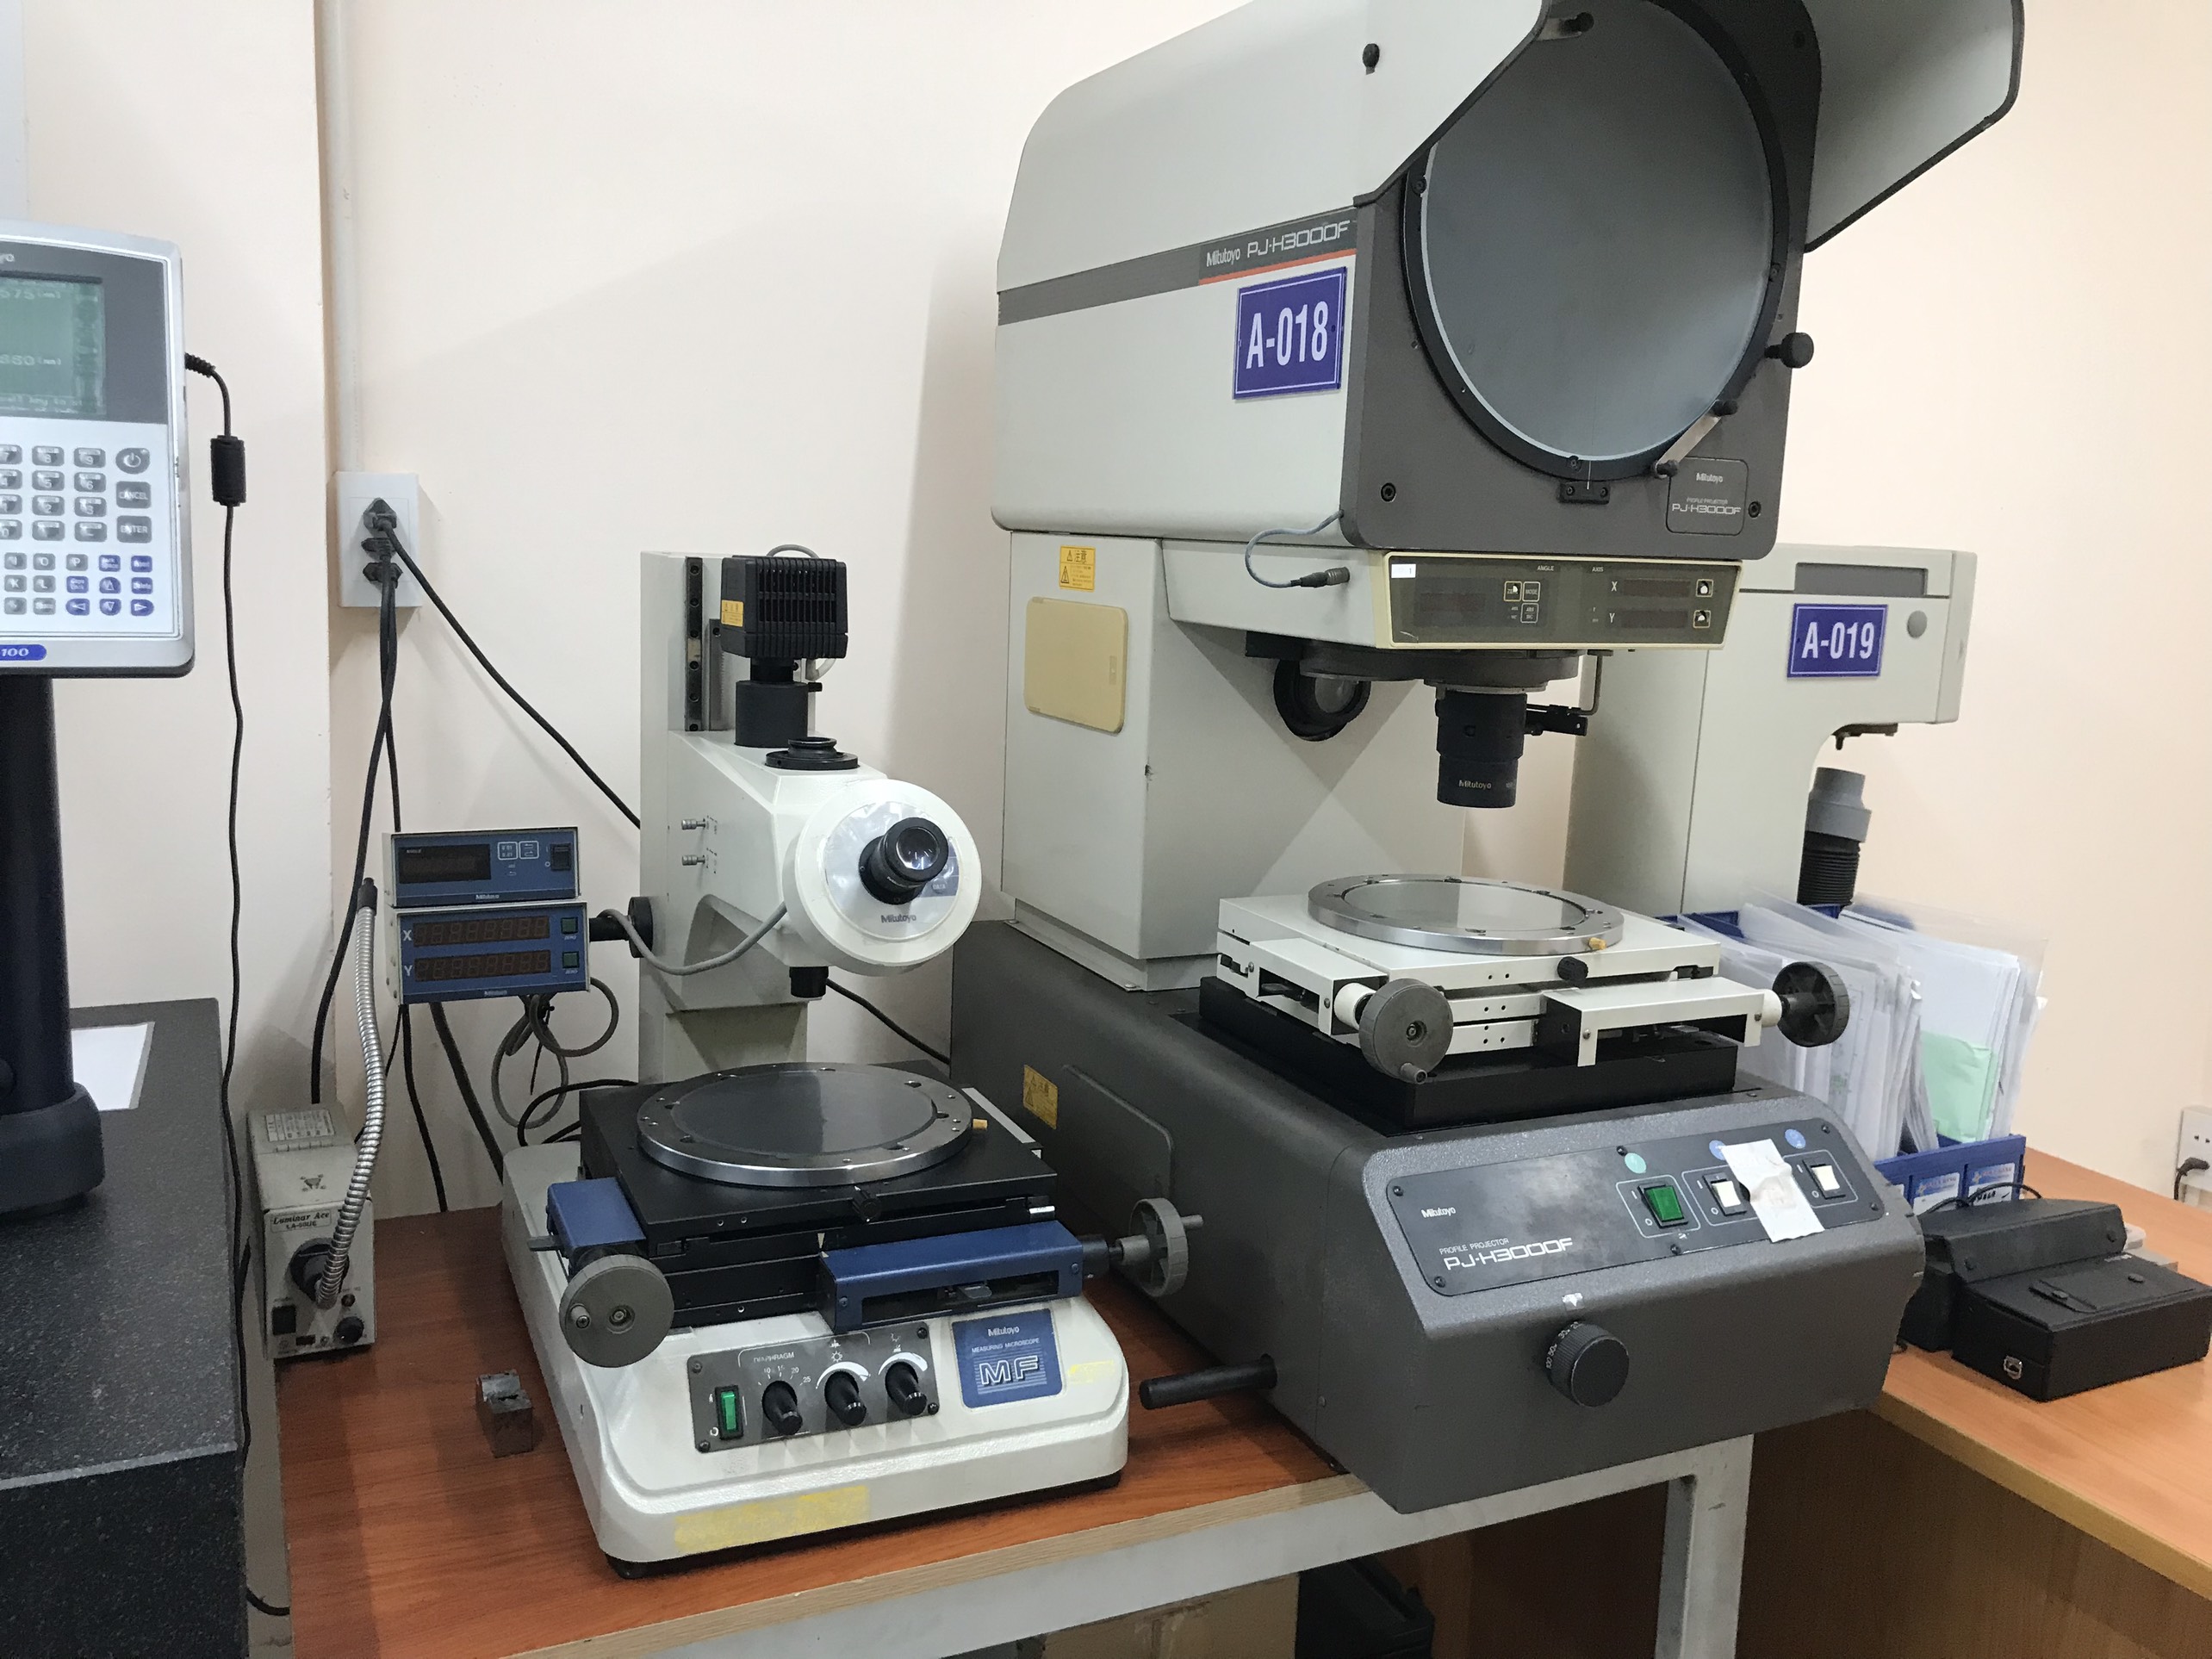
- Quality metrology utilizing ZEISS and Mitutoyo 3D CMMs, surface contour meters, and eddy-current crack detection
How Do Regional Engineering Facilities Manage Supplier Coordination and Quality Benchmarks?
Engineering teams manage multi-hub production by placing local technical staff directly on the ground in regional centers. A 26-person center in Xi'an and 7 local staff in Ho Chi Minh City manage QCLDM audits, DFM tolerance reviews, and PPAP Level 3 documentation to maintain a 50 PPM defect benchmark across supplier networks.
Coordinating complex components across specialized Asian factories requires standardized quality gates prior to mass production. Pre-quote DFM engineering includes 2D and 3D tolerance stack analysis, mold flow simulations, and progressive die evaluations before tooling fabrication begins.
Quality execution involves resident supplier quality engineer (SQE) audits, raw material analysis documentation, and in-process 3D CMM verification. This structured oversight allows engineering hubs to manage production programs across powder metallurgy, oilless bearings, aerospace 5-axis CNC machining, and heavy stamping facilities.
- DFM analysis featuring 2D and 3D tolerance verification and progressive die simulation
- Formal PPAP Level 3 documentation including material certificates and dimensional inspection records
- In-process dimensional metrology conducted via temperature-controlled ZEISS CMM labs
- Targeted quality control benchmark of 50 PPM maximum defect rates for high-volume automotive parts
Which Manufacturing Processes Support Custom Metal and Fluoropolymer Components?
Specialized manufacturing options range from sintered powder metallurgy and die casting to aerospace-grade 5-axis CNC machining and high-purity fluoropolymer molding. Specialist facilities produce oil-impregnated bronze bushings, heavy slewing bearings up to 5,000 mm in diameter, and cleanroom-machined PEEK or PTFE components for industrial applications.
Powdertrain and structural component programs leverage automated powder presses from 15T to 500T alongside mesh-belt and vacuum sintering furnaces. Facilities such as Jiande Welfine and Jiangmen Qiantong produce structural iron, copper, and stainless steel PM parts, as well as complex 17-4PH metal injection molded (MIM) components.
For high-temperature or high-purity industrial requirements, Zhenjiang RunFun provides cleanroom assembly and high-temperature injection molding of PTFE, PFA, and PEEK fluoropolymers. Aerospace and defense housings are machined at Hangtuo Luoyang using 5-axis CNC centers under AS9100D control systems.
- Powder Metallurgy & MIM: 15T to 500T CNC powder presses and vacuum sintering for structural gears and oil-impregnated bronze bushings
- Slewing Bearings: Single, double-row ball, and crossed-roller bearings from 200 mm to 5,000 mm diameter
- Precision CNC Machining: AS9100D aerospace 5-axis machining centers and turn-mill compounds for titanium and aluminum valve blocks
- Fluoropolymer Processing: Cleanroom molding and multi-axis CNC machining of PTFE, PEEK, PFA, and FFKM seals
When Can Procurement Teams Integrate Multi-Country Production Footprints?
Procurement teams integrate multi-country production footprints by using unified engineering partners to manage factory transfers across China, Vietnam, and Thailand. Transfer playbooks help migrate tooling, dies, and inspection gauges over a 10-month window without interrupting serial component supply or compromising quality standards.
Establishing production redundancy across Southeast Asian hubs allows industrial buyers to secure alternative manufacturing footprints while leveraging established tooling designs. For instance, driveline production launched at Ningbo Keminsheng can be synchronized with its upcoming 2027 plant in Thailand to provide continuous component sourcing.
Turnkey product lines, such as Bac Ninh-manufactured hydraulic hand pallet trucks or stamped fire extinguisher brackets, benefit from multi-country supply paths. Centralized trade services anchored by a Singapore headquarters streamline billing and audit coordination under Net 90 credit terms across regional manufacturing sites.
- 10-month production migration playbook for transferring dies, fixtures, and inspection gauges between regions
- Unified contract and billing administration managed through a Singapore headquarters with up to Net 90 credit terms
- Dual-country stamped assembly options for SPCC and SS304 brackets with 240-hour ASTM B117 salt spray protection
- European-standard hand pallet truck manufacturing in Bac Ninh, Vietnam with integrated cast-iron hydraulic pumps
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What quality documentation is provided prior to serial mass production?
Production programs utilize pre-quote DFM drawing reviews, PPAP Level 3 submissions, material certificates of analysis, and ZEISS 3D CMM inspection records to confirm dimensional accuracy before mass release.
How are spline shaft raceway tolerances controlled during high-volume manufacturing?
Concentricity tolerances of plus or minus 0.008 mm are maintained by combining 160T to 630T precision closed-die forging with 136 robotic CNC turning centers and high-speed hydraulic pull broaching.
What materials are available for powder metallurgy and MIM component manufacturing?
Options include iron, copper, SAE841 Sint B50 bronze, soft magnetic alloys, and vacuum-sintered 304, 316L, and 17-4PH stainless steels for automotive and industrial structural applications.
What testing procedures evaluate protective coatings on stamped metal brackets?
Stamped SPCC and SS304 fire extinguisher brackets undergo 240-hour minimum ASTM B117 salt spray testing and 1,500-hour UV powder coat exposure evaluations to ensure corrosion resistance.