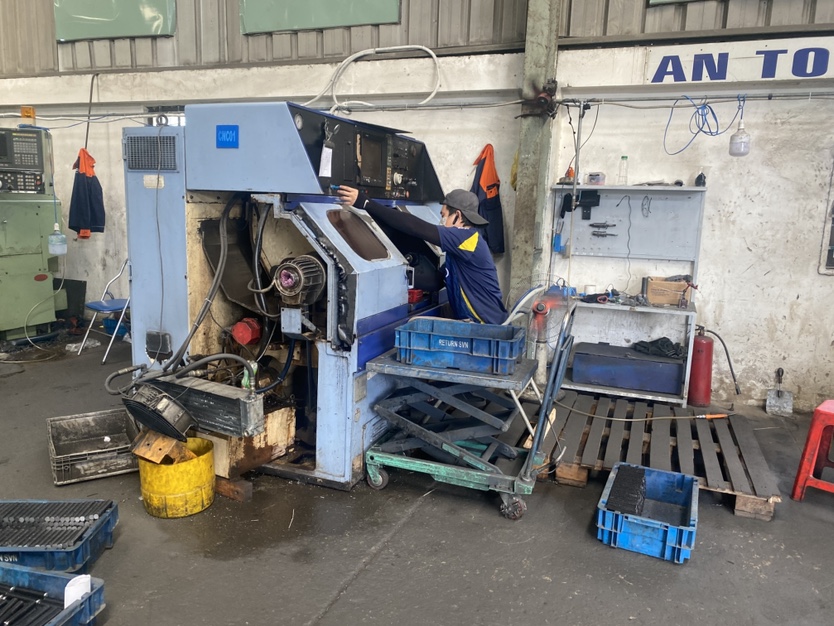
What Processes Support Driveline Component Forging and Machining?
Driveline component production relies on a 16-stage integrated manufacturing chain including bar cutting, isothermal annealing, closed-die forging, internal spline broaching, and robotic CNC turning. Automated heat treatment and grinding establish required surface hardness and dimensional precision, supported by eddy-current crack detection and 3D CMM inspection.
Key Takeaways
- Xi'an and Ho Chi Minh City engineering centers coordinate factory audits, DFM reviews, and ZEISS CMM inspection across regional production facilities.
- Driveline component production combines 160T-630T closed-die forging, internal spline broaching, and CQI-9 carbonitriding to maintain ±0.008 mm concentricity.
- Advanced powder metallurgy and metal injection molding processes utilize 15-500T presses and vacuum-sintering furnaces to achieve high density and precise tolerances.
- Quality verification relies on 3D coordinate measuring machines, eddy-current testing, surface roughness analysis, and metallographic density verification.
Precision driveline manufacturing utilizes closed-die forging presses ranging from 160T to 630T along with isothermal normalizing to produce consistent grain flow in carburizing alloy steels such as 20CrMnTi and SAE 5120H. Internal splines are formed using high-speed hydraulic pull broaching, followed by machining on automated lathe lines.
Thermal processing utilizes CQI-9 controlled carbonitriding furnaces to achieve a case depth of 0.85 mm to 1.25 mm and a hardness range of HRC 58 to 62. Final quality checks integrate eddy-current testing, magnetic particle crack inspection, contour analysis, and ultrasonic cleaning before vacuum anti-rust packaging.
- Closed-die warm and cold precision forging using 160T to 630T presses
- High-speed hydraulic pull broaching holding ±0.008 mm raceway concentricity
- CQI-9 controlled furnace carbonitriding achieving HRC 58–62 surface hardness
- Dimensional validation via ZEISS and Mitutoyo 3D CMM metrology systems
How Are Advanced Powder Metallurgy Components and Bearings Manufactured?
Powder metallurgy and bearing production utilize automatic CNC powder presses from 15T to 500T, mesh-belt sintering, and vacuum debinding technologies. Iron, copper, and stainless steel powders are processed into structural gears, oil-impregnated bushings, and complex metal injection molded components meeting high-density and strict dimensional specifications.
Powder metallurgy (PM) and metal injection molding (MIM) facilities convert raw metal powders into high-density structural transmission sprockets, oil pump rotors, and shock absorber pistons. Sintering occurs in controlled mesh-belt and vacuum furnaces, followed by steam treatment or secondary CNC machining when tight tolerances are required.
Bearing manufacturing encompasses PTFE composite self-lubricating bushings, bimetal bearings, graphite-plugged bronze bearings, spherical plain bearings, and large-diameter slewing rings up to Ø5,000 mm. Spherical raceway grinding, automated liner bonding, and phosphating surface treatments deliver low-friction performance under high static loads.
- Automatic CNC powder pressing across 15T to 500T capacity ranges
- Vacuum debinding and sintering for 304 and 316L stainless steel components
- Metal injection molding (MIM) of complex 17-4PH and 316L structural hardware
- Spherical plain bearings with PTFE liners and slewing rings up to Ø5,000 mm diameter
Which Quality Management Controls Ensure Multi-Facility Compliance?
Quality management across regional manufacturing hubs relies on full DFM drawing reviews, PPAP Level 3 documentation, and resident quality engineering oversight. Technical teams perform 2D and 3D tolerance analysis, coordinate measuring machine inspections, metallographic microstructural evaluations, and functional load testing before authorizing serial shipment.
Quality engineering teams operating out of Xi'an (26 staff) and Ho Chi Minh City (7 staff) execute on-site facility audits and manage QCLDM benchmark metrics across verified suppliers. Pre-production review includes mold flow simulation, progressive die design validation, and pre-quote GD&T analysis to resolve tooling defects prior to steel cutting.
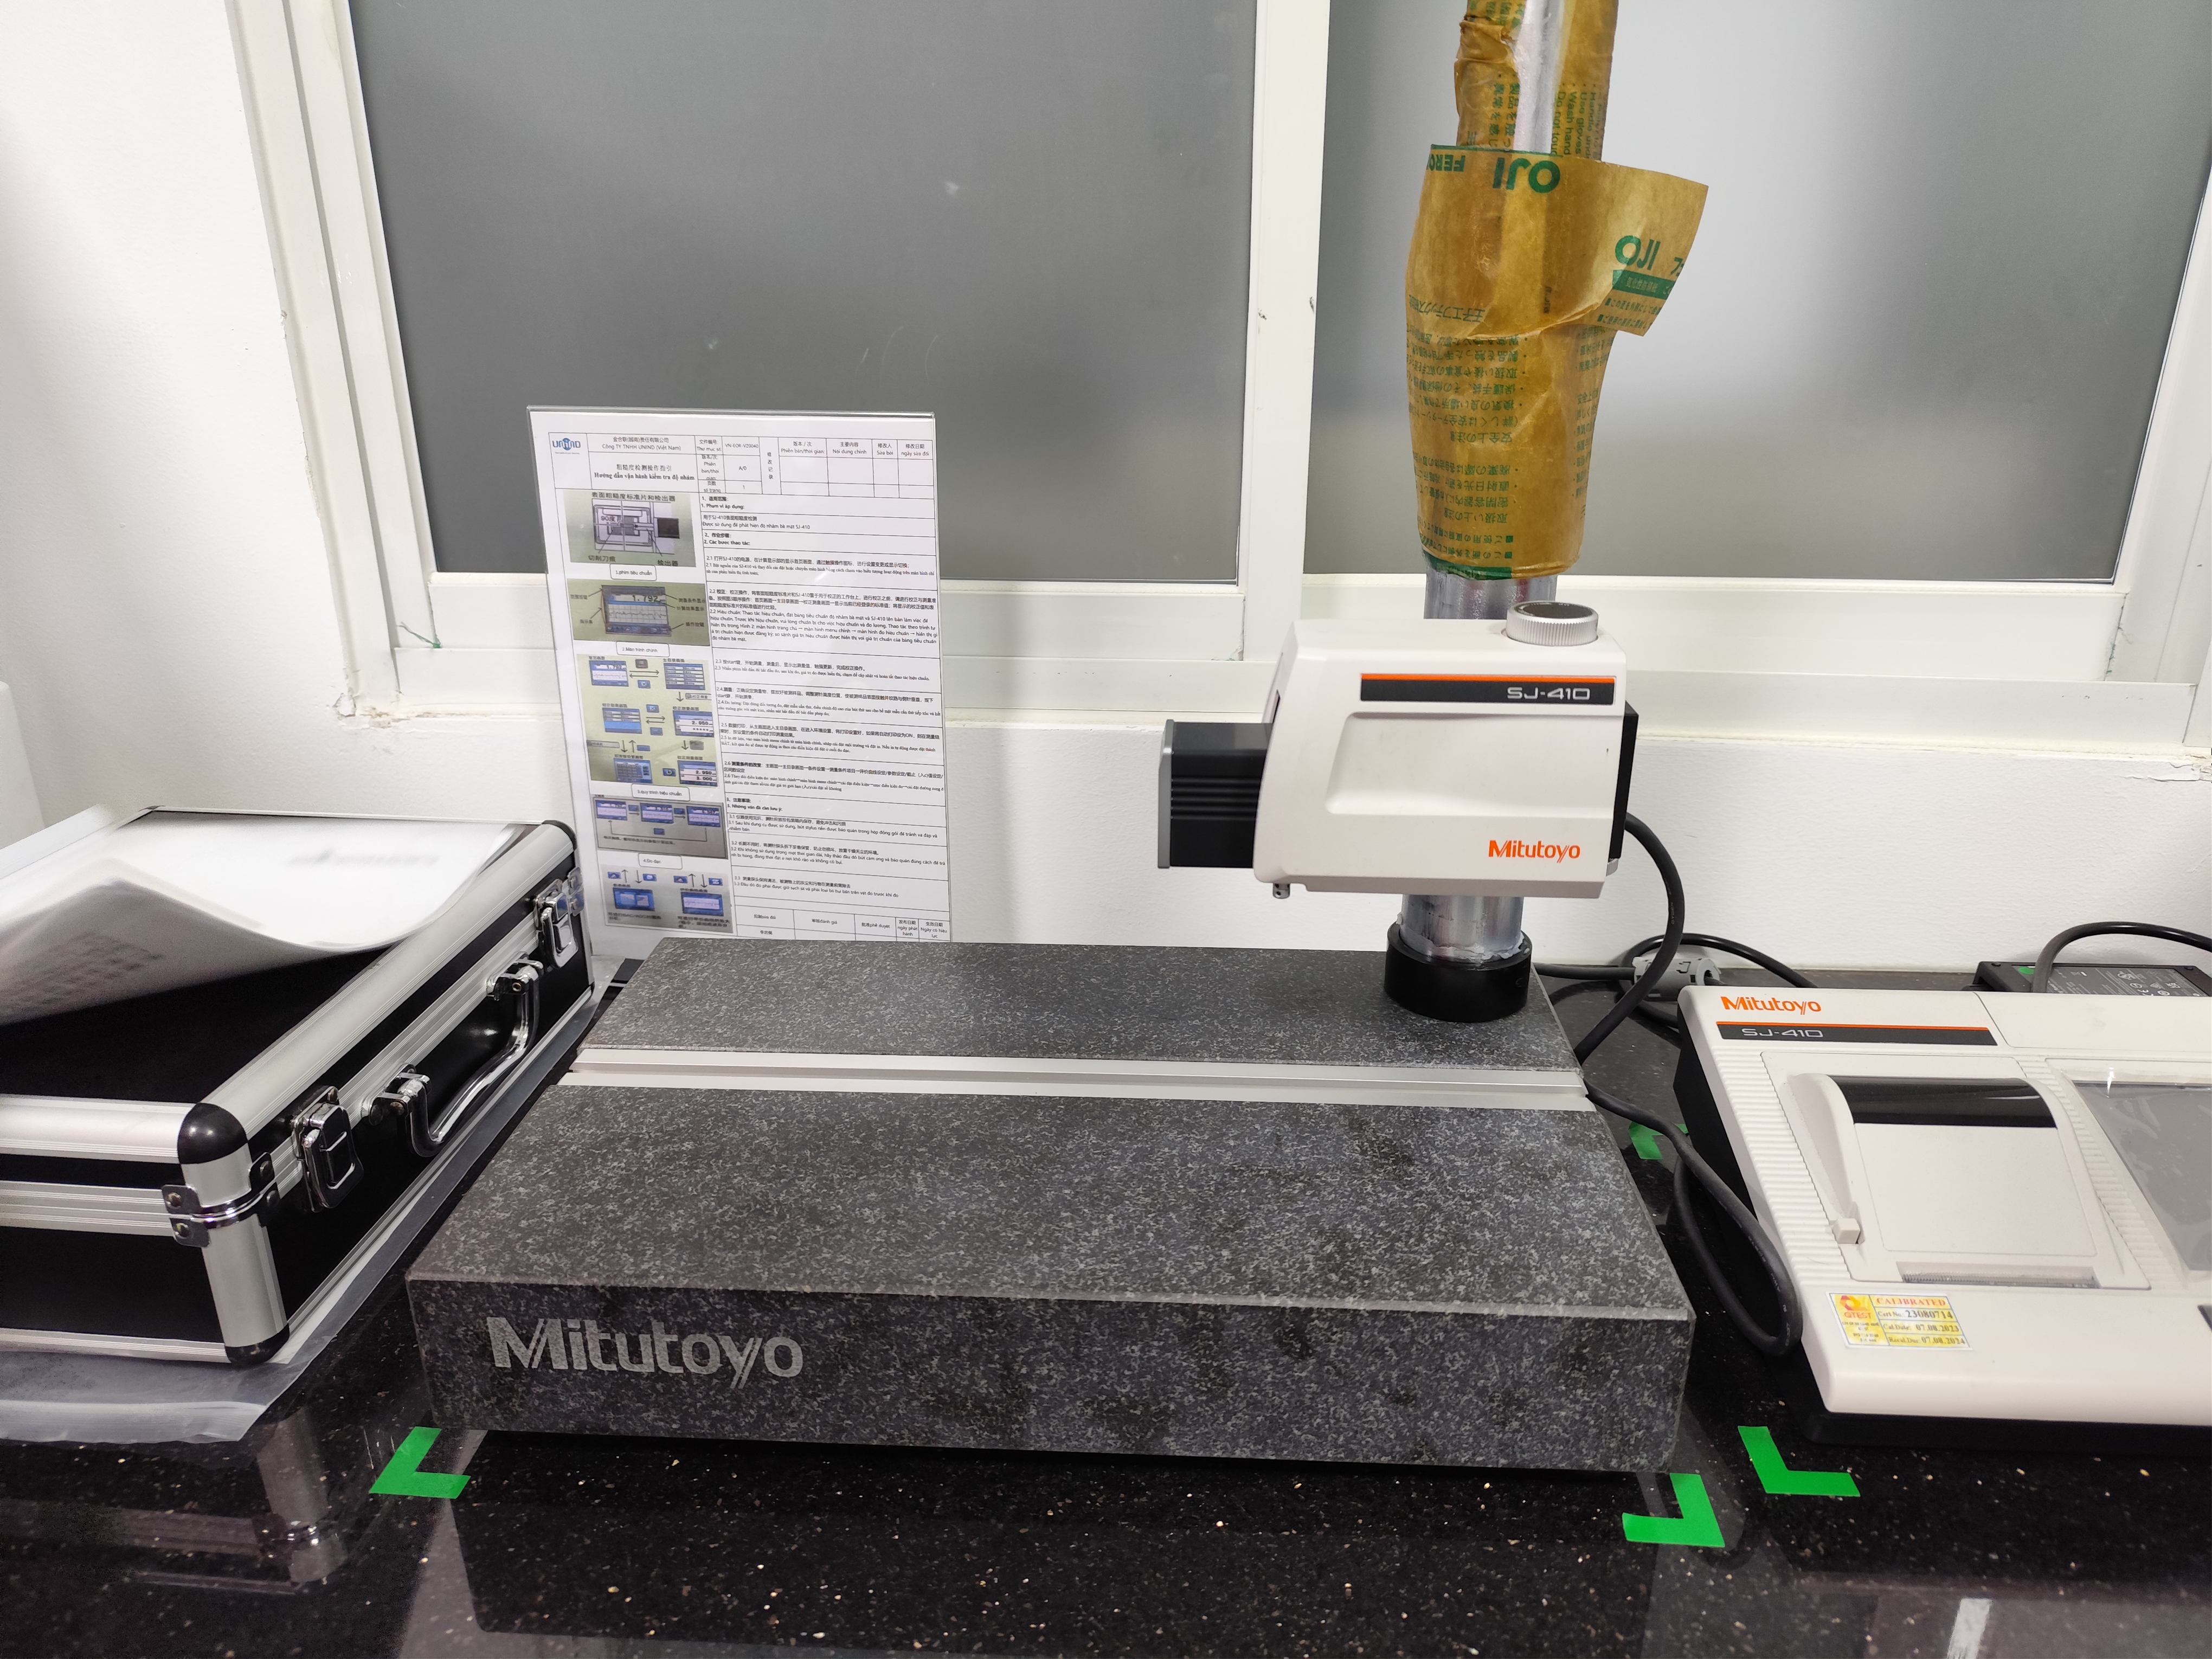
Metrology laboratories utilize ZEISS and Mitutoyo 3D CMMs, gear profile testers, surface roughness gages, and tribology test rigs. Inspection documentation including material chemical analysis, dimensional reports, salt-spray exposure data, and cycle load testing validates compliance across stamping, die casting, CNC machining, and assembly operations.
- PPAP Level 3 submission with initial sample inspection documentation
- 3D CMM metrology, contour evaluation, and gear profile analysis
- In-process eddy-current sorting and 100% magnetic particle crack inspection
- Salt-spray corrosion testing (240+ hours ASTM B117) and UV exposure analysis
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What engineering reviews occur before tooling production begins?
Pre-production engineering includes 2D and 3D design for manufacturability (DFM) reviews, geometric dimensioning and tolerancing (GD&T) analysis, progressive die layout, and mold flow simulation to verify component geometry before steel cutting.
What metrology equipment is used for dimensional verification?
Metrology laboratories utilize ZEISS and Mitutoyo 3D coordinate measuring machines (CMM), universal gear profile testers, contour instruments, surface roughness indicators, and metallographic density analysis systems.
How are internal splines and raceways produced on driveline parts?
Internal splines are formed using high-speed hydraulic pull broaching, while raceways are machined using hard-turning cells and 136 robotic CNC lathes to maintain raceway concentricity within ±0.008 mm.
What materials are available for custom fire extinguisher brackets and hand pallet trucks?
Fire extinguisher brackets use 2.0 mm to 4.0 mm SPCC steel or SS304 stainless steel with MIG/TIG welding, while hydraulic hand pallet trucks utilize cast-iron AC/DF hydraulic pumps, PU/nylon rollers, and heavy-gauge stamped steel frames.