How Do Regional Service Centers Manage Quality Control and DFM Review?
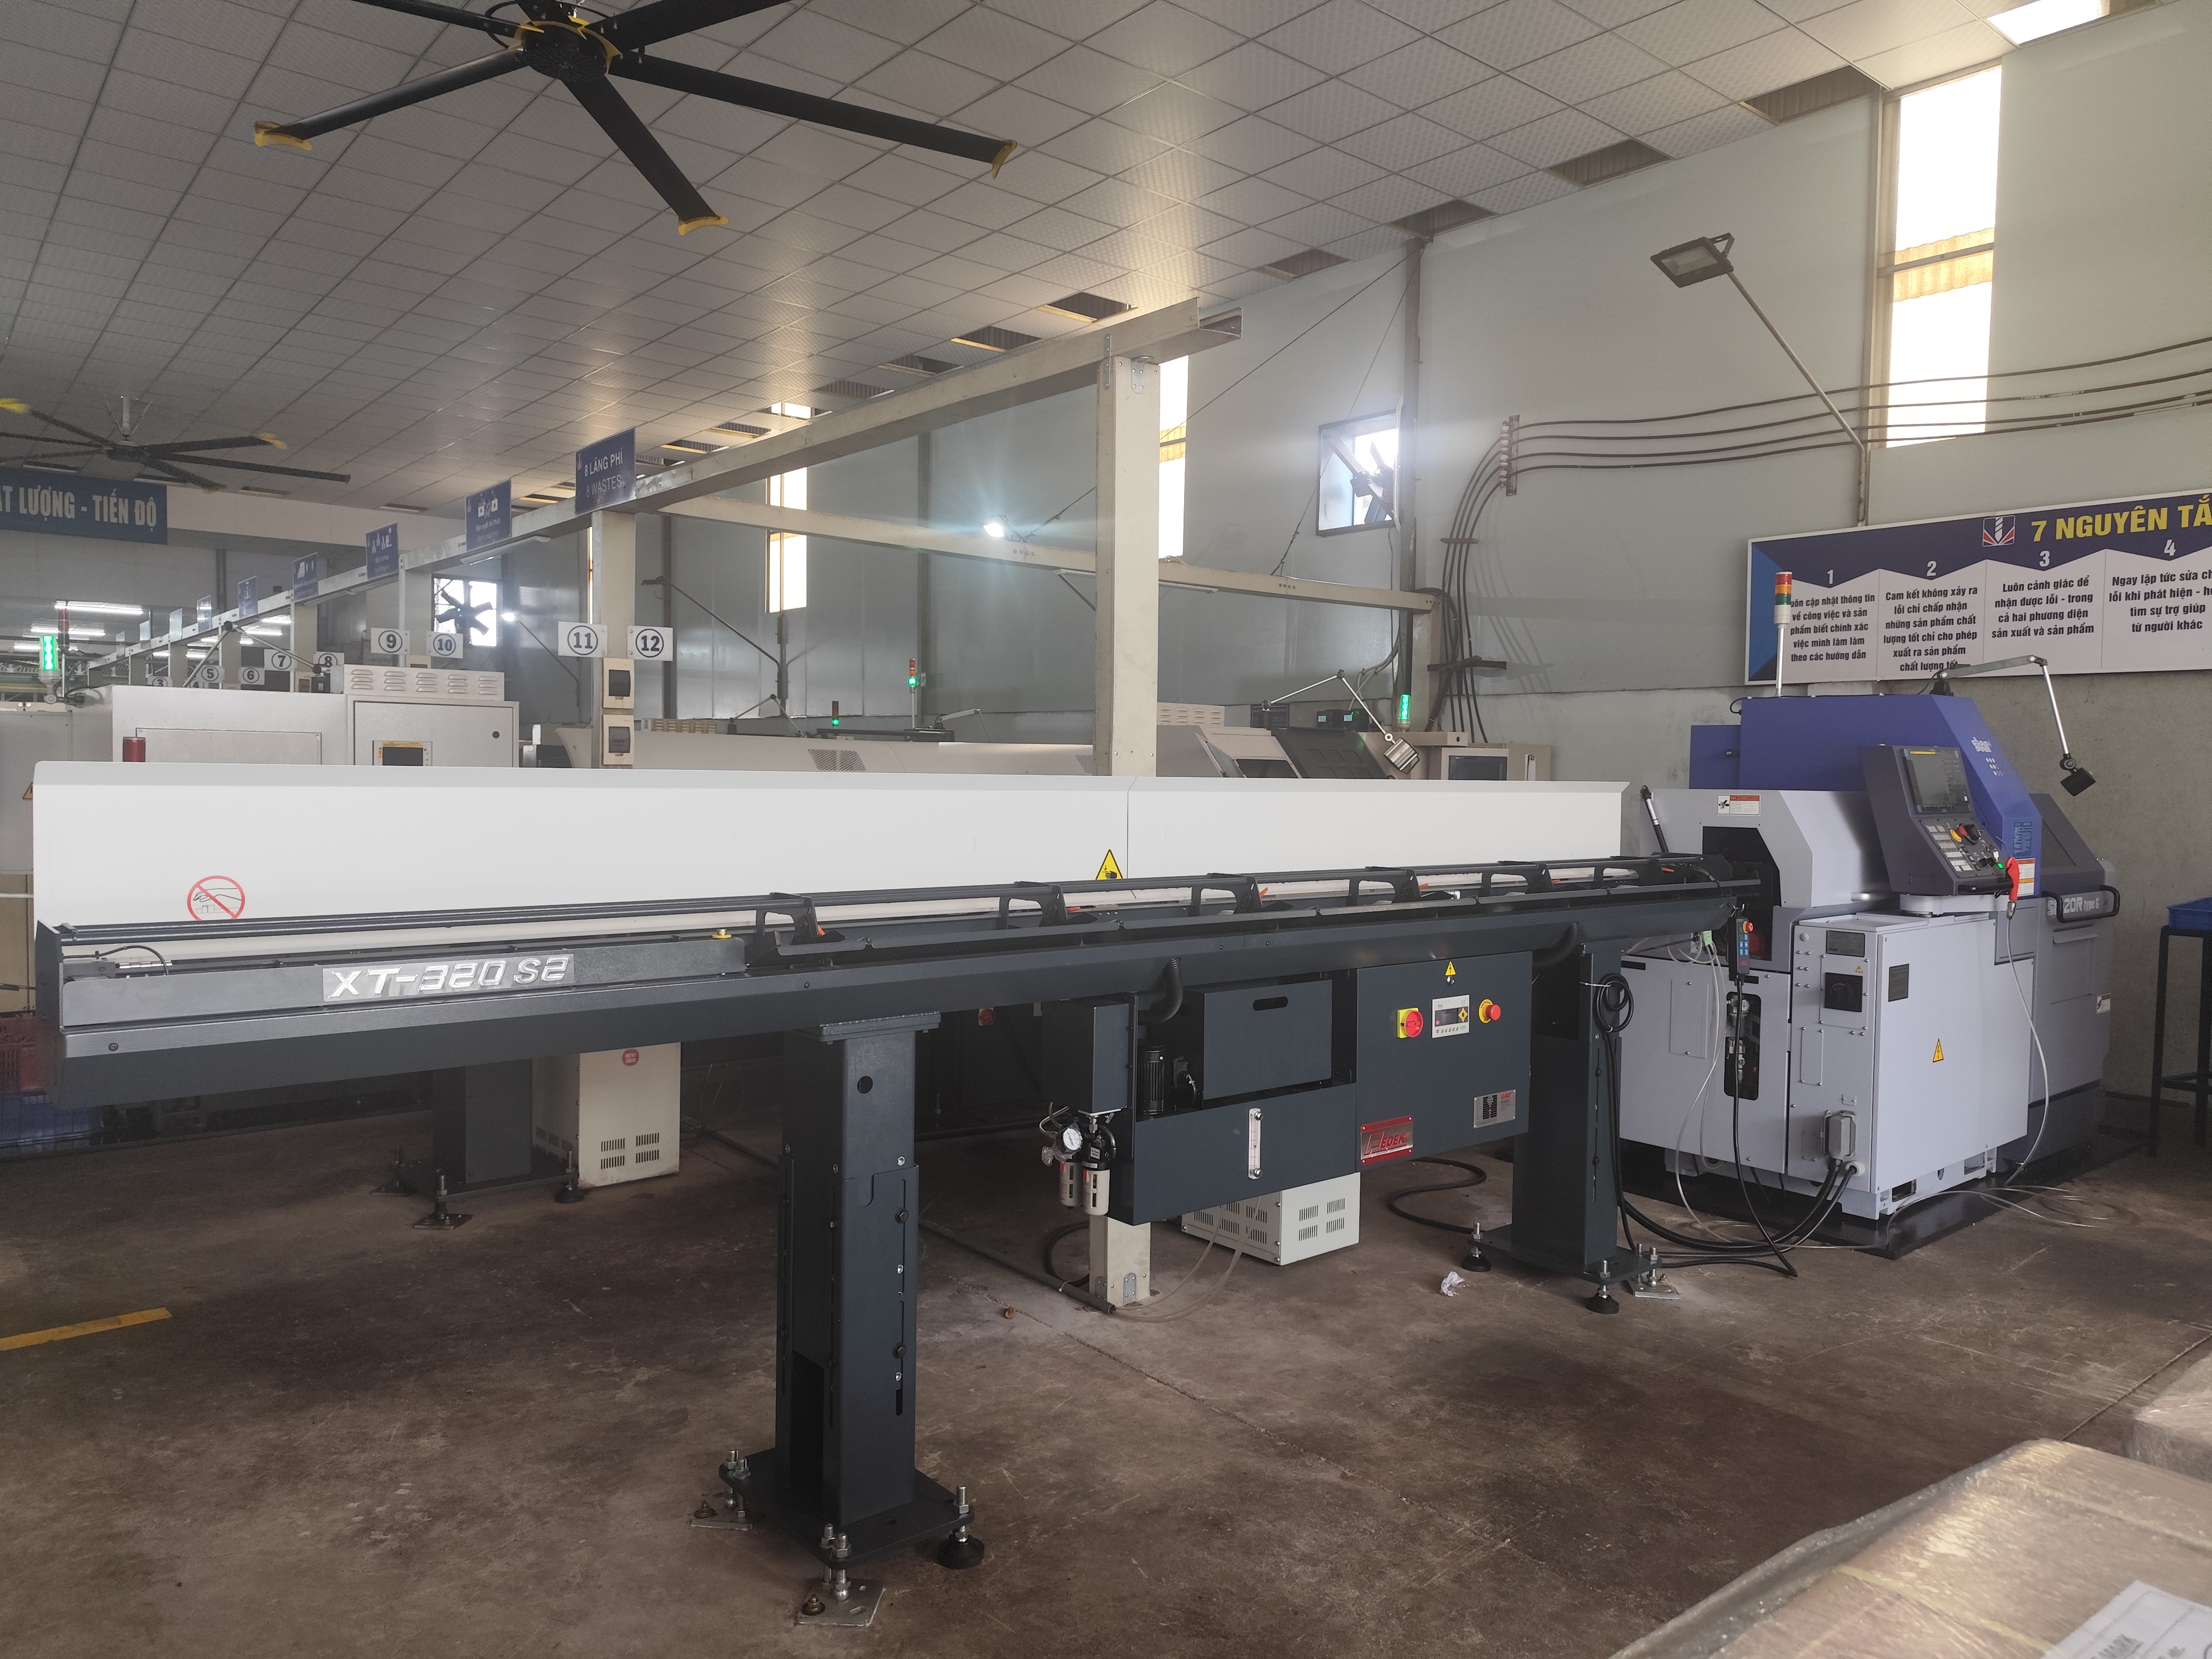
Regional service centers utilize embedded engineering teams to execute pre-quote DFM review, 2D and 3D tolerance analysis, mold flow simulations, and shop-floor quality audits across manufacturing hubs. Operating through Singapore headquarters alongside engineering staff in Xi'an, China and Ho Chi Minh City, Vietnam, these teams manage PPAP Level 3 documentation, in-process CMM metrology, and cross-border production transfers.
Key Takeaways
- Multi-country engineering oversight coordinated via Singapore HQ, a 26-person Xi'an center, and a 7-person Ho Chi Minh City team manages DFM, tooling, and quality across regional factories.
- Precision forging processes hold internal spline pitch tolerances of ±0.008 mm with HRC 58–62 case depth achieved through controlled carbonitriding furnaces.
- Automated inspection frameworks combine ZEISS 3D CMM metrology labs, eddy-current crack sorting, metallographic density verification, and a 50 PPM benchmark target.
Engineering coordination starts prior to tool production by validating 2D drawings, GD&T requirements, and 3D CAD models. Xi'an-based engineers analyze progressive die design, mold flow, and material selection for complex structural components, powder metallurgy sintered parts, and precision CNC valve blocks. This early engineering review prevents dimensional mismatches before tooling steel is cut.
On-site inspection protocol incorporates resident quality control engineers conducting supplier factory audits, in-process CMM measurements, and pre-shipment container loading audits. Quality benchmarking targets 50 PPM defect levels utilizing ZEISS 3D Coordinate Measuring Machines, metallographic density verification, and material composition analysis (COA) to maintain consistency across high-volume production lines.
- Pre-quote DFM intake featuring 2D/3D tolerance analysis and progressive die design.
- Quality benchmarking using PPAP Level 3 documentation and 50 PPM defect target control.
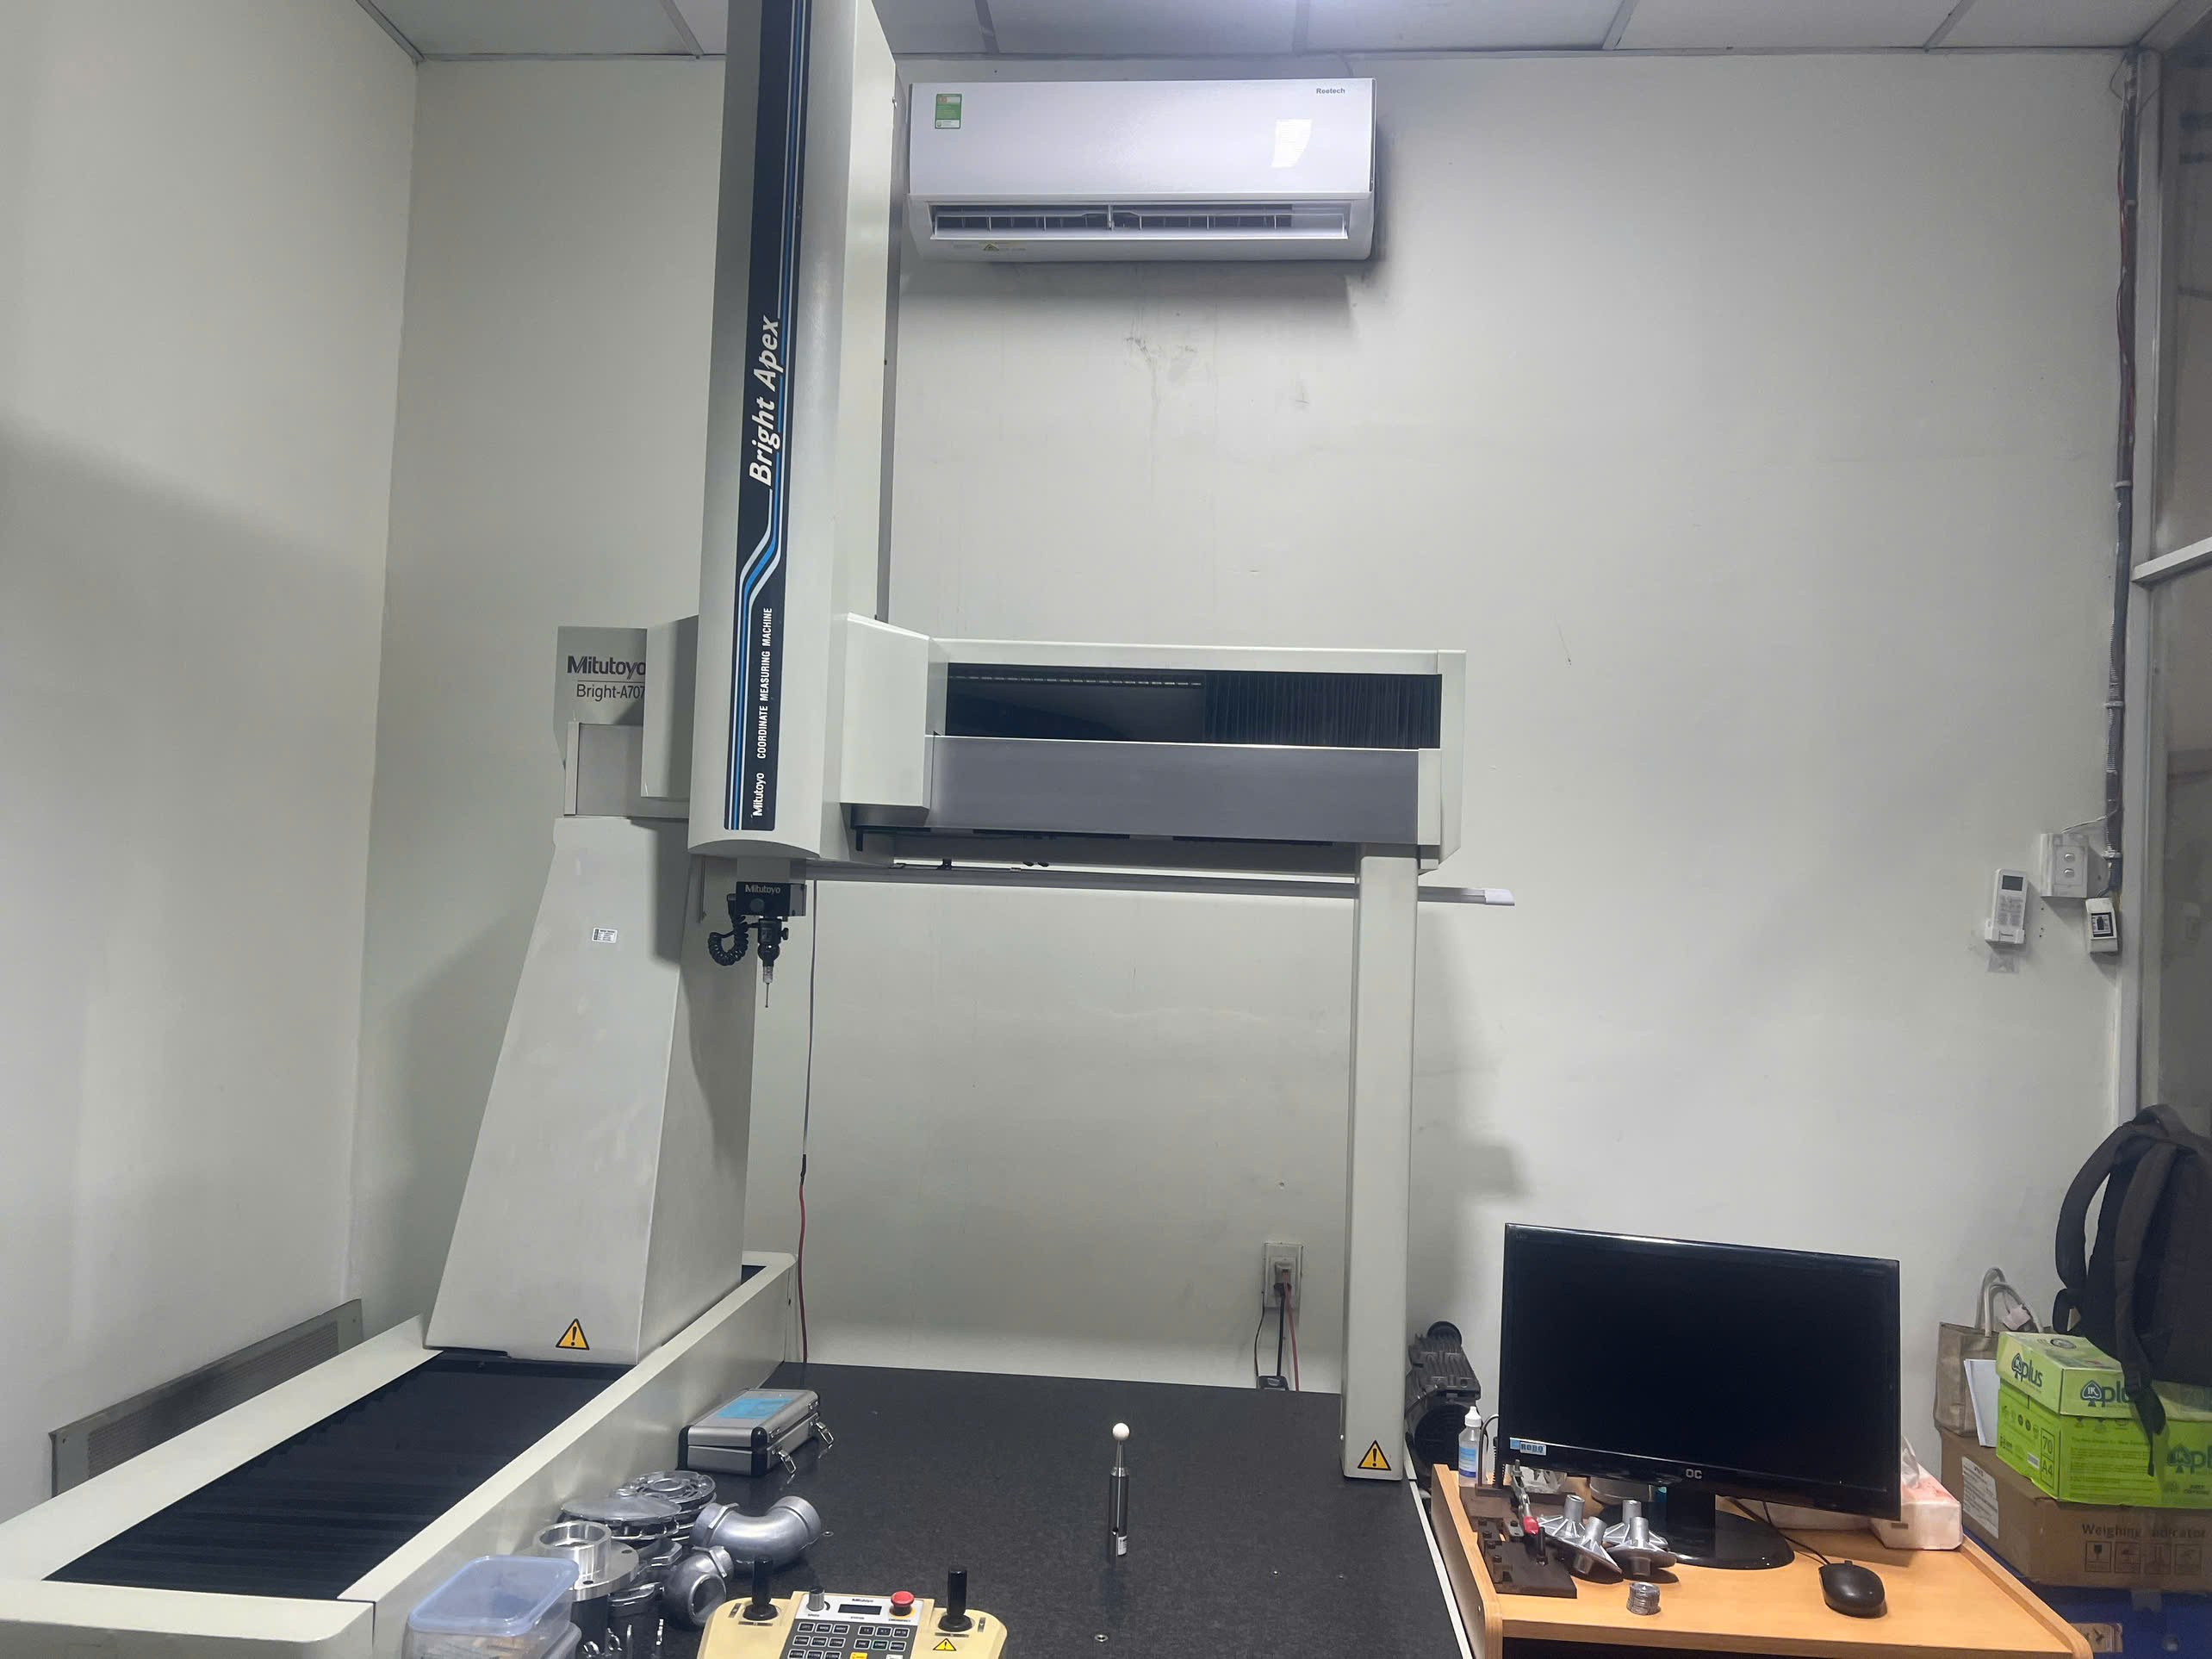
- In-process metrology equipped with ZEISS and Mitutoyo 3D CMM inspection systems.
- Comprehensive factory auditing covering QCLDM metrics, tooling milestones, and FAI tracking.
What Precision Tolerances Are Achieved in Driveline Forging and CNC Machining?
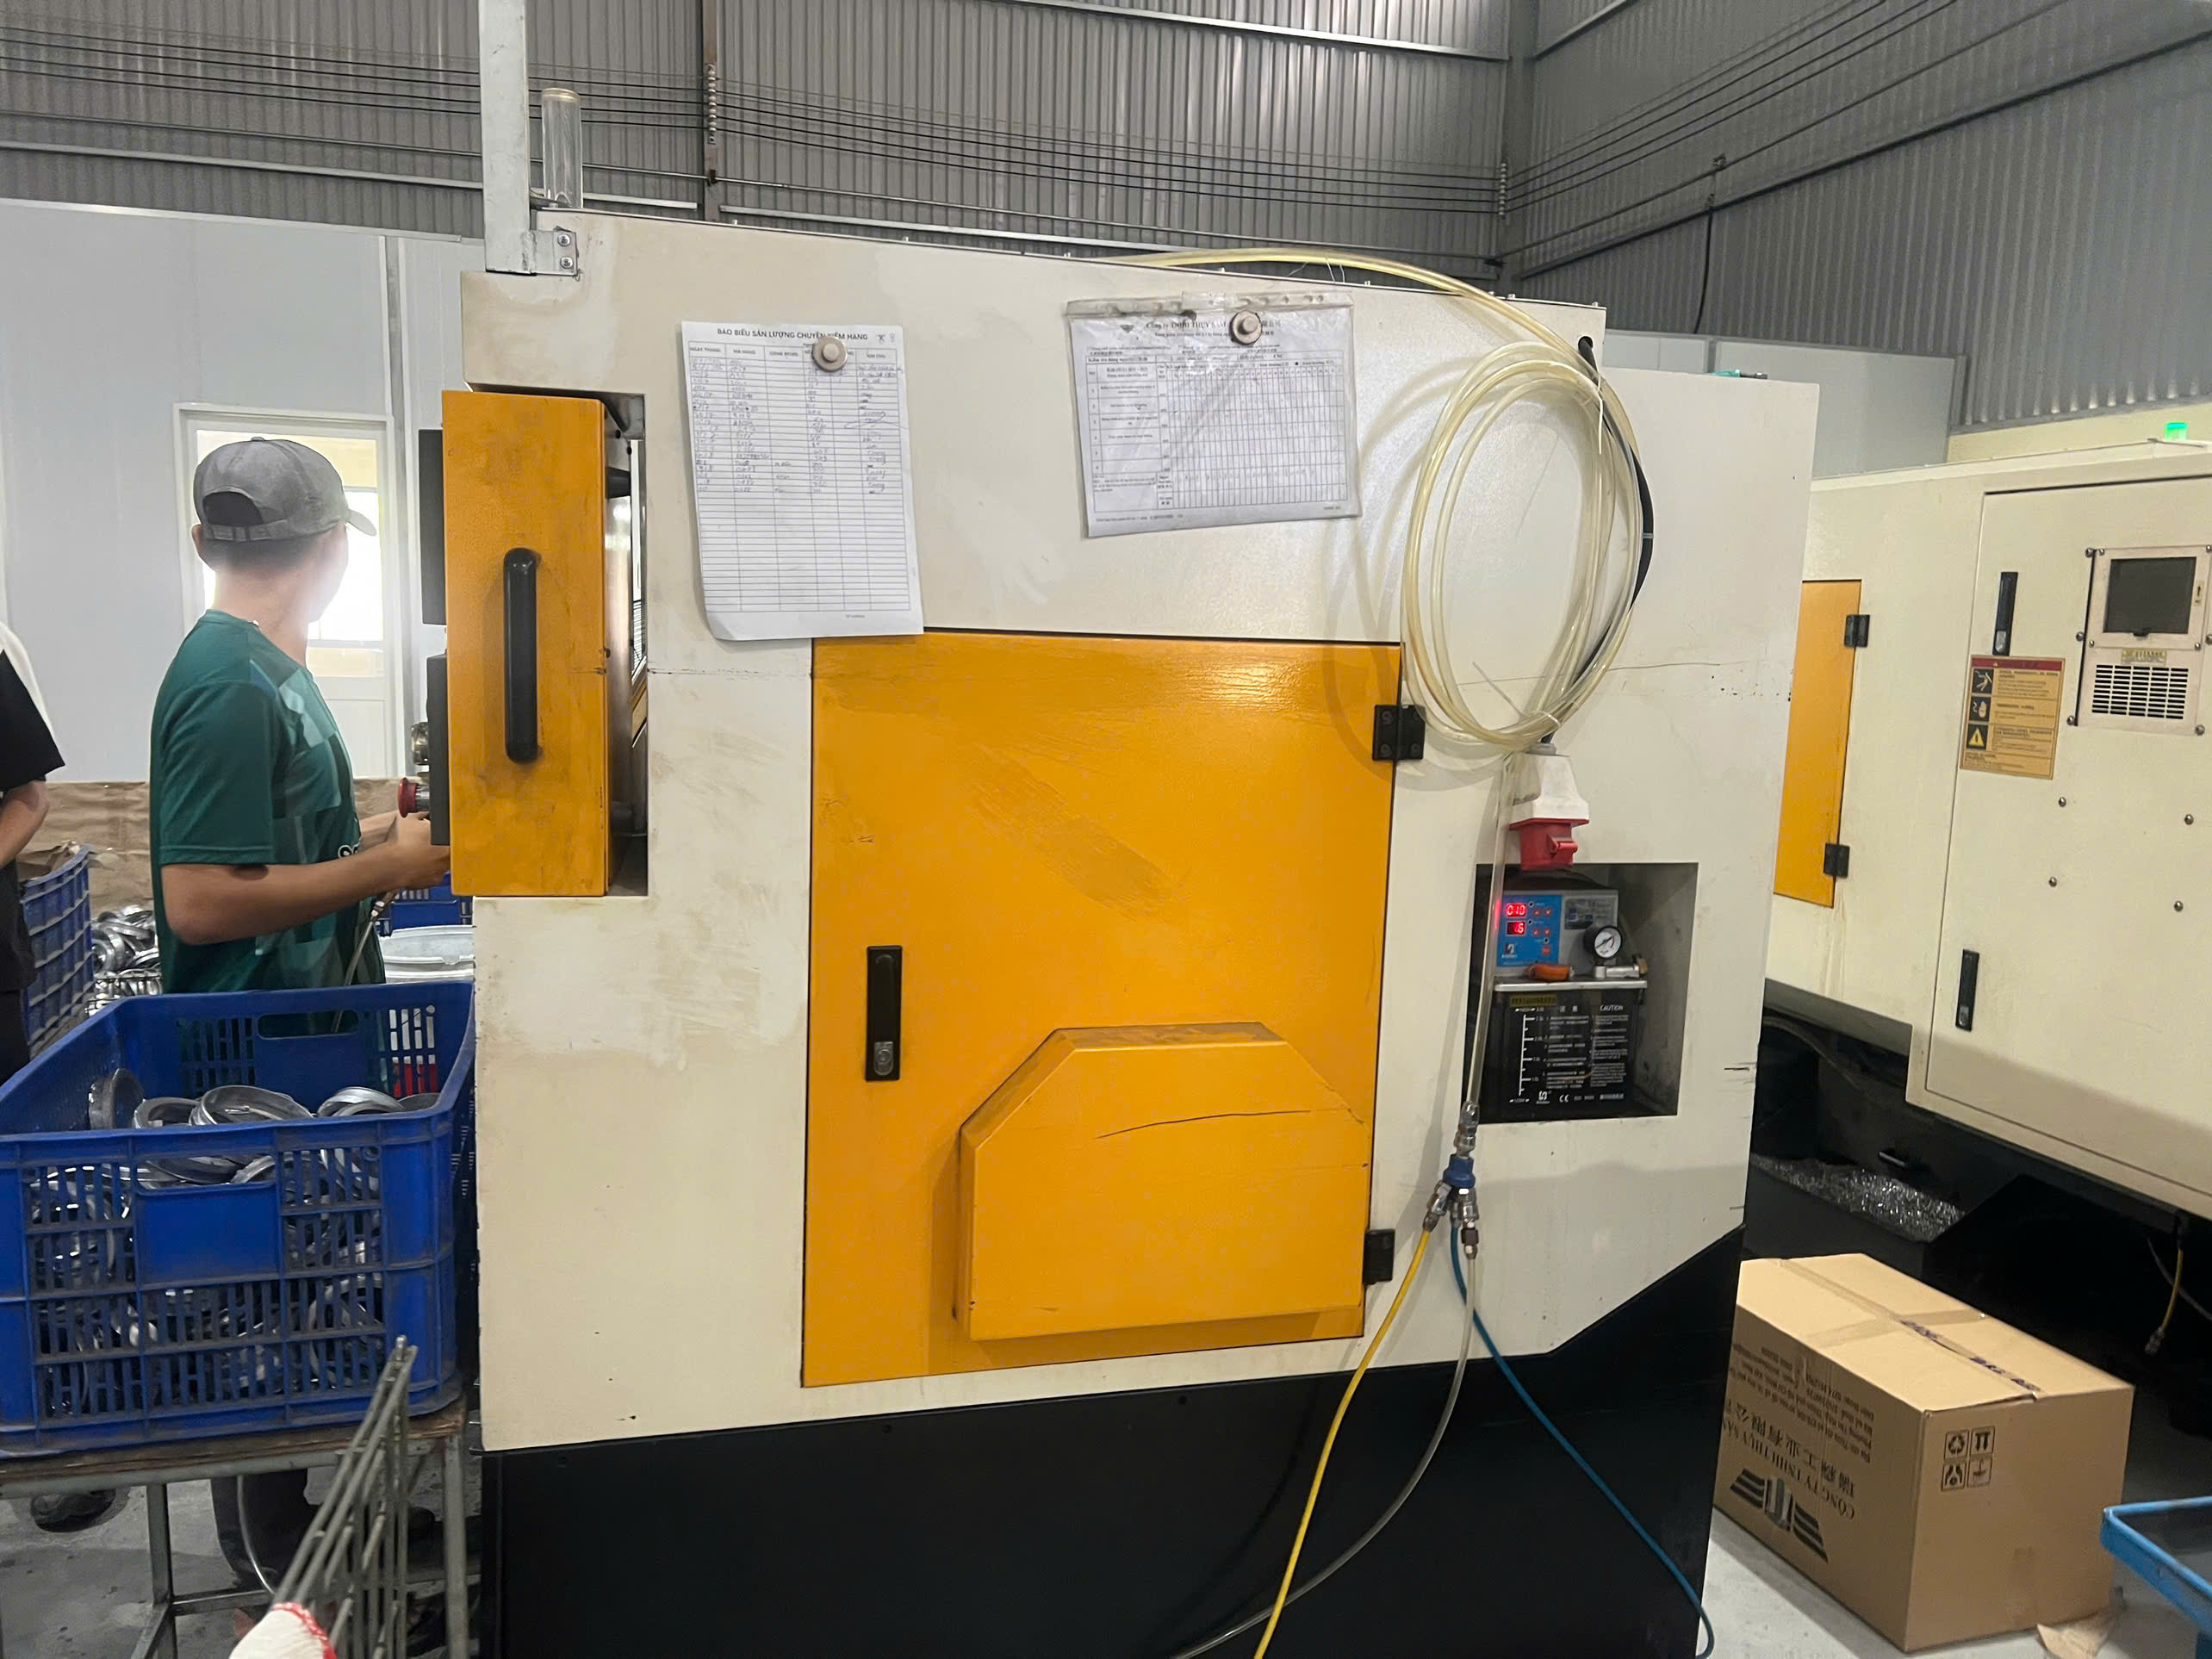
Precision driveline forging and CNC turning lines achieve internal spline pitch concentricity within ±0.008 mm for star sleeves, trunnion brackets, and core shafts. Closed-die cold and warm forging blanks undergo isothermal normalizing, 136 robotic CNC turning stations, automated hydraulic spline broaching, CQI-9 controlled carbonitriding, and 100% eddy-current crack sorting.
The manufacturing sequence for automotive drivetrain components starts with raw steel bar cutting, isothermal annealing, shot blasting, and saponification prior to 160T to 630T closed-die forging. Isothermal normalizing ensures a uniform Ferrite-Pearlite grain structure, which maintains dimensional stability during subsequent high-speed hydraulic pull broaching and CNC lathe turning.
Heat treatment utilizes automated continuous furnace carbonitriding to deliver a case hardened depth of 0.85 mm to 1.25 mm with surface hardness reaching HRC 58–62. Post-heat-treatment finishing incorporates automated raceway groove grinding, ultrasonic cleaning, 100% magnetic particle and eddy-current sorting, and vacuum anti-rust packaging to deliver serial driveline hardware.
- Closed-die forging blanks processed on 160T to 630T press lines with isothermal normalizing.
- Internal spline broaching maintaining raceway concentricity tolerances down to ±0.008 mm.
- Heat-treated carbonitriding achieving HRC 58–62 surface hardness at 0.85–1.25 mm case depth.
- Multi-station machining utilizing 136 robotic CNC lathes and German EMAG hard-turning cells.
- Automated defect sorting employing 100% eddy-current crack detection and magnetic inspection.
Which Advanced Materials and Bearing Technologies Are Available Across Partner Facilities?
Partner facilities manufacture diverse engineering materials including sintered iron and copper structural powder metallurgy, self-lubricating bimetal bushings, and high-purity fluoropolymers. Available bearing technologies range from Ø4 mm spherical plain rod ends and maintenance-free PTFE composite bushings up to Ø5,000 mm heavy-duty single and multi-row slewing bearings.
Powder metallurgy plants utilize 15T to 500T CNC automatic presses, mesh-belt sintering, and vacuum debinding lines to produce high-density transmission sprockets, shock absorber pistons, oil pump rotors, and sintered 304/316L stainless steel structural parts. Self-lubricating composite bushings incorporate SF-1/SF-2 PTFE layers, bimetal steel-bronze backings, and graphite-plugged bronze matrices for high-load applications.
For fluid handling and high-temperature environments, specialized processing covers high-purity PTFE, PFA, FEP, PVDF, and PEEK components. Multi-axis CNC machining cleanrooms and high-temperature hot-runner injection molding machines produce semiconductor wafer carriers, chemical tower internals, fluoropolymer seals, and FFKM encapsulated O-rings designed for demanding mechanical and chemical applications.
- Sintered PM parts including oil-impregnated bronze bushings, shock absorber pistons, and MIM 17-4PH components.
- Self-lubricating bearings covering PTFE composite bushings, bimetal liners, and graphite bronze bearings.
- Spherical plain bearings and hydraulic rod ends spanning Ø4 mm to Ø630 mm capacities.
- Heavy slewing rings up to Ø5,000 mm featuring single-row, double-row, and three-row roller configurations.
- High-performance fluoropolymers comprising cleanroom-machined PTFE, PFA, PEEK, and FFKM sealing elements.
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What metrology equipment is used to verify tight mechanical tolerances?
Metrology labs utilize ZEISS and Mitutoyo Crysta-Apex S 3D Coordinate Measuring Machines, contour measuring instruments, surface roughness gauges, and universal gear profile testers to verify dimensional accuracy, GD&T requirements, and raceway concentricity.
How are progressive stamping and robotic welding processes performed for structural components?
Progressive metal stamping is executed on press lines up to 315 tons, complemented by laser cutting, CNC bending, and robotic MIG/TIG welding cells. Finish options include outdoor-grade polyester powder coating withstand 240-hour salt spray exposure.
What options are available for hydraulic hand pallet truck manufacturing?
Turnkey pallet truck lines produce 2.0-ton to 5.0-ton capacity models with 550 mm or 685 mm fork widths. Features include AC/DF integrated cast-iron hydraulic pumps, 100% leak testing, polyurethane or nylon rollers, and robotic MIG welded chassis.