How do engineering teams coordinate precision cold forging and broaching workflows?
Engineering teams coordinate precision forging workflows through a 16-stage integrated process chain. Raw steel bar cutting and isothermal annealing lead into closed-die cold and warm forging, normalizing, and 136 robotic CNC turning centers. Internal spline broaching and hard grinding achieve ±0.008 mm pitch concentricity prior to automated CQI-9 carbonitriding furnace heat treatments.
Key Takeaways
- Technical supplier coordination centers in Xi'an and Ho Chi Minh City oversee DFM analysis, 100% leak testing, and ZEISS 3D CMM inspection routines.
- Automotive driveline forging achieves tolerances down to ±0.008 mm for spline raceway concentricity paired with CQI-9 heat treatments yielding HRC 58–62 hardness.
- Specialized manufacturing covers cold forging, powder metallurgy, 5-axis aerospace machining, PTFE fluoropolymers, and heavy sheet metal stamping.
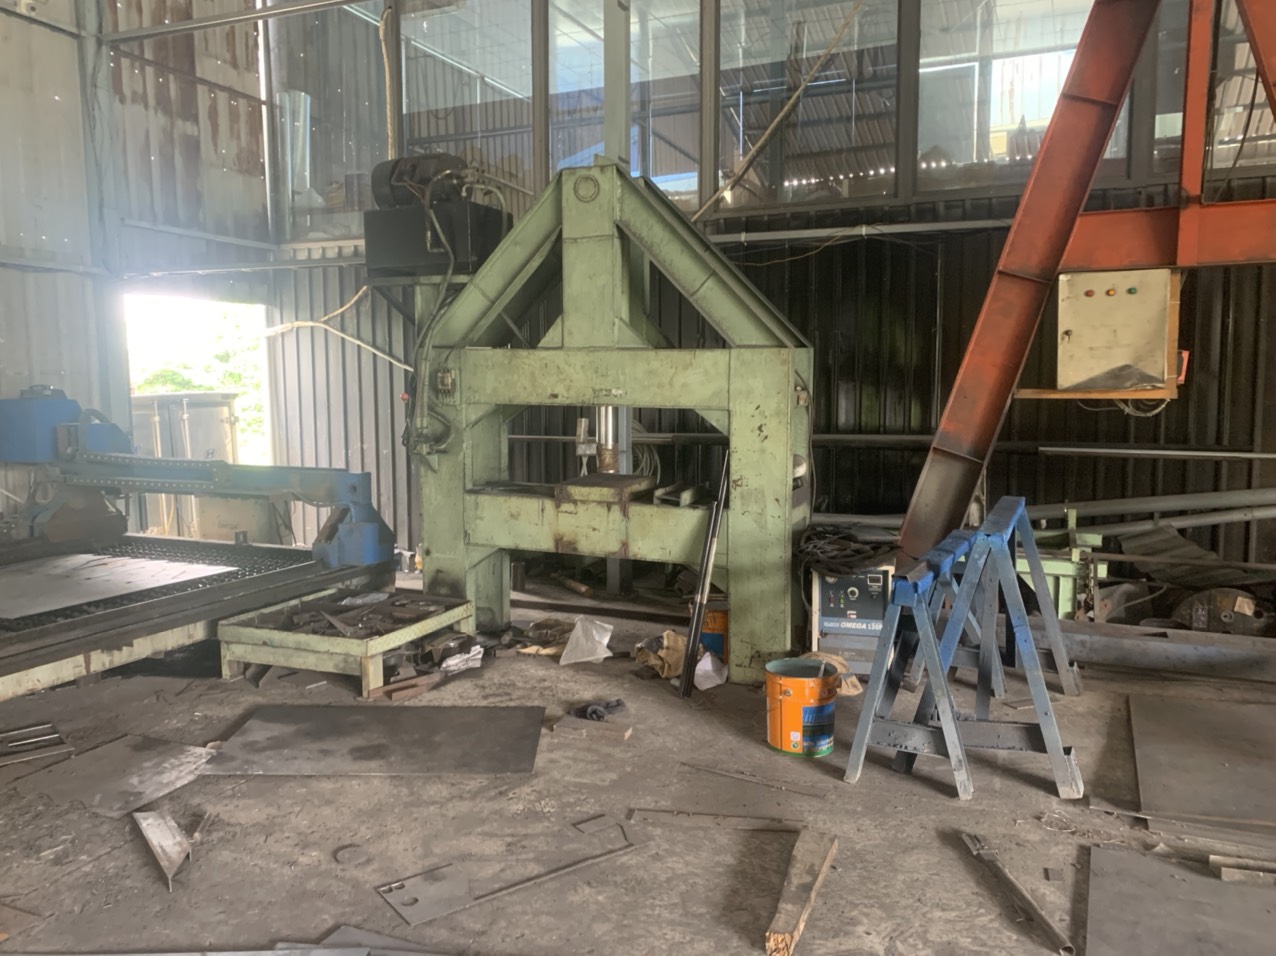
Driveline components such as CV joint star-shaped sleeves (#68-3 to #125) and TJ/AAR trunnion brackets rely on 20CrMnTi or SAE 5120H carburizing alloy steel. Closed-die forging blanks from 160T to 630T presses undergo isothermal normalizing to ensure a uniform Ferrite-Pearlite grain structure before internal splines are cut using high-speed hydraulic pull broaching.
Hard machining is performed using German EMAG hard-turning cells and automated robotic CNC lathes. Components undergo CQI-9 controlled carbonitriding and quenching to reach a case depth of 0.85 to 1.25 mm with HRC 58–62 surface hardness, verified by 100% eddy-current crack sorting and magnetic detection before ultrasonic cleaning and vacuum anti-rust packaging.
- 16-stage production flow including bar cutting, shot blasting, saponification, forging, and normalizing
- High-speed hydraulic internal spline broaching conforming to DIN 5480 and JIS B 1603 standards
- Tight tolerance control maintaining ±0.008 mm raceway concentricity on CNC turning centers
- Non-destructive eddy-current crack testing and ZEISS 3D CMM dimensional inspection routines

What capabilities define powder metallurgy and self-lubricating bearing production?
Powder metallurgy and self-lubricating bearing production utilize automatic CNC powder presses ranging from 5T to 680T, paired with continuous mesh-belt and vacuum sintering furnaces. Materials processed include SAE841 oil-impregnated bronze, 17-4PH and 316L stainless steel, bimetals, and PTFE composite linings designed for maintenance-free mechanical applications.
Sintered component manufacturing spans structural gears, shock absorber pistons, oil pump rotors, and transmission sprockets. Sintering processes utilize mesh-belt and vacuum degreasing furnaces, backed by steam treatments to enhance structural density and surface wear resistance.
Oilless and spherical plain bearing facilities produce SF-1/SF-2 PTFE composite bushings, bimetal sleeves, and graphite-plugged bronze bearings. Spherical raceways are ground on dedicated CNC lines, featuring automated PTFE fabric liner bonding and MoS2 phosphating surface treatments to sustain radial and axial loads.
- High-density metal injection molding (MIM) for complex 17-4PH and 316L stainless steel structural parts
- SAE841 and Sint B50 oil-impregnated sintered bronze bushings and soft magnetic cores
- Spherical plain bearings in GE, GEG, and GEZ series with maintenance-free PTFE liners
- Advanced metrology verification using universal gear profile testers and 3D CMM equipment
Which quality inspection protocols support heavy metal fabrication and plastics?
Quality inspection protocols for fabrication and plastics integrate multi-axis CMM metrology, 240-hour ASTM B117 salt spray testing, and cleanroom dimensional verification. Production employs 5-axis CNC machining, progressive stamping up to 315T, robotic MIG/TIG welding, and high-temperature fluoropolymer injection molding for engineered components.
Heavy stamping and structural assembly lines produce commercial hardware like fire extinguisher brackets (SPCC/SS304 steel, 2.0–4.0 mm gauge) and hand pallet trucks (2.0T to 5.0T capacity). Stamped components undergo robotic MIG welding, 5G vibration evaluations, and 1,500-hour UV powder coating. Hydraulic pump assemblies undergo 100% fluid leak testing prior to container shipment.
Precision 5-axis CNC machining and high-purity plastics processing handle ultra-demanding materials such as titanium, Inconel, PTFE, PEEK, PFA, and PVDF. Components such as semiconductor wafer carriers, chemical tower internals, and aerospace hydraulic valve blocks undergo cleanroom DI water washing and CMM inspection in temperature-controlled laboratories.
- 5-axis and 4-axis CNC machining for titanium, Inconel, and engineering plastics
- Progressive stamping presses up to 315T with integrated laser cutting and robotic welding cells
- Environmental resistance testing including 240-hour salt spray exposure and 1,500-hour UV coating tests
- Class cleanroom assembly and DI water cleaning lines for PEEK and fluoropolymer components

Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
How are line migrations executed between regional production centers?
Line transfers follow a 10-month migration playbook where progressive stamping dies, assembly fixtures, and quality inspection gauges are relocated from established plants to local hubs in Vietnam or Thailand without disrupting existing serial production schedules.
What metrology equipment is used to verify tight tolerance components?
Dimensional verification is conducted in temperature-controlled laboratories using ZEISS and Mitutoyo 3D Coordinate Measuring Machines (CMM), optical contour projectors, surface roughness analyzers, metallographic grain structure microscopes, and universal gear profile testers.
What surface treatment processes are applied to forged and stamped hardware?
Surface treatments include CQI-9 controlled carbonitriding, MoS2 phosphating, saponification, medium-frequency induction hardening, outdoor-grade polyester powder coating, and specialized steam treatments for sintered metal components.
Which material options are available for specialized engineering plastic parts?
High-purity fluoropolymers and engineering thermoplastics processed include PTFE, PEEK, PFA, FEP, PVDF, PI, PEI, PPS, and FFKM/FKM encapsulated O-rings, molded and machined in cleanroom settings.