How does structured DFM review and multi-axis CNC machining manage tight tolerances across Asian manufacturing hubs?
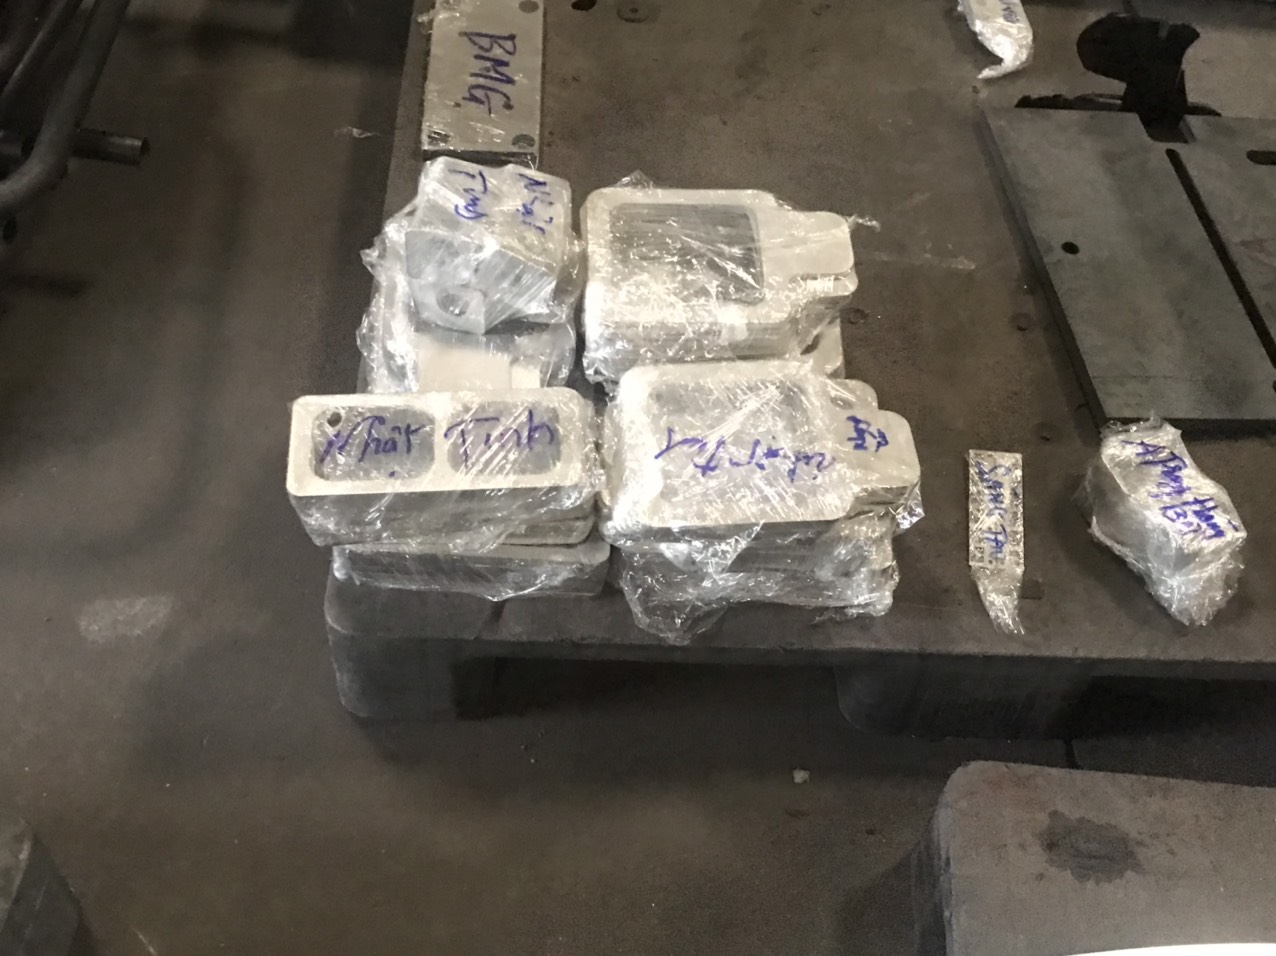
Structured design for manufacturing review uses pre-quote two-dimensional and three-dimensional tolerance analysis, progressive die modeling, and mold flow simulation before tool production. Multi-axis CNC machining centers, including aerospace-grade five-axis setups, hold tight tolerances such as plus or minus 0.008 millimeters concentricity across high-complexity titanium, aluminum, and stainless steel hardware.
Key Takeaways
- Pre-quote DFM review integrates 2D/3D tolerance analysis, progressive die design, and mold flow simulation prior to tooling production.
- Closed-loop driveline component manufacturing relies on a 16-stage process flow including warm forging, spline broaching, EMAG hard turning, and CQI-9 carbonitriding.
- Metrology and quality control utilize ZEISS and Mitutoyo 3D CMM systems, eddy-current crack testing, and metallographic density analysis to support 50 PPM targets.
Engineering coordination across multi-city hubs—including Xi'an, Ningbo, Wenzhou, and Jiangmen in China, along with Hanoi, Bac Ninh, Haiphong, and Ho Chi Minh City in Vietnam—requires rigorous DFM validation before cutting steel. Pre-quote engineering reviews evaluate 2D GD&T blueprints and 3D CAD models to resolve geometric discrepancies, optimize tool paths, and verify mold flow dynamics.
Advanced machining cells feature 5-axis and 4-axis CNC machining centers, turn-mill compounds, and precision slow-wire EDM. Specialized facilities operating under AS9100D aerospace quality management standards process ultra-precision titanium, Inconel, stainless steel, and aluminum components such as hydraulic valve blocks, optical mounts, and electro-mechanical housings.
- AS9100D aerospace 5-axis CNC machining for titanium, Inconel, and aluminum housings
- 136 robotic CNC lathes paired with 4 German EMAG hard-turning cells
- Pre-quote 2D/3D tolerance analysis, progressive die design, and mold flow simulation
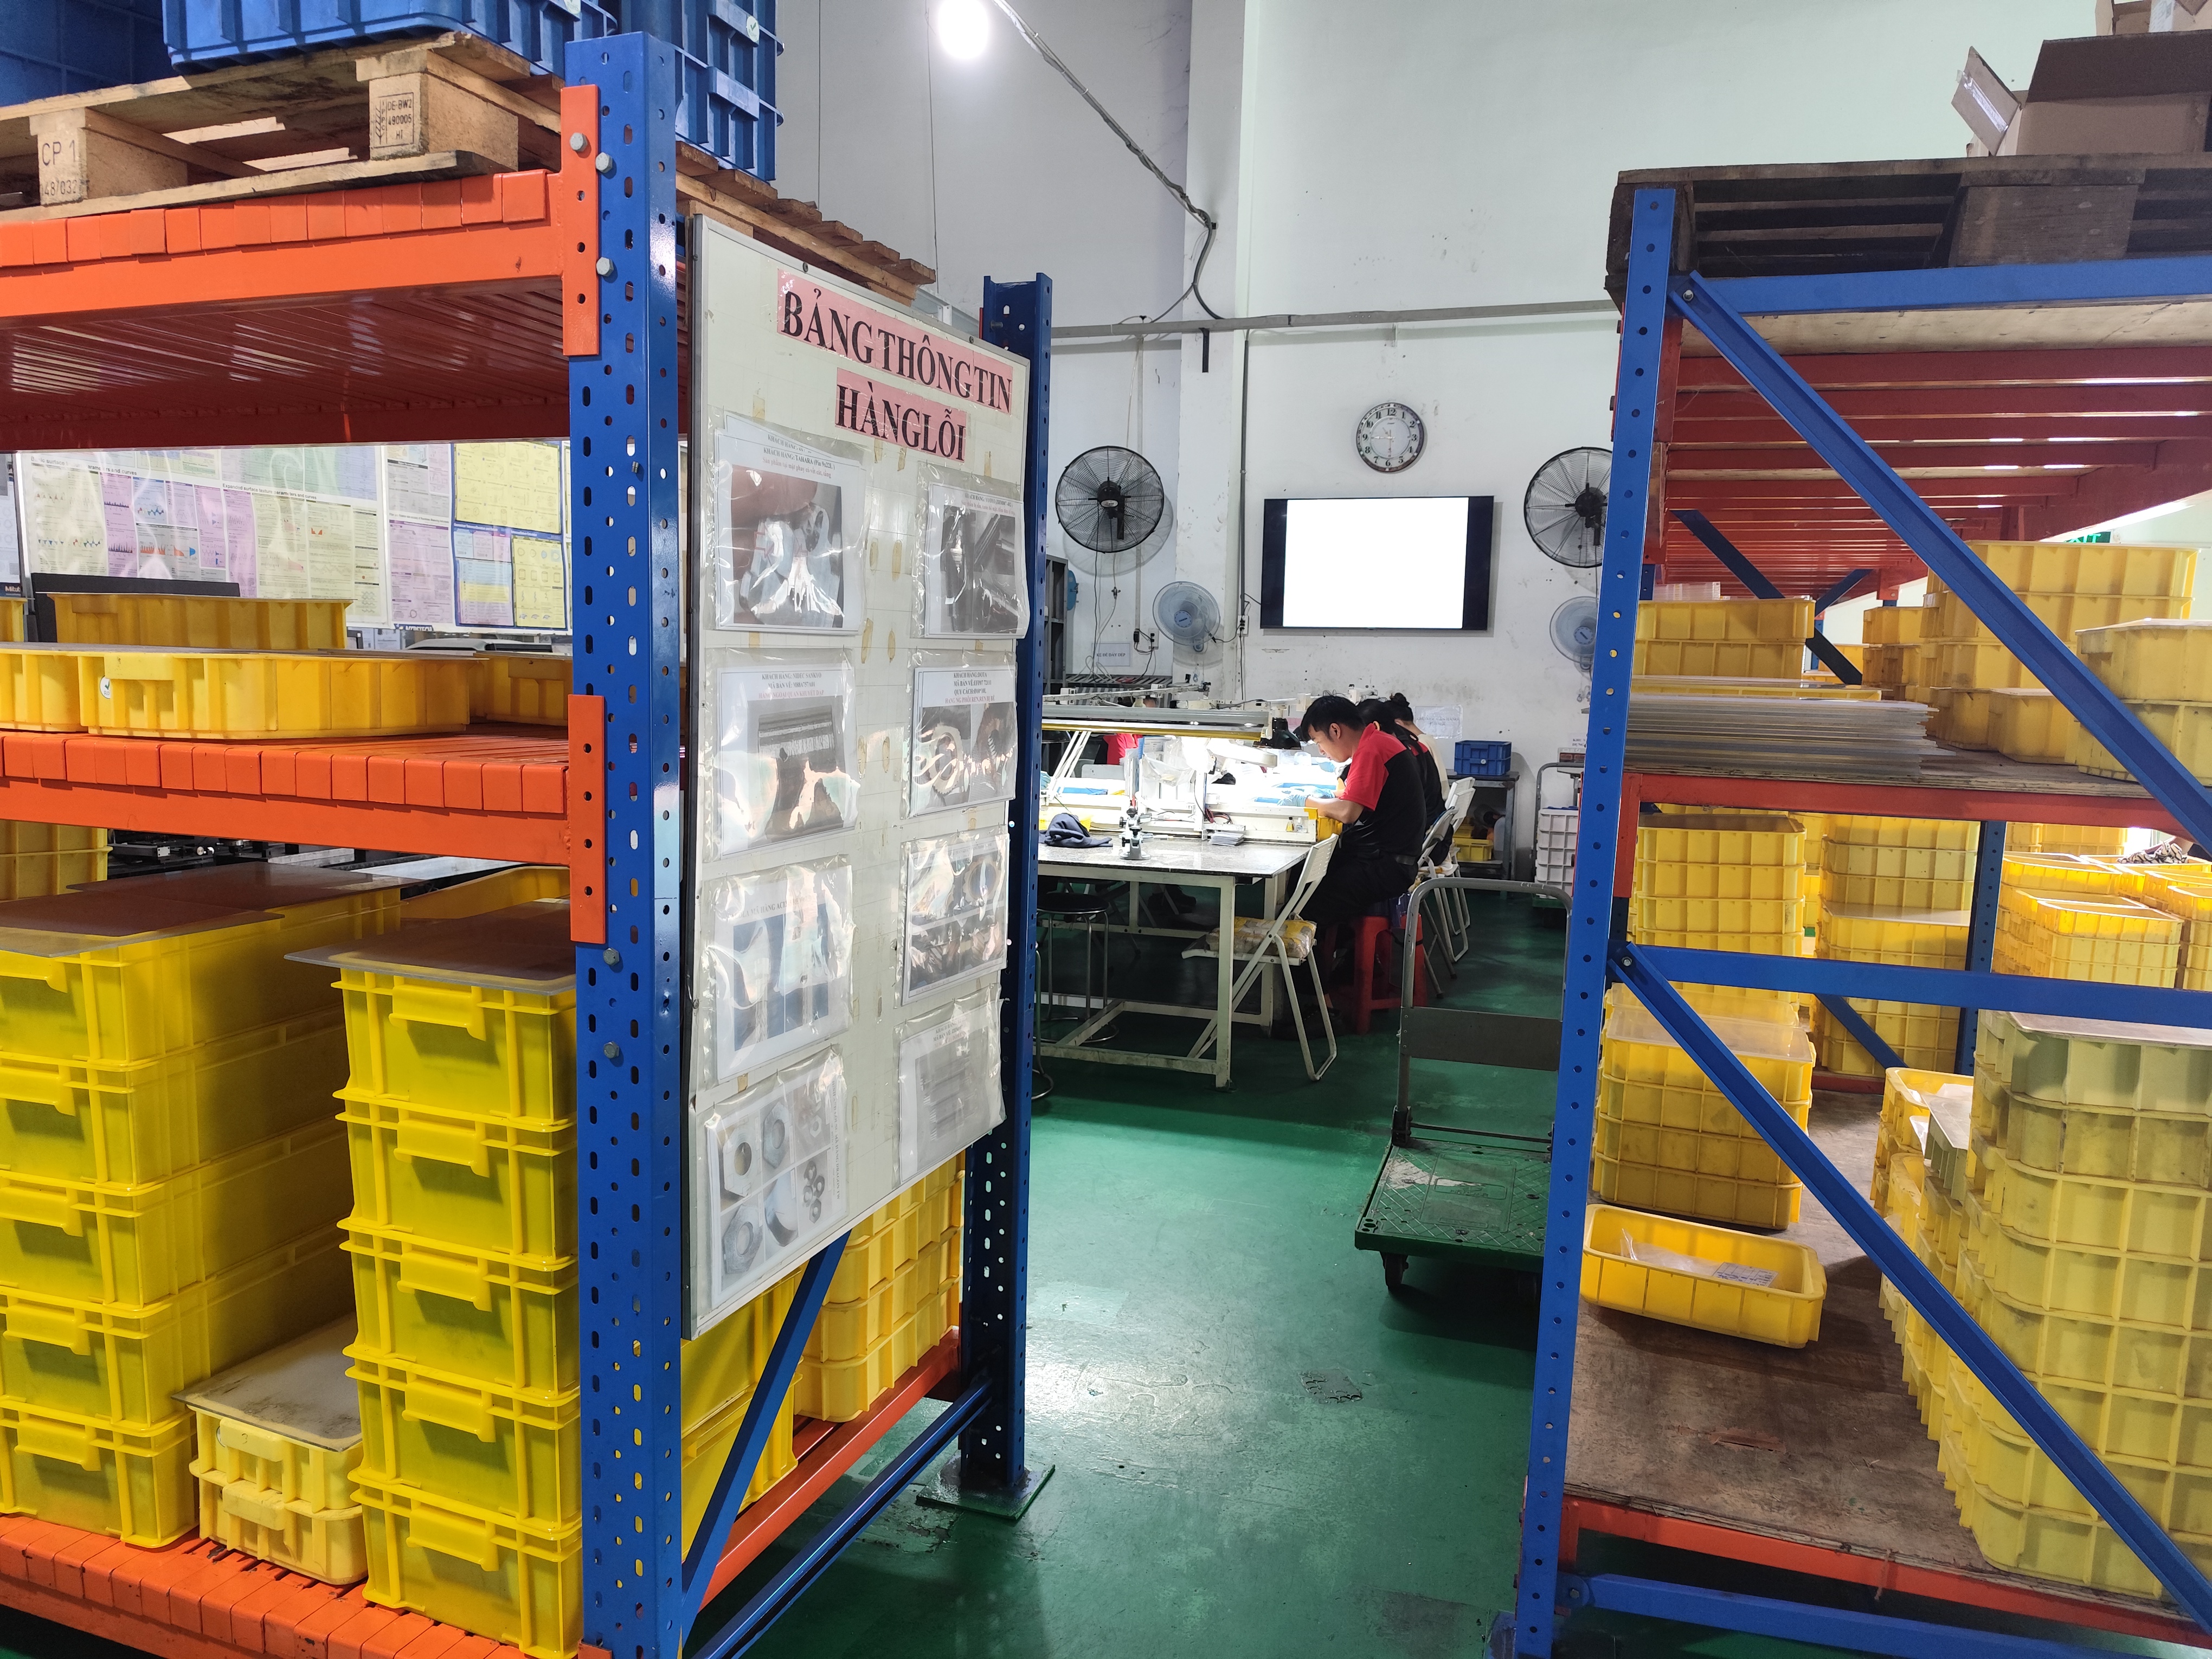
- Temperature-controlled metrology labs using ZEISS and Hexagon 3D coordinate measuring machines
What processes and metrology controls ensure precision in automotive forging and spline broaching?
Precision automotive driveline manufacturing relies on a sixteen-stage closed-loop process flow. Raw steel bars undergo isothermal annealing, shot blasting, saponification, cold or warm forging, and controlled normalizing. High-speed hydraulic pull broaching, robotic CNC turning, EMAG hard turning, and automated groove grinding achieve tight spline pitch precision before CQI-9 carbonitriding and magnetic crack inspection.
High-volume driveline production, such as CV joint star-shaped sleeves (#68-3 to #125) and trunnion brackets, uses 160T to 630T closed-die forging presses. Isothermal normalizing establishes a uniform Ferrite-Pearlite grain structure, ensuring stable dimensions during high-speed internal spline broaching and CNC turning.
Processed components made from 20CrMnTi or SAE 5120H carburizing alloy steel achieve case depths of 0.85 to 1.25 mm with surface hardness of HRC 58–62 after automated carbonitriding. Quality control protocols enforce 100% eddy-current crack detection, magnetic crack inspection, surface roughness profiling, and ultrasonic cleaning prior to anti-rust vacuum packaging.
- 16-stage in-house production flow from raw steel bar cutting to vacuum anti-rust packaging
- Closed-die warm and cold forging using 160T to 630T press capacities with controlled normalizing
- High-speed hydraulic pull broaching meeting DIN 5480 and JIS B 1603 internal spline standards
- Raceway concentricity and spline pitch maintained within ±0.008 mm tolerances
Which inspection steps and material standards govern powder metallurgy and bearing production?
Powder metallurgy and self-lubricating bearing production use automatic CNC presses from fifteen to five hundred tons, mesh-belt sintering, and steam treatment. Verification steps include metallographic density analysis, universal gear testing, continuous tribology testing, contour labs, and temperature-controlled ZEISS three-dimensional coordinate measuring machines to verify gear profiles and raceway geometries.
Powder metallurgy (PM) and metal injection molding (MIM) produce high-density structural gears, transmission sprockets, shock absorber pistons, and vacuum-sintered 304/316L stainless steel parts. Pressing systems ranging from 15T to 500T CNC automatic presses operate alongside catalytic debinding lines and mesh-belt sintering furnaces.
Bearing manufacturing covers SF-1 and SF-2 PTFE composite bushings, JF-800 bimetal bearings, JDB graphite-plugged bronze bearings, and Ø200–5,000 mm single and double-row four-point contact ball slewing bearings. Precision spherical plain bearings utilize automated PTFE fabric liner bonding and MoS2 phosphating lines, backed by radial and axial static load fatigue testing.
- Sintered PM structural components including SAE841 / Sint B50 oil-impregnated bronze bushings
- Metal Injection Molding (MIM) for complex 17-4PH and 316L stainless steel hardware
- Publicly listed bearing production yielding SF-1/SF-2 composite and bimetal self-lubricating bushings
- Spherical plain bearings (Ø4–630 mm) evaluated on static load fatigue and tribology test rigs

Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
How do regional engineering teams perform quality control and factory audits across Asian production facilities?
Engineering teams located in Xi'an, China (26 staff) and Ho Chi Minh City, Vietnam (7 staff) manage QCLDM factory audits, resident supplier quality engineering reviews, full PPAP Level 3 documentation, ZEISS CMM dimensional inspection, and material certificates of analysis.
What dimensional tolerances and surface treatments are achieved during CV joint star sleeve and spline shaft production?
Forged 20CrMnTi and SAE 5120H carburizing alloy steel components achieve spline pitch concentricity of ±0.008 mm, DIN 5480 or JIS B 1603 spline modules, case depth of 0.85 to 1.25 mm, and HRC 58–62 hardness via CQI-9 controlled carbonitriding.
What manufacturing equipment is used for high-volume powder metallurgy and MIM structural components?
Production facilities utilize 15T to 500T CNC automatic powder presses, 680T hydraulic presses, mesh-belt and vacuum debinding-sintering furnaces, and steam treatment equipment to fabricate iron, copper, and 304/316L stainless steel parts.
Which verification tests are applied to heavy-duty welded assemblies and finished industrial hardware?
Welded progressive stamping assemblies, hydraulic pallet trucks, and mounting brackets undergo 100% hydraulic pump leak testing, 240-hour plus ASTM B117 salt spray exposure, 1,500-hour UV powder coat testing, and cyclic load testing.