
How is precision metrology integrated into multi-stage component production?
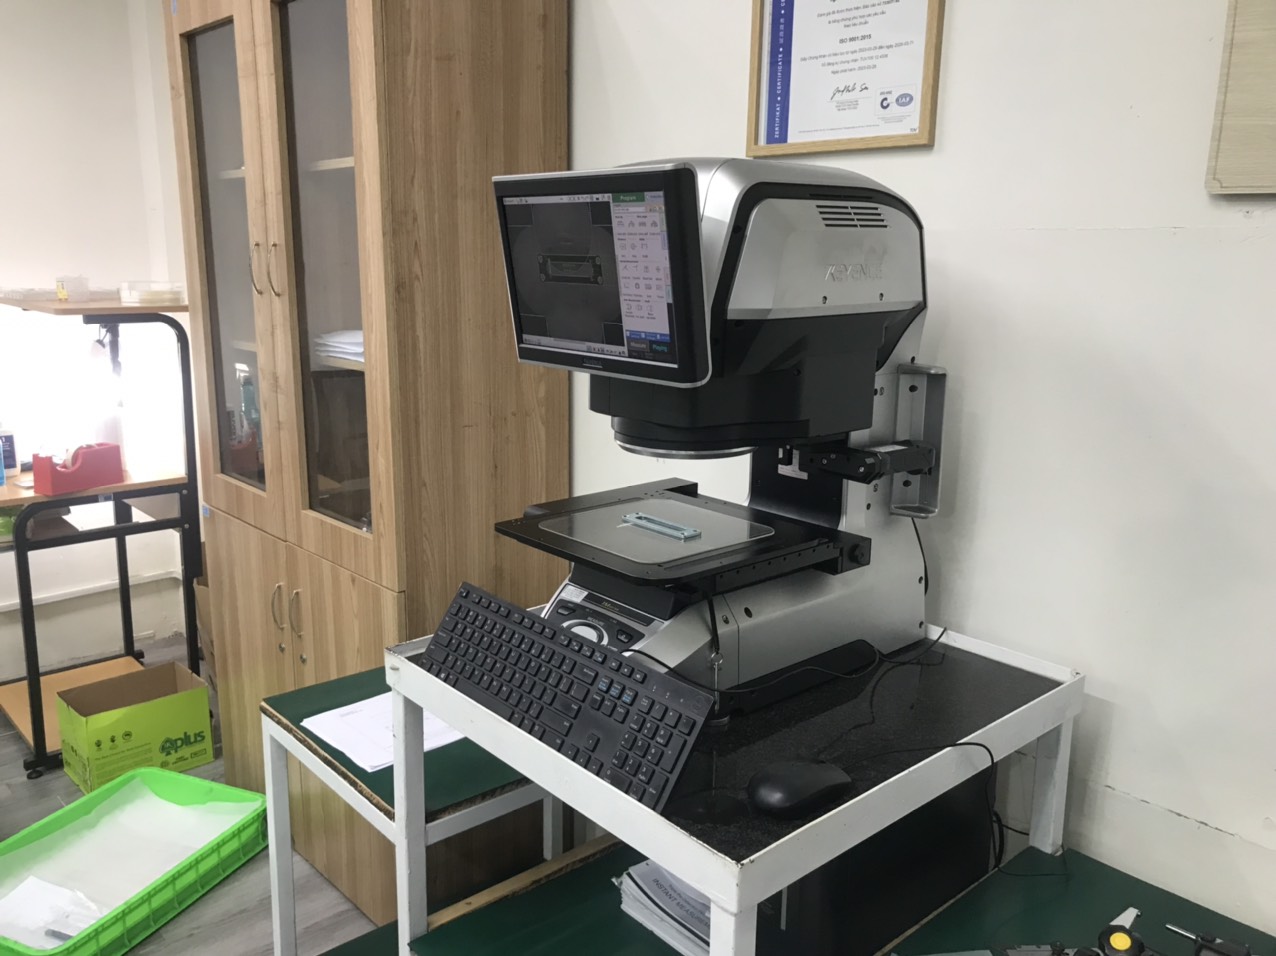
Metrology integration combines dimensional verification using ZEISS and Mitutoyo 3D coordinate measuring machines with specialized testing on the shop floor. Inspection protocols include contour measuring, surface roughness checks, metallographic microstructure evaluation, eddy-current crack sorting, and 100% leak testing for hydraulic pump assemblies across Asian manufacturing hubs.
Key Takeaways
- Multi-regional engineering coordination spans Singapore HQ, a 26-person team in Xi'an, China, and an 11-person local engineering group in Ho Chi Minh City, Vietnam, expanding to Thailand in 2027.
- Driveline component fabrication uses 16-stage closed-loop processing including 20CrMnTi/SAE 5120H forging, hydraulic spline broaching holding ±0.008 mm pitch tolerance, and CQI-9 heat treatment.
- Metrology inspection incorporates ZEISS and Mitutoyo 3D CMM dimensional verification, eddy-current crack sorting, and metallographic density analysis for precision parts.
Coordinate measuring machines from ZEISS and Mitutoyo provide dimensional verification for critical features across multi-axis machining and forging workflows. Inspection routines in specialized labs evaluate contour geometry, surface roughness, and metallographic grain structures to confirm component integrity before serial assembly.
In addition to CMM metrology, automated inspection steps are implemented directly within production lines. Hydraulic pump assemblies undergo 100 percent leak checks, while drive components pass through automated eddy-current and magnetic particle crack sorting stations.
- ZEISS and Mitutoyo Crysta-Apex S 3D CMM metrology for 3D coordinate inspection
- Surface roughness, contour analysis, and metallographic microstructure verification
- Automated eddy-current and magnetic crack sorting for heat-treated forgings
- 100% hydraulic leak testing on cast-iron pump assemblies
What manufacturing processes control complex automotive drivetrain production?
Driveline component manufacturing utilizes a 16-stage vertically integrated workflow combining raw steel bar cutting, precision cold or warm forging, isothermal normalizing, robotic CNC turning, internal spline broaching, automated groove grinding, and CQI-9 controlled carbonitriding. This process sequence maintains tight dimensional tolerances for star sleeves, trunnion brackets, and core shafts.
Automotive driveline manufacturing relies on sequential closed-loop processing to produce components such as star-shaped inner races, trunnion brackets, and forged core shafts. Starting from raw steel bar cutting, materials undergo isothermal annealing, shot blasting, and surface saponification prior to precision cold or warm forging.
Following closed-die forging, parts pass through controlled normalizing, 136 robotic CNC turning setups, 4 German EMAG hard-turning centers, and high-speed hydraulic spline broaching. Final operations apply CQI-9 controlled carbonitriding furnace cycles to achieve case hardness values between HRC 58 and 62.
- ±0.008 mm spline pitch raceway concentricity on hydraulic pull broaches
- HRC 58–62 case hardness with 0.85 to 1.25 mm case depth via CQI-9 carbonitriding
- 20CrMnTi and SAE 5120H carburizing alloy steel material processing
- Spline module standards adhering to DIN 5480 and JIS B 1603 specifications
Which material and tooling options support specialized industrial components?
Material capabilities encompass carburizing alloy steel 20CrMnTi, sintered 304 and 316L stainless steels, titanium, Inconel, engineering fluoropolymers like PTFE and PEEK, and bimetal composites. Tooling options include progressive stamping dies up to 315 tons, 5-axis CNC machining centers, and powder metallurgy presses ranging from 15 to 500 tons.
Precision hardware production utilizes dedicated material formulations and processing equipment customized to component geometry. Powder metallurgy facilities utilize 15 to 500-ton CNC automatic powder presses, mesh-belt sintering furnaces, and catalytic debinding lines for metal injection molding of complex stainless steel and iron structural parts.
Aerospace-grade machining centers employ 5-axis CNC milling, turn-mill centers, and slow-wire EDM to process titanium, Inconel, and aluminum alloys. For bearing applications, continuous bronze-powder sintering strip lines and automated CNC boring lines produce self-lubricating PTFE composite bushings and bimetal bearings.
- Powder metallurgy structural parts: SAE841 bronze, 304/316L stainless steel, and iron alloys
- Aerospace 5-axis CNC machining: titanium, Inconel, aluminum, and stainless steel valve blocks
- Fluoropolymer components: high-purity PTFE, PEEK, PFA, FEP, PVDF, and FFKM seals
- Heavy stamping and welding: progressive presses up to 315T with robotic MIG/TIG welding cells
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What quality management standards and inspection equipment are used for powder metallurgy and bearing production?
Production facilities utilize quality frameworks including IATF 16949:2016, ISO 9001:2015, and AS9100D. Inspection equipment includes ZEISS 3D CMMs, universal gear testers, tribology laboratory rigs, and gear profile meters to evaluate density, dimensions, and surface finishes.
How are drive shafts, spline sleeves, and trunnion brackets heat treated?
Components undergo CQI-9 controlled continuous furnace carbonitriding followed by quenching. This process generates a hard exterior case depth of 0.85 to 1.25 mm with surface hardness from HRC 58 to 62, verified through 100 percent eddy-current sorting.
What production capacity exists for heavy stamping, laser cutting, and robotic welding?
Stamping operations feature up to 33 presses with capacities reaching 315 tons, complemented by laser cutting machinery, 22 robotic CNC milling setups, and 9 Panasonic or OTC MIG/TIG welding robots capable of high-volume sheet metal assemblies.
How is engineering coordination managed across multiple Asian manufacturing locations?
Coordination is maintained through a Singapore headquarters, a 26-person engineering service center in Xi'an, China, and an 11-person local engineering team in Ho Chi Minh City, Vietnam, extending coverage to Thailand facilities.