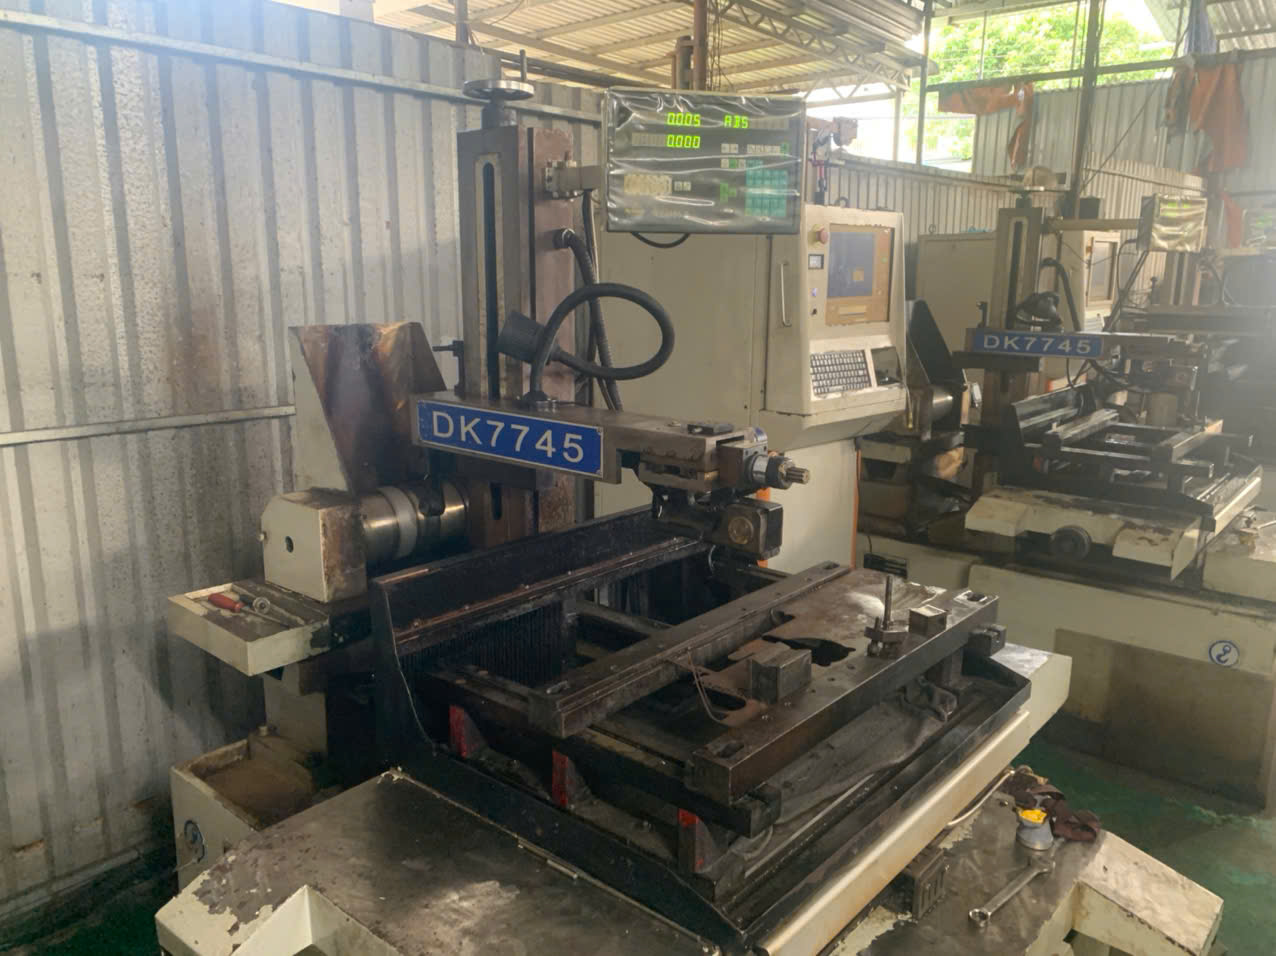
How does pre-quote DFM review prevent precision machining and tooling defects?
Pre-quote Design for Manufacturability (DFM) reviews utilize 2D and 3D tolerance analysis, progressive die design, and mold flow simulation before tool steel is cut. Managed by engineering teams in Xi'an, China, these evaluations establish 50 PPM quality controls, full PPAP Level 3 documentation, and ZEISS 3D coordinate measuring machine (CMM) verification across specialized Asian manufacturing centers.
Key Takeaways
- Dolphin Services manages pre-quote DFM tolerance analysis, supplier audits, and in-process ZEISS CMM dimensional inspection across 26 engineers in Xi'an, China and 7 local staff in Vietnam.
- Driveline components like CV joint star-shaped sleeves utilize 20CrMnTi/SAE 5120H steel, closed-die forging, internal spline broaching, and CQI-9 controlled carbonitriding to achieve HRC 58 to 62 hardness and plus-minus 0.008 mm concentricity.
- Multi-country Asian manufacturing networks support specialized processes including 15 to 500T powder metallurgy pressing, 5-axis micro-machining, 5-meter slewing bearings, and high-purity PEEK and PTFE fluoropolymer molding.
DEWIN's Xi'an service center houses 26 engineering and quality specialists who orchestrate DFM evaluations across primary manufacturing hubs in Zhejiang, Jiangsu, Guangdong, Shandong, and Henan. Pre-production analysis includes checking geometrical dimensioning and tolerancing (GD&T) against production line capability to confirm tolerances before initiating tooling fabrication.
For high-precision projects, engineering teams conduct metallographic density verification and CMM dimensional profiling to ensure compliance with technical specifications. Supplier quality engineers perform resident audits and monitor in-process controls to maintain target quality standards across high-volume assembly lines.
- Pre-quote 2D DWG blueprint intake and GD&T tolerance analysis
- Progressive die design and mold flow computer simulations
- PPAP Level 3 submission with ZEISS 3D CMM metrology inspection documentation
- Material certificates of analysis (COA) and metallographic microstructure testing
- 50 PPM defect benchmarking backed by resident supplier quality engineering audits
What manufacturing steps ensure precision internal spline broaching and heat treatment quality?
Precision internal spline broaching relies on a 16-stage integrated flow beginning with raw 20CrMnTi steel bar cutting, closed-die forging, and isothermal normalizing. High-speed hydraulic pull broaching and 136 robotic CNC lathes hold ±0.008 mm raceway concentricity, followed by CQI-9 controlled carbonitriding furnaces to yield HRC 58–62 hardness and eddy-current crack sorting.
Production of CV joint star-shaped sleeves (#68-3 to #125) and TJ/AAR trunnion brackets at the Ningbo Keminsheng facility follows a strict multi-stage metallurgical process flow. Steel bars undergo cold or warm precision forging across 160T to 630T closed-die presses, paired with controlled normalizing to establish uniform Ferrite-Pearlite grain structure before machining.
Final dimensional accuracy is achieved through 136 robotic CNC turning centers and 4 German EMAG hard-turning cells. Machined parts pass through internal spline broaching to meet DIN 5480 or JIS B 1603 module standards, before entering automated continuous carbonitriding furnaces to secure a 0.85 to 1.25 mm case depth.
- Raw steel bar cutting, isothermal annealing, shot blasting, and saponification
- Closed-die precision cold and warm forging (160T–630T presses) with controlled normalizing
- Robotic CNC turning across 136 lathes and 4 German EMAG hard-turning cells
- High-speed hydraulic internal spline broaching meeting DIN 5480 / JIS B 1603 specifications
- CQI-9 controlled carbonitriding furnace quenching achieving HRC 58–62 case hardness
- Post-heat treatment eddy-current crack sorting, magnetic inspection, and ultrasonic cleaning
Which specialized manufacturing processes are available across audited Asian facilities?
Audited Asian facilities provide specialized manufacturing across powder metallurgy, slewing bearings, fluoropolymers, aerospace 5-axis CNC machining, and heavy sheet metal stamping. Capabilities range from 15–500T automatic powder presses and 5m vertical turning centers to cleanroom-molded PEEK components and 315T progressive stamping presses with OTC and Panasonic welding robotics.
The audited Asian supplier network covers diverse technical materials and processes. Companies such as Jiande Welfine Technology and Shaoxing Guoteng Auto Parts operate 5 to 500-ton CNC powder presses, vacuum sintering furnaces, and mesh-belt steam treatment for automotive transmission sprockets, structural gears, and SAE841 oil-impregnated bronze bushings.
For heavy machinery and fluid control, Xuzhou Wanda Slewing Bearing manufactures Ø200 to 5,000 mm four-point contact ball and crossed-roller bearings using 5m CNC vertical turning centers. Zhenjiang RunFun Engineering Plastics delivers cleanroom DI-water washed PTFE, PFA, and PEEK semiconductor components, while Hangtuo Mechanical Technology provides AS9100D aerospace 5-axis machining for titanium and Inconel valve blocks.
- Powder Metallurgy & MIM: 15–500T CNC powder presses, 17-4PH/316L stainless steel injection molding, and vacuum sintering
- Slewing Bearings: Ø200–5,000 mm contact ball/roller slewing rings with medium-frequency induction hardening
- Aerospace 5-Axis CNC: Multi-axis machining and slow-wire EDM for titanium, Inconel, and aluminum valve housings
- Oilless & Spherical Bearings: SF-1/SF-2 PTFE composite bushings, JDB graphite bronze, and spherical plain bearings
- Engineering Plastics: Cleanroom injection molding and multi-axis CNC of high-purity PTFE, PFA, PEEK, and FFKM seals
- Heavy Stamping & Robotic Welding: Progressive stamping presses up to 315T with OTC/Panasonic robotic MIG welding cells
How is production line relocation managed between China and Vietnam?
Production line relocation is executed through a 10-month China-to-Vietnam migration playbook that transfers progressive stamping dies, assembly fixtures, and quality control gauges without interrupting supply chains. Local Vietnamese engineering teams in Ho Chi Minh City and Bac Ninh coordinate factory setup, robotic welding cells, and pre-shipment container loading audits.
Transferring hardware production between Asian manufacturing centers requires rigorous logistical and quality coordination. DEWIN's 7-person team in Ho Chi Minh City directly oversees local plant operations across Bac Ninh, Hanoi, Haiphong, Binh Duong, and Dong Nai. The team manages substantial transformation compliance for regional supply chains.
Dedicated product lines in Vietnam include European-standard 2.0T to 5.0T hydraulic hand pallet trucks produced in a 16,000 m² Bac Ninh plant featuring AC/DF integrated cast pumps and 100% leak testing. In addition, progressive stamping facilities manufacture SPCC and SS304 fire extinguisher brackets rated for 5G vibration environments with 240-hour ASTM B117 salt spray resistance.
- 10-month migration playbook for transferring dies, fixtures, and QC inspection gauges
- On-the-ground engineering oversight by 7 local staff in Ho Chi Minh City and Bac Ninh
- Direct access to Lach Huyen deep-water container terminal in Haiphong for trans-Pacific shipping
- Dedicated 16,000 m² Vietnam plant for CE hydraulic hand pallet trucks with 100% pump leak testing
- Progressive sheet metal stamping for UL 711 / DOT fire extinguisher brackets with 1,500-hour UV powder coating
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What metrology equipment is used for dimensional verification of machined components?
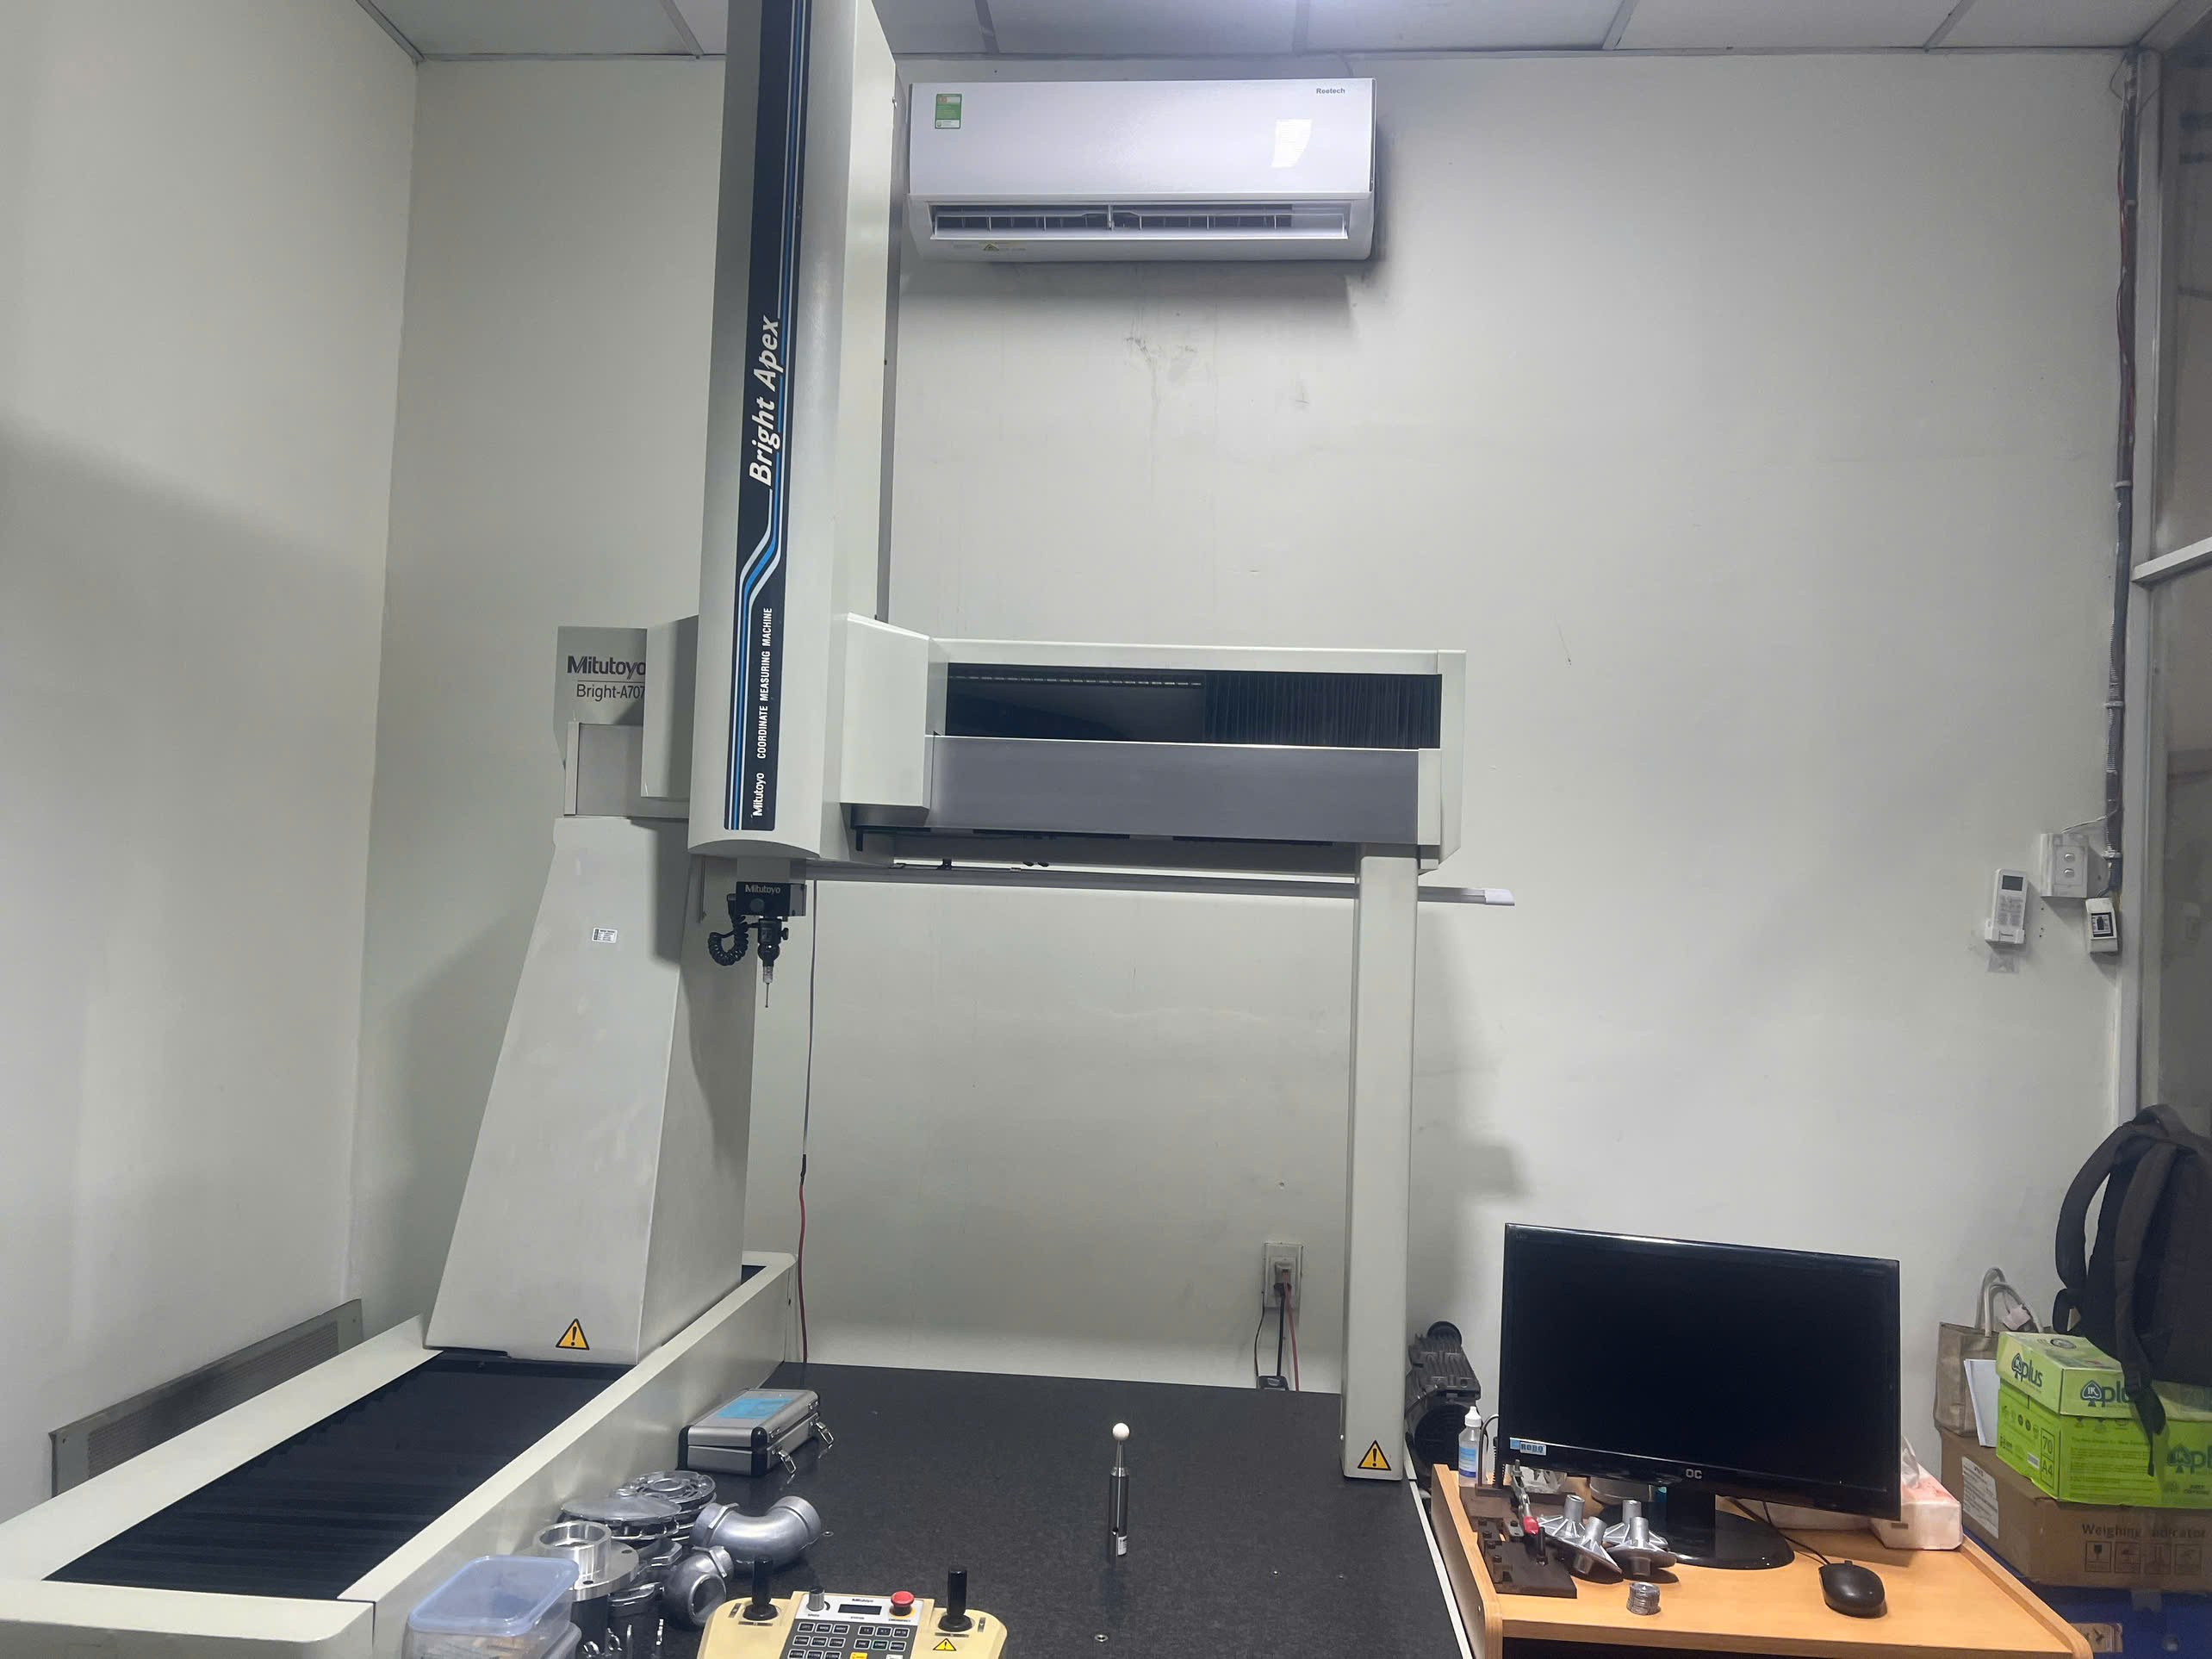
Quality control laboratories utilize ZEISS 3D Coordinate Measuring Machines (CMM), Mitutoyo Crysta-Apex S metrology systems, contour measuring tools, surface roughness meters, and metallographic microstructure testing equipment.
Which raw steel grades are utilized for forged automotive driveline parts?
Driveline components such as CV joint star sleeves and core shafts are manufactured from 20CrMnTi and SAE 5120H carburizing alloy steel, subjected to isothermal annealing and normalizing prior to machining.
What production capacity exists for powder metallurgy structural components?
Audited powder metallurgy facilities operate automatic CNC powder presses ranging from 15T to 680T, outputting over 150 million structural iron, copper, and stainless steel parts annually across vacuum sintering and debinding lines.
How are hydraulic pumps tested in the Vietnam hand pallet truck manufacturing hub?
At the 16,000 m² Bac Ninh facility, every AC/DF integrated cast-iron hydraulic pump undergoes 100% pressure leak testing before assembly onto 2.0T to 5.0T capacity hand pallet truck frames.