How do procurement teams coordinate multi-country production across Asian manufacturing hubs?
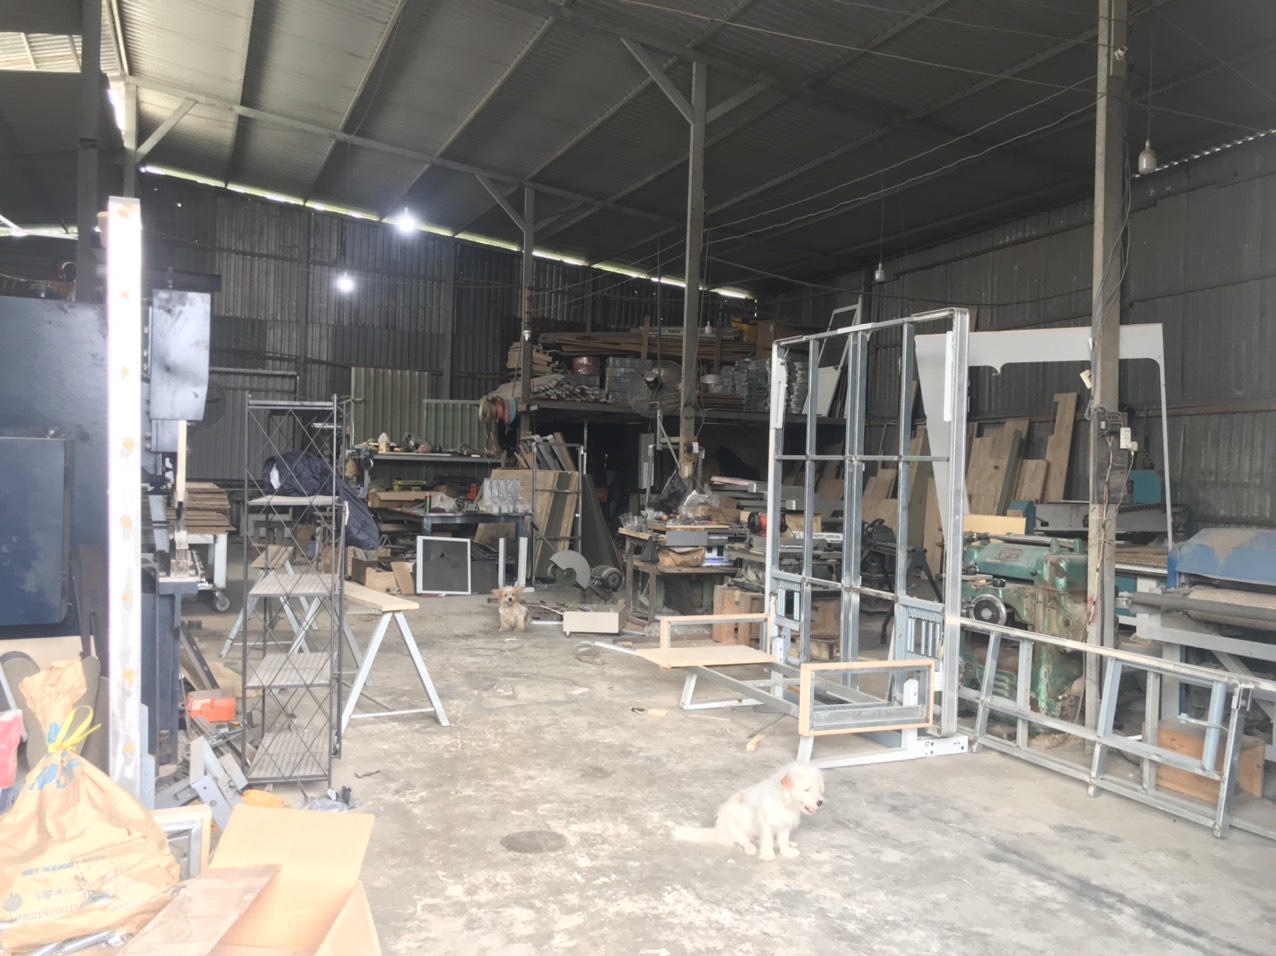
Procurement teams coordinate multi-country production across Asia by managing engineering review, supplier scoring on Quality, Cost, Logistics, Development, and Management (QCLDM), and transfer playbooks. Local engineering teams in Xi'an and Ho Chi Minh City oversee factory audits, tooling transfer, and quality controls across China, Vietnam, and upcoming Thailand facilities without interrupting serial supply.
Key Takeaways
- Precision components utilize advanced inspection systems, including ZEISS 3D coordinate measuring machines (CMM) and Mitutoyo contour metrology labs.
- Driveline components achieve spline pitch tolerances of ±0.008 mm through closed-die forging, hard turning, pull broaching, and carbonitriding.
- Progressive stamping dies machined from D2 or DC53 tool steel at 60 to 62 HRC hold punch-to-die clearances within ±0.002 mm for high-volume execution.
- Embedded engineering centers coordinate supplier evaluation scored on Quality, Cost, Logistics, Development, and Management (QCLDM) across regional hubs.
Managing supply chains across multiple Asian manufacturing regions requires a structured approach to supplier evaluation and engineering oversight. Procurement teams utilize Quality, Cost, Logistics, Development, and Management (QCLDM) scoring frameworks to audit factories and track milestone progress from blueprint intake to mass production. Embedded engineering hubs in Xi'an, China, and Ho Chi Minh City, Vietnam, coordinate design for manufacturability (DFM) reviews, pre-quote tolerance analysis, and tooling transfers across regional facilities.
When relocating tooling or expanding production corridors across China, Vietnam, and Thailand, structured relocation playbooks ensure uninterrupted component flow. Production lines transfer progressive stamping dies, fixtures, and inspection gauges while maintaining continuous quality control and full Production Part Approval Process (PPAP) Level 3 documentation.
- Supplier Auditing: Factory evaluation based on QCLDM criteria, shop-floor inspections, and process capability scoring.
- Engineering Review: Pre-quote 2D DWG and 3D CAD tolerance analysis, progressive die design, and mold flow simulation.
- Tooling Transfer: Structured relocation playbooks for moving dies, fixtures, and inspection gauges without production disruption.
- Regional Alignment: Coordination across manufacturing clusters in Zhejiang, Jiangsu, Guangdong, Bac Ninh, and Ho Chi Minh City.
What technical standards and metrology tools verify precision forged and machined components?
Precision forged and machined driveline components are verified using ZEISS 3D coordinate measuring machines (CMM), Mitutoyo metrology, contour profiling, surface roughness checks, and metallographic microstructure testing. Manufacturing lines leverage automated truss-robot loading, high-speed hydraulic pull broaching, automated continuous carbonitriding, and eddy-current crack sorting to maintain tight spline tolerances and case hardness.
High-precision drivetrain and structural parts require strict metrological control throughout the manufacturing lifecycle. Forging processes start with 160T to 630T closed-die warm or cold precision forging, accompanied by isothermal normalizing to produce uniform Ferrite-Pearlite grain flow. Subsequent operations utilize hard-turning lathe cells, high-speed hydraulic pull broaching, and automated continuous carbonitriding furnaces to achieve exact metallurgical and dimensional parameters.
Quality verification relies on multi-axis coordinate measuring machines and dedicated metrology labs. Automated eddy-current sorting checks parts for internal cracks and hardness variations prior to vacuum packaging, maintaining strict defect benchmarking across high-volume production runs.
- Precision Forging: Closed-die forging for CV joint star-shaped sleeves (#68-3 to #125), core shafts, and trunnion brackets.
- Machining & Broaching: Robotic CNC hard turning and hydraulic pull broaching holding ±0.008 mm spline pitch tolerances.
- Metrology Lab Verification: ZEISS and Mitutoyo 3D CMM inspection, contour testing, surface roughness analysis, and metallographic verification.
- Thermal & Surface Treatment: CQI-9 controlled carbonitriding achieving case depth of 0.85 to 1.25 mm and HRC 58 to 62 surface hardness.
Which design for manufacturability checks ensure dual-shore progressive stamping die stability?
Design for manufacturability checks for progressive stamping dies evaluate tool steel selection, wire EDM clearances, and standardized guide components before production. Machining dies from vacuum-hardened D2 or DC53 tool steel at 60 to 62 HRC using multi-pass wire EDM maintains punch-to-die clearances within ±0.002 mm, ensuring dimensional stability across dual-shore manufacturing runs.
Dual-shore sheet metal stamping programs connecting toolrooms in China with production facilities in Vietnam rely on rigorous tool engineering standards. DFM reviews confirm material selection, press tonnage requirements, and progressive die layout before cutting tool steel. High-volume stamping lines utilize SPCC or SS304 sheet metals ranging from 2.0 to 4.0 mm gauge thickness for heavy-duty structural components and fire extinguisher brackets.
To withstand continuous high-speed press runs, progressive die sets incorporate standardized components and wear-resistant tool steels. Toolrooms machine punches and dies using multi-pass wire electrical discharge machining (EDM) to maintain exact cutting clearances, supported by surface finishing treatments such as outdoor-grade polyester powder coating for corrosion resistance.
- Tool Steel Selection: Vacuum-hardened D2 (SKD11) or DC53 powdered metal tool steel hardened to 60–62 HRC.
- Precision Clearance: Multi-pass wire EDM holding punch-to-die clearances within ±0.002 mm.
- Standardized Tooling Components: Standardized MISUMI or FIBRO guide pillars, nitrogen gas springs, and modular pitch-pilot inserts.
- Secondary Processing & Finishing: High-tonnage stamping, CNC bending, robotic MIG/TIG welding, and salt-spray resistant powder coating.

Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What core metrology tools are used to verify precision machined and sintered components?
Verification relies on ZEISS 3D coordinate measuring machines (CMM), Mitutoyo metrology equipment, contour profiling tools, surface roughness testing, universal gear testers, and metallographic microstructure verification.
How are internal splines and star-shaped sleeves manufactured for driveline assemblies?
Core components undergo 160T to 630T closed-die warm or cold precision forging with isothermal normalizing, followed by automated CNC turning, high-speed hydraulic pull broaching, CQI-9 controlled carbonitriding, and eddy-current sorting.
What tooling standards are applied to progressive stamping dies for cross-border production?
Progressive stamping dies utilize vacuum-hardened D2 (SKD11) or DC53 tool steel heat-treated to 60–62 HRC, multi-pass wire EDM processing for ±0.002 mm punch clearances, standardized MISUMI or FIBRO guide pillars, nitrogen gas springs, and modular pitch-pilot inserts.
What processes are supported across powder metallurgy and sintered part manufacturing?
Powder metallurgy facilities utilize 5T to 500T CNC automatic powder presses, mesh-belt and vacuum sintering furnaces, steam treatment, and specialized equipment to produce structural gears, transmission sprockets, shock absorber pistons, oil pump rotors, and oil-impregnated bronze bushings.