What engineering processes control precision tolerances in automotive drivetrain components?
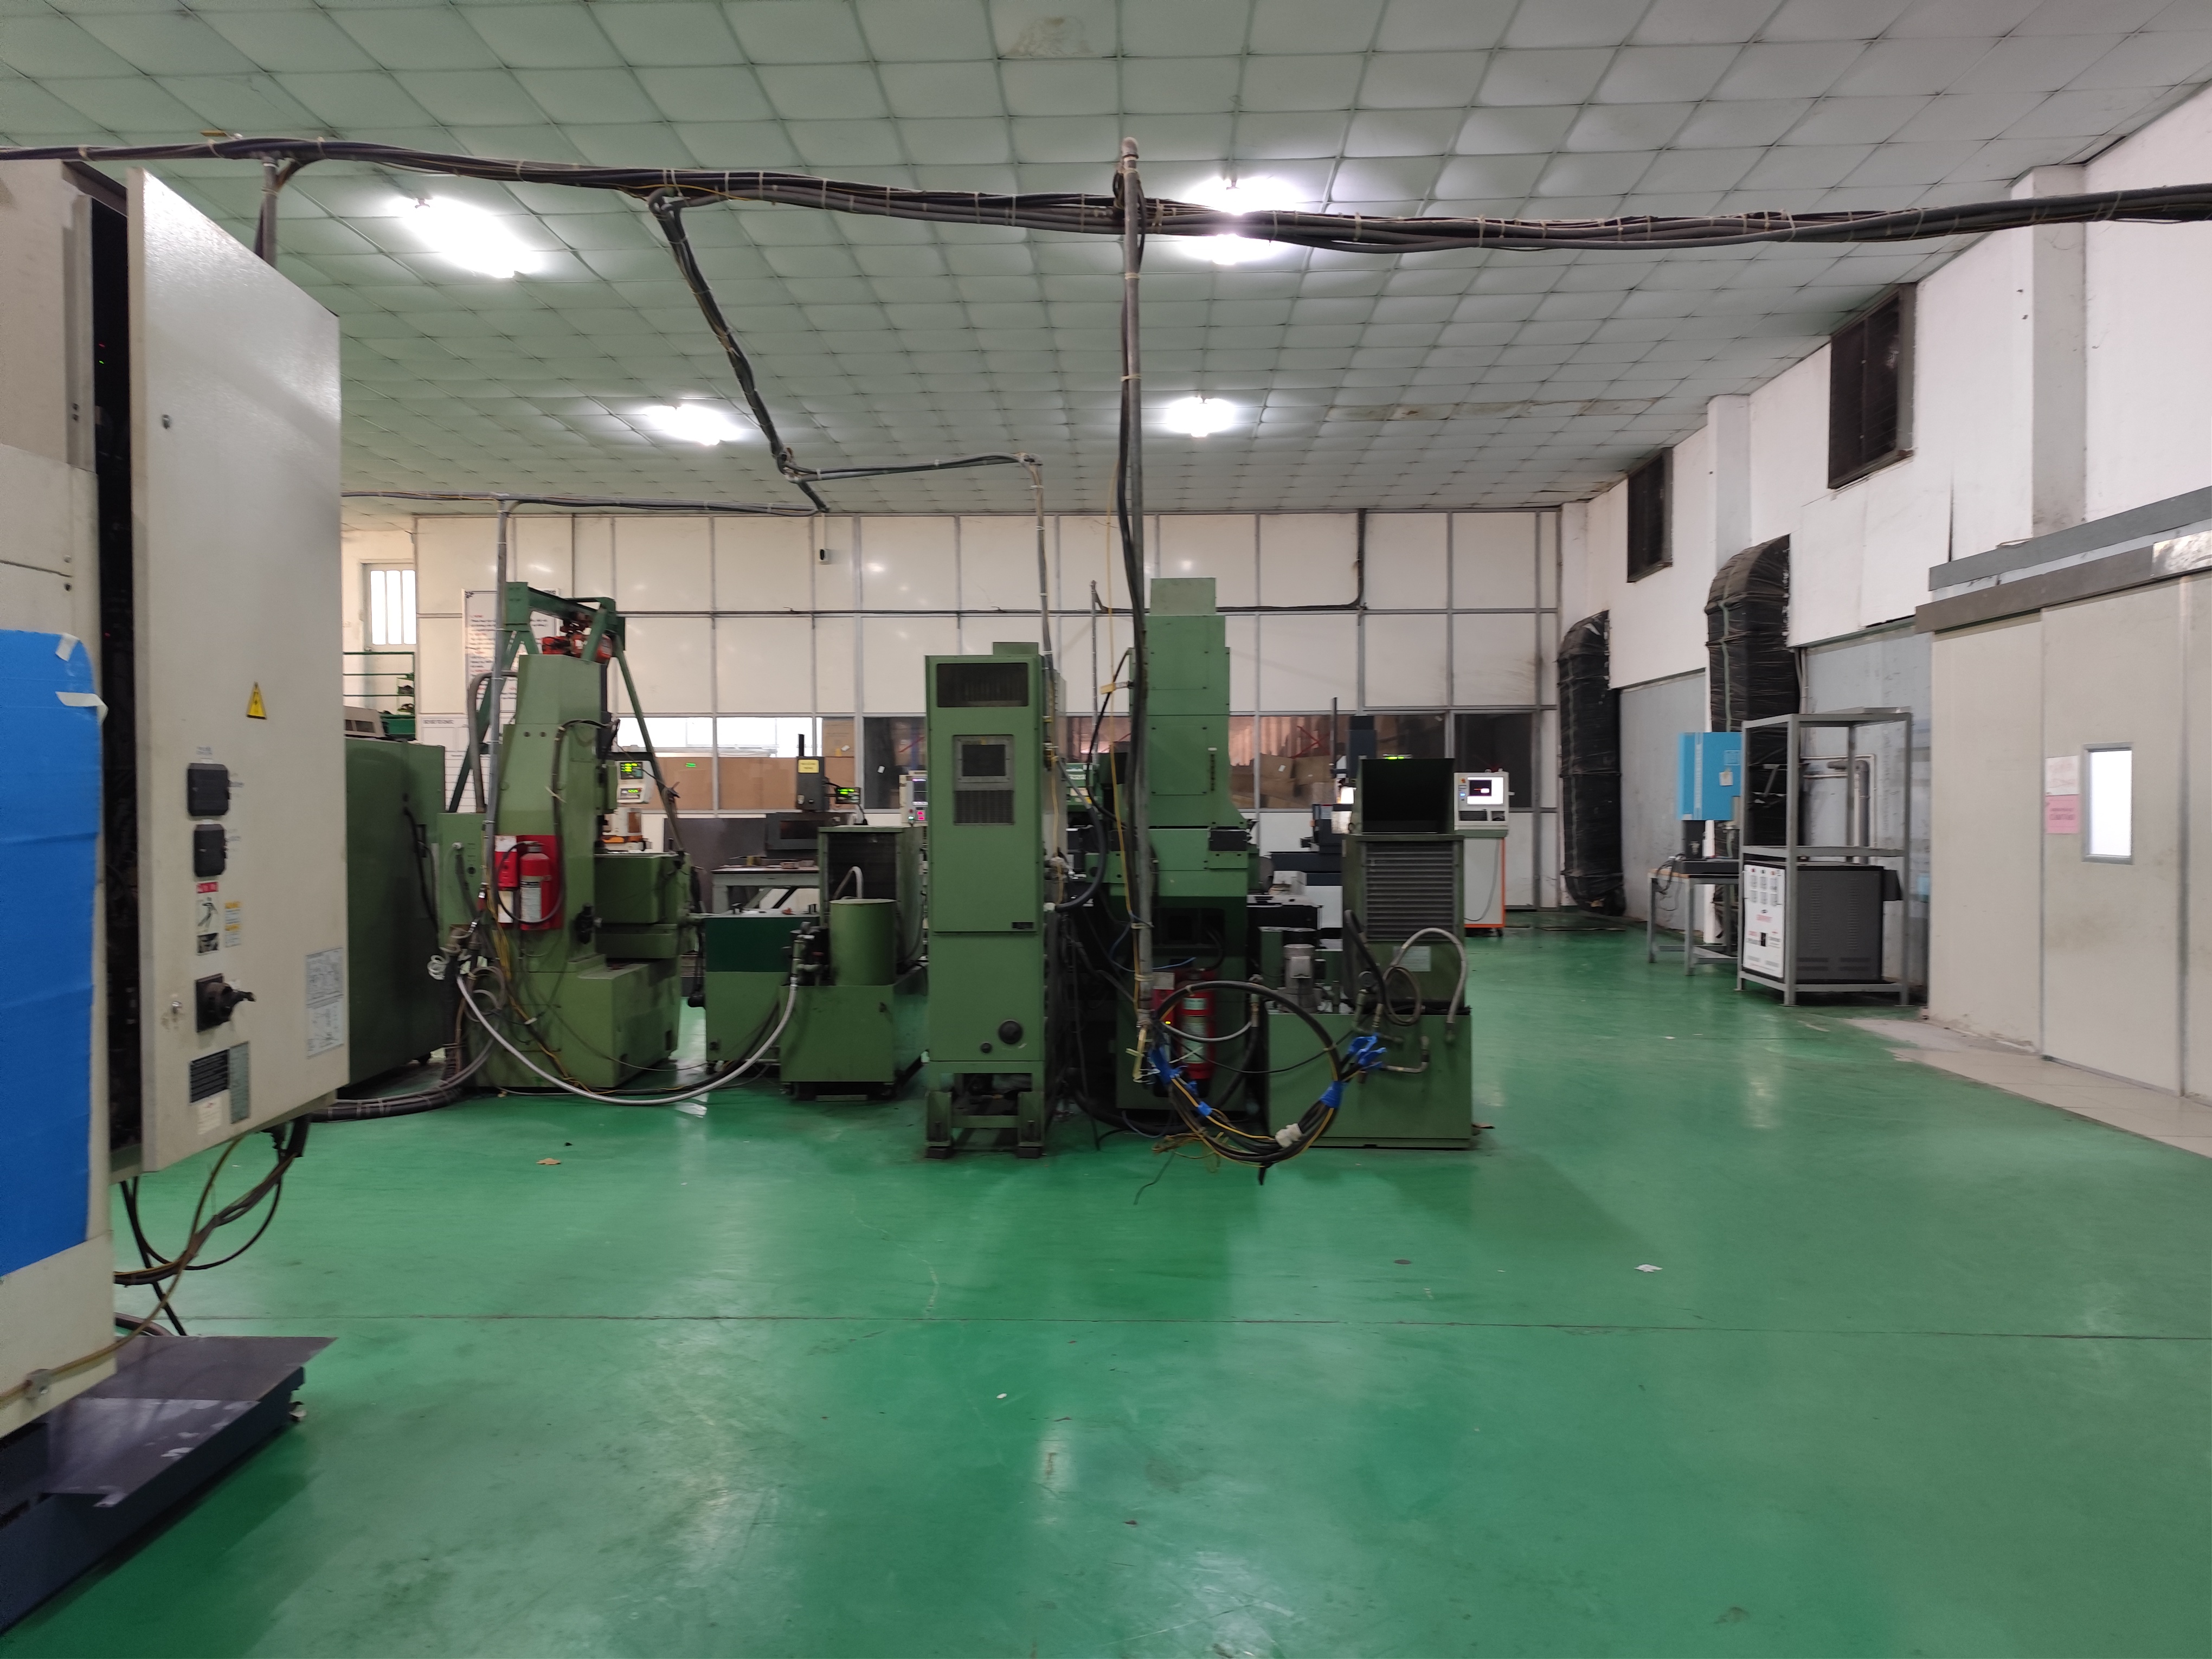
Automotive drivetrain manufacturing relies on a sixteen-stage vertically integrated process flow including isothermal annealing, precision cold or warm forging, and internal spline broaching. Machining utilizing 136 robotic CNC lathes and EMAG turning centers maintains spline pitch tolerances to plus or minus 0.008 millimeters, followed by CQI-9 carbonitriding for HRC 58 to 62 carburized hardness.
Key Takeaways
- Drivetrain components maintain spline pitch tolerances of ±0.008 mm with HRC 58–62 hardness through 16-stage forging, CNC turning, spline broaching, and CQI-9 heat treatment.
- Engineering service hubs in Xi'an (26 staff) and Ho Chi Minh City (7 staff) oversee QCLDM audits, DFM review, and a 10-month China-to-Vietnam tooling transfer playbook.
- Precision manufacturing across audited facilities spans powder metallurgy, AS9100D 5-axis CNC micro-machining, heavy stamping up to 315T, and high-purity fluoropolymer fabrication.
- Metrology validation utilizes ZEISS 3D CMM dimensional inspection, eddy-current crack sorting, and ASTM B117 salt spray testing.
High-precision driveline manufacturing requires structured step-by-step processing to achieve high-volume repeatability and tight geometric control. In automotive drivetrain programs, raw 20CrMnTi or SAE 5120H carburizing alloy steel undergoes bar cutting, isothermal annealing, shot blasting, and saponification prior to closed-die cold or warm precision forging in press lines ranging from 160T to 630T. Controlled normalizing ensures uniform Ferrite-Pearlite grain flow before secondary operations begin.
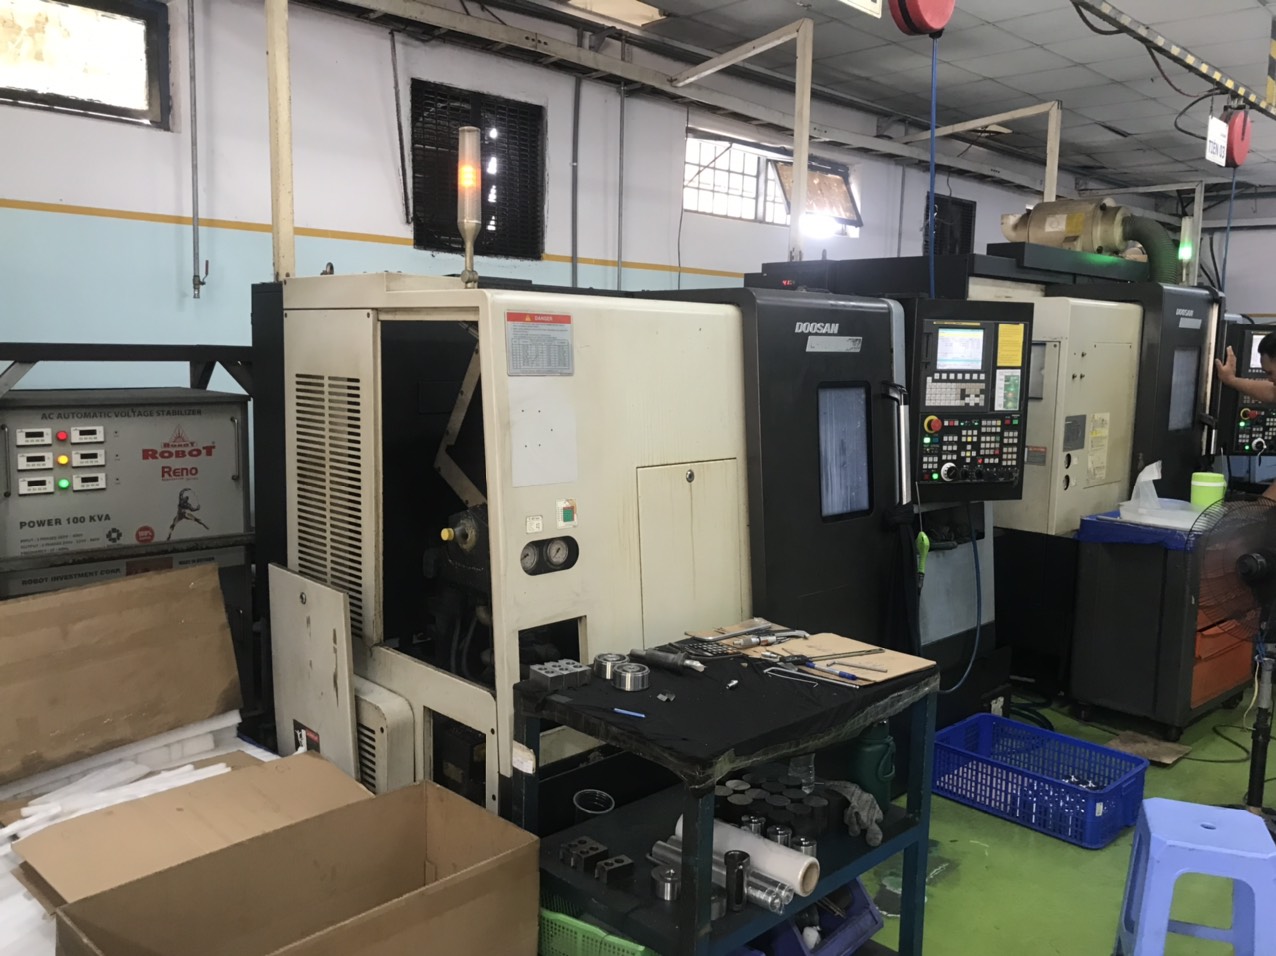
Internal geometry and drive splines are shaped via high-speed hydraulic pull broaching and high-precision hard turning. Workpieces are machined using 136 robotic CNC lathes and EMAG turning centers, maintaining raceway concentricity and DIN 5480 or JIS B 1603 spline module specifications. Following automated groove grinding, components undergo CQI-9 controlled carbonitriding and quenching to establish a 0.85 mm to 1.25 mm carburized depth.
- Raw Material Selection: 20CrMnTi and SAE 5120H carburizing alloy steel bars.
- Forging & Pre-Treatment: 160T–630T closed-die precision forging with isothermal normalizing.
- Machining Equipment: 136 robotic CNC lathes, 72 robotic CNC mills, and 4 German EMAG turning centers.
- Spline Geometry & Tolerance: Internal spline broaching maintaining ±0.008 mm spline pitch tolerance.
- Heat Treatment Parameters: CQI-9 carbonitriding delivering HRC 58–62 carburized hardness.
How do multi-region engineering teams coordinate production transfers between China, Vietnam, and Thailand?
Regional engineering coordination connects a 26-person service center in Xi'an, China with 7 local staff in Ho Chi Minh City, Vietnam. Teams execute a 10-month migration playbook to transfer dies, tooling fixtures, and quality control gauges while deploying DFM review, PPAP Level 3 documentation, and sub-component sourcing across China, Vietnam, and Thailand.
Managing multi-country manufacturing requires local engineering oversight and structured project playbooks. DEWIN coordinates production across China, Vietnam, and Southeast Asia through Singapore HQ and dedicated regional centers. The Xi'an Service Center in China employs 26 full-time staff handling pre-quote 2D/3D DFM tolerance analysis, progressive die design, mold flow simulation, and PPAP Level 3 documentation.
In Vietnam, 7 local staff operate across Ho Chi Minh City, Binh Duong, Dong Nai, Bac Ninh, and Haiphong to manage audited production nodes. A 10-month migration playbook enables transferring stamping dies, assembly fixtures, and quality inspection gauges from China to Vietnam without interrupting supply. Sourcing expansion includes a 2027 Thailand manufacturing facility covering 25,000 square meters in Ningbo HQ synergy.
- Xi'an Service Center (China): 26 engineers managing DFM review, tooling design, and PPAP Level 3 controls.
- Vietnam Local Hub: 7 engineers in Ho Chi Minh City and Bac Ninh overseeing 300+ mapped factories.
- Line Relocation Playbook: 10-month structured transfer of progressive dies, welding cells, and QC gauges.
- ASEAN Network Expansion: Synergies connecting China, Vietnam, and Thailand manufacturing plants.
Which inspection standards and metrology tools verify structural component quality?
Quality verification relies on ZEISS and Mitutoyo 3D CMM metrology, contour testing, surface roughness evaluation, and metallographic microstructure analysis. Suppliers utilize IATF 16949:2016, AS9100D, and ISO 9001:2015 frameworks alongside 100 percent eddy-current crack sorting, magnetic particle detection, and 240-hour ASTM B117 salt spray testing to validate production integrity.
Quality management across diverse component categories requires specialized metrology equipment and strict audit frameworks. Precision machining nodes utilize ZEISS and Mitutoyo Crysta-Apex S 3D coordinate measuring machines for 3D dimensional verification, alongside specialized contour, surface roughness, and metallographic microstructure testing.
Manufacturing facilities align with international operational standards, including IATF 16949:2016 for automotive drivetrain components, AS9100D for aerospace 5-axis CNC micro-machining, and ISO 13485:2016 for medical components. Non-destructive evaluation incorporates 100 percent eddy-current crack sorting, magnetic particle inspection, and 240-hour ASTM B117 salt spray testing for protective coatings.
- Metrology Instruments: ZEISS and Mitutoyo 3D CMMs, contour testers, and metallographic labs.
- Aerospace Machining Standards: AS9100D and GJB 9001C-2017 compliant 5-axis CNC machining.
- Powder Metallurgy Standards: IATF 16949:2016 sintered gears, rotors, and oil-impregnated bushings.
- Surface Finishing Verification: 240-hour ASTM B117 salt spray and 1,500-hour UV powder coat testing.
Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What processes are available for powder metallurgy and metal injection molding?
Powder metallurgy processes include automatic presses from 15T to 500T, vacuum sintering, and mesh-belt furnaces producing structural gears, shock absorber pistons, oil-impregnated bronze bushings, and oil pump rotors. Metal injection molding (MIM) utilizes 17-4PH and 316L stainless steel with catalytic debinding and vacuum sintering.
How are heavy stamping and robotic welding assemblies validated?
Heavy stamping facilities utilize progressive presses up to 315T, laser cutting, and Panasonic or OTC welding robots for assemblies such as desk frames, monitor arms, and fire extinguisher brackets. Validation includes 5G vibration testing, 240-hour ASTM B117 salt spray exposure, and cyclic load testing.
What fluoropolymer and high-performance engineering plastic parts are produced?
Engineering plastic operations process high-purity PTFE, PFA, FEP, PVDF, PEEK, PI, and PPS. Processes include Class cleanroom assembly, multi-slider hot-runner injection molding, compression sintering, and multi-axis CNC machining for chemical tower internals, semiconductor wafer carriers, and encapsulated O-rings.
Which bearing categories and size ranges are supported across audited plants?
Bearing production spans SF-1 and SF-2 PTFE composite bushings, bimetal bearings, graphite-plugged bronze bearings, and spherical plain bearings from 4 mm to 630 mm. Large-scale production covers single, double-row, and crossed-roller slewing bearings from 200 mm up to 5,000 mm diameter.