
How Does On-Site Engineering Oversight Manage DFM and Precision Machining Across Asian Production Hubs?
On-site engineering oversight coordinates design for manufacturability reviews, pre-quote tolerance analyses, and multi-axis CNC machining across specialized facilities in China and Vietnam. Managed by dedicated engineering teams in Xi'an and Ho Chi Minh City, this structured coordination standardizes quality control using ZEISS coordinate measuring machines to verify tight dimensional tolerances across complex metal parts.
Key Takeaways
- Engineering teams in Xi'an, China (26 staff) and Ho Chi Minh City, Vietnam (7 staff) manage factory audits, DFM reviews, and ZEISS CMM dimensional inspections.
- Precision automotive forging utilizes a 16-stage in-house process flow featuring isothermal annealing, 136 robotic CNC lathes, internal spline broaching, and CQI-9 heat treatment.
- Powder metallurgy, metal injection molding (MIM), and fluoropolymer processing support high-volume structural gears, oilless bushings, and semiconductor components.
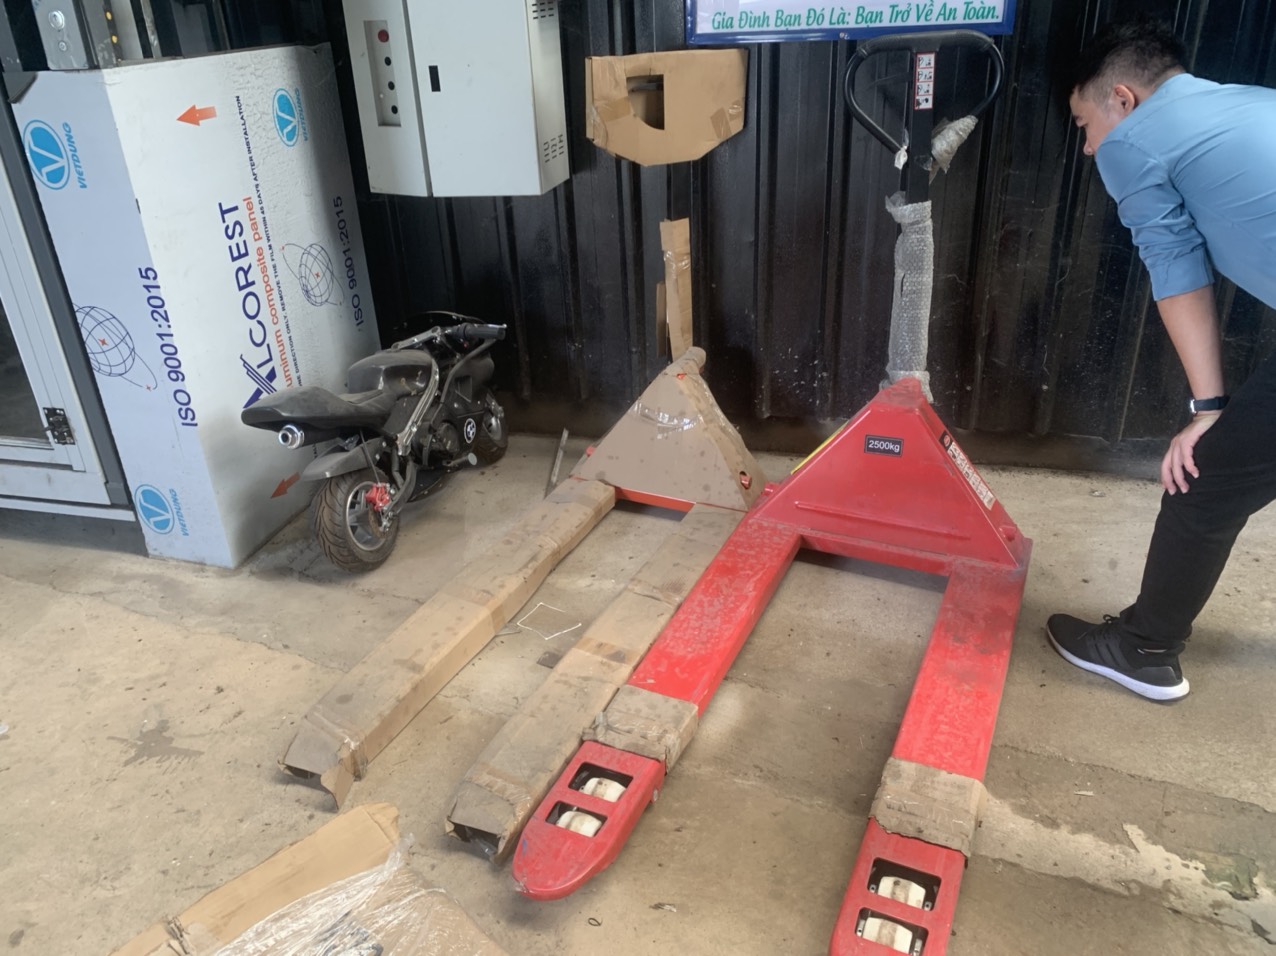
- Turnkey assembly programs manufacture CE-compliant hydraulic hand pallet trucks in Bac Ninh, Vietnam and UL 711 heavy-duty brackets with ASTM B117 salt spray protection.
Managing complex cross-border supply chains requires active on-site engineering teams directly stationed in key industrial cities. Through centralized engineering centers in Xi'an, China and local offices in Ho Chi Minh City, native technical personnel conduct comprehensive supplier audits, review 2D drawings and 3D CAD files, and establish robust Quality, Cost, Logistics, Development, and Management (QCLDM) protocols.
Precision machining operations utilize advanced multi-axis equipment, including 5-axis CNC machining centers, turn-mill compound machines, and Swiss-type CNC lathes. Dimensional accuracy is continuously validated in temperature-controlled metrology laboratories equipped with ZEISS and Mitutoyo 3D Coordinate Measuring Machines (CMM), ensuring strict compliance with GD&T specifications down to micro-level tolerances.
- 2D drawing and 3D CAD DFM analysis with tolerance verification prior to tooling production
- AS9100D aerospace-grade 5-axis and 4-axis CNC machining for complex titanium and aluminum housings
- In-process ZEISS 3D CMM dimensional inspection and material composition documentation
- Seamless multi-region production management across China, Vietnam, and Thailand facilities
What Inspection Standards and Processing Stages Secure Quality in Automotive Forging Operations?
Automotive forging operations maintain quality through a 16-stage vertically integrated process flow that incorporates raw steel bar cutting, isothermal annealing, precision cold or warm forging, and CQI-9 heat treatment. Quality assurance relies on automated eddy-current crack detection, magnetic particle inspection, and ZEISS 3D metrology lab verifications to ensure exact spline pitch and raceway concentricity.
High-stress driveline components, such as CV joint star-shaped sleeves, trunnion brackets, and core shafts, demand strict metallurgical control and precise mechanical processing. Facilities operating under IATF 16949 quality management and CQI-9 heat-treat standards utilize closed-die warm and cold forging presses ranging from 160T to 630T capacity to establish optimal grain flow prior to machining.
Following precision forging, parts undergo high-speed hydraulic pull broaching to generate internal splines held to DIN 5480 and JIS B 1603 module standards. Automated loading robots feed 136 CNC turning centers and 4-axis German EMAG hard-turning cells, maintaining raceway concentricity tolerances within ±0.008 mm before continuous furnace carbonitriding and induction hardening.
- 16-stage vertically integrated process: bar cutting, annealing, shot blasting, saponification, forging, normalizing, turning, broaching, milling, grinding, carbonitriding, eddy-current testing, cleaning, and vacuum packing
- Automated internal spline broaching achieving ±0.008 mm spline pitch tolerances
- Controlled CQI-9 carbonitriding furnace hardening delivering case depths of 0.85 to 1.25 mm (HRC 58–62)
- 100% eddy-current and magnetic particle crack sorting prior to anti-rust packaging
Which Specialized Materials and Manufacturing Processes Are Utilized for Industrial Components?
Industrial components leverage specialized processes including powder metallurgy, metal injection molding, fluoropolymer machining, heavy stamping, and robotic welding. Factories utilize high-tonnage mechanical and hydraulic presses, mesh-belt sintering furnaces, cleanroom molding lines, and automated MIG welding cells to produce structural gears, oilless bushings, slewing bearings, and heavy-duty brackets across multi-country manufacturing networks.
Powder metallurgy (PM) and Metal Injection Molding (MIM) enable high-density production of complex structural parts, including sintered transmission gears, oil pump rotors, and 316L stainless steel components. Automated powder presses from 5T to 680T coupled with mesh-belt and vacuum sintering furnaces achieve high metallurgical density and dimensional stability across iron, bronze, and stainless steel alloys.
For sliding, rotational, and structural applications, specialized facilities manufacture self-lubricating PTFE composite bushings, bimetal bearings, spherical plain bearings, and large-diameter slewing rings up to Ø5,000 mm. Additionally, cleanroom processing of high-purity fluoropolymers like PEEK, PTFE, and PFA provides chemically resistant components for semiconductor and fluid handling equipment.
- Powder metallurgy structural gears, SAE841 oil-impregnated bronze bushings, and 17-4PH / 316L MIM components
- Ø200–5,000 mm single/double-row four-point contact ball and crossed-roller slewing bearings
- Heavy progressive stamping presses up to 315T and robotic MIG/TIG welding cells for ergonomic frames and brackets
- High-purity PTFE, PFA, PEEK, and PVDF fluoropolymer cleanroom injection molding and multi-axis CNC machining
- CE and ISO 3691-5 hydraulic hand pallet truck manufacturing in Bac Ninh, Vietnam
- UL 711 heavy-duty stamped fire extinguisher brackets with 240hr+ ASTM B117 salt spray protection

Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
How are pre-production drawings and tolerances validated before tooling creation?
Engineering teams conduct pre-quote 2D and 3D design for manufacturability (DFM) reviews, tolerance stack-up analyses, progressive die simulations, and mold flow modeling. This step ensures that part geometry, material callouts, and GD&T requirements align with factory equipment capabilities before tool steel is cut.
What metrology equipment is used to inspect precision machined tolerances?
Facilities utilize climate-controlled metrology laboratories equipped with ZEISS and Mitutoyo Crysta-Apex 3D Coordinate Measuring Machines, contour measuring instruments, surface roughness testers, and metallographic hardness testing systems to verify critical dimensions down to ±0.008 mm.
How does the 16-stage driveline forging process control part defect rates?
The 16-stage process combines controlled bar cutting, isothermal annealing, saponification, closed-die cold/warm forging, and normalized grain flow with automated CNC turning, CQI-9 carbonitriding, and 100% inline eddy-current crack testing to maintain defect rates down to 50 PPM benchmarks.
What surface treatment standards apply to heavy-duty stamped brackets?
Heavy-duty stamped brackets undergo high-tonnage progressive stamping, robotic MIG welding, and outdoor-grade polyester powder coating designed to withstand 240-hour ASTM B117 salt spray testing and 1,500-hour UV exposure requirements.