How do cross-border engineering teams manage supplier quality and DFM reviews?
Cross-border engineering teams manage supplier quality through early design for manufacturing (DFM) drawing reviews, structured QCLDM factory audits, and direct quality control presence. Operating hubs in Xi'an, China, and Ho Chi Minh City, Vietnam, coordinate tolerance analysis, PPAP Level 3 documentation, and ZEISS 3D coordinate measuring machine metrology across regional manufacturing facilities.
Key Takeaways
- Production management across China, Vietnam, and Thailand leverages local teams in Xi'an and Ho Chi Minh City for DFM reviews, QCLDM audits, and ZEISS CMM metrology.
- Driveline component fabrication utilizes a 16-stage process—including cold/warm forging, broaching, and CQI-9 heat treatment—achieving ±0.008 mm spline pitch tolerances.
- Advanced materials and processes span AS9100D 5-axis aerospace machining, metal injection molding, powder metallurgy, high-purity fluoropolymers, and heavy sheet metal stamping.
Engineers based in Xi'an (26 staff) and Ho Chi Minh City (11 staff) execute pre-quote 2D and 3D tolerance analysis, progressive die design evaluation, and mold flow simulations prior to tooling fabrication. Resident quality engineers maintain supplier quality standards across 178 factories in Vietnam and specialized facilities throughout China.
Quality management protocols incorporate early product development tracking, milestone-by-milestone tooling validation, and first article inspections. Production relocation playbooks enable transferring dies, fixtures, and custom gauges within 10 months to maintain supply chain continuity.
- DFM and Tooling Engineering: Pre-quote 2D/3D tolerance analysis, progressive die design, and mold flow simulation before cutting steel.
- Metrology Verification: ZEISS and Hexagon 3D CMM inspection, contour testing, surface roughness analysis, and metallographic density checks.
- Quality Control Benchmarking: PPAP Level 3 documentation, material certificates of analysis (COA), and resident supplier quality engineer (SQE) audits aimed at 50 PPM benchmarks.
- Relocation Management: 10-month production transfers moving dies, fixtures, and quality control gauges across regional facilities without supply interruptions.
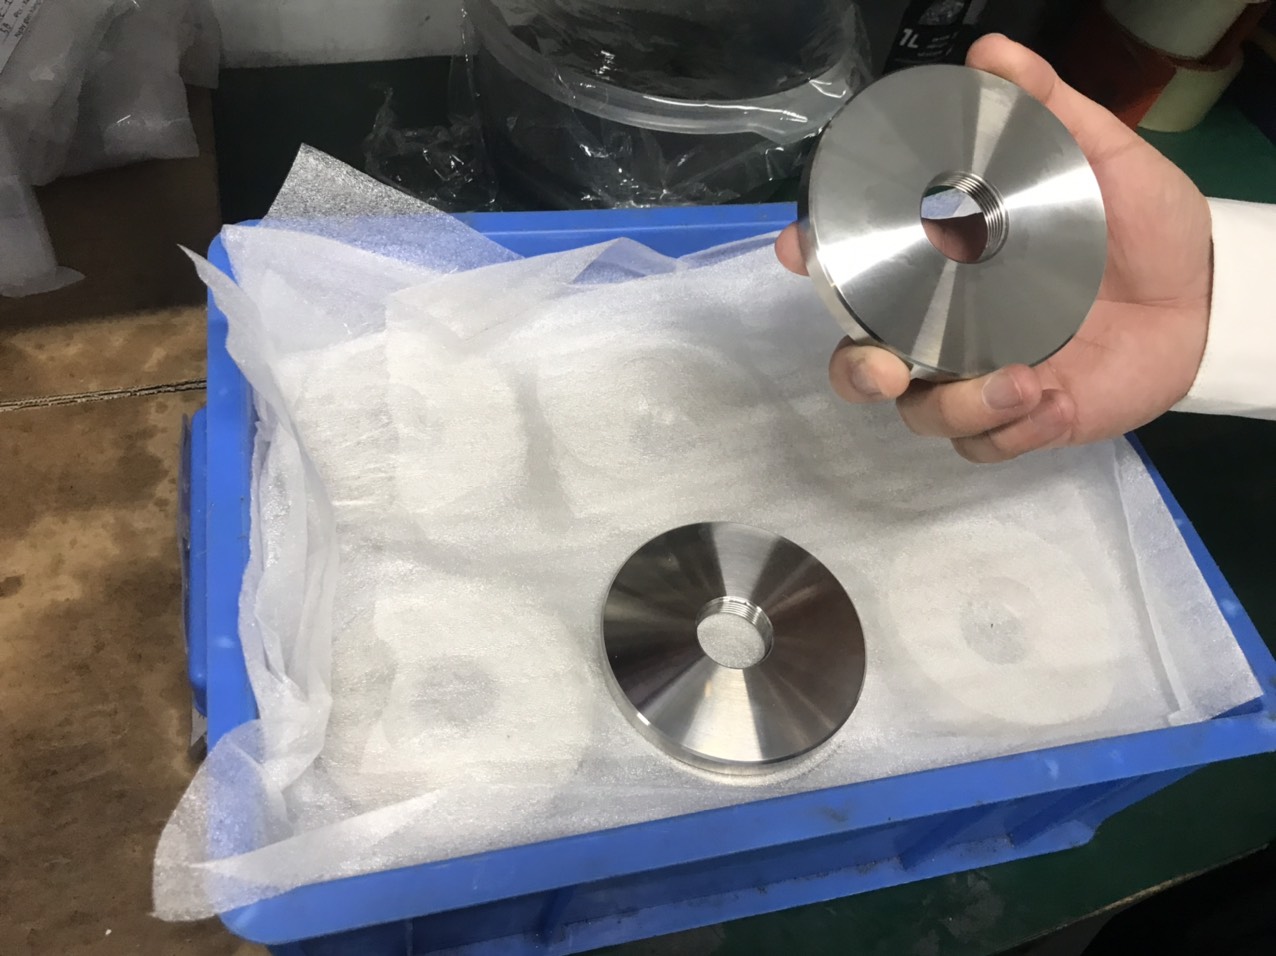
What manufacturing processes control tight tolerances for driveline components?
Driveline components rely on a vertically integrated 16-stage process flow combining precision cold/warm forging, isothermal normalizing, automated robotic turning, and internal spline broaching. Controlled carbonitriding heat treatment under CQI-9 standards achieves case hardness of HRC 58–62 and spline pitch accuracy of ±0.008 mm prior to eddy-current crack testing and ultrasonic cleaning.
High-volume drivetrain parts, such as CV joint star-shaped sleeves (#68-3 to #125) and TJ/AAR trunnion brackets, undergo a 16-stage production flow starting with raw steel bar cutting, isothermal annealing, shot blasting, and saponification with phosphating.
Precision cold and warm closed-die forging (160T to 630T) establishes uniform Ferrite-Pearlite grain flow. Hard turning on 136 robotic CNC lathes and 4 German EMAG centers works alongside high-speed hydraulic pull broaching to maintain DIN 5480 or JIS B 1603 spline module specifications.
- Precision Forging: 160T–630T closed-die cold and warm forging with controlled normalizing to establish uniform grain flow.
- Automated Machining: Hard-turning on 136 robotic CNC lathes and 4 German EMAG centers alongside 72 robotic CNC milling machines.
- Spline Broaching: High-speed hydraulic pull broaching meeting DIN 5480 and JIS B 1603 spline module standards.
- Surface Treatment & Testing: CQI-9 controlled carbonitriding (0.85–1.25 mm case depth), 100% eddy-current crack sorting, and vacuum anti-rust packaging.
Which specialized materials and processes are deployed across Asian manufacturing hubs?
Asian manufacturing hubs deploy diverse production processes including powder metallurgy, 5-axis aerospace CNC machining, fluoropolymer molding, and automated progressive stamping. These facilities process titanium, Inconel, 304/316L stainless steel, PEEK, PTFE, and bimetals to produce structural gears, aerospace valve blocks, oilless bushings, and heavy-duty stamped hardware.
Specialized specialist plants managed through the Xi'an center handle complex structural and friction components. For instance, powder metallurgy and metal injection molding (MIM) facilities produce iron, copper, 17-4PH, and 316L stainless steel sprockets, oil pump rotors, and soft magnetic cores.
Precision machining centers utilize 70 sets of 5-axis and 4-axis CNC machines for aerospace-grade titanium and Inconel hydraulic valve blocks. Plastic processing facilities execute cleanroom assembly, DI water cleaning, and high-temperature injection molding of PEEK, PFA, FEP, and PTFE components for semiconductor and chemical applications.
- Aerospace Micro-Machining: 5-axis and 4-axis CNC machining, turn-mill compounds, and wire EDM for titanium and Inconel aerospace valve blocks.
- Powder Metallurgy & MIM: 15–500T powder presses and vacuum degreasing-sintering furnaces for structural gears, oil pump rotors, and 17-4PH / 316L MIM components.
- Bearings & Tribology: Continuous bronze-powder sintering strip lines for PTFE composite bushings, bimetal bearings, graphite-plugged bronze, and spherical plain bearings.
- High-Purity Plastics: Cleanroom high-temperature injection molding and multi-axis CNC machining of PEEK, PFA, FEP, and PTFE fluoropolymer parts.
- Stamping & Welding: Progressive stamping up to 315T, laser cutting, and 9 robotic MIG/TIG welding cells for stamped brackets and desk frames.

Precision Manufacturing & Sourcing Specification Matrix
| Technical Dimension | Standard Commercial Grade | High-Precision OEM Export Grade | DEWIN Verification Protocol |
|---|---|---|---|
| Machining & Forming Tolerance | ISO 2768-m (±0.10 mm nominal) | ISO 2768-f (±0.01 mm – ±0.025 mm critical bores) | Calibrated 3D CMM & Air/Pin Gauging |
| Surface Roughness & Finish | Ra 1.6 – 3.2 µm as-machined / standard coat | Ra 0.4 – 0.8 µm precision ground / MIL-A-8625 anodized | Profilometer & Coating Thickness Gauge |
| Material & Alloy Certification | Supplier Mill Test Report (MTR) | Independent OES chemical & mechanical verification | EN 10204 3.1 + RoHS/REACH Compliance |
| Batch Inspection & Packaging | ISO 2859-1 (AQL 1.0 Major / 2.5 Minor) | Zero-defect critical features + VCI export crating | Pre-Shipment Inspection (PSI) Report |
Frequently Asked Questions
What metrology equipment is utilized to inspect precision machined components?
Production facilities employ temperature-controlled metrology labs equipped with ZEISS and Mitutoyo Crysta-Apex S 3D coordinate measuring machines, gear profile testers, contour instruments, surface roughness analyzers, and metallographic density verification equipment.
What production capacity exists for driveline CV joint star sleeves?
Driveline manufacturing lines produce up to 2.9 million star-shaped sleeves monthly covering over 500 SKUs (ranging from #68-3 to #125), alongside 3.6 million TJ/AAR trunnion brackets per year.
How are environmental resistance standards met for stamped steel assemblies?
Stamped assemblies such as fire extinguisher brackets undergo outdoor-grade polyester powder coating, quick-release latch fitting, and pass 240+ hour ASTM B117 salt spray exposure along with 1,500-hour UV weathering tests.
What options exist for hydraulic hand pallet truck manufacturing in Vietnam?
Facilities in Bac Ninh, Vietnam, produce 2.0T to 5.0T capacity hand pallet trucks compliant with ISO 3691-5 standards, featuring AC/DF integrated cast-iron pumps, PU/Nylon rollers, robotic MIG welding, and 100% hydraulic leak testing.