Sheet metal fabrication procurement 1 trips up even experienced buyers. I’ve watched clients lose months to rework because a supplier missed a bend tolerance or chose the wrong steel grade — problems that proper vetting would have prevented.
Common pitfalls in sheet metal fabrication procurement include focusing only on piece price while ignoring supplier capabilities, applying unrealistic tolerances across entire drawings, selecting inappropriate materials, skipping design for manufacturability reviews, and assuming surface finishes will hide fabrication flaws. These mistakes drive hidden costs, delays, and quality failures.
Each of these pitfalls feeds the next. A cheap quote often hides capability gaps. Capability gaps produce quality control issues 2. Quality issues cause delivery delays. And delays erode trust. Let me walk you through the specific traps I see most often — and how to avoid them.
How can I ensure my supplier doesn't overlook critical tolerances in my sheet metal drawings?
A lesson we learned early at DEWIN: a U.S. client sent us a drawing with every single dimension held to ±0.05 mm. The part was a simple mounting bracket. No feature on it required that level of precision, yet the previous supplier had quoted it at face value — and still delivered parts out of spec.
To ensure your supplier respects critical tolerances, clearly distinguish critical dimensions from general ones on your drawings, apply the 4T rule for features near bends, and require your supplier to submit a tolerance review or DFM feedback before production begins.
Why Blanket Tight Tolerances Backfire
When every dimension on a drawing carries a tight tolerance, the fabricator faces a choice: price the job sky-high to cover extra setups, or quietly treat the tight callouts as general tolerances to keep costs down. Neither outcome is good for you.
Tight tolerances on non-critical dimensions force extra inspection steps. They require slower machine feeds. They demand more skilled operators. All of this adds cost without improving the part's function in its final assembly.
The 4T Rule and Bend Proximity
One of the most overlooked tolerance specifications in sheet metal work is the relationship between holes and bends. If a hole sits too close to a bend line, the material stretches and distorts the hole. The industry standard — the 4T rule 3 — states that features must be at least four times the material thickness away from any bend.
| Material Thickness | Minimum Feature Distance from Bend | Common Violation |
|---|---|---|
| 1.0 mm | 4.0 mm | Holes placed 2 mm from bend |
| 1.5 mm | 6.0 mm | Slots placed 3 mm from bend |
| 2.0 mm | 8.0 mm | Notches placed 4 mm from bend |
| 3.0 mm | 12.0 mm | Cutouts placed 6 mm from bend |
How We Handle Tolerance Reviews
On our side, every new project goes through a formal DFM review 4 before we confirm pricing. Our engineering team in Vietnam flags any dimension that conflicts with standard fabrication limits. We send back a marked-up drawing — green for feasible, yellow for achievable at added cost, red for physically impossible without process changes.
This approach catches problems before tooling is cut. It also opens a dialogue. Many clients tell us their previous suppliers never questioned a drawing. That silence is not a sign of capability. It is a sign of risk. A fabricator who accepts every tolerance without comment either does not understand the drawing or plans to ignore it.
Practical Steps for Buyers
Here is what I recommend to every procurement manager reviewing sheet metal drawings:
- Mark critical dimensions with a diamond or GD&T callout. Leave the rest at general tolerance.
- Ask your supplier to confirm the 4T rule compliance for every feature near a bend.
- Request a first-article inspection report 5 (FAIR) that specifically measures critical dimensions.
- Include a tolerance review step in your supplier selection criteria before awarding the job.
Even a ±0.1 mm deviation in material thickness can disrupt downstream tooling compatibility. So the goal is not to relax everything — it is to focus precision where it matters.
Why am I experiencing frequent delivery delays and quality issues with my current sheet metal source?
Last quarter, a client came to us after their existing supplier missed three consecutive shipments. The root cause was not capacity. It was a communication breakdown: the supplier had changed raw material grades without informing the buyer, causing weld failures that triggered rework loops.
Frequent delivery delays and quality control issues usually stem from poor supplier vetting, lack of process controls, material substitution without approval, absent DFM collaboration, and no structured inspection protocol — not simply from production capacity limitations.

The Real Causes Behind Chronic Delays
Most buyers blame delays on production capacity. In my experience, the true culprits are upstream: unclear specifications, raw material availability problems, and the absence of a quality management system 6 that catches defects early.
When a supplier lacks a formal inspection process — where quality checks are not limited to the operator doing the work — defects travel downstream. A bad bend becomes a bad weld becomes a bad assembly. Each stage of rework adds days. Multiply that across a batch, and your lead time doubles.
Price-First Procurement Creates a Vicious Cycle
Here is the pattern I see repeatedly:
| Stage | What Happens | Result |
|---|---|---|
| RFQ | Buyer selects lowest bidder | Supplier underbids to win |
| Production | Supplier cuts corners on material or inspection | Defects emerge at assembly |
| Rework | Supplier reworks or ships non-conforming parts | Delivery slips by 2–4 weeks |
| Escalation | Buyer demands expedited shipment | Air freight costs spike |
| Re-sourcing | Buyer starts looking for new supplier | 3–6 months lost |
This cycle repeats because the supplier selection criteria never changed. The buyer still leads with price. The next supplier underbids again. And the loop continues. Understanding why sheet metal fabrication supplier quotes vary so much is key to breaking this pattern.
What Effective Lead Time Management Looks Like
At DEWIN, we manage lead time through three mechanisms:
- Material pre-confirmation: Before production, we confirm the exact grade and temper with the client. No substitutions without written approval.
- In-process inspection gates: Our Vietnam team conducts inspections at cutting, forming, welding, and finishing stages — not just final inspection.
- Weekly progress reporting: Clients receive updates with photos and measurements at each gate. If a problem appears, we catch it in week one, not week six.
Supply chain resilience also matters. We maintain relationships with multiple raw material suppliers across Vietnam and the broader ASEAN region. When one source faces a shortage, we have backups. This redundancy is not free, but it is far cheaper than a missed delivery.
The Role of Industry Certifications
Certifications like ISO 9001 7 are not magic. But they indicate that a supplier has documented processes. A certified supplier has control plans, corrective action procedures, and audit trails. These systems make quality repeatable. Without them, quality depends entirely on individual skill — and individuals have bad days.
When evaluating a new source, I recommend asking not just "Do you have ISO 9001?" but "Show me your control plan for this part." The answer tells you more than the certificate on the wall.
What are the hidden risks I should watch for when sourcing sheet metal parts from Vietnam?
When we opened our Vietnam office seven years ago, we saw the opportunity clearly — competitive labor costs, a growing manufacturing base, and geographic diversification away from China. But we also discovered risks that do not show up on a quote sheet.
Hidden risks when sourcing sheet metal parts from Vietnam include inconsistent raw material availability, limited local supply of specialty grades, fewer experienced fabricators compared to China, potential communication breakdowns due to language gaps, and less mature quality management systems at many smaller shops.
Material Sourcing Challenges
Vietnam's domestic steel production is growing, but the range of available grades is narrower than what you find in China, Japan, or South Korea. If your part requires a specific grade — say, SUS 316L stainless steel 8 in a particular temper — it may need to be imported. That adds lead time and cost.
| Factor | Vietnam | China |
|---|---|---|
| Domestic steel grade variety | Moderate | Extensive |
| Specialty alloy availability | Often imported | Usually domestic |
| Lead time for imported material | 4–8 weeks | 1–3 weeks |
| Average fabricator experience level | Growing, variable | Deep, established |
| English communication capability | Moderate | Variable but more accessible via trading companies |
The Quality Management Gap
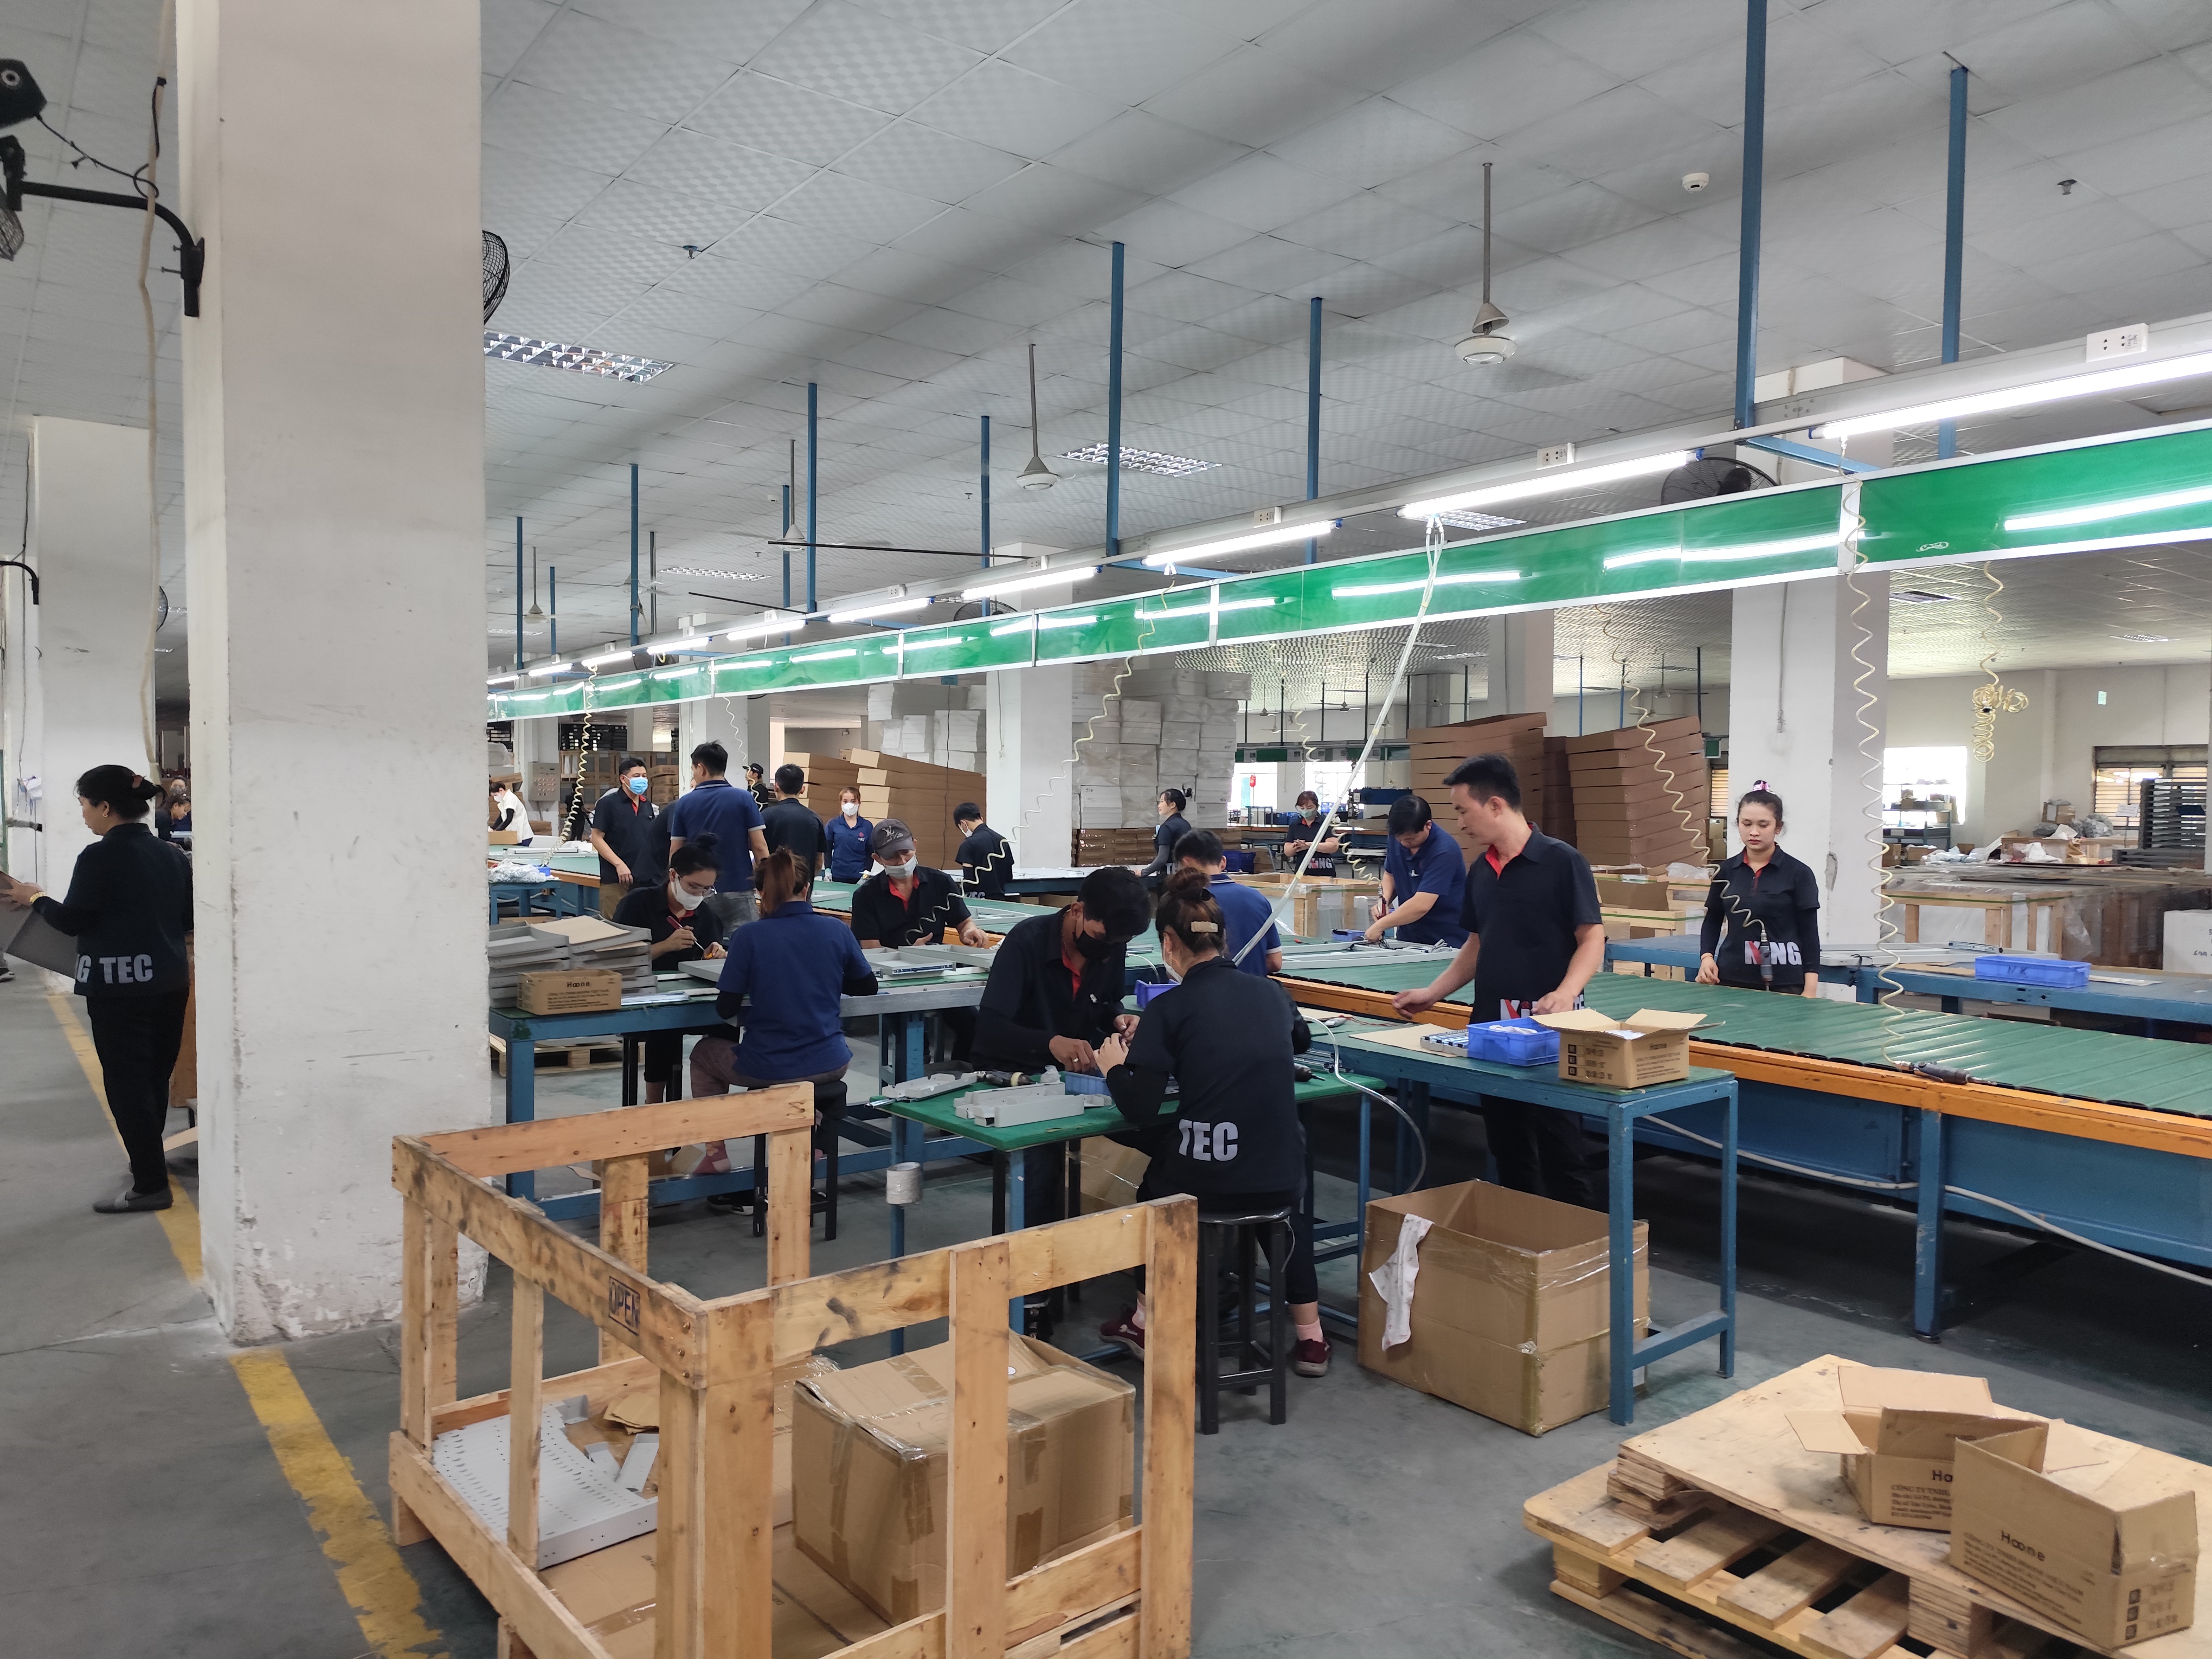
Many Vietnamese sheet metal shops are young. They have modern equipment — laser cutters, CNC press brakes, robotic welders — but their quality systems lag behind the hardware. I have walked through shops with million-dollar machines and no documented control plans. The equipment can hold tolerance. The system cannot guarantee it will, every time.
This is where our local team adds value. With seven employees on the ground in Vietnam, we conduct supplier audits, witness first-article inspections, and verify process controls before any production run ships. We function as an extension of the buyer's quality team, closing the gap between the buyer's expectations and the supplier's current systems.
Communication and Project Management
A communication breakdown is the fastest way to turn a good supplier into a bad experience. Language barriers are real. Technical English — drawing callouts, GD&T symbols, surface finish specifications — is specialized vocabulary. A misread note on a drawing can mean the difference between a countersunk hole and a counterbored hole.
We mitigate this by serving as the technical bridge. Our engineers review every drawing with the Vietnamese fabricator, confirm critical requirements in Vietnamese, and document agreements in bilingual reports. This extra step costs time upfront but eliminates rework downstream.
What Vietnam Does Well
Despite these risks, Vietnam offers genuine advantages for the right projects:
- Cost optimization strategies: Labor and overhead costs remain 15–30% lower than coastal China for comparable work.
- Production capacity growth: New factories are opening with modern equipment and younger, trainable workforces.
- Trade policy benefits: Vietnam's free trade agreements with the EU and other markets offer tariff advantages.
- Geopolitical diversification: For buyers managing China-related supply chain risk, Vietnam provides a credible alternative.
The key is to enter with eyes open. Vietnam is not a drop-in replacement for China. It is a complementary source that requires more hands-on management — at least until the supplier matures. If you are sourcing sheet metal fabrication for the first time, understanding these regional differences is especially important.
How can I secure flexible payment terms while maintaining high quality standards for my custom parts?
One of the most honest conversations I have with new clients happens around payment terms. A purchasing manager in the U.S. recently told me: "Every supplier in Asia wants 100% payment before shipment. But I need 60-day terms to manage my cash flow. And the last supplier I gave open terms to delivered garbage."
To secure flexible payment terms without sacrificing quality, work with suppliers who have established trust-building frameworks — such as starting with smaller orders on standard terms, graduating to open account terms as quality is proven, and selecting partners with formal PPAP and inspection protocols that ensure accountability.
Why Payment Terms and Quality Are Linked
This connection is not obvious, but it is real. When a buyer pays 100% upfront, the supplier's financial incentive to deliver on time and on spec drops. The money is already in the bank. Conversely, when a buyer demands 90-day terms from a small supplier, that supplier may cut corners on material or skip inspection steps to conserve cash.
The healthiest arrangement balances risk for both sides.
A Graduated Approach to Terms
At DEWIN, we use a staged model. It works like this:
| Stage | Order Size | Payment Terms | Quality Gate |
|---|---|---|---|
| Trial order | Small batch (50–200 pcs) | 30% deposit, 70% before shipment | Full PPAP and first-article inspection |
| Second order | Medium batch | 30% deposit, 70% net 30 | In-process and final inspection reports |
| Ongoing production | Full production volumes | Open account, net 60–90 | Ongoing SPC data and periodic audits |
This model lets the buyer verify quality before extending credit. It also lets the supplier demonstrate capability before absorbing financial risk.
The Role of Process Controls in Earning Trust
Payment flexibility is earned, not given. A supplier earns it by proving their processes are reliable. That means PPAP documentation 9, process control plans, calibrated measurement equipment, and inspection records that are traceable.
Our clients in the U.S. and Europe tell us that the ability to offer 60–90 day open account terms — backed by documented quality systems — is a key differentiator. It solves their cash flow problem without creating a quality problem.
Design for Manufacturability as a Cost Lever
There is another angle here that procurement managers sometimes miss. When we conduct a design for manufacturability review early in the project, we often find ways to simplify the part. Fewer bends. Standard hole sizes. Relaxed non-critical tolerances. These changes reduce the fabrication cost, which makes the overall program more financially viable — and makes flexible terms sustainable for everyone.
Cost optimization strategies are not just about negotiating the price down. They are about engineering the cost out of the part before production begins.
Conclusion
Sheet metal fabrication procurement success comes down to choosing the right partner — not the cheapest quote. Define your critical tolerances, verify supplier capabilities, manage material risks, and build payment terms around proven quality performance.
Frequently Asked Questions
How can I ensure my supplier doesn't overlook critical tolerances in my sheet metal drawings?
A lesson we learned early at DEWIN: a U.S. client sent us a drawing with every single dimension held to ±0.05 mm. The part was a simple mounting bracket. No feature on it required that level of precision, yet the previous supplier had quoted it at face value — and still delivered parts out of spec.
Why am I experiencing frequent delivery delays and quality issues with my current sheet metal source?
Last quarter, a client came to us after their existing supplier missed three consecutive shipments. The root cause was not capacity. It was a communication breakdown: the supplier had changed raw material grades without informing the buyer, causing weld failures that triggered rework loops.
What are the hidden risks I should watch for when sourcing sheet metal parts from Vietnam?
When we opened our Vietnam office seven years ago, we saw the opportunity clearly — competitive labor costs, a growing manufacturing base, and geographic diversification away from China. But we also discovered risks that do not show up on a quote sheet.
Footnotes
1. Provides insights into sourcing and procurement strategies for sheet metal fabrication. ↩︎
2. Explains the fundamentals and best practices of quality control in manufacturing. ↩︎
3. Clearly defines and illustrates the 4T rule for sheet metal bending design. ↩︎
4. Explains the steps and importance of a Design for Manufacturability (DFM) review. ↩︎
5. Describes the purpose and typical contents of a First Article Inspection Report (FAIR). ↩︎
6. Outlines the seven fundamental principles of quality management. ↩︎
7. Provides an official overview of the ISO 9001 quality management system standard. ↩︎
8. Details the properties, applications, and benefits of SUS 316L stainless steel. ↩︎
9. Provides a comprehensive overview of the Production Part Approval Process (PPAP) documentation. ↩︎