

When our engineering team reviews drawings from U.S. clients, one overlooked detail causes more rework than almost anything else: surface roughness requirements 1 on sheet metal fabrication parts.
Surface roughness requirements for sheet metal fabrication depend on part function: 6.3 µm Ra for clearance surfaces, 3.2 µm Ra for structural brackets, 1.6 µm Ra for mating or press-fit parts, and 0.8 µm Ra or finer for sealing or bearing applications. Specifying mill finishes or grit levels is often more practical for aesthetic parts.
Getting these specifications wrong creates a chain reaction. Parts arrive too rough for a proper seal, or too smooth for powder coating adhesion, or finished to an unnecessary standard that inflates your cost. Below, I will walk through the key decisions you need to make before placing your next order.
How do I determine the correct Ra value for my custom sheet metal parts?
A lesson we learned early in our supply chain work: many purchasing managers copy Ra value 2s from machined part drawings and paste them onto sheet metal drawings without questioning whether that Ra value is even achievable or necessary.
To determine the correct Ra value, first classify each surface by function — clearance, structural, mating, or sealing. Clearance surfaces need 6.3 µm Ra, structural faces need 3.2 µm Ra, mating surfaces need 1.6 µm Ra, and high-pressure seals require 0.8 µm Ra or finer.

Start With Function, Not Habit
The biggest mistake I see is over-specification. A structural bracket that bolts to a frame does not need the same surface finish as an O-ring groove. Yet I have reviewed drawings where every surface was called out at 1.6 µm Ra, which forced the supplier into secondary grinding operations. That added cost and delayed delivery by a week.
Here is a simple decision framework. Ask yourself: does this surface seal against another part? Does it slide or rotate against another surface? Does it need to resist corrosion without coating? Does it need to look good? Your answers determine whether you need an Ra value, a grit specification, or a mill finish.
Ra Value Reference Table by Application
| Application | Recommended Ra (µm) | Ra (µin) | Typical Process |
|---|---|---|---|
| Clearance surfaces (no contact) | 6.3 | 250 | Standard sheet metal fabrication 3 |
| Structural brackets, non-mating faces | 3.2 | 125 | Laser cutting, standard finishing |
| Mating parts, press-fits, O-ring grooves | 1.6 | 63 | Fine machining or controlled finishing |
| High-pressure fluid seals | 0.8 | 32 | Precision grinding |
| High-load bearings, optical housings | 0.4 | 16 | Lapping, superfinishing |
When Ra Is the Wrong Metric
For many sheet metal parts, Ra is not the best way to communicate what you want. If your goal is a consistent brushed aesthetic appearance on a stainless steel enclosure, specifying a #4 finish or 150 grit is far more practical. Mill finishes 4 like 2B (bright cold-rolled) or BA (bright annealed) are tied directly to the source material and are easier for a supplier to control.
I have seen cases where a client specified 0.8 µm Ra on a decorative panel. The supplier achieved it through extra polishing — and the cost doubled. A simple #4 brushed finish would have met the client's actual need at a fraction of the price. Material surface texture should guide your specification language.
When friction and wear are concerns — say, a sliding interface between two metal parts — then Ra is the right metric. When you just want the panel to look clean and uniform, grit or mill finish is the right metric.
How can I verify that my supplier's QC process matches my surface roughness specifications?
One of our clients in the Midwest shipped back an entire batch of mounting brackets because the surface finish did not match the drawing. The supplier had no record of ever checking it. That experience reinforced something we enforce on every project: if you cannot measure it, you cannot control it.
To verify your supplier's QC process, request their quality inspection procedure for surface roughness — including the instrument type (contact profilometer or non-contact sensor), calibration records, sampling plan, and acceptance criteria. Ask for first article inspection reports with actual Ra or Rz readings before approving production.

The Tools That Matter
Surface roughness is measured with a profilometer. A contact-type profilometer 5 drags a stylus across the surface and records the peaks and valleys. The instrument then calculates the Ra value (the arithmetic average of those deviations) and the Rz value (the average maximum peak-to-valley height over a set of sampling lengths).
For quick shop-floor checks, handheld profilometers are common and affordable. For formal quality inspection, a benchtop profilometer with traceable calibration is the standard. Some advanced fabricators now use non-contact optical sensors for in-process monitoring, which allows real-time adjustments during production.
What to Ask Your Supplier
Here is a checklist I use when auditing a sheet metal supplier's surface finish capability:
- Instrument type and model: Do they own a profilometer measurement device, or do they outsource testing?
- Calibration schedule: Is the instrument calibrated to a traceable standard? How often?
- Sampling plan: How many parts per batch are checked? Which surfaces are measured?
- Acceptance criteria: Is the pass/fail threshold clearly defined in their work instructions?
- Records: Can they provide test reports with actual Ra and Rz data?
If a supplier cannot answer these questions clearly, that is a red flag. In our experience managing suppliers across Vietnam and other Asian sourcing markets, we have found that the suppliers who invest in proper measurement equipment are the same ones who deliver right first time.
Surface Finish Comparator Plates
For a fast, low-cost reference, surface finish comparator plates 6 (sometimes called Rupert plates) are useful. These are small metal plates with sections machined to known Ra values. You hold one next to your part and compare by touch and sight. They are not a substitute for profilometer measurement, but they help purchasing managers and inspectors develop a feel for different finishes.
Beyond Ra: Waviness and Lay
For highly sensitive applications, Ra alone does not tell the whole story. Waviness describes longer-wavelength undulations on the surface — think of gentle waves versus sharp scratches. Lay describes the direction of the dominant surface pattern (e.g., parallel lines from a grinding wheel). Both waviness and lay can affect how a gasket seats, how a coating adheres, or how two surfaces mate under load. If your application is sensitive to these factors, specify them on your drawing.
Will choosing a finer surface finish impact my project budget and delivery schedule?
A trade-off we weigh on nearly every project: how smooth does this surface really need to be, and what will that cost? The answer is almost always "smoother costs more and takes longer," but the magnitude of that jump varies dramatically depending on where you are on the Ra scale.
Yes, finer surface finishes directly increase both cost and lead time. Moving from 3.2 µm Ra to 1.6 µm Ra adds moderate cost, but jumping to 0.8 µm or 0.4 µm Ra can double or triple finishing costs because it requires precision grinding or lapping operations that are not standard in sheet metal fabrication.
The Cost Curve Is Not Linear
The relationship between surface roughness and cost is exponential, not linear. Standard sheet metal fabrication processes — laser cutting, punching, bending — produce surfaces in the 3.2–6.3 µm Ra range naturally. Achieving anything finer requires additional operations.
| Ra Value (µm) | Relative Cost | Additional Process Required | Impact on Lead Time |
|---|---|---|---|
| 6.3 | Baseline (1x) | None — standard fabrication | None |
| 3.2 | 1.0–1.2x | Light deburring or standard finishing | Minimal |
| 1.6 | 1.3–1.5x | Fine grinding or controlled sanding | +1–2 days |
| 0.8 | 2.0–2.5x | Precision grinding | +3–5 days |
| 0.4 | 3.0–4.0x | Lapping or superfinishing | +5–10 days |
These multipliers are approximate, but they reflect the pattern I have seen across dozens of sourcing projects. The jump from 1.6 µm to 0.8 µm is where costs spike, because you move from standard shop capabilities into specialized equipment.
Where the Budget Really Gets Hit
It is not just the finishing operation itself. Finer finishes require tighter dimensional tolerances in upstream processes. A part that needs 0.8 µm Ra on a mating face may also need tighter flatness control on the blank before grinding. That ripples back through the entire process chain.
Additionally, inspection time increases. Checking Ra on every part with a profilometer takes time. If only 1 in 10 parts needs checking at 3.2 µm Ra, your supplier might need to check every part at 0.4 µm Ra because the process window is so tight.
Coating Interactions
Here is something many engineers miss: if your part will be powder coated or painted, an overly smooth surface can actually hurt you. Paint and powder coating adhere best to surfaces with some tooth — typically in the 3.2–6.3 µm Ra range. A mirror-polished surface may cause the coating to peel or show every minor imperfection underneath (a defect called "telegraphing").
So before specifying a fine finish, ask whether the part will receive a secondary coating. If it will, you may save money and get a better result by leaving the surface at its natural roughness. For a deeper look at how different coatings interact with substrate preparation, see our guide on the best surface treatment options for sheet metal fabrication.
| Coating Type | Optimal Ra Range (µm) | Why |
|---|---|---|
| Powder coating | 3.2–6.3 | Needs mechanical tooth for adhesion |
| Wet paint | 1.6–3.2 | Moderate roughness hides imperfections |
| Anodizing (aluminum) | 0.8–1.6 | Smoother substrate = better anodized finish |
| Electroplating | 0.4–1.6 | Surface defects replicate through plating |
This table is a practical guide we share with clients during the co-development phase. It prevents unnecessary spending on finishes that will be covered up anyway.
What role does surface roughness play in the long-term durability of my fabricated components?
During a recent project review, a client asked us why their brackets were showing early signs of corrosion at the bend lines. The root cause was not the material or the coating — it was the surface roughness at the bend radius. Micro-cracks and roughened grain boundaries created initiation points for corrosion.
Surface roughness directly affects long-term durability by influencing corrosion resistance, fatigue life, friction and wear, and coating adhesion. Rougher surfaces trap moisture and contaminants that accelerate corrosion, while smoother surfaces reduce stress concentrators that can initiate fatigue cracks under cyclic loading.
Corrosion Resistance and Surface Texture
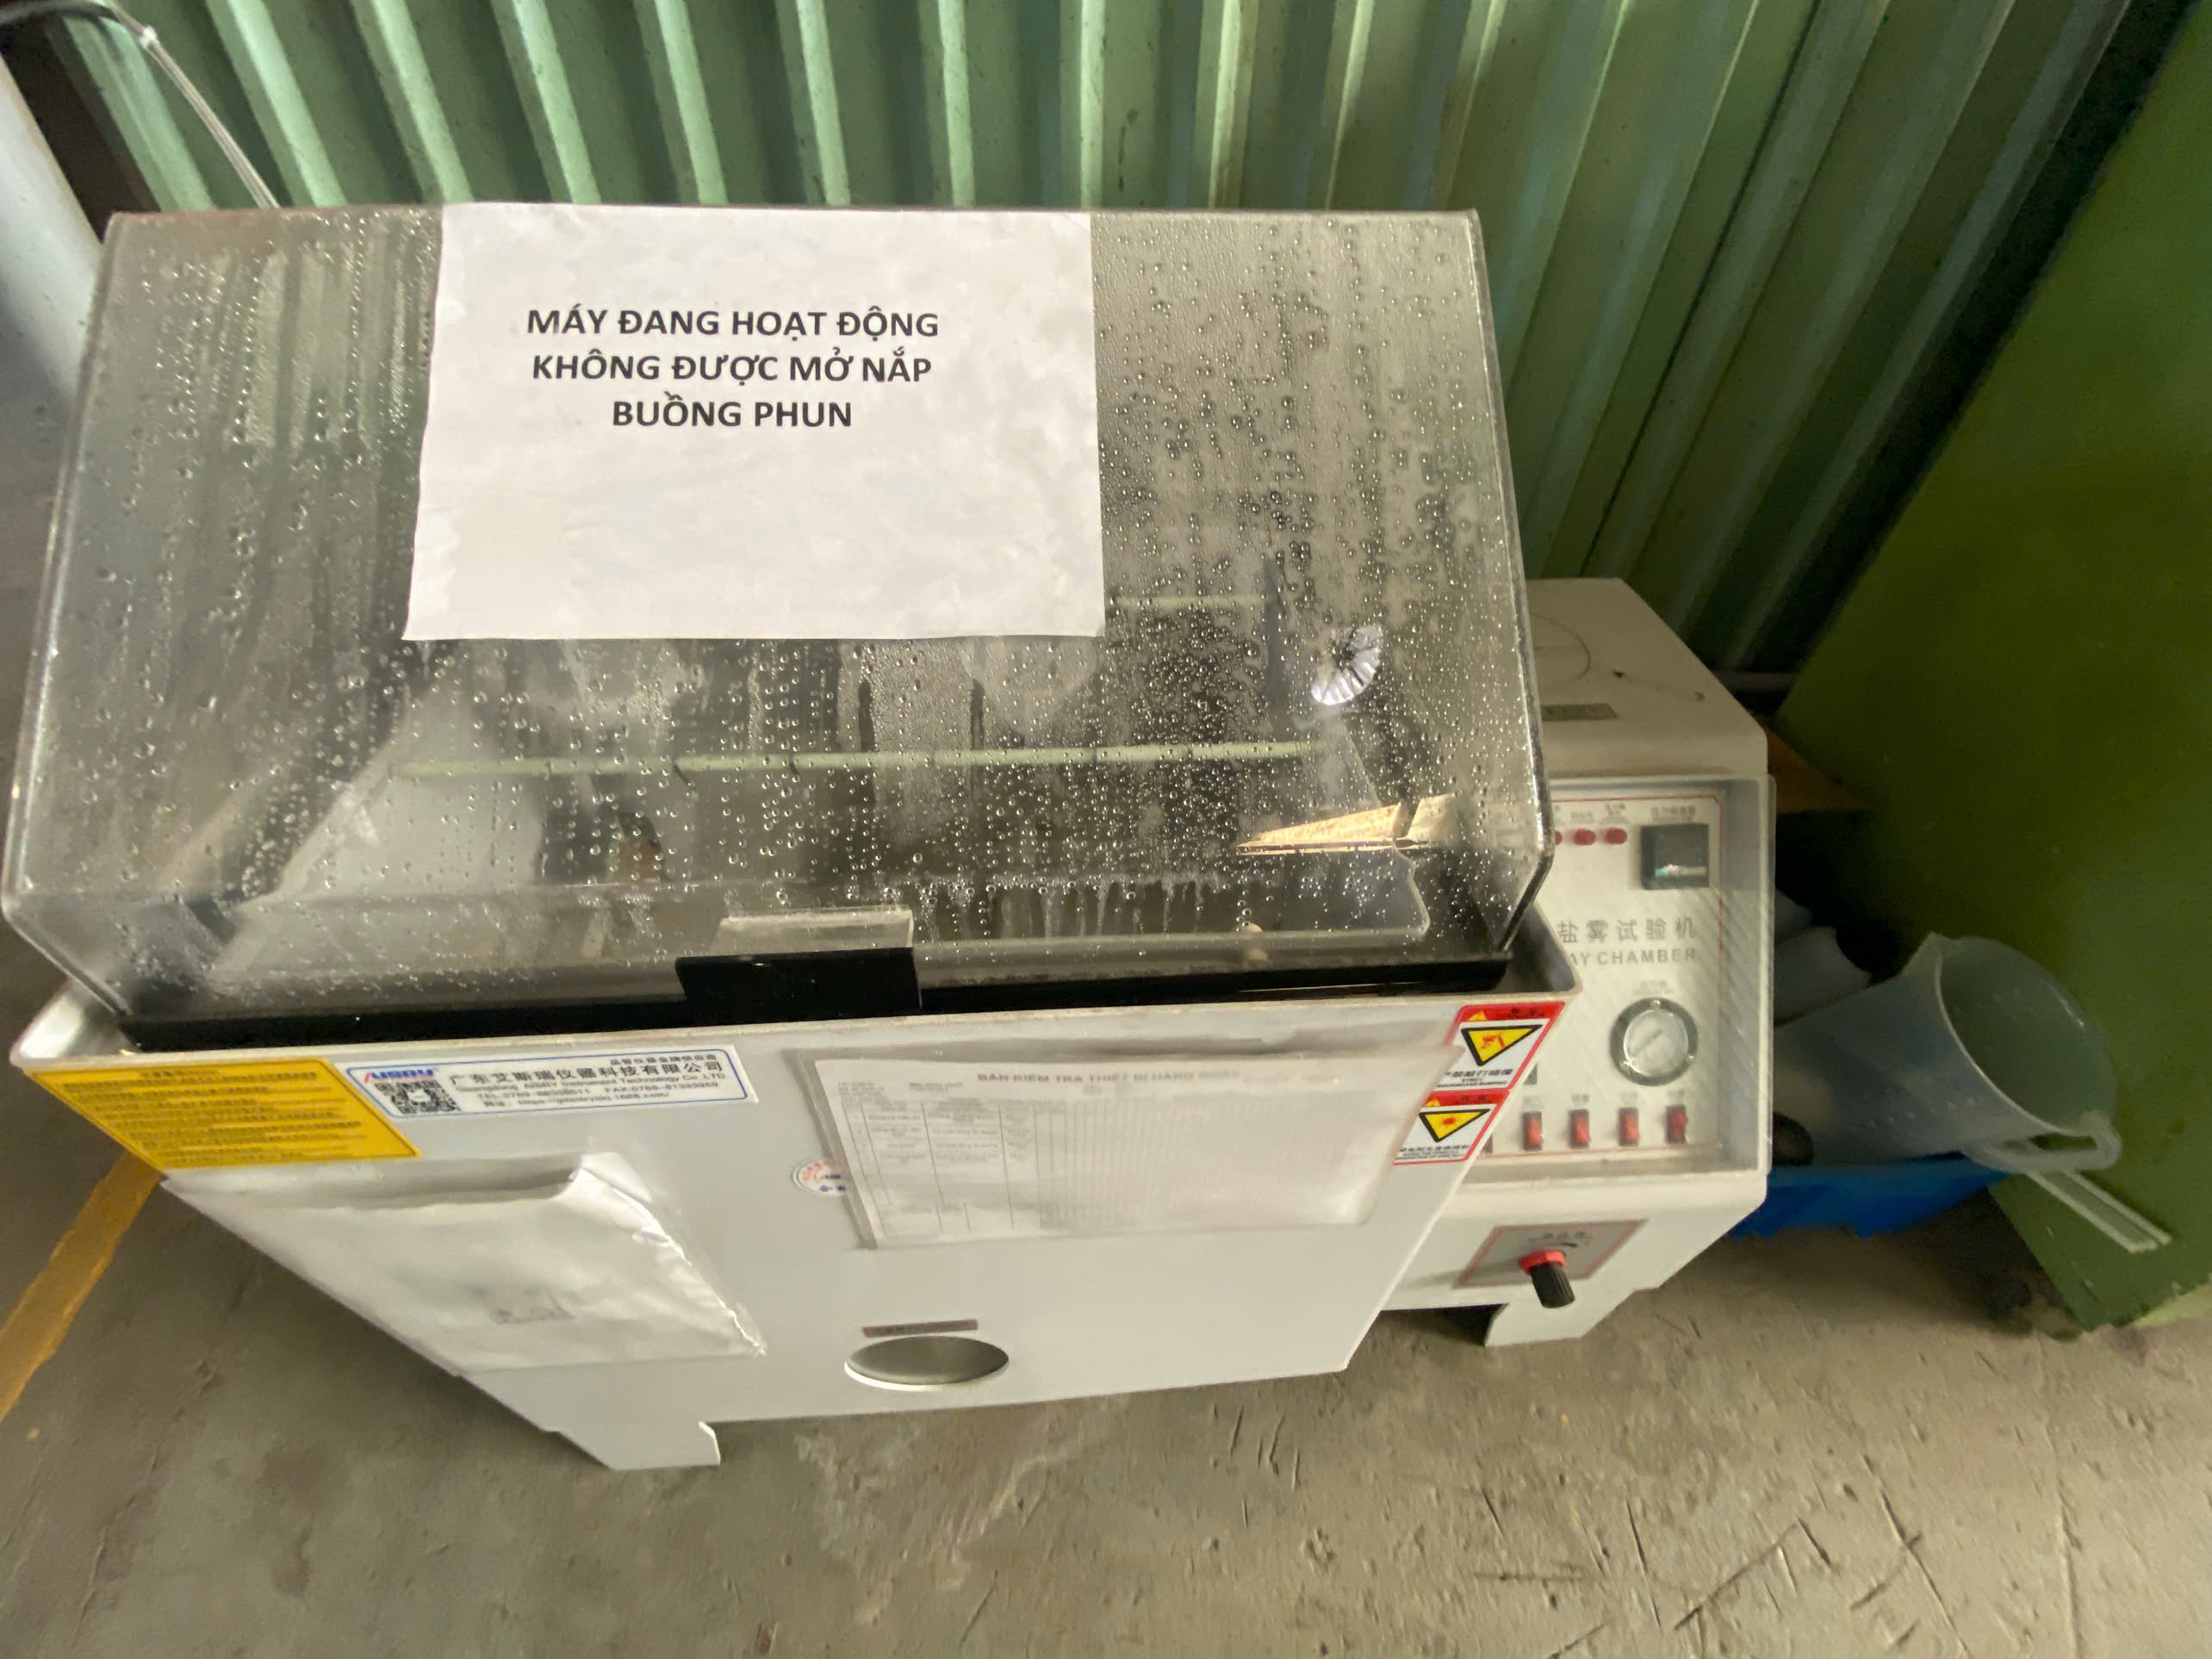
A rough surface has more peaks and valleys. Those valleys trap moisture, salt, and other corrosive agents. Even on stainless steel, a rough surface corrodes faster than a smooth one because the passive oxide layer is thinner and less uniform at the valley bottoms.
For components exposed to outdoor environments, marine atmospheres, or chemical processing, specifying a smoother finish on critical surfaces extends service life measurably. In the food and medical industries, surface finish standards often mandate specific Ra values (typically below 0.8 µm Ra) to ensure cleanability and prevent bacterial growth in micro-crevices.
Fatigue Life
Every scratch, groove, and valley on a metal surface is a potential stress concentrator. Under cyclic loading — vibration, repeated flexing, pressure cycling — cracks tend to initiate at the roughest points on the surface. A smoother surface means fewer and smaller stress concentrators, which translates to longer fatigue life 7.
This is why aerospace and automotive structural components often require tighter surface finish standards than general industrial parts. The investment in a smoother finish pays for itself in extended service intervals and reduced field failures.
Friction, Wear, and Mating Surfaces
When two metal surfaces slide or press against each other, surface roughness controls the real contact area. Rough surfaces touch only at their peaks, concentrating load on a tiny fraction of the nominal area. This causes higher local stress, faster wear, and more friction.
For press-fit joints, O-ring grooves, and sliding interfaces, controlling Ra ensures predictable friction and wear behavior. Too rough and the O-ring wears prematurely. Too smooth and the press-fit may not hold because there is not enough mechanical interlock.
A Practical Durability Checklist
When I assess whether a part needs a durability-driven surface finish, I ask five questions:
- Is the part exposed to moisture, chemicals, or salt spray?
- Will the part experience cyclic loading or vibration?
- Does the surface mate with another component under load?
- Will the surface receive a protective coating?
- Is the part in a cleanroom, food-contact, or medical environment?
If the answer to any of these is yes, surface roughness deserves careful specification — not just for appearance, but for the long-term performance of the component.
Conclusion
Surface roughness requirements for sheet metal fabrication are a balance of function, cost, and durability. Specify Ra for functional surfaces, use mill finish or grit for aesthetics, verify your supplier's QC process 9, and avoid over-specification to protect your budget and timeline. For a comprehensive overview of how these standards are defined and applied across the industry, explore our article on surface roughness standards for sheet metal fabrication. And if you are building a robust supplier qualification process, our guide on how to develop incoming inspection standards for sourcing sheet metal fabrication covers the full inspection framework.
Frequently Asked Questions
How do I determine the correct Ra value for my custom sheet metal parts?
A lesson we learned early in our supply chain work: many purchasing managers copy Ra value 2 s from machined part drawings and paste them onto sheet metal drawings without questioning whether that Ra value is even achievable or necessary.
How can I verify that my supplier's QC process matches my surface roughness specifications?
One of our clients in the Midwest shipped back an entire batch of mounting brackets because the surface finish did not match the drawing. The supplier had no record of ever checking it. That experience reinforced something we enforce on every project: if you cannot measure it, you cannot control it.
Will choosing a finer surface finish impact my project budget and delivery schedule?
A trade-off we weigh on nearly every project: how smooth does this surface really need to be, and what will that cost? The answer is almost always "smoother costs more and takes longer," but the magnitude of that jump varies dramatically depending on where you are on the Ra scale.
Footnotes
1. Explains ISO standard for surface roughness measurement methodology and terminology. ↩︎
2. Defines Ra (Roughness Average) as a critical parameter in surface roughness measurement. ↩︎
3. Provides a comprehensive overview of the sheet metal fabrication process and methods. ↩︎
4. Details various mill finishes for stainless steel and their production processes. ↩︎
5. Explains the working principle, applications, and strengths of contact profilometry. ↩︎
6. Describes surface profile comparators for quick visual and tactile assessment of roughness. ↩︎
7. Replaced HTTP unknown with an authoritative academic article (PMC) on the effect of surface roughness on fatigue life. ↩︎
8. Discusses how surface finishing and roughness significantly impact a material’s corrosion resistance. ↩︎
9. Emphasizes the importance of surface roughness measurement in the quality control process. ↩︎