
Outdoor aluminum components face severe environmental degradation from UV exposure and coastal salt air. Choosing the wrong surface treatment leads to premature field failures, bubbling, and corrosion. We guide you through selecting the optimal Vietnamese finish.
Anodizing aluminum creates an electrochemical oxide layer that excels in high-UV and wear-intensive environments, whereas powder coating applies an organic polymer resin barrier that provides superior chemical resistance and unlimited custom color options for outdoor structural applications.
Key takeaways:
- Anodizing preserves the natural metallic texture of aluminum and prevents sub-film corrosion, making it ideal for high-wear coastal hardware.
- Powder coating provides a thick polymer barrier with exceptional color options, utilizing AAMA 2605 specifications for long-term architectural durability.
- Proper chemical pre-treatment, including chromate-free conversion coating, is mandatory for maximum powder coat adhesion.
- Vietnamese manufacturers offer advanced surface finishing capabilities backed by tariff-free imports to the US and extensive trade networks.
How do anodizing and powder coating compare in outdoor corrosion resistance?
Our quality engineers analyze outdoor corrosion performance daily. We evaluate how electrochemical oxides and polymer barriers withstand coastal environments under accelerated testing standards.
Anodizing provides superior resistance to ultraviolet degradation and prevents exfoliation corrosion by forming an integral oxide layer, whereas powder coating offers a thick physical barrier that protects aluminum from aggressive chemical exposure and harsh environmental soils.
Defining Anodizing and Powder Coating
Anodizing is an electrochemical process that converts the aluminum substrate surface into a durable, corrosion-resistant anodic oxide finish. Powder coating is a dry finishing process where electrostatically charged polymer resins are sprayed onto a grounded metal part and cured under heat to form a protective skin.
Anodized finishes excel in sunny environments. Because the anodic layer is integrated with the underlying aluminum, it cannot peel or flake. However, high-salinity coastal environments can attack the thin oxide layer if it is not sealed properly during manufacturing.
Conversely, powder coating relies on a physical barrier. If this barrier is breached by a scratch, moisture can migrate underneath, causing filiform corrosion. Therefore, outdoor architectural components often utilize AAMA 2605 compliant powder coatings to achieve multi-decade weatherability. To ensure long-term outdoor survival, Western buyers should request detailed salt spray testing reports (ASTM B117) from Vietnamese suppliers before finalizing surface finish specifications for coastal hardware.
Our network includes aluminum extrusion and casting experts. For example, Lixil Global Manufacturing Viet Nam is a verified aluminum extrusion manufacturer in Vietnam with 31 factory photos on file, providing integrated extrusion and anodizing capabilities.
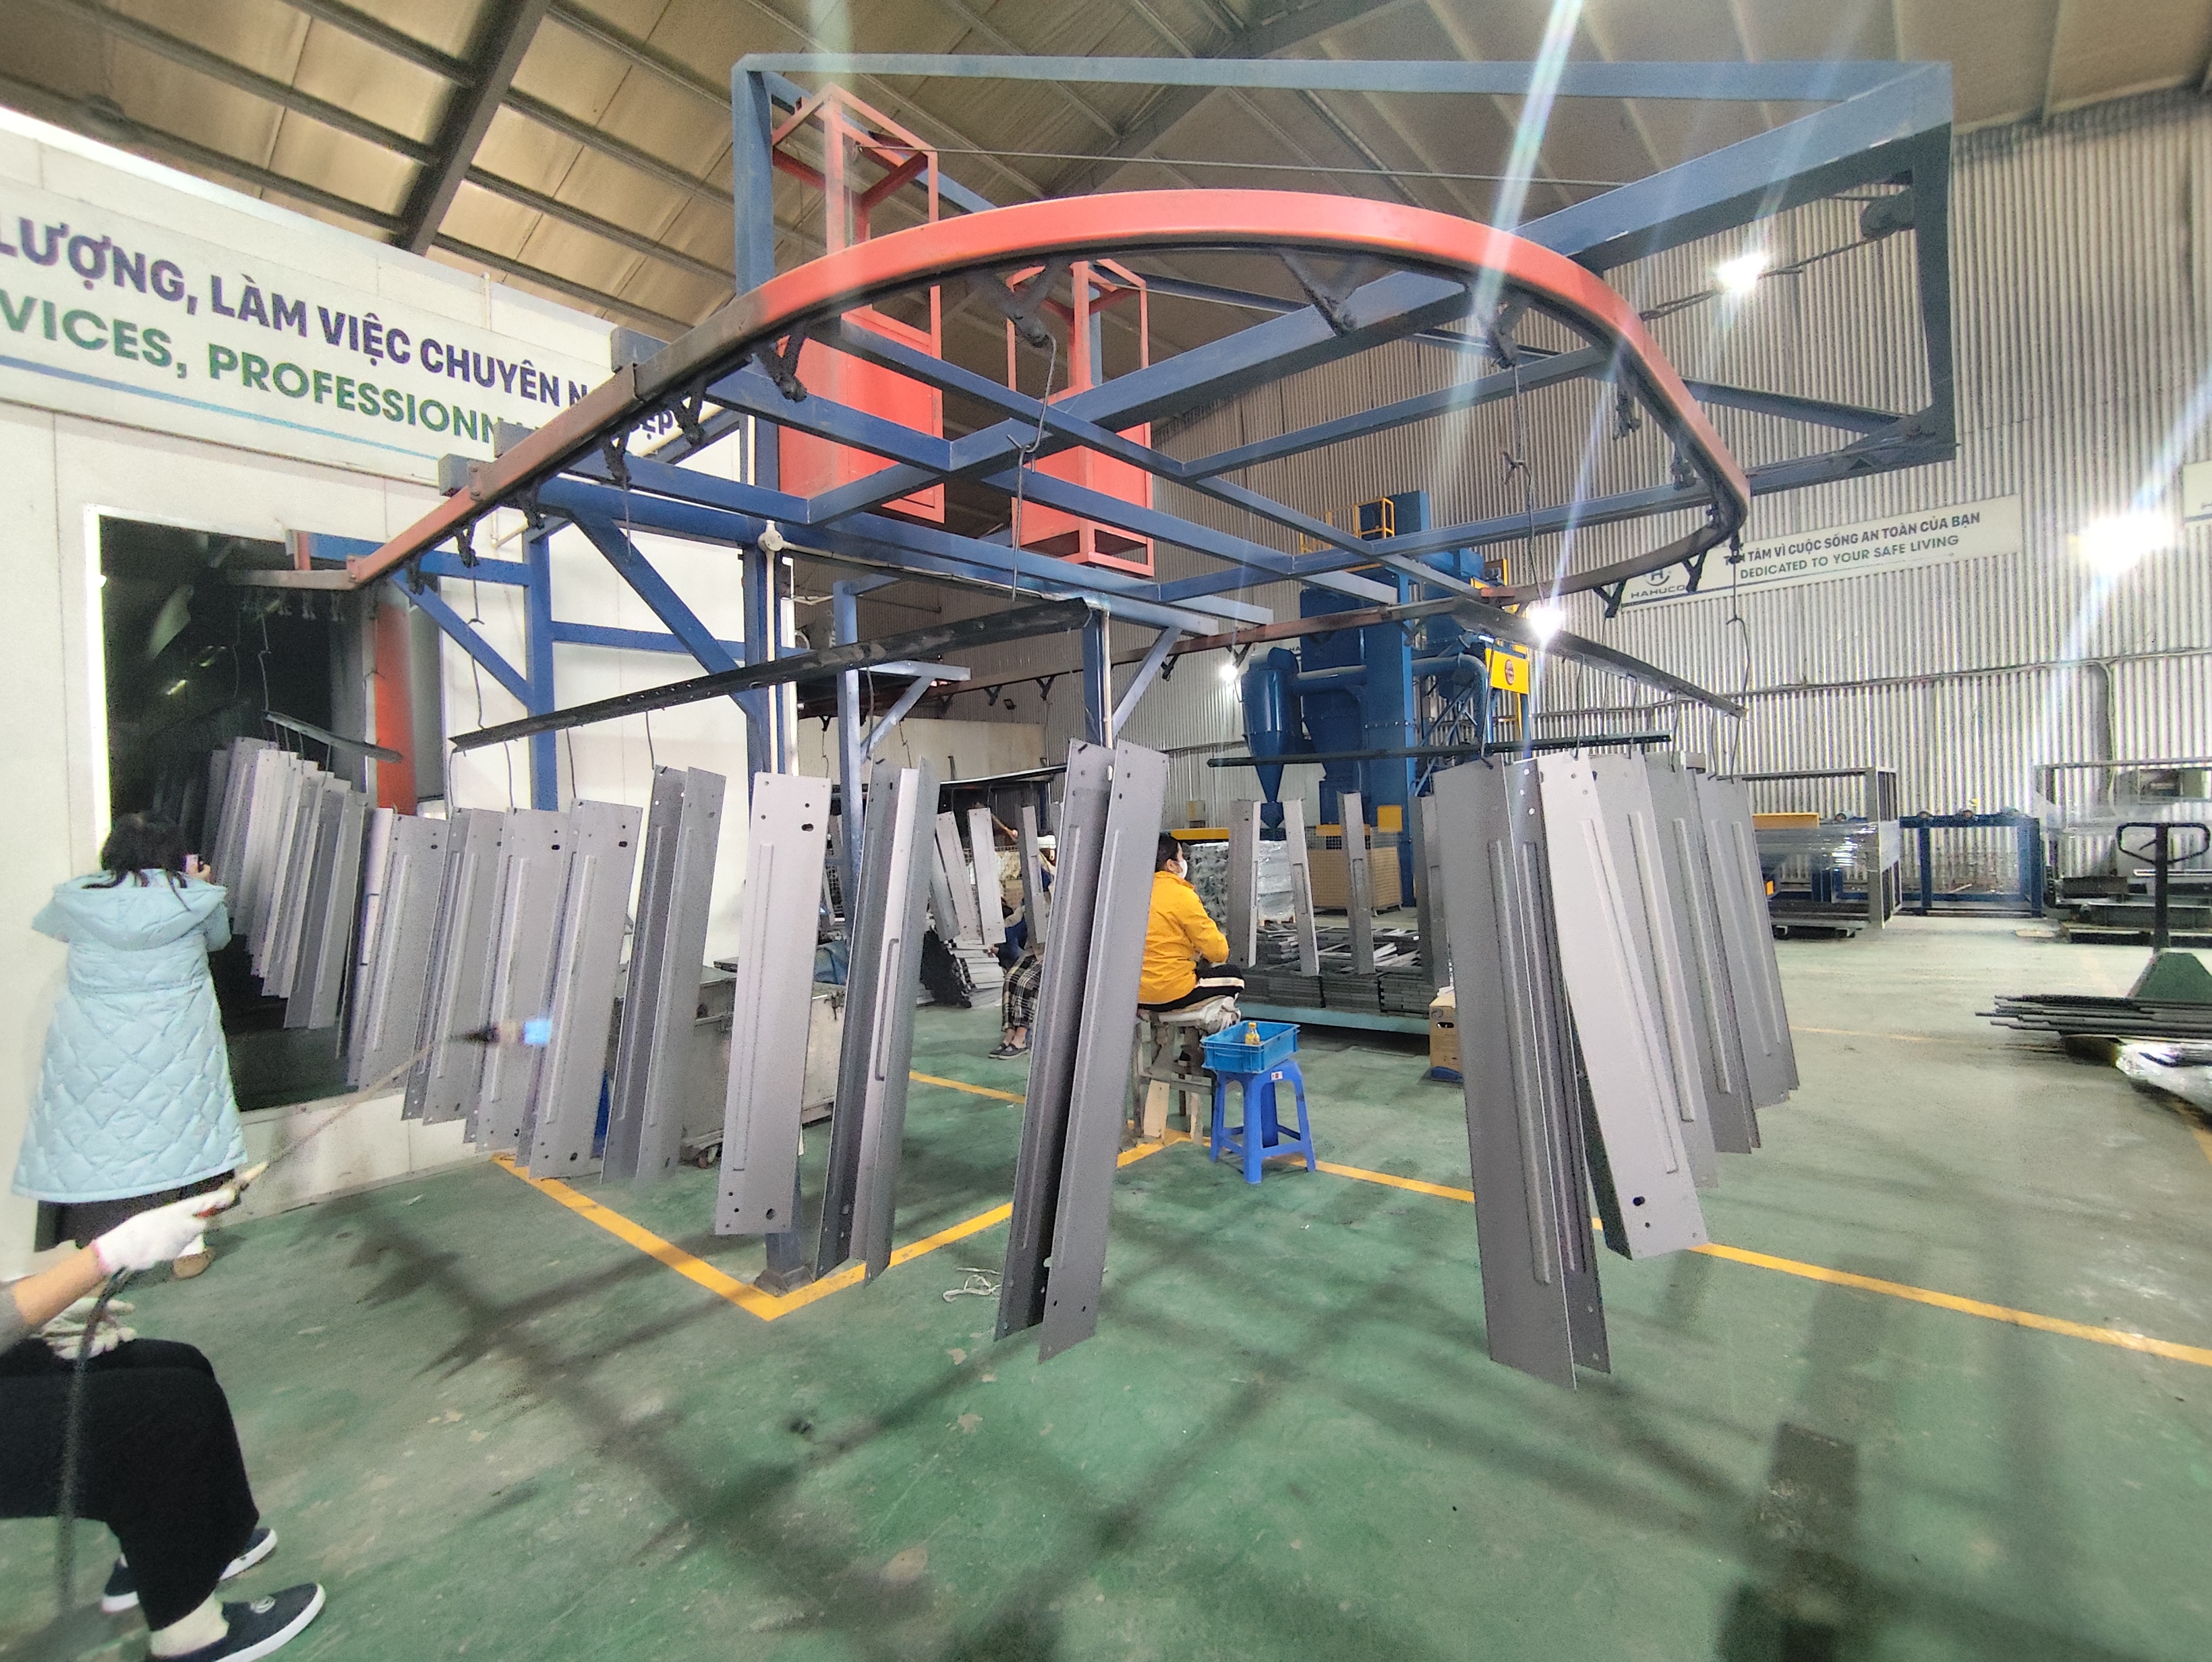
Which finish offers better cost efficiency for high-volume aluminum manufacturing?
We evaluate the total cost of ownership for Western buyers. We analyze chemical line operating costs, material scrap rates, and labor inputs across high-volume production runs.
Powder coating typically offers better cost efficiency for high-volume production due to lower energy consumption, faster cycle times, and minimal hazardous waste disposal compared to the multi-stage chemical baths required for hard-coat anodizing.
Total Sourcing Cost Drivers
When sourcing from the Vietnam supplier database, unit cost is driven by capital equipment depreciation, chemical consumption, and energy use. Powder coating typically requires lower energy consumption during application compared to the chemical baths required for hard-coat anodizing. Anodizing lines require substantial electrical power to maintain low temperatures in the sulfuric acid tanks, driving up operational overhead.
Furthermore, powder coating allows for high material recovery. Over-sprayed powder can be reclaimed and reused, resulting in material utilization rates exceeding 95%. Hard anodizing, by contrast, relies on consumable chemical solutions that require strict waste-water treatment protocols before disposal.
However, anodizing preserves the original metallic appearance and texture of aluminum parts better than opaque powder coatings. For high-volume consumer-facing hardware, the aesthetic value of anodizing may justify the cost premium. Below is a cost-to-performance breakdown:
| Metric | Hard-Coat Anodizing | Standard Powder Coating |
|---|---|---|
| Relative Tooling & Setup Cost | Medium-High | Low-Medium |
| Energy Consumption | Very High | Medium |
| Material Waste Rate | 10% to 15% (baths) | < 5% (with reclamation) |
| Line Cycle Time | Long (multi-bath dipping) | Short (continuous spray & cure) |
Western buyers can leverage DEWIN’s instant quoting portal to evaluate these trade-offs early in the design cycle.
How do I verify surface treatment quality when sourcing from Vietnamese suppliers?
Our on-ground audit engineers verify finishing quality weekly. We inspect chemical concentration logs, adhesion test records, and dry film thickness measurements directly on the factory floor.
Sourcing teams verify surface treatment quality in Vietnam by performing cross-hatch adhesion tests, dry film thickness measurements, and auditing chemical bath maintenance protocols to ensure consistent coating performance on finished aluminum components.
Auditing the Production Line
Sourcing teams ought to audit a manufacturer’s chemical bath maintenance protocols, as process control in anodizing impacts corrosion life more than the alloy composition itself. When we execute our 50-point Dolphin Audit, we inspect chemical titration logs, bath temperature controls, and rinsing step frequencies. For powder coating, chemical pre-treatment, such as chromate-free conversion coating, is critical for achieving proper powder coat adhesion on extruded aluminum. Without a properly controlled pre-treatment line, even high-quality powder resins will peel off within months of outdoor exposure.
We recommend specifying a strict Quality Control Plan (QCP) that mandates standardized testing protocols. For powder coating, the ASTM D3359 cross-hatch tape test must show zero paint lift. For anodizing, the coating thickness should be verified using eddy-current instruments according to ASTM B244.
Many of our vetted Vietnamese manufacturing facilities have advanced QA equipment. For example, Tho Thanh Phat Die-Casting Company is a verified aluminum die-casting manufacturer with 158 factory photos, listing a 3D CMM and dedicated CNC milling machines on file, ensuring mechanical and dimensional precision before surface application.
| Verification Test | Target Specification | Standard Reference |
|---|---|---|
| Coating Thickness | Class I Anodized: 18µm+ / Powder: 60-80µm | ASTM B244 / ISO 2360 |
| Adhesion Strength | 5B Rating (Zero paint lift) | ASTM D3359 |
| Specular Gloss | Customer specified tolerance | ASTM D523 |
| UV Resistance | No chalking or color shift | AAMA 2605 / ISO 11507 |
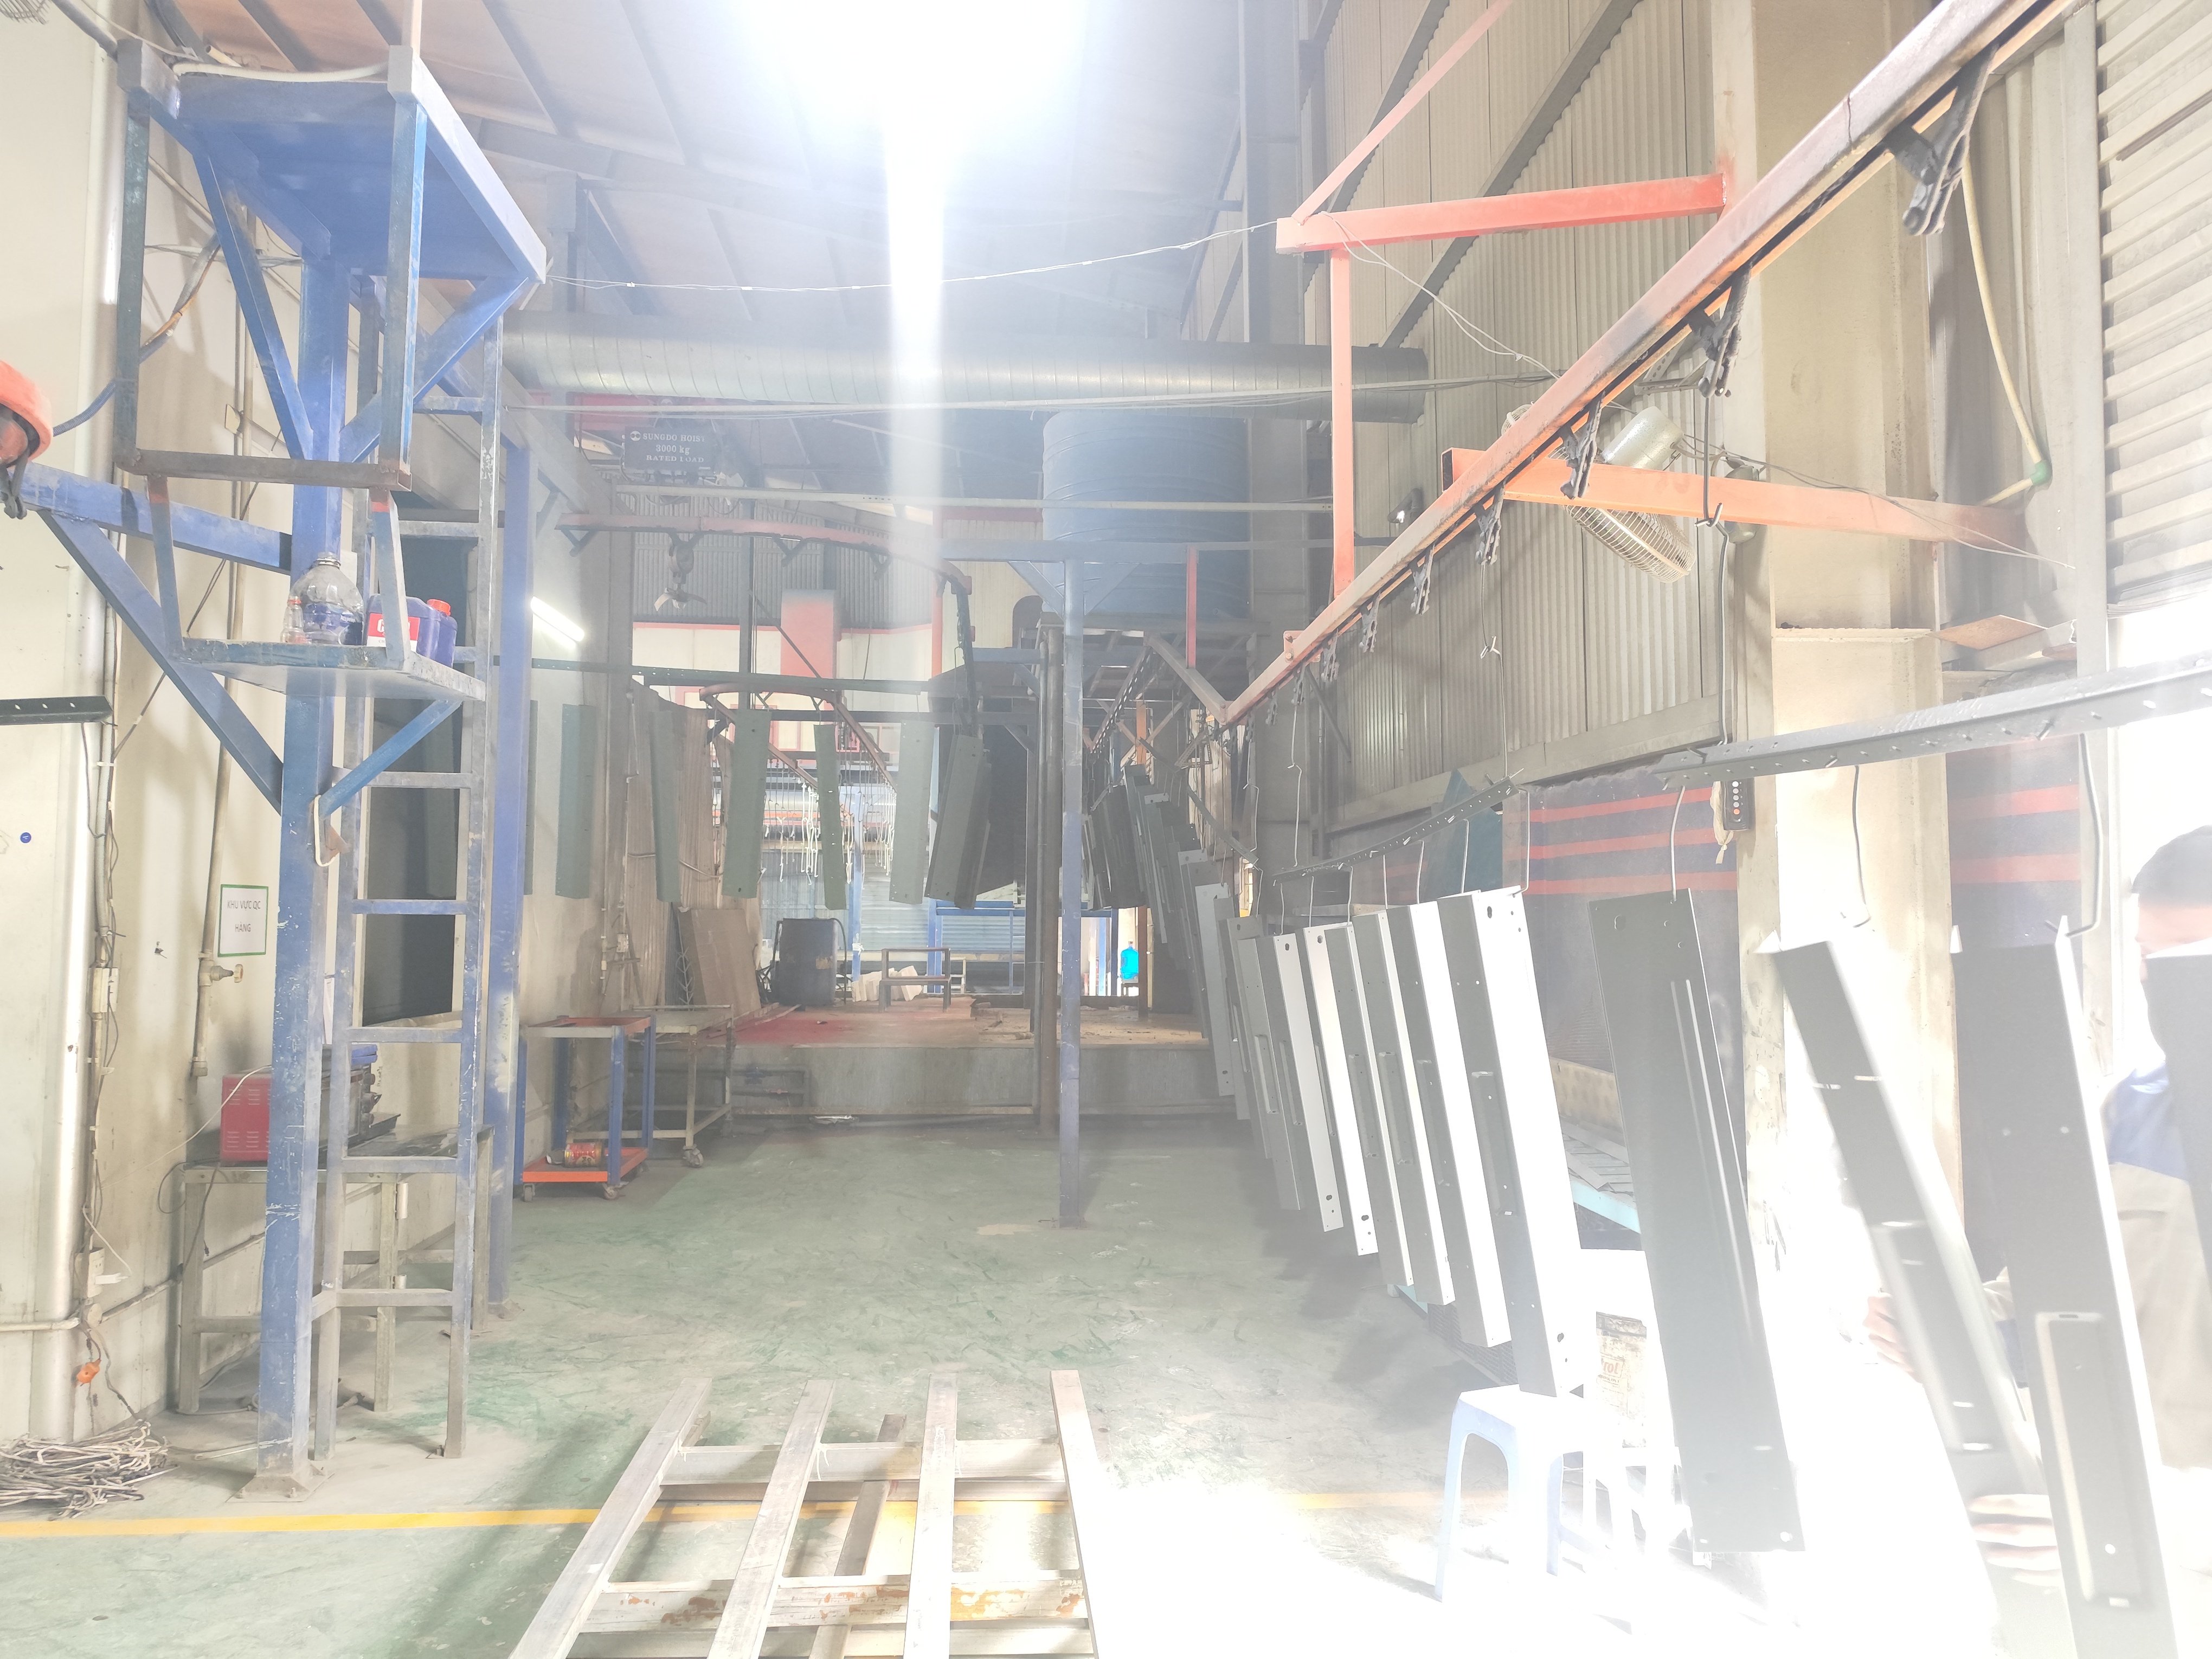
What environmental compliance standards apply to aluminum finishing processes in Asia?
We help Western brands navigate complex environmental regulations. We monitor wastewater treatment, volatile organic compound emissions, and global chemical compliance frameworks across our audited supplier network.
Environmental compliance standards for aluminum finishing in Vietnam mandate strict industrial wastewater treatment protocols for heavy metals and acid discharge, alongside alignment with RoHS and REACH regulations for exported components.
Global and Local Compliance Frameworks
Western procurement managers must ensure that their offshore production partners adhere to both local Vietnamese environmental laws and international compliance directives. For components destined for the European Union, the finishes must comply with the Registration, Evaluation, Authorisation and Restriction of Chemicals (REACH) and the Restriction of Hazardous Substances (RoHS) directives. For instance, traditional hexavalent chromium pre-treatments are widely restricted; modern compliant lines use trivalent chromium or completely chromate-free zirconium-based conversion coatings.
Anodizing plants produce acid-waste streams containing dissolved aluminum and nickel salts from the sealing step. Under Vietnamese environmental protection laws, these factories must operate advanced on-site wastewater treatment plants (WWTPs) to neutralize pH and precipitate heavy metals before discharging water into municipal systems.
When we conduct a Dolphin Audit, we verify the factory’s waste disposal contracts and environmental discharge permits. While powder coating provides superior initial color flexibility, hard anodizing remains the superior strategic choice for high-wear outdoor structural components facing abrasive environmental exposure, provided the supplier manages their chemical compliance transparently. This combination of strict local auditing and tariff-free access through Vietnam’s 16+ FTAs (including the EVFTA and CPTPP) allows US and EU buyers to build a clean, compliant supply chain.
FAQ
Can powder coating be applied over an anodized aluminum surface?
Powder coating can be applied over an anodized aluminum surface to combine the corrosion resistance of anodizing with the aesthetic benefits of powder paint. However, the anodized layer must be unsealed and completely clean to ensure the polymer coating adheres properly without delaminating.
How does the salt spray resistance of anodizing compare to powder coating?
Anodizing typically resists salt spray for 1,000 to 3,000 hours depending on the seal quality, whereas high-performance powder coatings complying with AAMA 2605 can exceed 3,000 hours of exposure. Anodizing preserves the original metallic appearance, while powder coating provides a thicker physical barrier against aggressive salt ions.
Do US Section 301 tariffs apply to finished aluminum components from Vietnam?
qualifying Vietnam-origin goods are not subject to US Section 301 Chinese punitive tariffs, making Vietnam-manufactured aluminum parts a highly cost-effective alternative to Chinese-manufactured components. This tariff advantage applies to both anodized and powder-coated assemblies, provided the country of origin is certified as Vietnam.
Conclusion
Selecting the right outdoor aluminum finish requires balancing environmental exposure, cost, and compliance. Our verified Vietnamese supplier facilities deliver high-quality, tariff-free surface finishes. Contact us to submit your RFQ and get an instant quote.