
Sourcing small-batch OEM stamping components often leads to unquoted setup fees, delayed production runs, and inconsistent part quality. Buyers need a reliable auditing framework to verify whether a supplier can genuinely handle flexible, low-volume orders without compromises.
Verifying supplier production flexibility for small-batch OEM stamping requires evaluating press changeover times, inspecting modular tooling capabilities, checking pilot-to-production pricing tiers, and auditing historical short-run delivery records before issuing a binding purchase order.
Key takeaways:
- Audit die changeover protocols and require Single-Minute Exchange of Die (SMED) targets under one hour.
- Evaluate hybrid production workflows that combine laser blanking with soft-tool bending for low volumes.
- Require itemized tooling quotes and tiered pricing for 100, 500, and 1,000-piece stamping runs.
- Verify quality controls using CMM inspection reports dedicated to short-run first-article parts.
What Questions Confirm a Stamping Supplier’s Small-Batch Capabilities?
When our audit engineers walk production floors, vague claims fall apart under technical scrutiny. We ask specific operational questions to separate low-volume press shops from mass-production factories.
Confirming a stamping supplier’s small-batch capability requires asking for specific press tonnages, average die changeover durations, in-house die modification lead times, and first-article inspection reports from previous 100-to-1,000-piece manufacturing runs.
What Is Small-Batch OEM Stamping Flexibility?
Small-batch OEM stamping is the manufacturing of custom metal components in low-to-medium volumes—typically between 100 and 2,500 units per order—using specialized press setups, modular dies, or hybrid sheet metal routes. True supplier flexibility means adjusting line scheduling and tooling strategies to deliver low-volume orders economically without forcing mass-production minimums.
| Technical Audit Question | High-Flexibility Indicator | Low-Flexibility Red Flag |
|---|---|---|
| Which press runs the batch? | Dedicated 45T–110T mechanical or hydraulic press | Unspecified high-tonnage progressive press |
| What is the die changeover time? | Standardized setup completed in under 60 minutes | Setup times exceeding 3 to 4 hours |
| How are low-volume prototypes made? | Hybrid laser-cut preforms with universal bending dies | Requires full progressive hard tooling upfront |
| How is quality verified? | Dedicated CMM and optical comparator checks | Sampling only during high-speed runs |
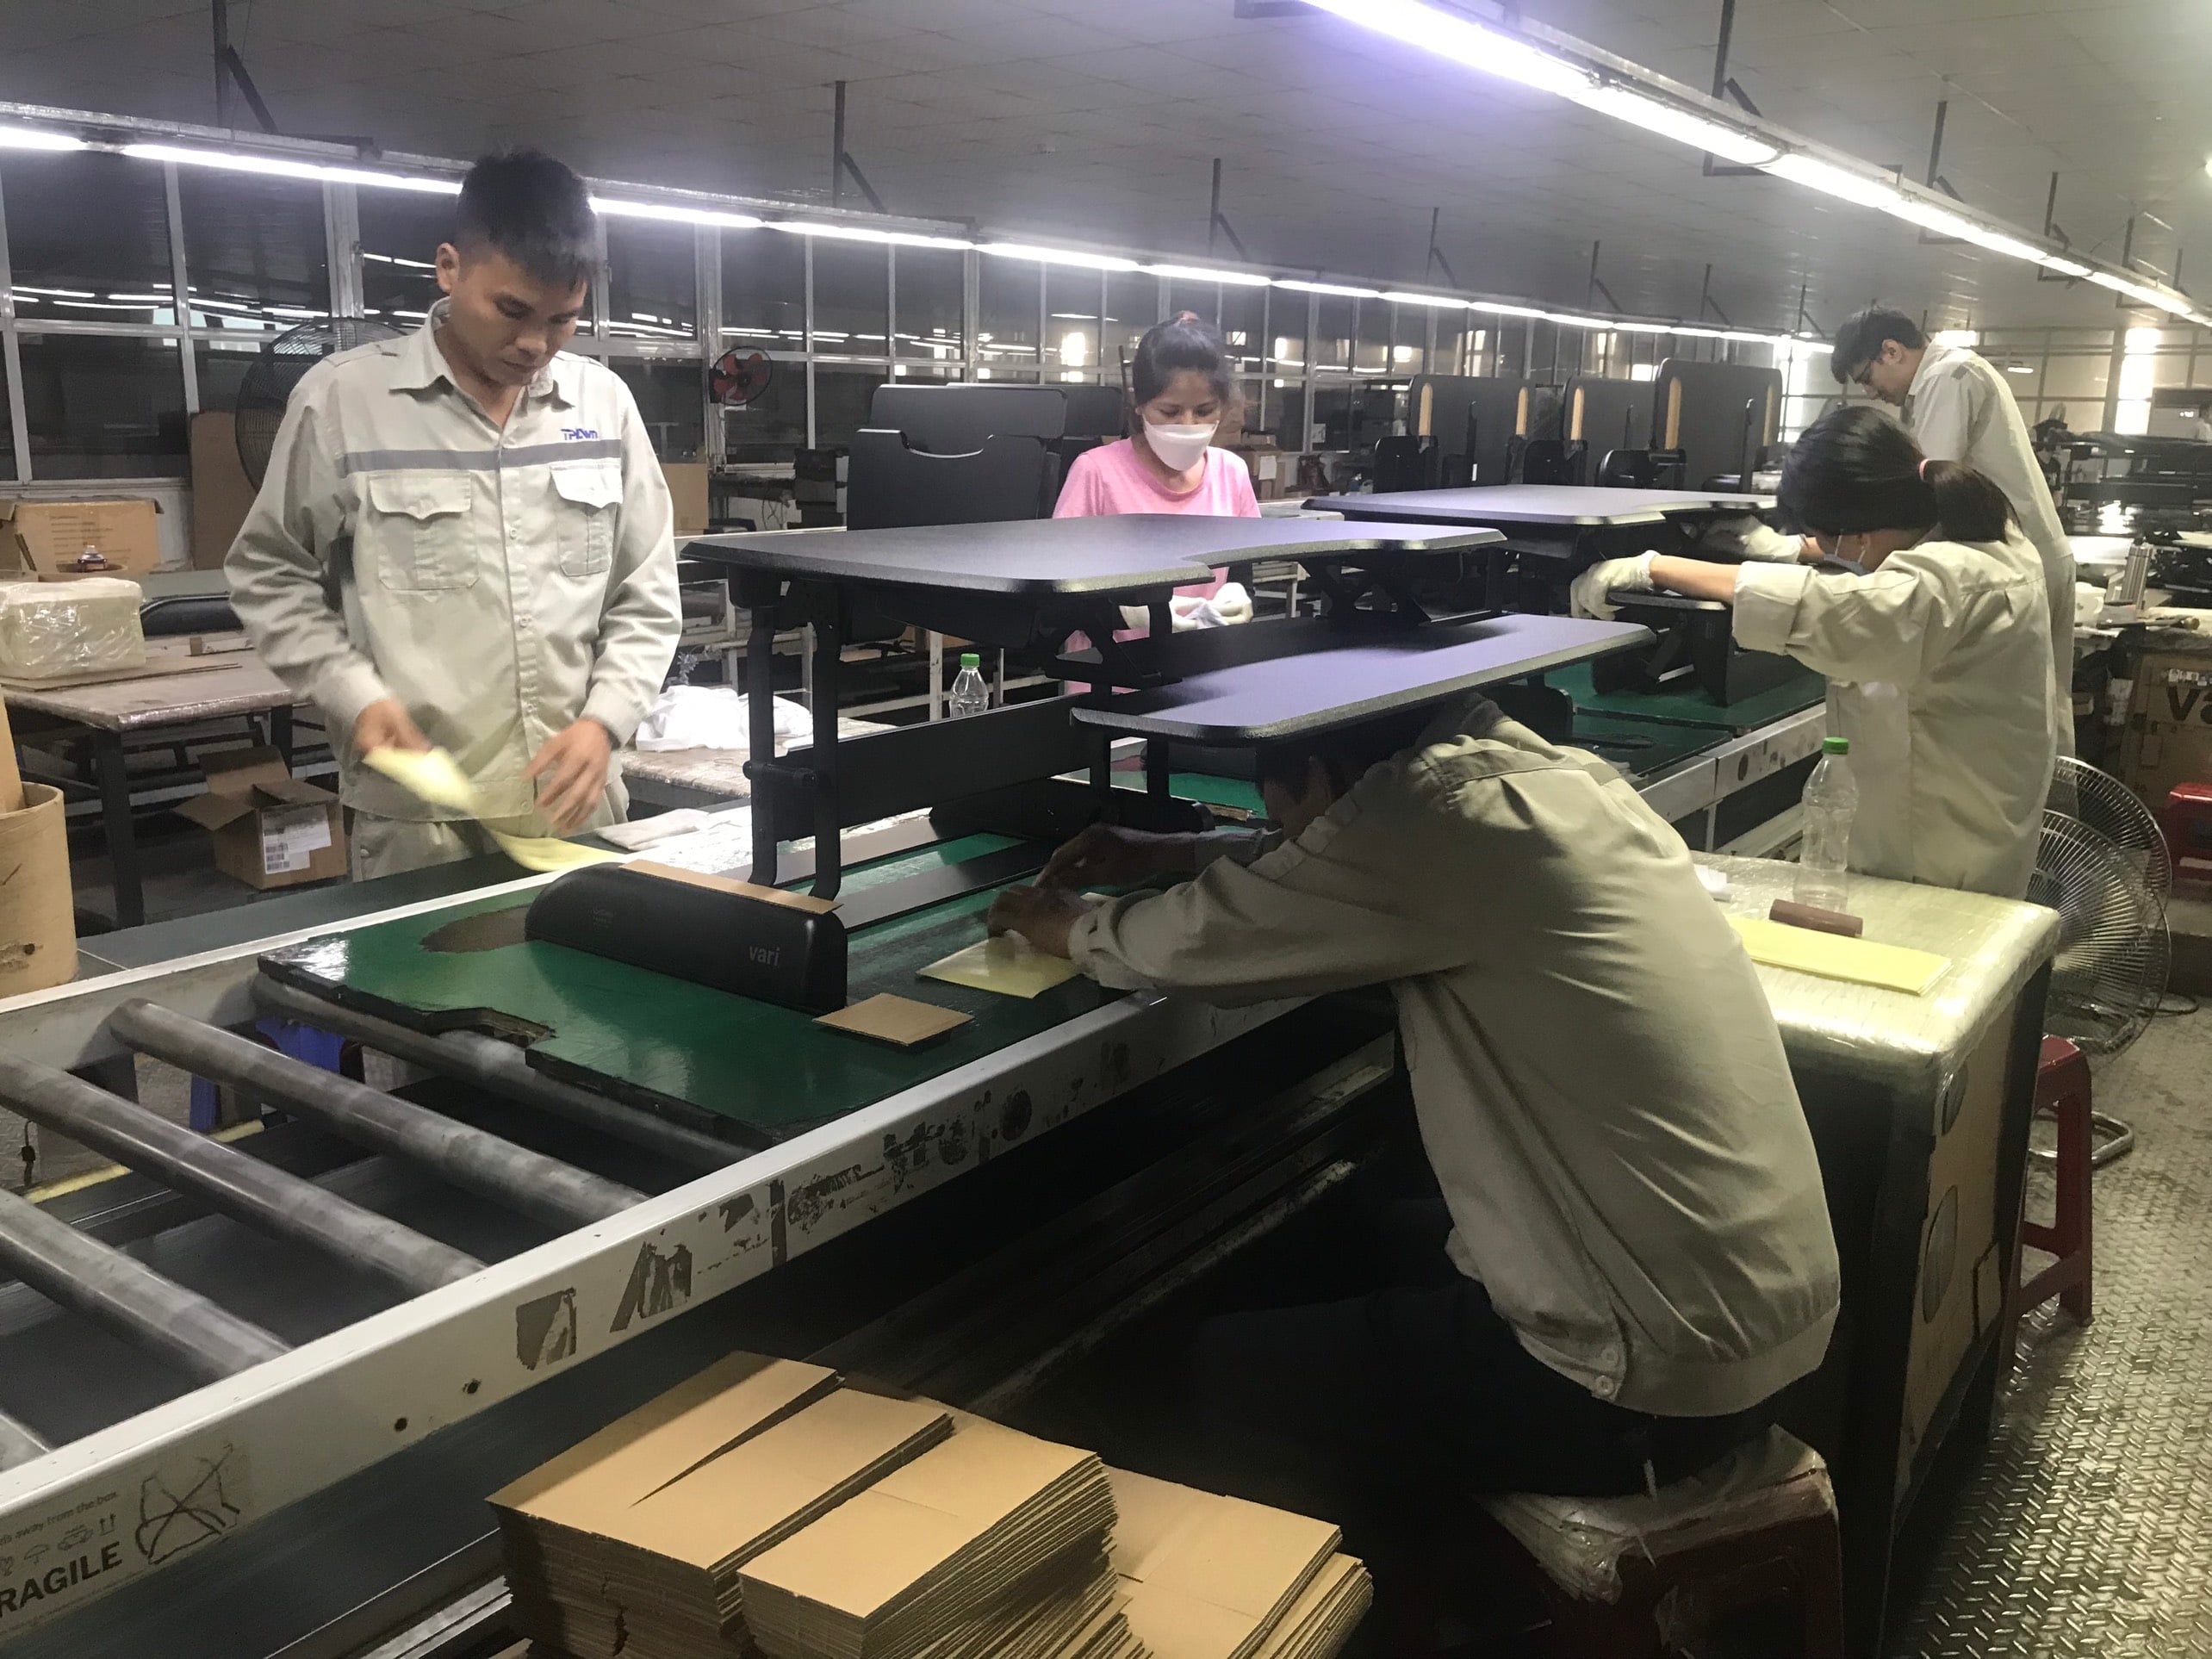
Across our network of vetted Vietnamese manufacturing facilities in Vietnam (listed in our supplier database), 13 factories specialize directly in stamping and bending and 17 specialize in sheet metal fabrication. Suppliers focused on low volume prioritize rapid die changeovers over raw strokes-per-minute output. When evaluating a factory, request proof of how they manage short production slots alongside long-run orders.
How Can You Test MOQ Flexibility Before Signing a Stamping Contract?
Sales teams often advertise flexible minimum order quantities without shop-floor alignment. Our audit engineers run tiered volume stress tests to verify genuine unit economics and production commitment.
Testing MOQ flexibility requires requesting itemized quotes across 100, 500, and 2,500-unit tiers, verifying whether die maintenance and setup fees are separated from piece prices, and negotiating pilot lot approval gates.
Evaluating unit price jumps across volume tiers exposes whether a supplier penalizes low-volume orders. In a healthy low-volume cost structure, piece prices decrease predictably as set-up costs amortize over larger quantities. If a 100-piece quote is ten times higher per unit than a 1,000-piece quote, the factory is pricing out small batches because their setup times are too long.
| Volume Tier | Tooling Strategy | Unit Cost Impact | Primary Risk Factor |
|---|---|---|---|
| 100–300 units | Laser cutting + universal press brake | Higher piece price, zero hard tooling | Operator manual bending variation |
| 500–1,000 units | Stage/compound dies in master die set | Moderate piece price, low tooling cost | Extended setup times on busy presses |
| 2,500+ units | Full progressive hard die | Lowest piece price, high initial tooling | Tooling modification costs if design changes |
Under international trade frameworks like the EVFTA and CPTPP, importing stamped metal components from Vietnam offers significant supply chain advantages, including relief from Section 301 Chinese punitive tariffs for qualifying goods on Vietnam-origin goods. However, buyers must ensure supplier pricing structures reflect real setup mechanics rather than arbitrary small-batch surcharges.
What Tooling and Changeover Strategies Enable Fast Low-Volume Runs?
High-speed progressive dies waste capital on small batches. We evaluate whether a press shop uses modular die plates, quick clamping systems, and hybrid production routes to cut lead times.
Low-volume OEM stamping flexibility relies on modular master die sets, quick die change clamping hardware, standardized press shut heights, and hybrid production workflows that combine laser blanking with secondary bending operations.
Modular Tooling vs. Hard Progressive Tooling
Modular tooling uses a standardized master die shoe installed permanently on the press. Machine operators swap small die inserts for specific forming, punching, or notch operations. This eliminates the need to build a full, multi-station progressive tool for a 500-piece batch, reducing upfront tooling investment by up to 70%.
Another effective strategy is hybrid sheet metal fabrication. Factory floor assets like laser cutters can produce flat blank shapes directly from CAD files without blanking dies. Press operators then use simple single-stage forming dies or press brakes to execute critical bends. For example, Lap Phuc Mechanical Production Trading, a verified stamping & bending manufacturer in our database, maintains CNC laser cutting machines and bending equipment on file. This combination enables rapid processing of low-volume structural brackets without building complex progressive dies.
Of the vetted Vietnamese manufacturing facilities with equipment lists on file in our database, 29 feature precision bending machines and 7 list CNC laser cutting machines. Utilizing factories with both laser cutting and secondary forming equipment ensures your short-run orders move smoothly from CAD to finished part.
What Operational Red Flags Indicate Poor Stamping Flexibility?
During our 50-point Dolphin Audit inspections, specific shop-floor bottlenecks signal whether a supplier will sideline your short-run orders when mass-production jobs arrive.
Operational red flags in small-batch OEM stamping include cluttered die storage, setup times exceeding two hours, lack of dedicated short-run quality control equipment, and complete outsourcing of tool maintenance and die repairs.
Auditing Shop-Floor Organization and Quality Assets
A disorganized press shop cannot support rapid changeovers. Look at die storage racks during a factory visit. If dies sit on the floor covered in grease without standardized shut-height labels, die changeovers will take hours. Systematic factories use color-coded quick-change clamps and pre-heated die beds to achieve Single-Minute Exchange of Die (SMED) benchmarks.
Quality verification assets are equally critical. Small production runs require swift first-article inspection (FAI) to approve press setups before the batch finishes. Factories like Smctech maintain punching machines and CNC laser cutting on file to support agile production schedules. Across our audited supplier network, 8 factories maintain 3D CMM equipment on file and 6 feature standard CMM machines. These metrology tools enable engineers to verify complex bend radii, hole center distances, and springback allowances on short runs within minutes of setup.
FAQ
What is a typical lead time for small-batch OEM stamping in Vietnam?
Small-batch OEM stamping lead times in Vietnam typically range from 2 to 4 weeks for initial samples using hybrid tooling, and 1 to 2 weeks for repeat runs. Exact lead times are confirmed per project during quoting based on material availability and tooling complexity.
Should buyers amortize tooling costs or pay upfront for low-volume stamping?
Buyers should pay for low-volume stamping tooling upfront as a separate line item rather than amortizing costs into unit prices. Separate tooling payments ensure part ownership, prevent unit price inflation on repeat orders, and clarify exact piece-price economics across changing order volumes.
How does laser cutting complement small-batch OEM metal stamping?
Laser cutting complements small-batch stamping by fabricating flat preforms without requiring dedicated blanking dies. This hybrid workflow drastically cuts upfront tooling expense, enables rapid design iterations, and reduces press setup time to secondary forming and bending operations.
Conclusion
Verifying supplier production flexibility requires detailed audits of changeover procedures, tooling setups, and quality systems. By testing pricing structures and shop-floor capabilities, procurement teams secure reliable short-run production. Submit your engineering drawings today to get an instant quote.