As global supply chains realign, Vietnam has developed into a serious destination for plastic injection molding — not a low-complexity fallback. Driven by foreign direct investment from South Korea, Japan, and the US, the local ecosystem now supports multi-shot molding, medical cleanrooms, and in-house tooling. This guide is written for the design engineer or sourcing manager who needs to know what to look for on the floor before committing a tool.
To qualify a Vietnamese injection molder, verify the press mix covers your part with utilization headroom, confirm racked and logged mold storage with in-house repair, match certifications to your application, and require a metrology lab plus a First Article Inspection before you cut steel.
Key takeaways:
- Vietnam’s molding base spans micro-molding to 3000T presses, with 2K, insert, and overmolding widely available at Tier 1 and Tier 2 suppliers.
- The tool — not the press — is your biggest risk and your biggest asset. How a factory stores, maintains, and logs molds predicts whether you get 100,000 shots or 30,000.
- Match the certification to the application: ISO 9001 is table stakes, IATF 16949 for automotive, ISO 13485 plus a validated cleanroom for medical.
- A quotable molding RFQ needs resin grade, annual volume, cavitation intent, cosmetic/appearance spec, and the acceptance standard (AQL level).
- Qualify with an equipment-level audit and a First Article Inspection, not a certificate scan.
What Does a Vietnamese Molding Factory Look Like Inside?
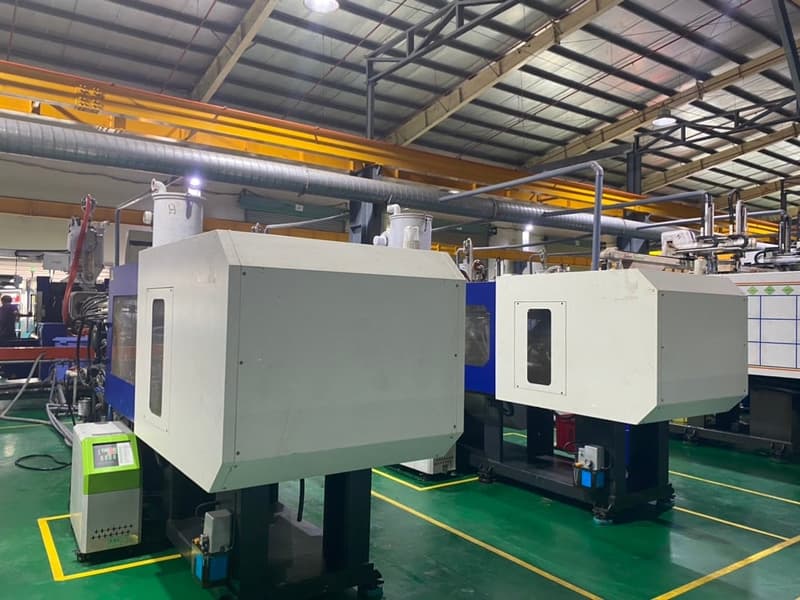
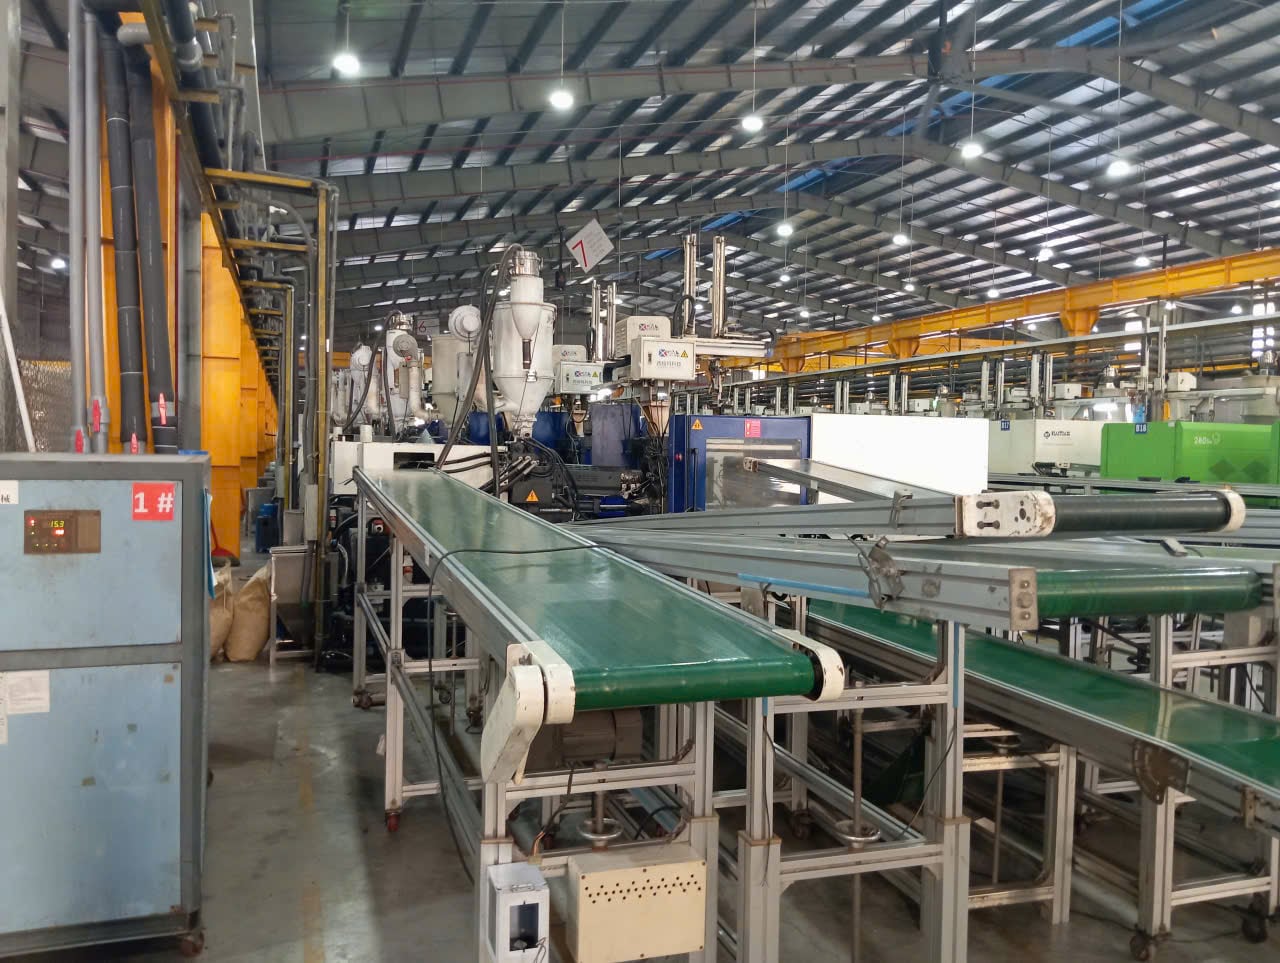
A modern Vietnamese molding shop looks much like its Korean or Japanese counterpart — because many were built with that capital and those customers in mind. Presses run under real-time process monitoring, robots handle sprue picking and part extraction, and tooling is stored in dedicated racks rather than stacked in a corner.
A modern Vietnamese molding shop mirrors its Korean or Japanese counterpart: presses run under real-time process monitoring, robots handle sprue picking and part extraction, and tooling sits in dedicated racks rather than stacked in a corner — because many were built with that capital and those customers in mind.
1. Machinery and tonnage range
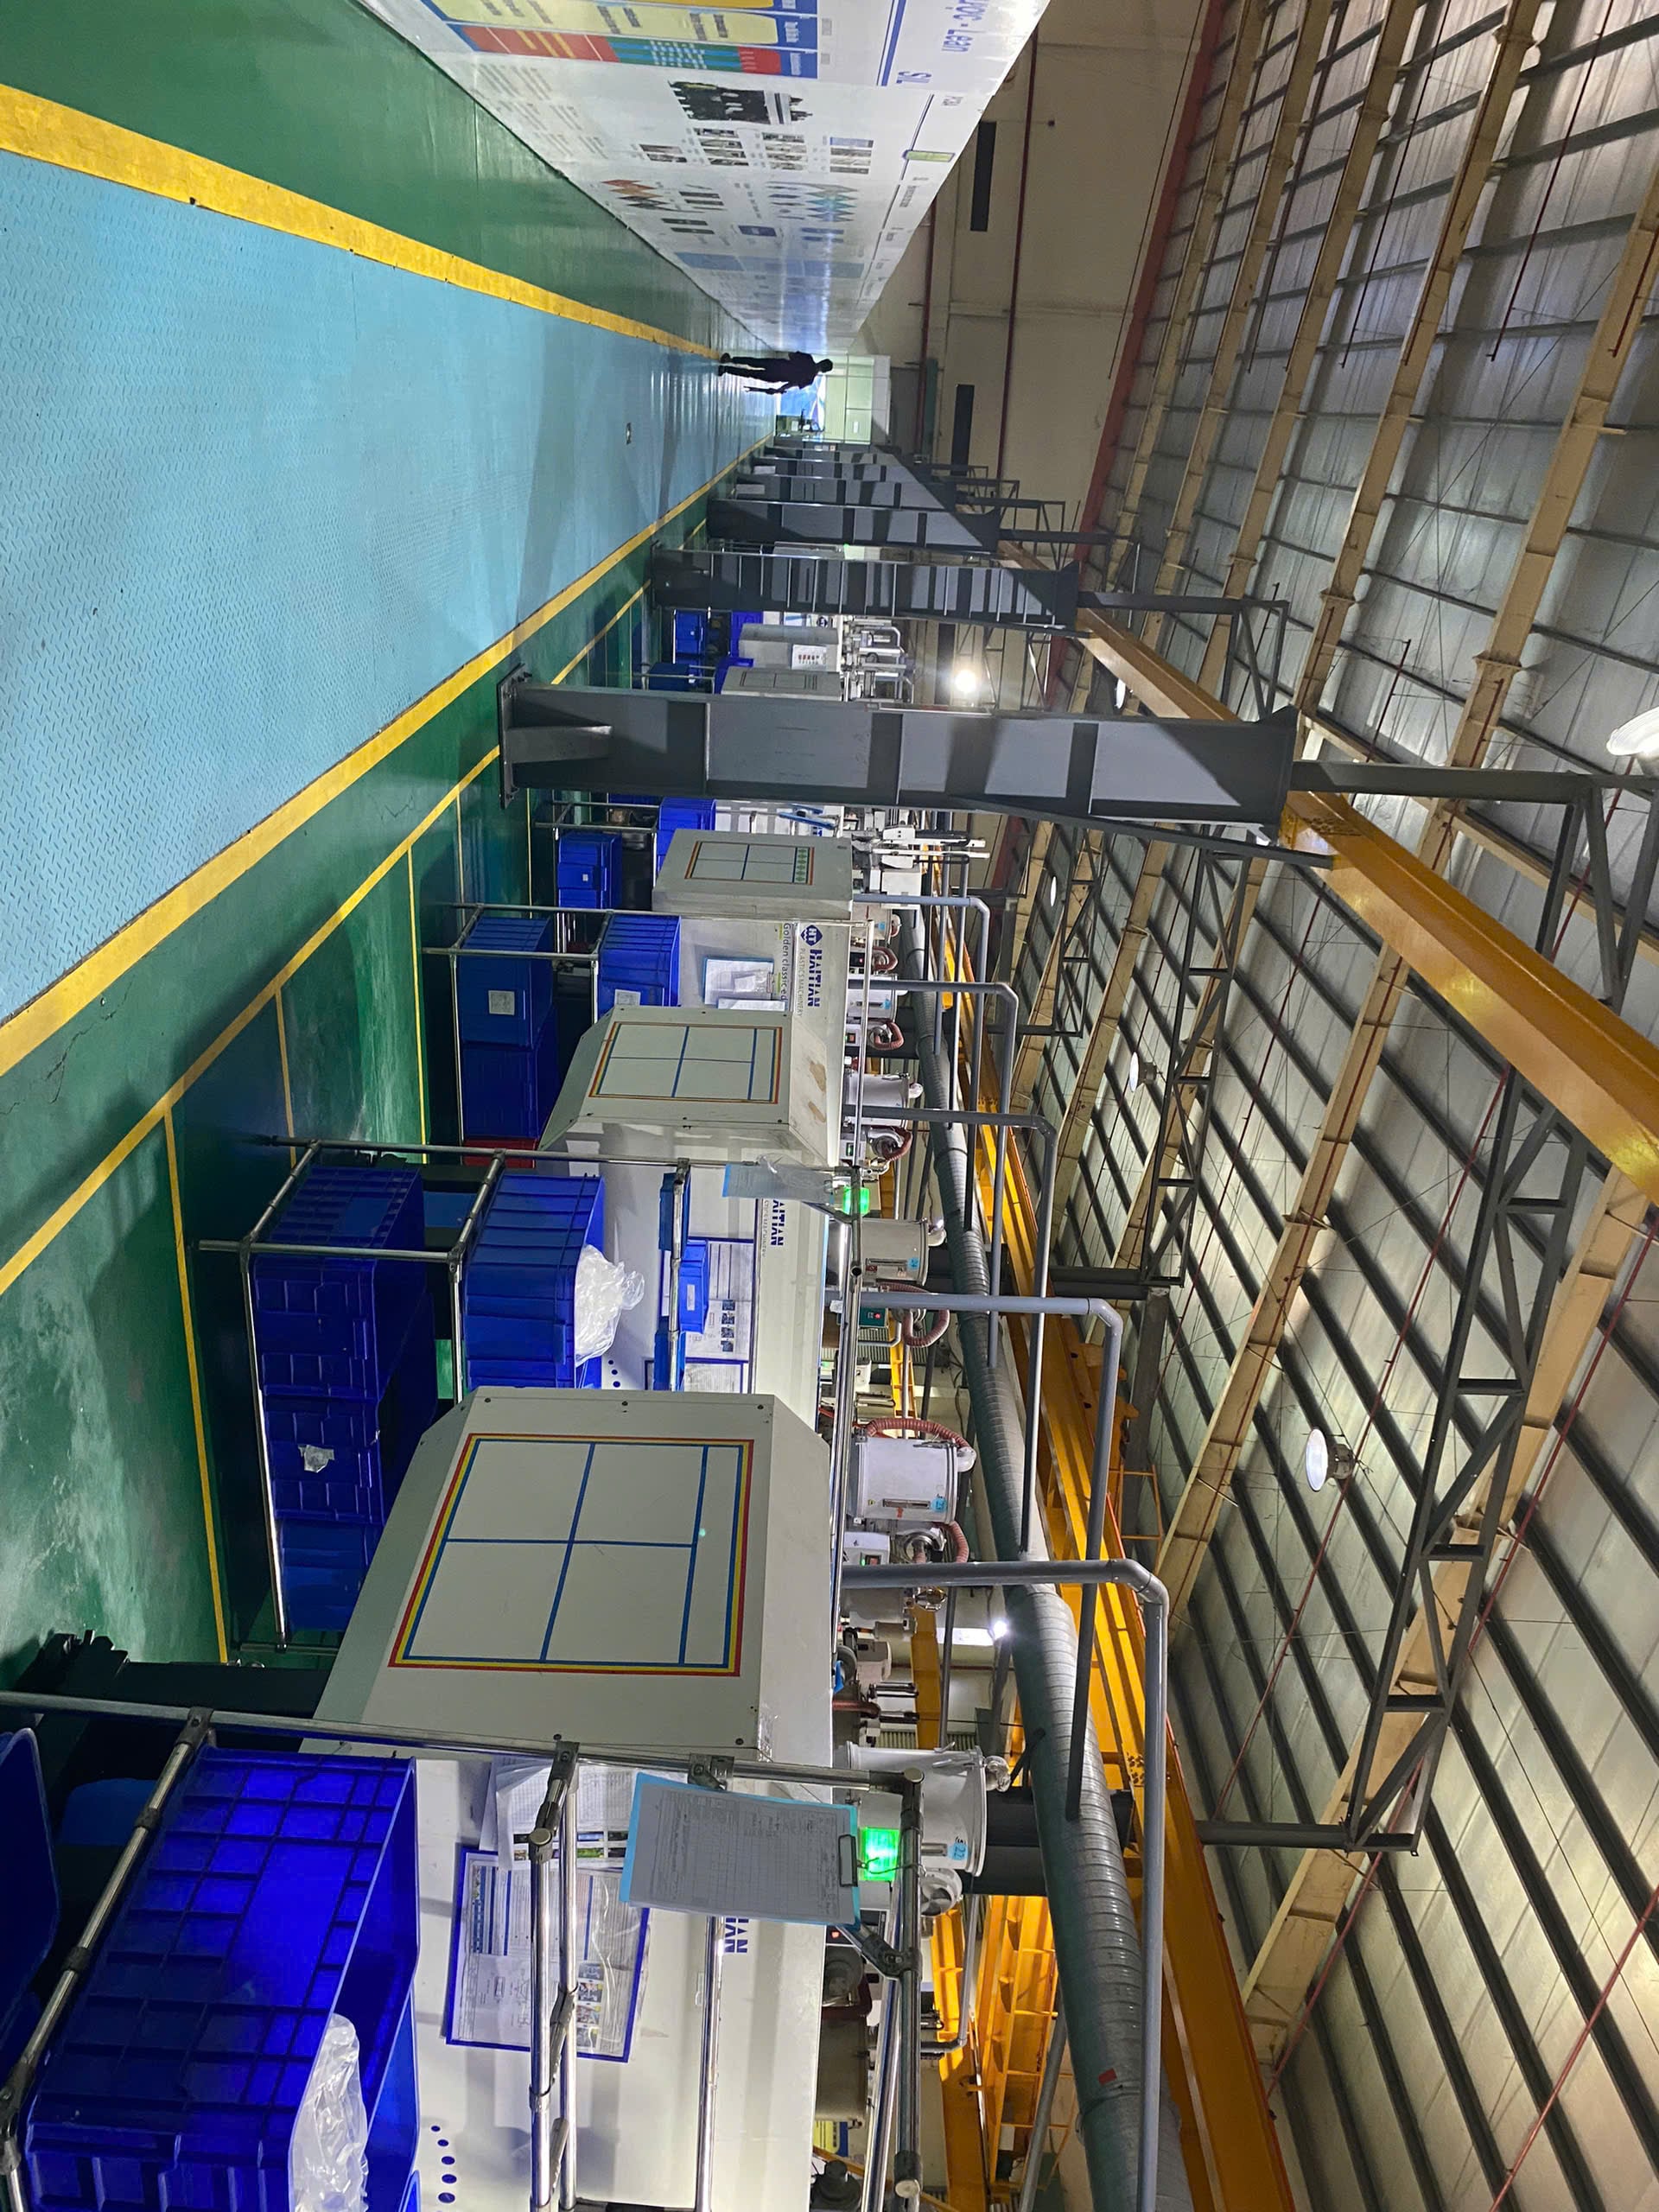
Verified suppliers operate a wide press range, accommodating everything from micro components to large automotive panels.
- Tonnage: 50T for small precision parts up to 3000T+ for large structural moldings
- Brands: facilities are commonly equipped with Engel, KraussMaffei, Arburg, Sumitomo, and high-spec Haitian presses
- Automation: robotic sprue pickers and part-handling systems that stabilize cycle time and reduce the labor content of each shot
The number that matters for your part is not the biggest press on the floor — it is whether the right tonnage sits in the machine mix with utilization headroom. A shop that has to run your 200T job on an idle 800T press will quote defensively.
2. Specialized molding capabilities
Capabilities extend well beyond single-shot molding:
| Process | What it does | Typical use |
|---|---|---|
| Double-shot (2K) | Two materials or colors in one cycle | Soft-touch grips, seals, multi-color housings |
| Insert molding | Encapsulates metal inserts in the shot | Threaded brass bosses, contacts, terminals |
| Overmolding | Bonds an elastomer over a rigid substrate | Handles, gaskets, cosmetic overlays |
| Gas-assist | Hollow sections in thick features | Handles, structural panels, sink-free ribs |
3. Tooling and mold discipline
A reliable molding partner is defined by how it treats tooling. The best Vietnamese factories run climate-controlled mold storage and in-house maintenance shops, and many build and validate steel locally using imported 5-axis CNC and EDM equipment before mass production begins.
Ask three questions on every audit: Are molds racked and logged with shot counts? Is there in-house polishing and repair? Is storage climate-controlled to prevent rust on steel tools? For a deeper treatment, see our injection mold tooling guide.
4. Quality control (QCLDM)
Match certifications to your application, and verify the lab that backs them:
- ISO 9001:2015 — baseline quality management (expect it everywhere)
- IATF 16949 — automotive; implies PPAP discipline and SPC
- ISO 13485 — medical devices; look for a validated Class 7/8 cleanroom
Well-equipped labs run CMMs, optical comparators, and melt-flow indexers to confirm both resin properties and dimensional accuracy. Follow good injection molding design rules upstream and you reduce the defects those labs have to catch.
How Do I Build a Quotable Molding RFQ?
Molding quotes swing widely when the request is ambiguous, because estimators price uncertainty as risk. A clean package tightens both price and lead time. Include:
A quotable molding RFQ carries resin grade and supplier, annual volume and cadence, a cosmetic/appearance spec, tolerances referenced to a standard, an AQL acceptance level, and any regulatory needs — sent as a STEP file plus a dimensioned 2D drawing so estimators price the part, not the uncertainty.
- Resin grade and supplier, not just “ABS” — flow, filler, and colorant drive cycle time and tool wear
- Annual volume and order cadence — this sets cavitation and the right press class
- Cosmetic/appearance spec — gloss, texture (e.g. MoldTech), gate and knit-line acceptance
- Tolerances referenced to a standard, tight only where function requires it
- Acceptance standard — AQL level for cosmetic and dimensional defects
- Regulatory needs — food-contact, medical, flammability (UL) ratings
Send a STEP file plus a dimensioned 2D drawing carrying the notes above. For a cost breakdown of how these choices move the number, see injection molding cost in Vietnam.
What Actually Drives My Molded-Part Price?
Two decisions set most of a molded part’s unit cost, and both are yours to make before the RFQ goes out: cavitation and cycle time.
Two decisions set most of a molded part’s unit cost, and both are yours before the RFQ: cavitation — how many parts a tool makes per shot — and cycle time, driven by wall thickness, cooling, and resin. Match cavitation to annual volume and design for uniform walls.
Cavitation is how many parts a tool produces per shot. A single-cavity tool is cheap to build but expensive per part; a multi-cavity or family tool costs more upfront but amortizes across volume. The right choice follows your annual volume — under-caviting a high-runner wastes press hours, over-caviting a low-runner wastes tooling capital.
Cycle time is driven by wall thickness, cooling, and resin. Thick sections cool slowly and dominate the cycle; uniform walls, generous radii, and good cooling-channel design shave seconds off every shot, which compounds across a production run. A molder running scientific-molding process control will quote a tighter, more defensible cycle than one relying on operator feel.
The takeaway for buyers: design decisions made at the CAD stage — wall uniformity, draft, gate location — are locked into the unit price for the life of the tool. Involve the molder’s engineers early, before the steel is cut.
How to Qualify a Vietnamese Molder
Before you cut steel, confirm every item:
- Press tonnage range covers your part with utilization headroom
- Documented tool maintenance and shot-count logs
- Climate-controlled, racked mold storage
- In-house or nearby tooling repair capability
- Certification matched to application (IATF / ISO 13485 as needed)
- Metrology lab with CMM and resin verification (melt-flow)
- First Article Inspection agreed before mass production
- A physical audit report and QCLDM tier on file
Frequently Asked Questions
What press tonnage do I need for my part?
Tonnage scales with projected area and material — a rough rule is 2–5 tons of clamp force per square inch of projected part area, higher for stiff or filled resins. The molder confirms it with a mold-flow analysis. What you should verify is that the required tonnage exists in the shop’s mix with capacity to spare.
Can Vietnamese factories build the tool, or only run it?
Many Tier 1 molders build tools in-house using 5-axis CNC and EDM, and validate the steel locally before production. Others partner with dedicated tool shops in the same industrial zone. Either can work — what matters is documented tool maintenance and a clear owner for repairs over the tool’s life.
Are cleanroom and medical molding realistic in Vietnam?
Yes. Several audited facilities run ISO 13485 systems with validated Class 7 and Class 8 cleanrooms for medical components. As always, confirm the certification is current and that the cleanroom is validated for your specific product class.
How do I protect my tooling investment offshore?
Contract clearly on tool ownership, require shot-count logging and scheduled maintenance, and work through a single accountable counterparty. DEWIN contracts through a US Delaware LLC, so your tooling agreement sits under US jurisdiction rather than with an overseas entity.
Vietnam’s molding sector has the presses, the tooling depth, and the quality systems demanding programs require — the discipline that pays off is verifying them before the tool is cut. Explore the injection molding service, browse the verified partner facility directory, or get an instant quote with your drawings and resin spec.